High-Performance Reactive Extruder Solutions
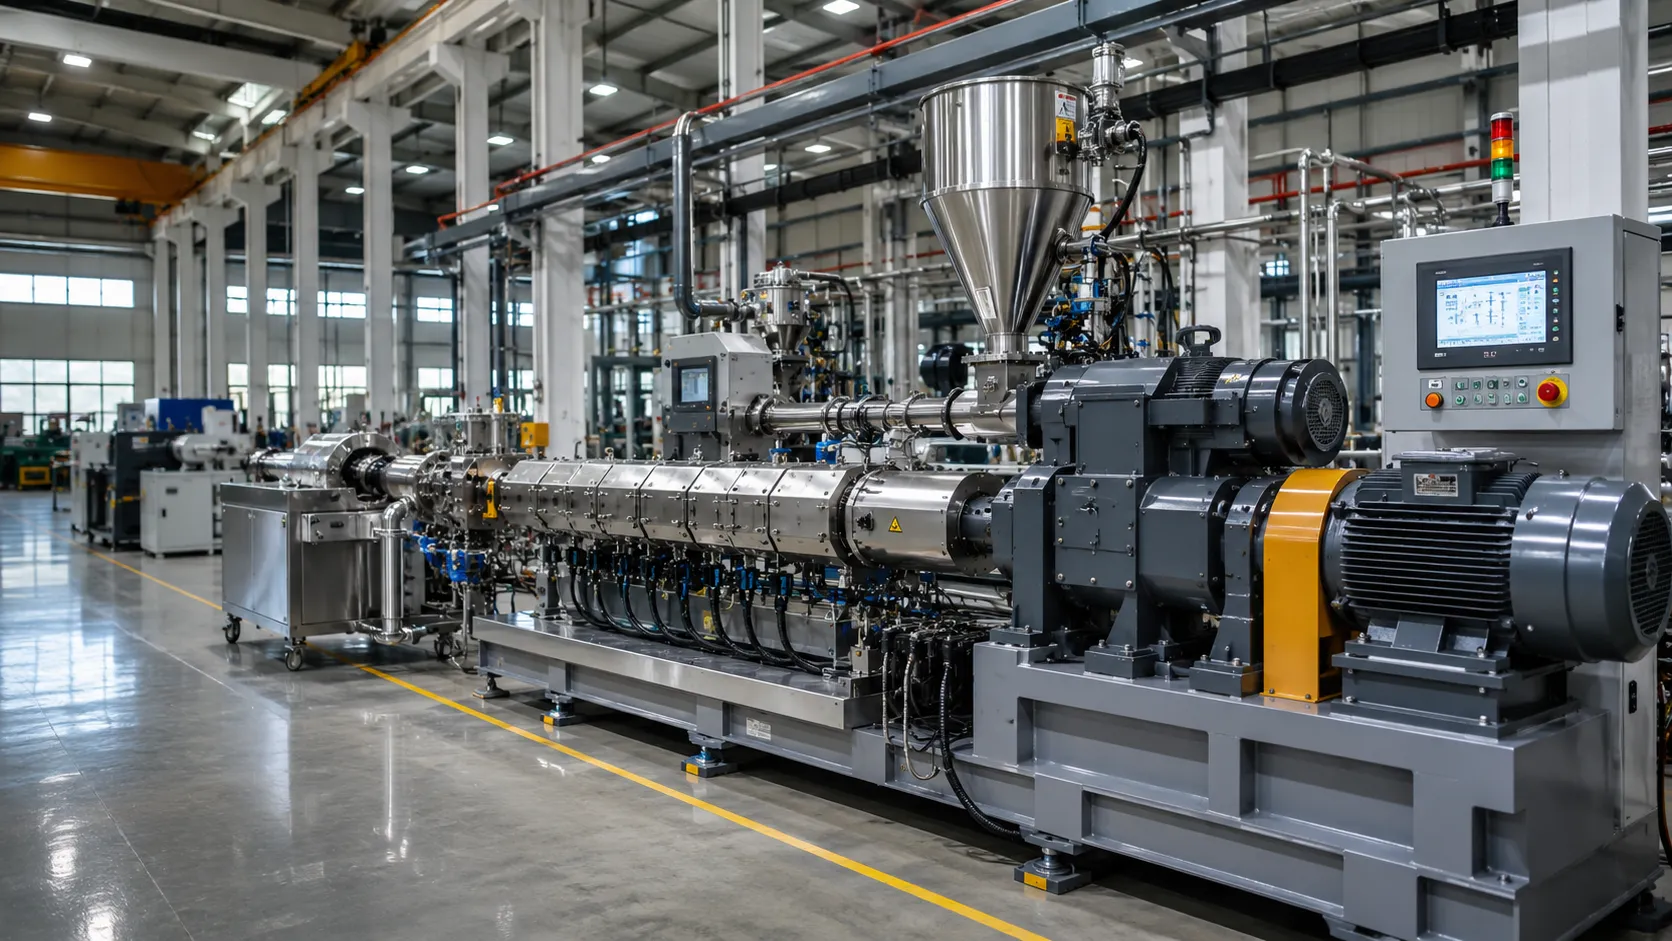
UET has built twin-screw reactive extruders since 2005. Today our SHJ series runs TPU, PLA/PBAT and grafting lines in more than 80 countries — sized from 0.5 kg/h lab units to 3,250 kg/h production lines.
20+ Years Experience
80+ Countries
ISO 9001 Certified
CE Certified
3,250
kg/h Max Output
±1.5°C
Temp Precision
30-40%
Energy Saving
99.5%
Operation Uptime
What Is a Reactive Extruder?
A reactive extruder (REX) turns a co-rotating twin-screw extruder into a continuous chemical reactor. Monomers, polymers and additives are metered into the barrel, and as they melt and mix, the reaction actually happens inside the machine — polymerization, grafting, cross-linking or compatibilization — before the melt is devolatilized and pelletized in the same pass.
Why does that matter? A batch reactor takes hours per batch and usually needs solvents you later have to recover. A reactive extruder finishes the same chemistry in minutes, solvent-free, with much tighter control over residence time and temperature. That is exactly why TPU, biodegradable resins and most graft copolymers are increasingly made this way.
As the reactive extruder manufacturer, we configure every line around your chemistry: screw layout, L/D ratio, side-feeding positions, venting and temperature profile. Send us your formulation and target output — our application engineers return a proposed screw configuration together with your quotation.
Typical Reactive Processes
- Bulk polymerization (TPU, PLA, PMMA)
- Grafting — e.g., maleic anhydride (MAH) onto PP/PE
- Cross-linking — silane, peroxide (XLPE cable compounds)
- Reactive blending & compatibilization
- Devolatilization & purification of recycled polymers
- Chain extension of biopolymers
Materials We Process
TPU
PLA
PBAT
PBS
PA6/PA66
PC
PBT
ABS
PP
PE
EVA
PVC
Masterbatch
Nanocomposites
Reactive Extrusion Pain Points — and How We Solve Them
Six problems we hear most often from plants running reactive processes, and what our SHJ line does about each one.
Batch-to-Batch Quality Drift
A batch reactor rarely repeats itself exactly. Our lines hold melt temperature within ±1.5 °C and keep residence time distribution narrow, so viscosity and conversion stay on spec — shift after shift.
Compliance & Market Access Risk
Food-contact, medical and EU exports demand documented compliance. We supply SS316L contact parts on request and ship CE, ISO 9001 and RoHS documentation with every line.
Maintenance Eating Your Margin
Bimetallic barrels (HRC 60–65) and powder-metallurgy screw elements last roughly 3× longer in abrasive recipes. Most customers run 180+ days between overhauls.
Formulas That Don’t Fit the Machine
Modular barrels and a 32:1–68:1 L/D range mean we reconfigure the same machine for a new recipe — side feeder here, extra vent there — instead of you buying another extruder.
Cross-Contamination Between Runs
Self-cleaning screw geometry plus optimized purge procedures get you from one color or grade to the next without a full teardown.
Downtime You Can’t Afford
Over-spec’d gearboxes (T/A³ ≤ 8), Siemens/ABB electricals and 24/7 engineer support keep our installed fleet above 99% uptime.
Laboratory, Pilot & Industrial Reactive Extruders for Sale
Three proven scales, one platform — so your lab results transfer to production without surprises.
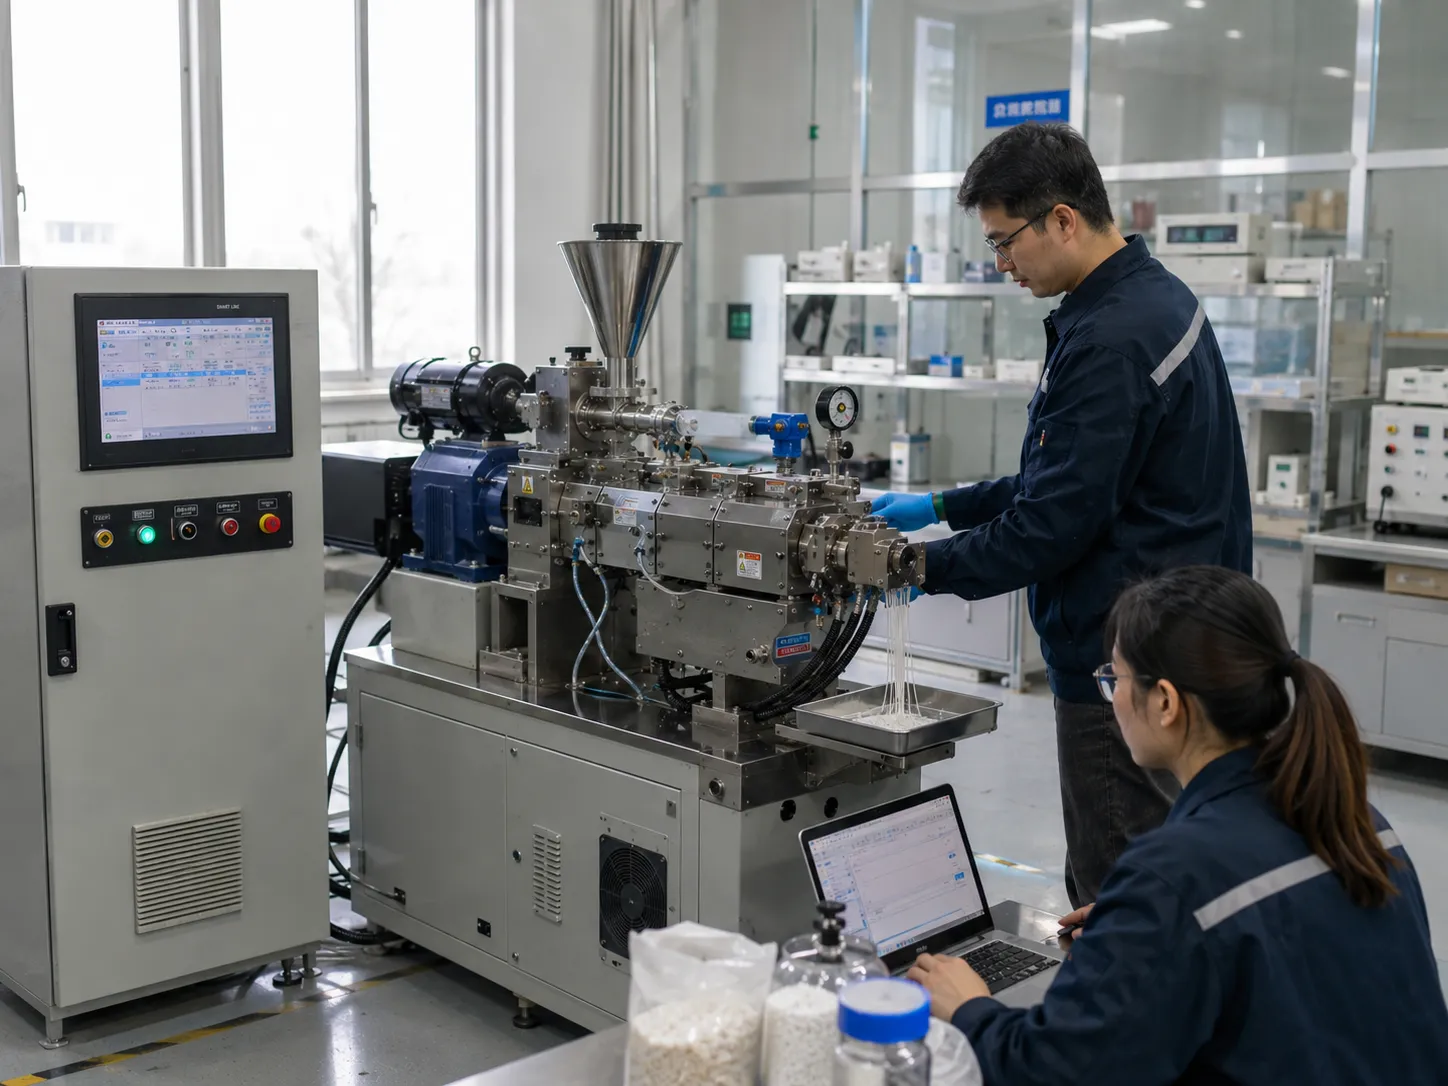
R&D & Testing
Get Quote
Laboratory Scale
Runs on a few kilograms of material, so you can screen formulations before committing production resin. Traceable parameters scale directly to bigger models.
- Output: 0.5 – 15 kg/h
- Screw Diameter: 21.7 – 35.6 mm
- Motor: 4 – 22 kW
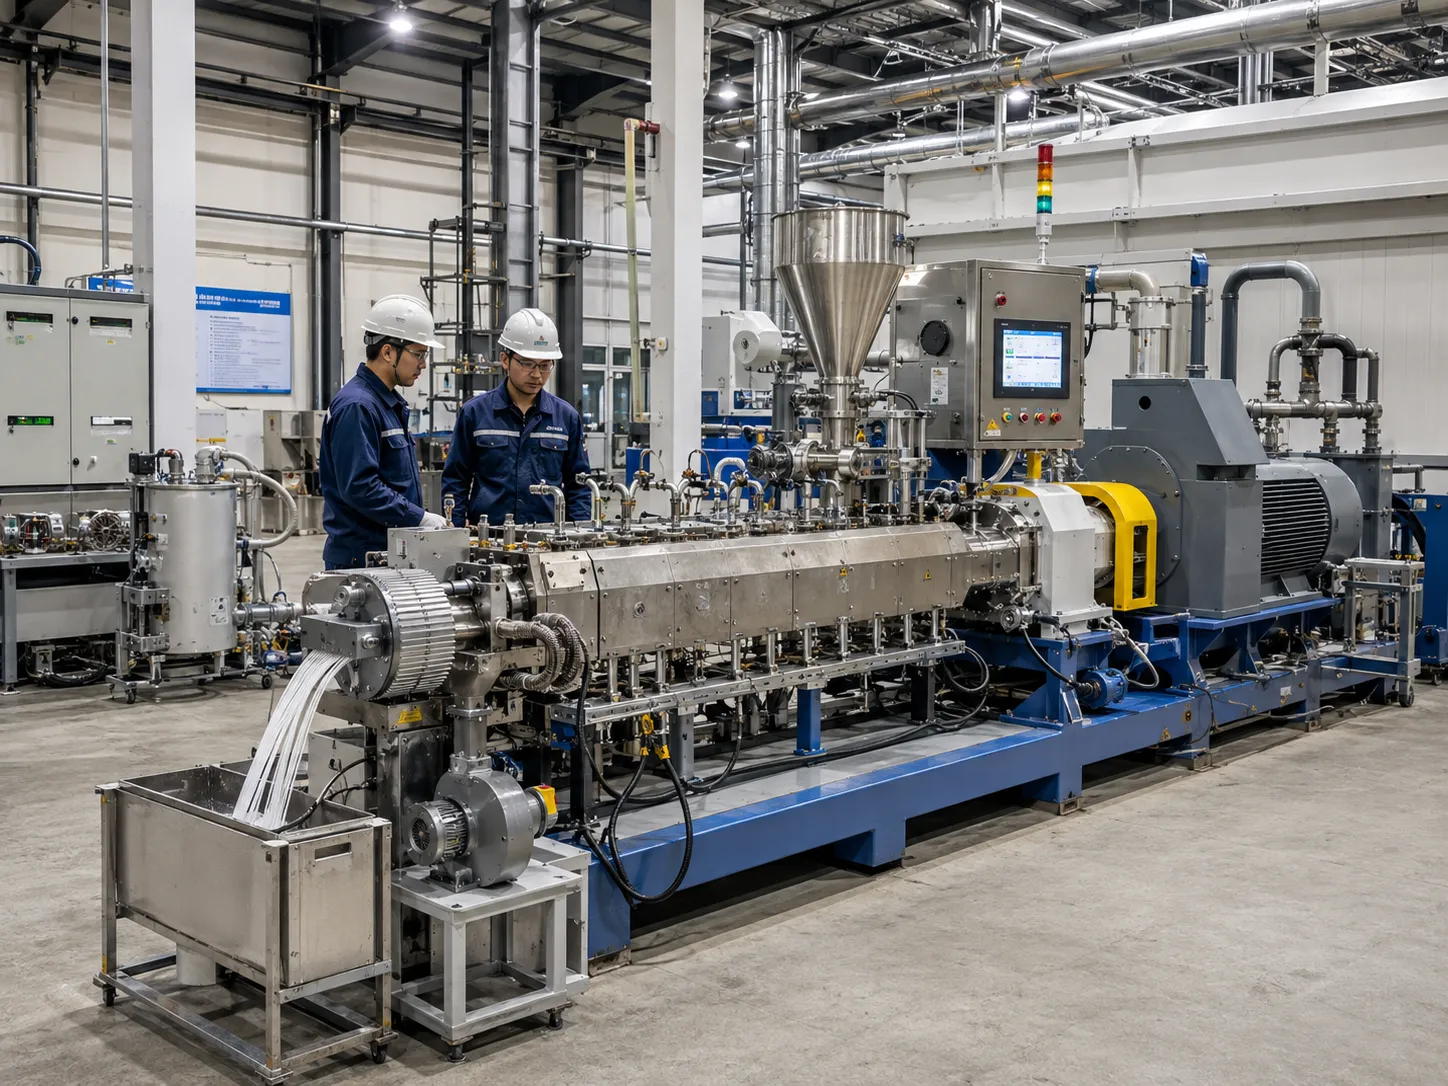
Pilot Production
Get Quote
Intermediate Pilot Scale
The bridge between lab and plant. Big enough to produce saleable trial lots for customers, small enough to change conditions quickly while you lock the process window.
- Output: 20 – 200 kg/h
- Screw Diameter: 35.6 – 50.5 mm
- Motor: 22 – 55 kW
Mass Production
Get Quote
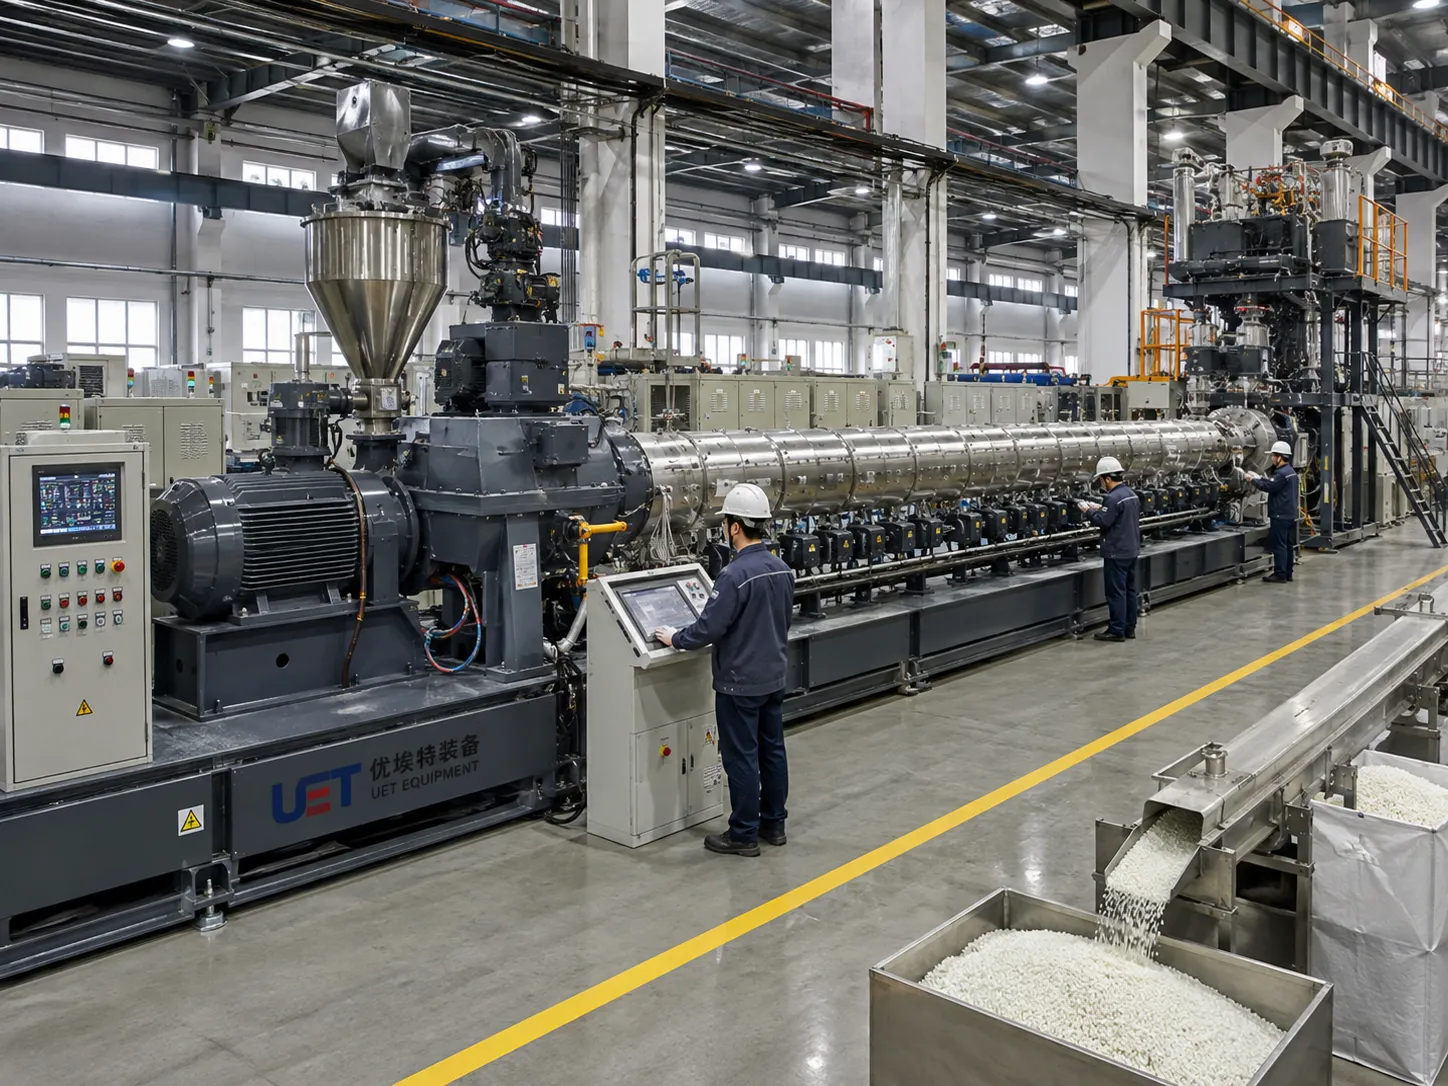
Industrial Production
Built for 24/7 duty: heavy gearboxes, redundant heating zones and downstream pelletizing matched to the same output curve. This is the machine your P&L is counting on.
- Output: 300 – 3,250 kg/h
- Screw Diameter: 62.4 – 133 mm
- Motor: 55 – 500 kW
Complete Model Specifications
SHJ Series Co-Rotating Twin Screw Reactive Extruders
| Model | Screw Diameter (mm) | L/D Ratio | Screw Speed (RPM) | Motor Power (kW) | Torque Grade (T/A³) | Output (kg/h) |
|---|---|---|---|---|---|---|
| SHJ-20 | 21.7 | 32 – 68 | 400 – 600 | 4 | 5.8 | 0.5 – 15 |
| SHJ-30 | 30.0 | 32 – 68 | 400 – 600 | 11 | 5.8 | 5 – 50 |
| SHJ-36 | 35.6 | 32 – 68 | 500 – 800 | 15 – 22 | 5.7 | 20 – 80 |
| SHJ-42 | 41.2 | 32 – 68 | 500 – 800 | 22 – 37 | 5.7 | 50 – 120 |
| SHJ-50 | 50.5 | 32 – 68 | 500 – 800 | 37 – 55 | 5.8 | 80 – 200 |
| SHJ-63 | 62.4 | 32 – 68 | 500 – 800 | 55 – 90 | 5.8 | 150 – 350 |
| SHJ-72 | 71.0 | 32 – 68 | 500 – 800 | 90 – 160 | 5.7 | 300 – 600 |
| SHJ-85 | 82.0 | 32 – 68 | 500 – 600 | 160 – 200 | 5.7 | 600 – 1000 |
| SHJ-92 | 91.0 | 32 – 68 | 500 – 600 | 250 | 5.8 | 840 – 1600 |
| SHJ-135 | 133.0 | 32 – 68 | 650 – 750 | 400 – 500 | 5.8 | 1950 – 3250 |
Note: Every model can be re-specified — L/D ratio (32:1–68:1), barrel material (bimetallic or SS316L), feeder and vent positions — around your reaction. Tell us the chemistry; we’ll size the machine.
Technical Advantages of UET Reactive Extruders
Not marketing claims — the design decisions that decide whether your reaction converts on spec, at full output, three years from now.
High Torque Density
T/A³ ≤ 8. That headroom is what lets you run high-viscosity TPU or 40% glass fiber at full output without torque alarms.
±1.5 °C Zone Control
Each barrel zone runs its own PID heating/cooling loop, so heat-sensitive chemistry like PLA stays inside its narrow window.
L/D 32:1–68:1, Your Choice
Longer L/D when the reaction needs residence time, shorter when it doesn’t. We recommend the smallest setup that does the job.
Self-Cleaning Co-Rotating Screws
Intermeshing elements wipe the barrel wall continuously — better heat transfer, less gel formation, faster purging between grades.
Real Devolatilization
Two to four vent ports under vacuum strip unreacted monomer and volatiles, so conversion and odor specs are met at the die.
Built & Tested In-House
Every reactive extruder runs a 72-hour full-load test — plus a material trial with your recipe — before crating. Inspect in person or by video.
Reactive Extruder Applications & Industries Served
Eight application families our application engineers run in the test lab every week.
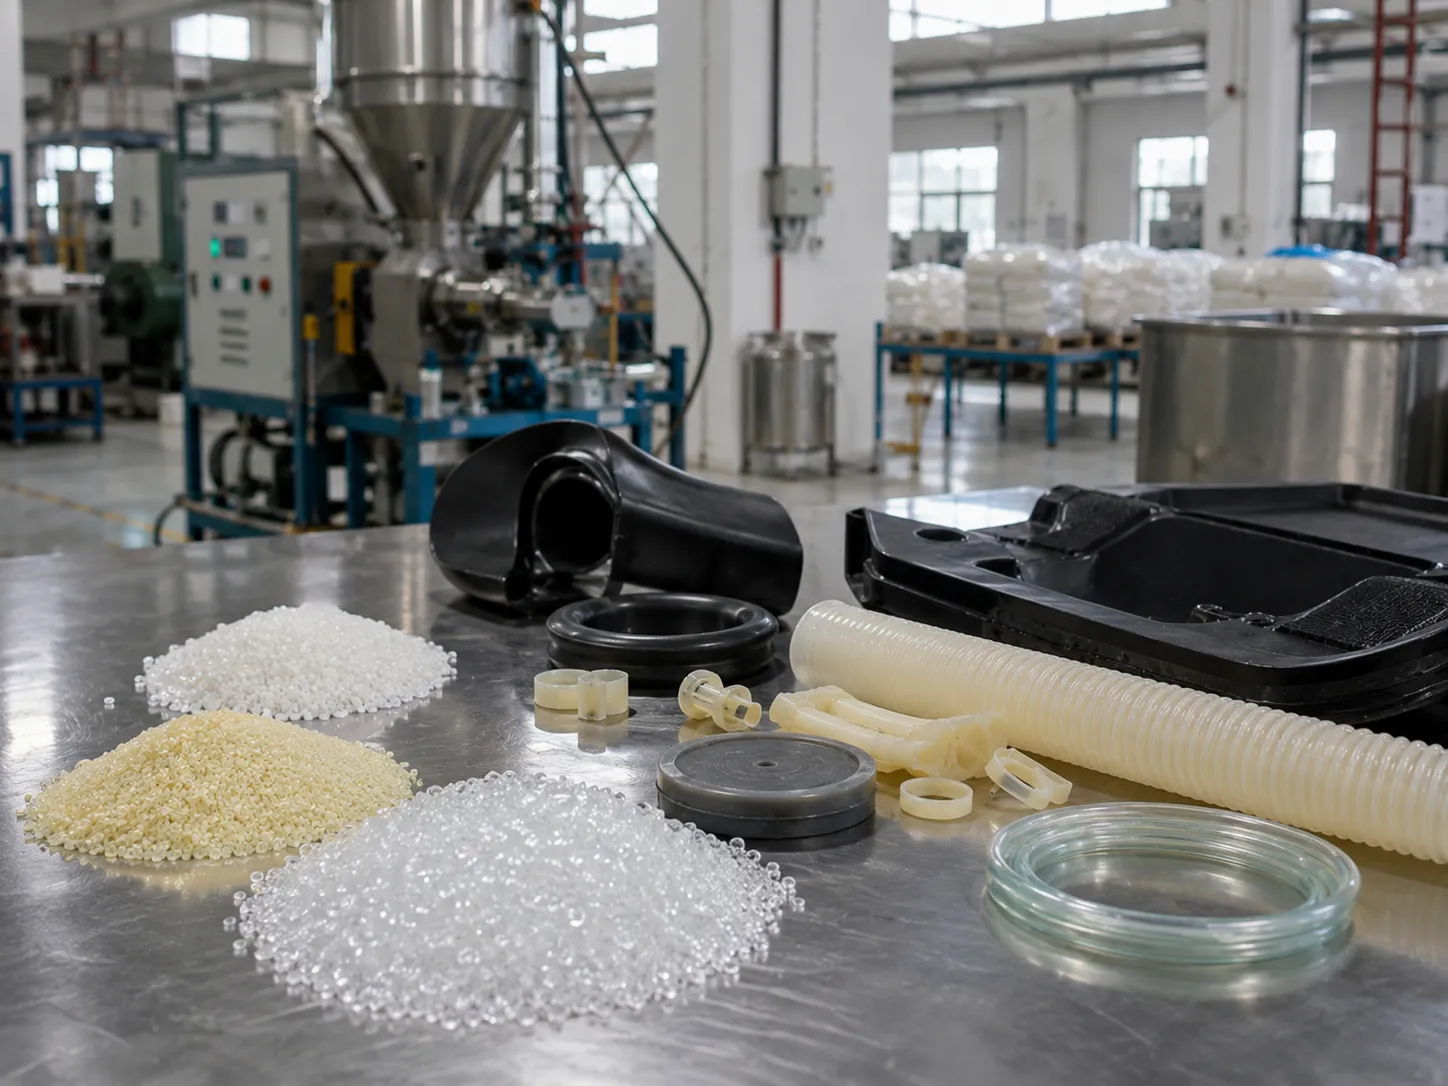
Thermoplastic Polyurethane (TPU)
One-step TPU synthesis with hardness dialed in from Shore A 60 to D 70, for automotive, footwear and medical parts.
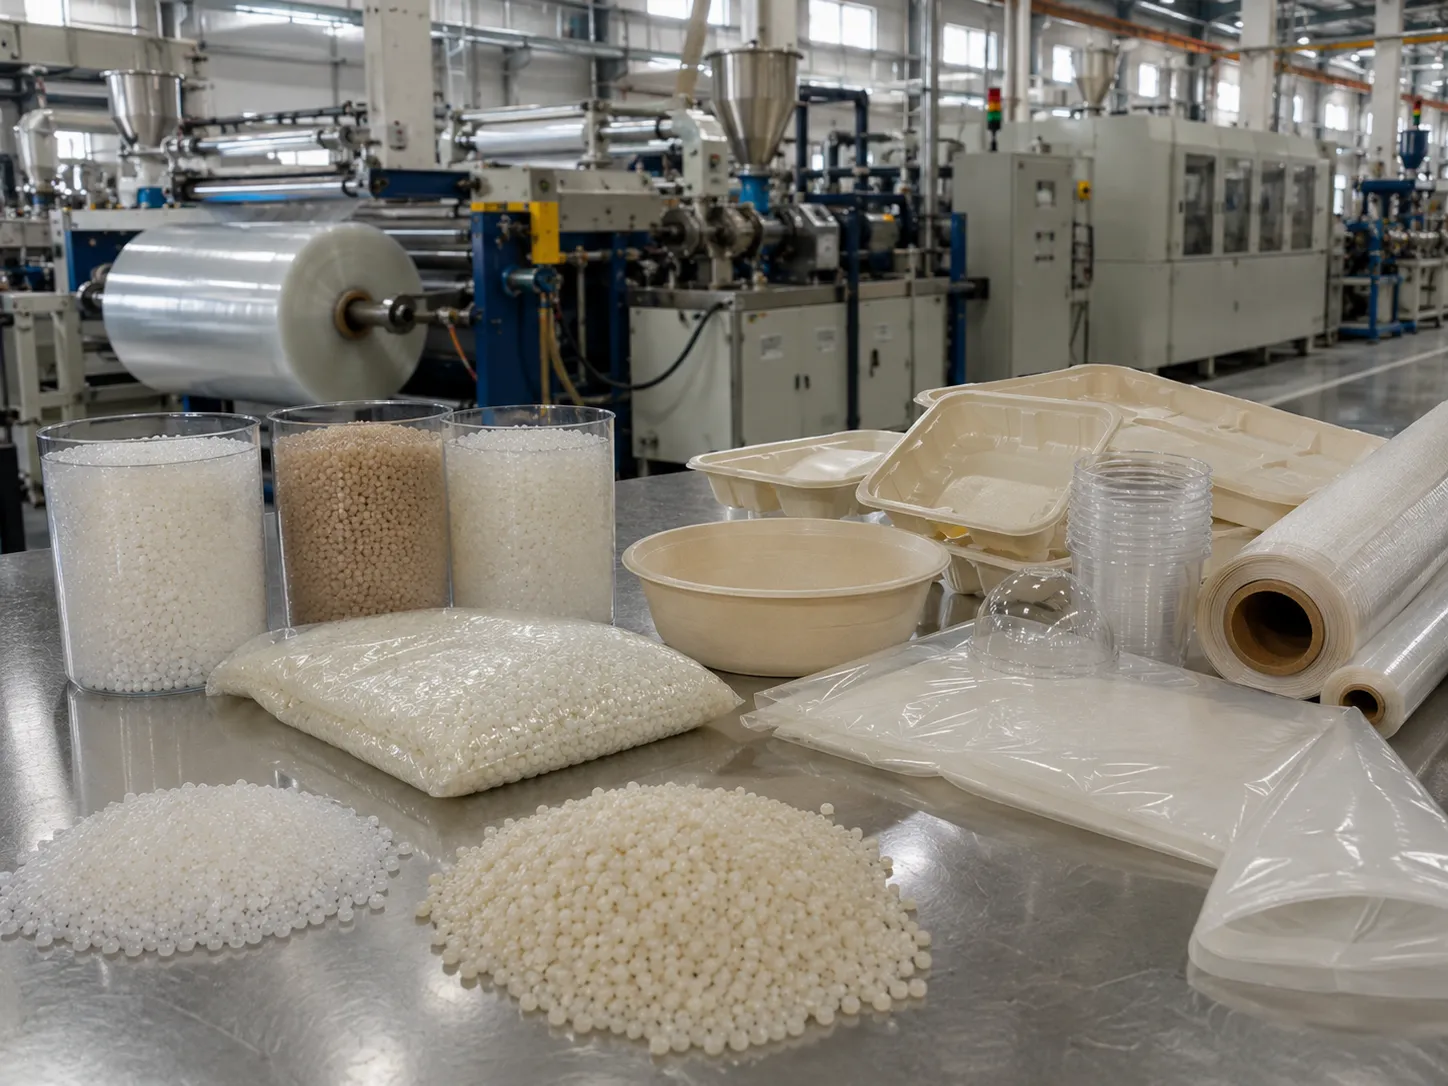
Biodegradable Polymers
PLA, PBAT and PBS compounded with chain extenders, keeping molecular weight — and degradation specs — under control.
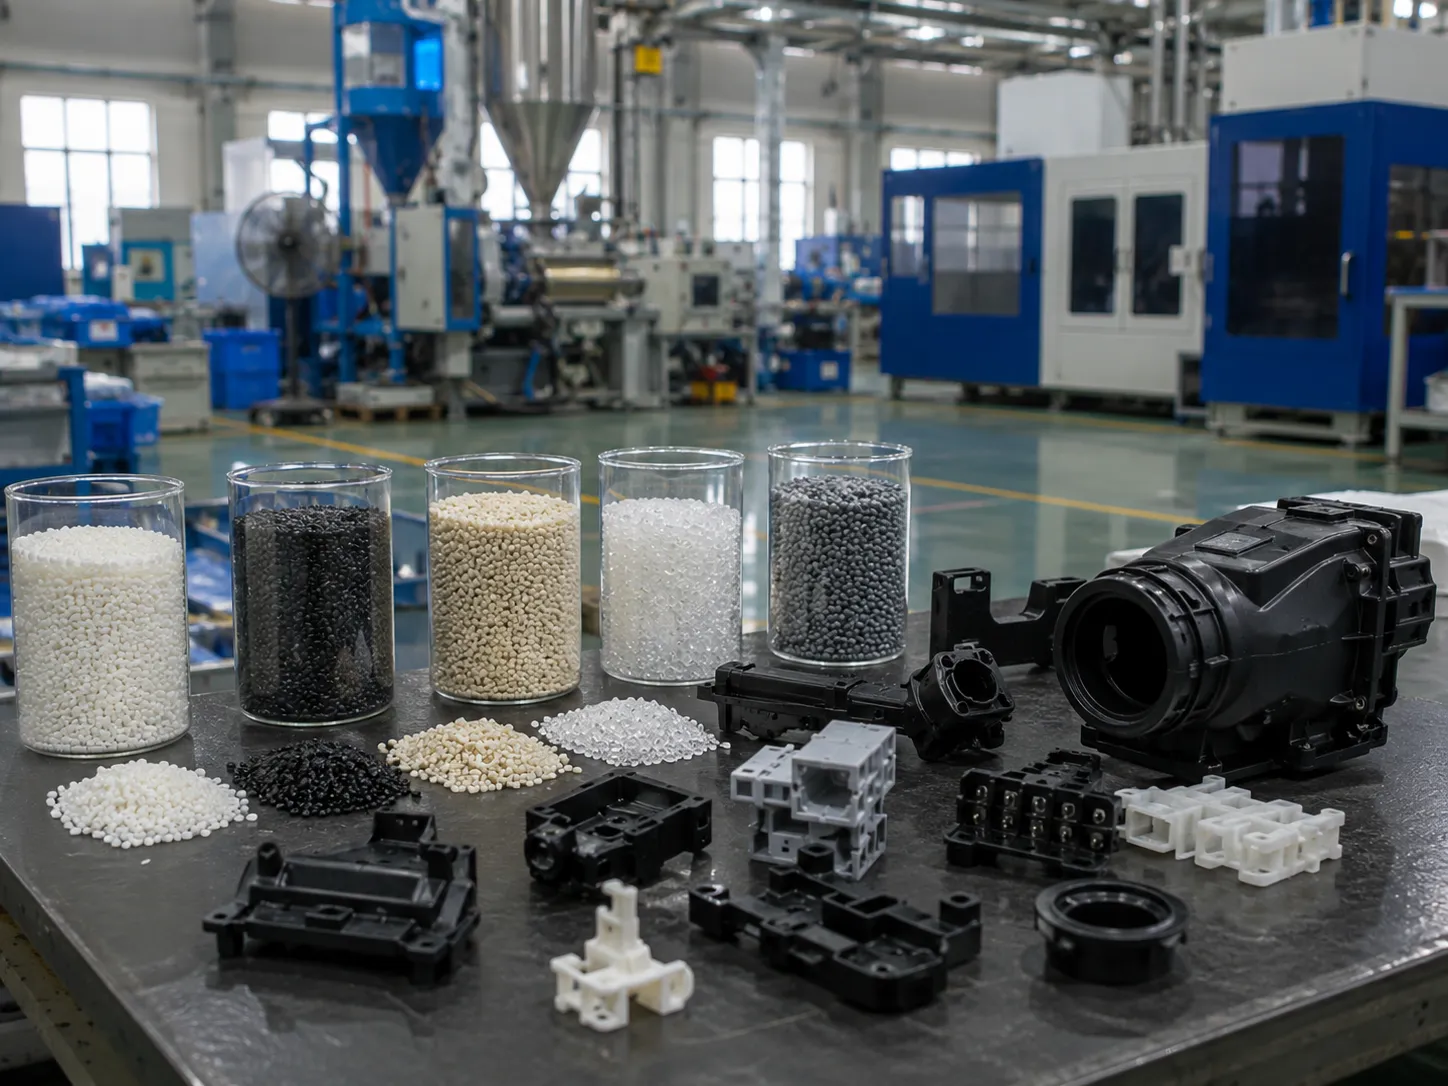
Engineering Plastics
PA, PC and PBT modified with glass fiber or minerals; properties stay intact because dispersion happens without over-shearing.
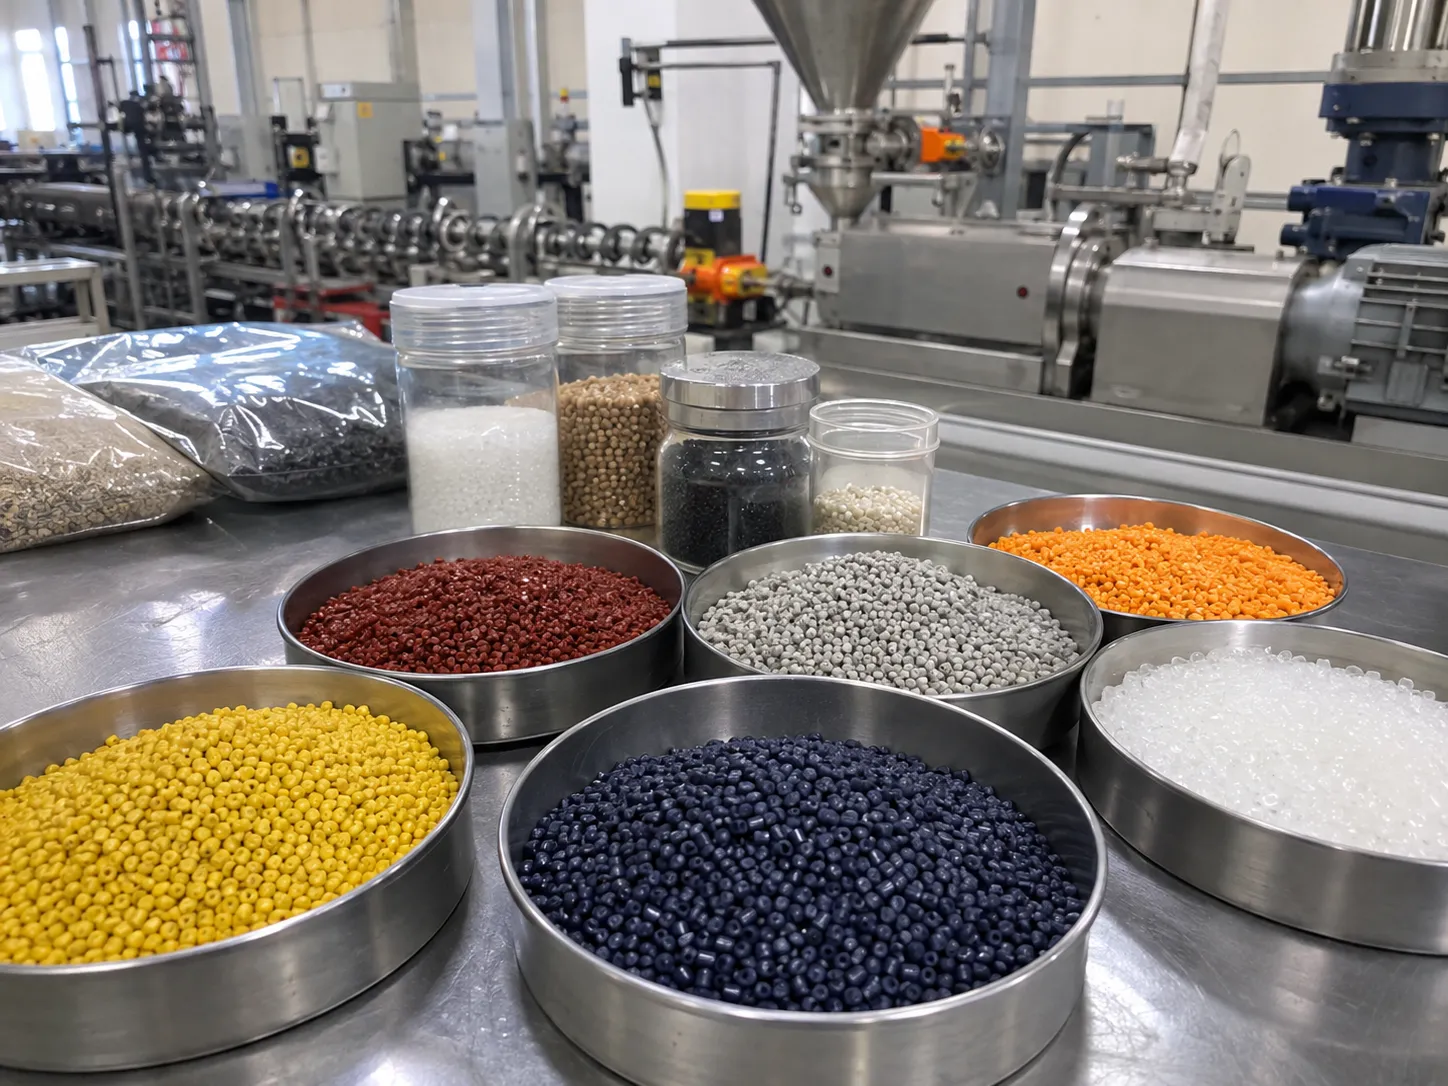
Reactive Masterbatches
High-loading functional masterbatches where the carrier is reacted, not just blended, for stable dosage downstream.
Polymer Grafting
MAH grafting and silane cross-linking — the classic REX jobs — with graft ratio held by precise residence time control.
Nanocomposites
Clay, carbon nanotubes or graphene dispersed at nano scale — the double meshing shear of twin screws makes it possible.
Reactive Extrusion vs Batch Reactor — an Honest Comparison
Batch reactors still have their place. But for most continuous chemistries, the numbers below explain why the industry is moving to REX.
| Feature | UET Reactive Extruder | Traditional Batch Reactor |
|---|---|---|
| Processing Time | Continuous — 5–10 min residence | 2–8 h per batch |
| Energy Efficiency | 30–40% lower specific energy | Repeated heating/cooling cycles |
| Product Consistency | Steady-state, tight spec control | Drift between batches |
| Solvent Usage | Solvent-free or minimal | Large volumes, recovery needed |
| Environmental Impact | Low waste, no recovery plant | High waste, recovery plant |
| Scale-Up | Linear from lab to production | Re-optimization at every scale |
How a Reactive Extruder Works
Follow the material through the machine — four stages, one continuous pass.
Reactive Extrusion Process Flow
Precise Feeding
Loss-in-weight feeders meter monomers, polymers, catalysts and additives at ±0.5% accuracy
Melting & Mixing
Kneading blocks build the shear and temperature profile that starts the reaction
Reaction & Venting
Vacuum ports pull off volatiles and by-products, driving conversion to completion
Extrusion & Pelletizing
Melt pump and die deliver stable pressure; strands or underwater pelletizing finish the job
Material Introduction
Liquid and solid feeds enter at separate ports — catalyst downstream of the melt zone, for example — exactly where your chemistry wants them.
Reaction Zones
Barrel sections run 180–320 °C under independent PID control, so exothermic reactions never run away from you.
Devolatilization
Vacuum vents remove water, alcohol or unreacted monomer as they form — which is what pushes condensation reactions to completion.
Twin Screw Mixing
Continuous surface renewal gives the short, uniform residence time distribution that batch reactors simply cannot match.
Key Components of a UET Reactive Extruder
Every core module is machined in our own Nanjing plant — which is why we can hold 0.02 mm tolerances and 1–2 week lead times.
Loss-in-Weight Feeding
±0.5% dosing of monomers, additives and catalysts keeps reaction stoichiometry stable.
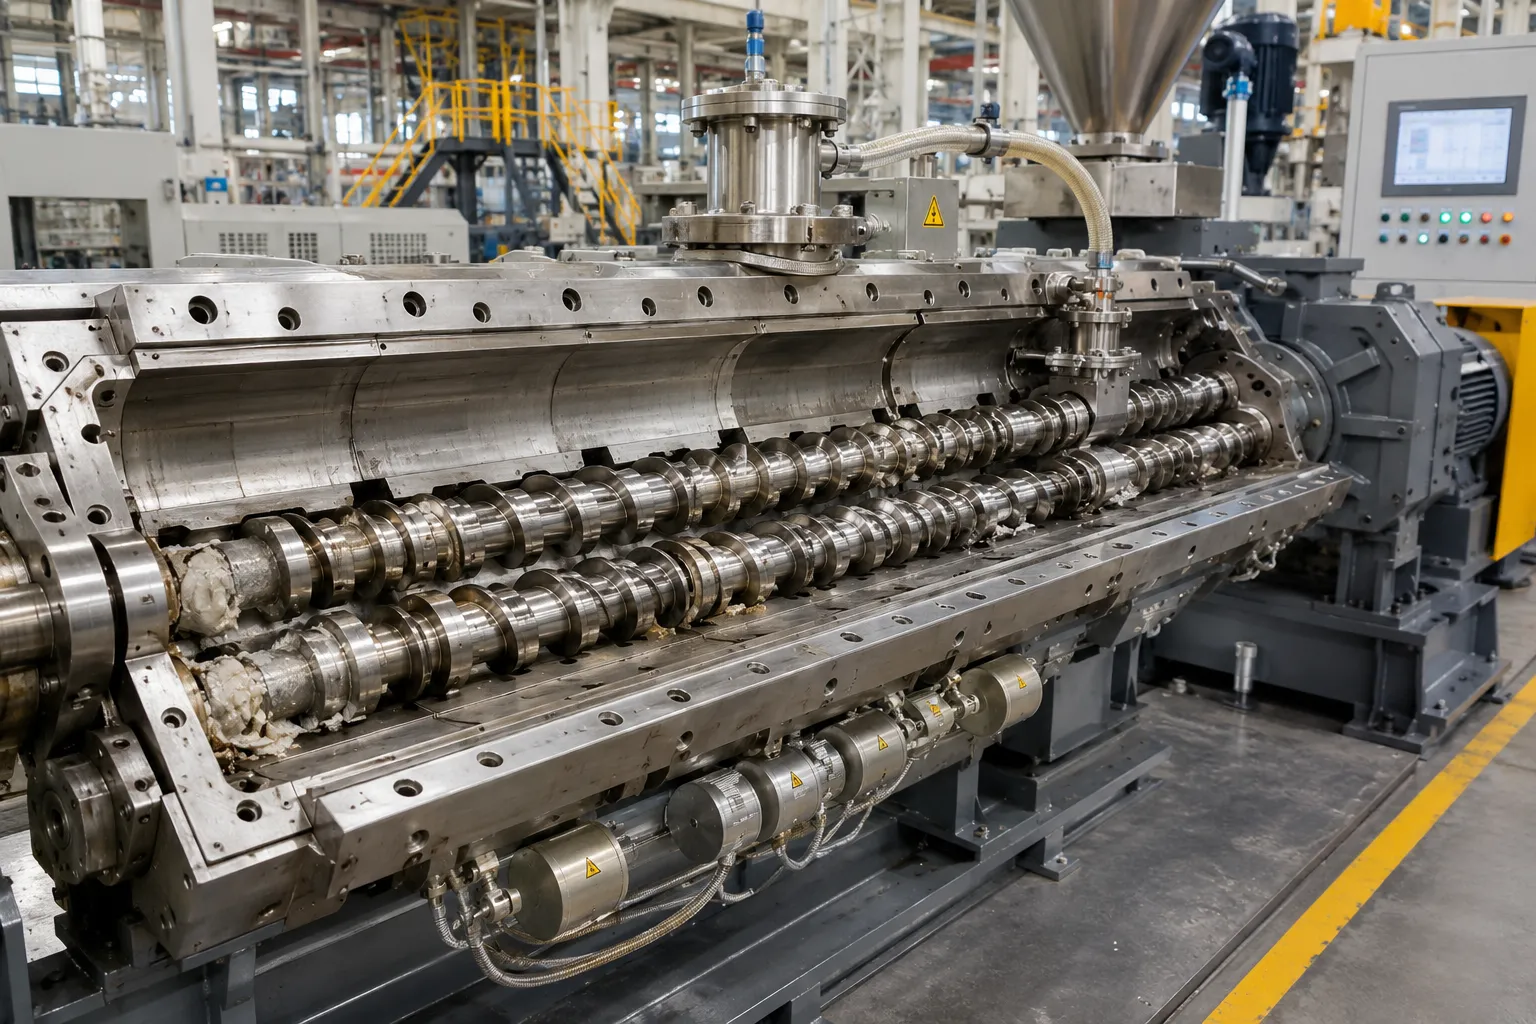
Co-Rotating Twin Screws
Modular conveying, kneading and reverse elements — configured per reaction, swapped in hours.
Modular Barrel
Bimetallic or SS316L sections, 8–12 zones, side-feed and vent openings where you need them.
High-Torque Gearbox
T/A³ ≤ 8, rated for 24/7 duty under high-viscosity reactive loads.
Heating / Cooling Zones
Independent PID loops hold each zone within ±1.5 °C.
Vacuum Venting System
2–4 vent ports with liquid-ring pump strip volatiles and by-products.
Die Head & Melt Pump
Stable discharge pressure for uniform strands or underwater pelletizing.
PLC Control System
Siemens/ABB PLC, touchscreen HMI, recipe storage and remote diagnostics.
Reactive Extruder Factory: Manufacturing & Quality Control
Visit in person or by live video — the plant, the machining centers and the test bay are all open to you before you pay a deposit.
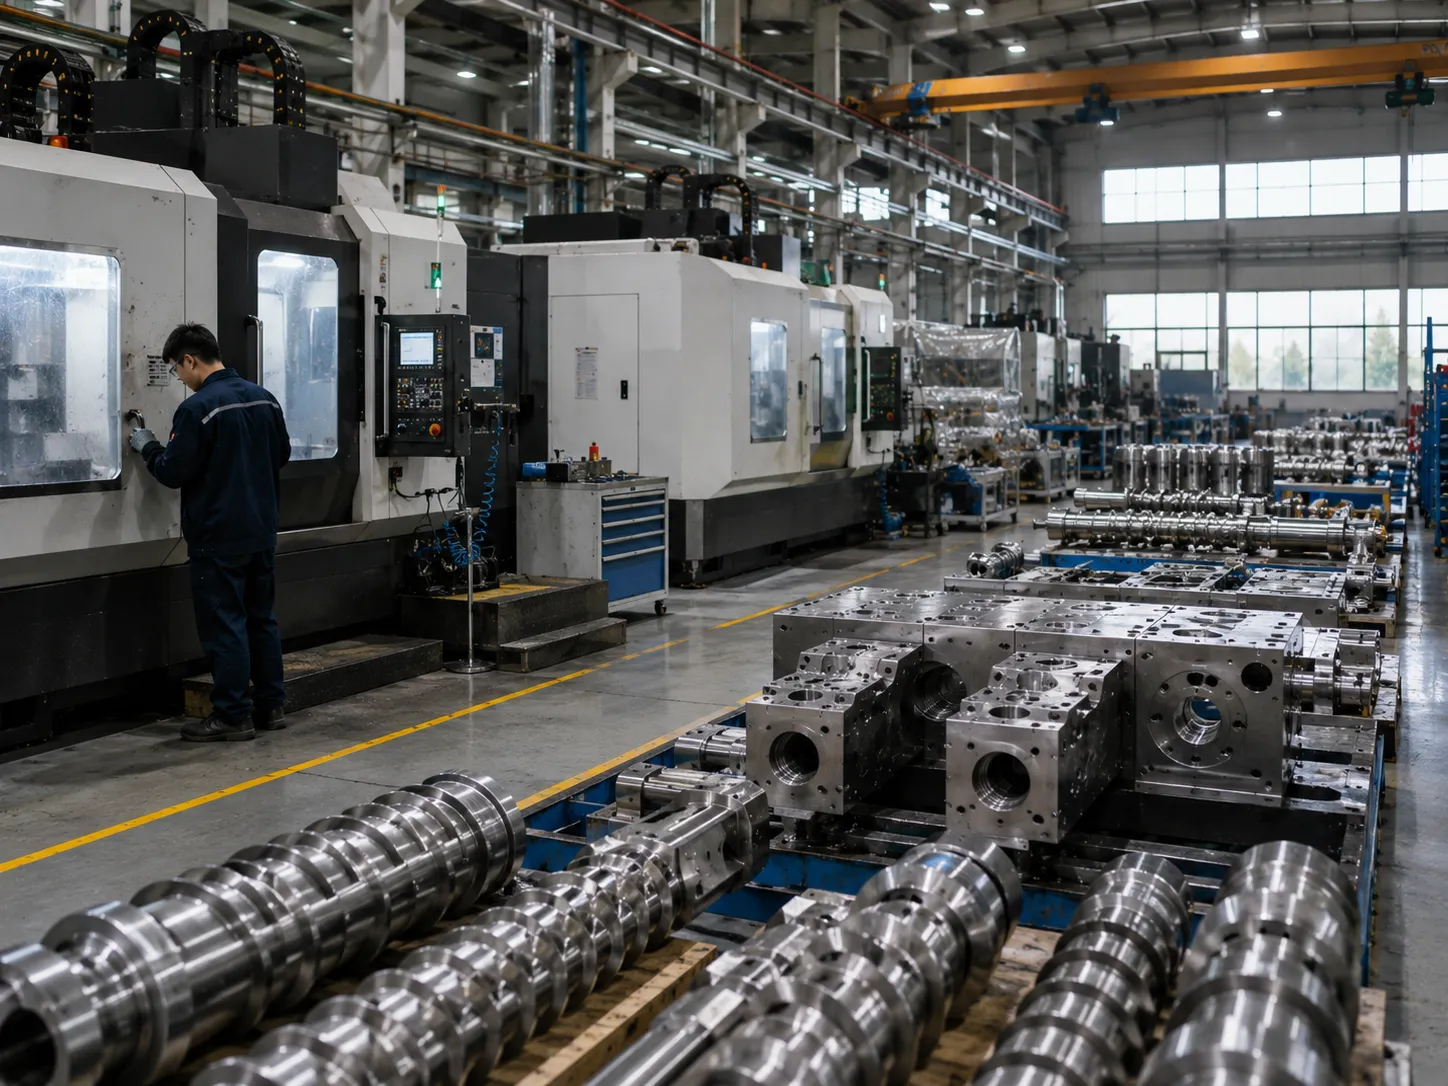
In-House Machining
20,000 m² plant with 5-axis CNC centers. Screws and barrels are machined, nitrided and inspected under one roof — no outsourced core parts.
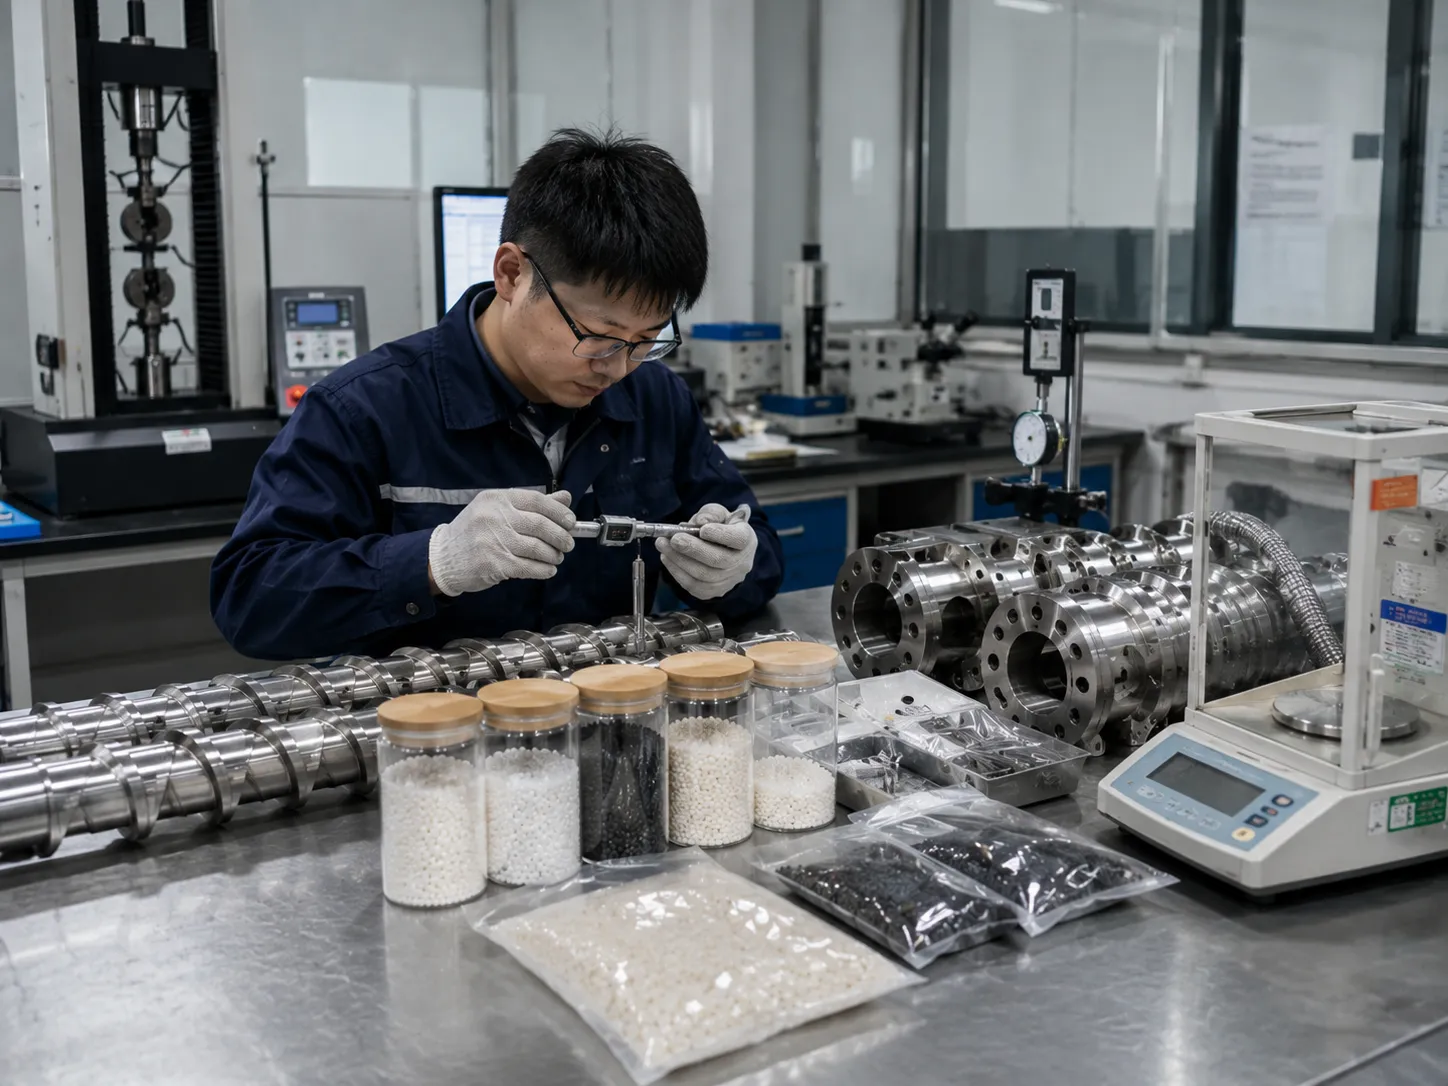
Quality Control
Hardness, composition and dimensional checks on incoming steel; every finished component measured against drawing before assembly.
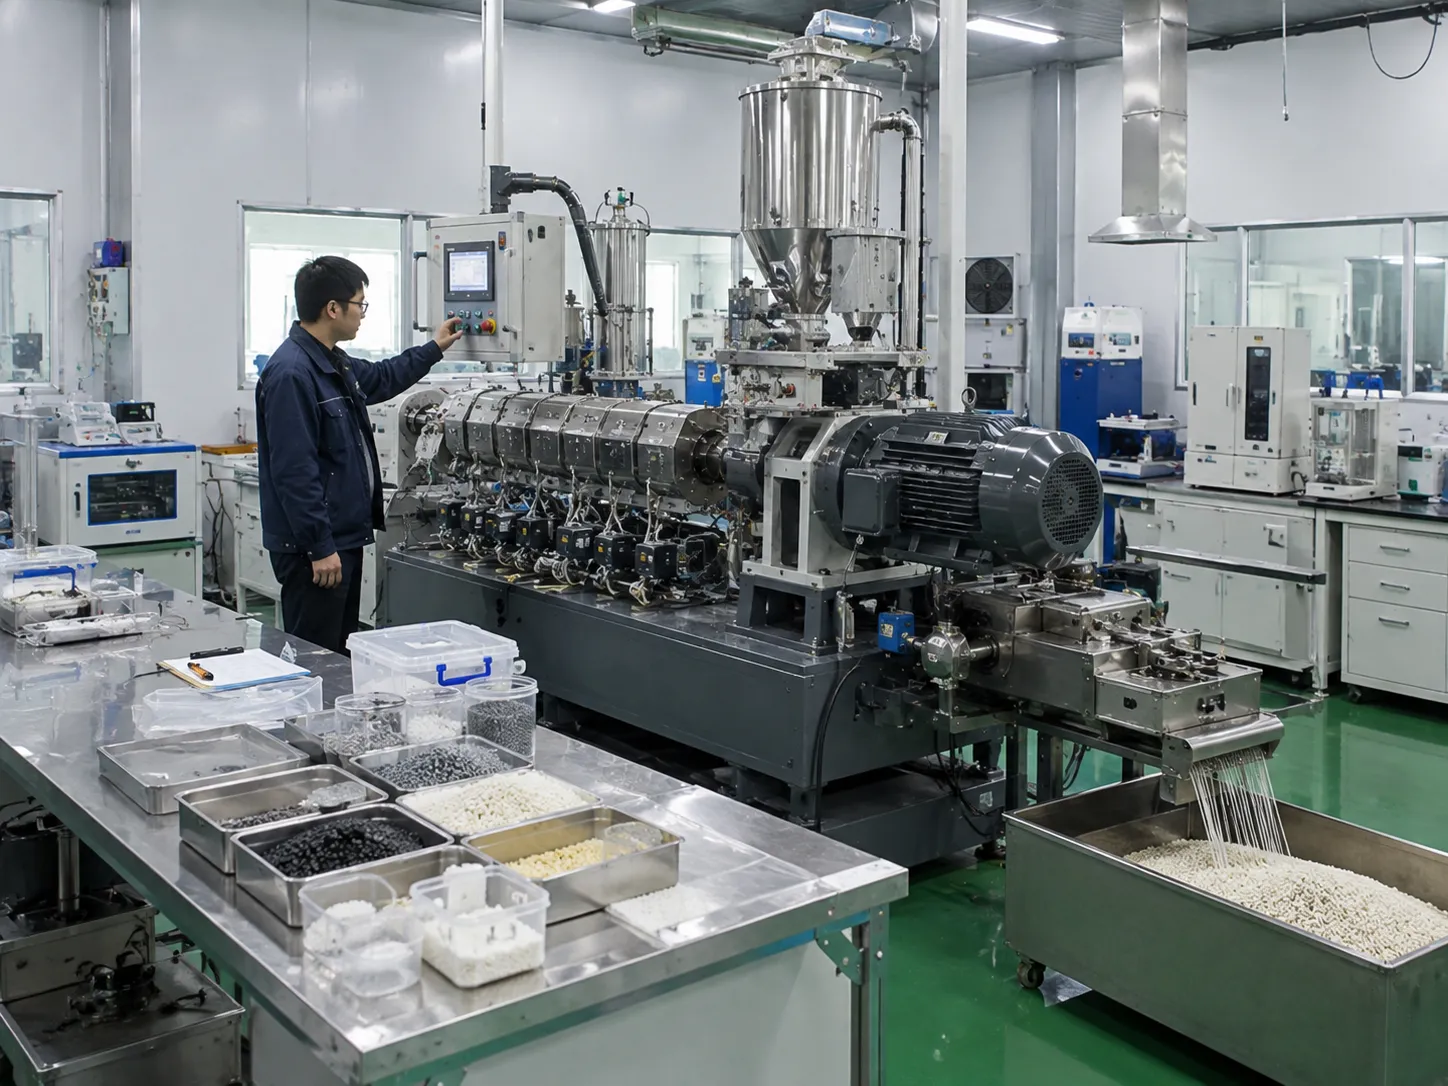
Material Test Lab
Pilot extruders running customer trials weekly. Your formulation is proven on our machines before your purchase order is confirmed.
ISO 9001
CE
SGS
BV
What Customers Say About UET Reactive Extruders
Unedited feedback from production teams running our lines on three continents.
“We moved our PLA/PBAT line from batch reactors to the SHJ-92 last year. Energy bill dropped about a third, solvent recovery went away completely, and our molecular weight distribution has never been this tight. The modular screws also let us switch formulations in an afternoon.”
“The SHJ-63 has been running our TPU line for eight months. Zone temperatures hold within a degree, which is exactly what the chemistry needs. When we had a question during commissioning, their engineer answered on WhatsApp the same evening.”
“Two SHJ-72 machines handle our 40% glass-filled PA6 and PC compounds without complaint. UET’s engineers came to Mumbai for commissioning and trained our shift teams properly. Uptime has stayed above 98% since.”
Your Trusted Reactive Extruder Manufacturer & Supplier in China
UET is a factory, not a trading company. Our Nanjing plant machines every screw element and barrel in-house — that is how we hold 0.02 mm tolerances and ship standard models in 1–2 weeks.
You deal directly with the engineers who designed your line. Quotations are itemized — extruder, electricals, downstream, spares — so you always know exactly what you are paying for.
Why Source from UET
- Factory-direct pricing — no middlemen margin
- OEM/ODM & full customization (screw layout, L/D, metallurgy)
- MOQ: 1 unit — trial orders supported
- Lead time: 1–2 weeks standard, 4–6 weeks custom
- CE, ISO 9001 — SGS/BV third-party inspection welcome
- 24/7 engineer response & lifetime spare parts at cost
Related Extruder Solutions
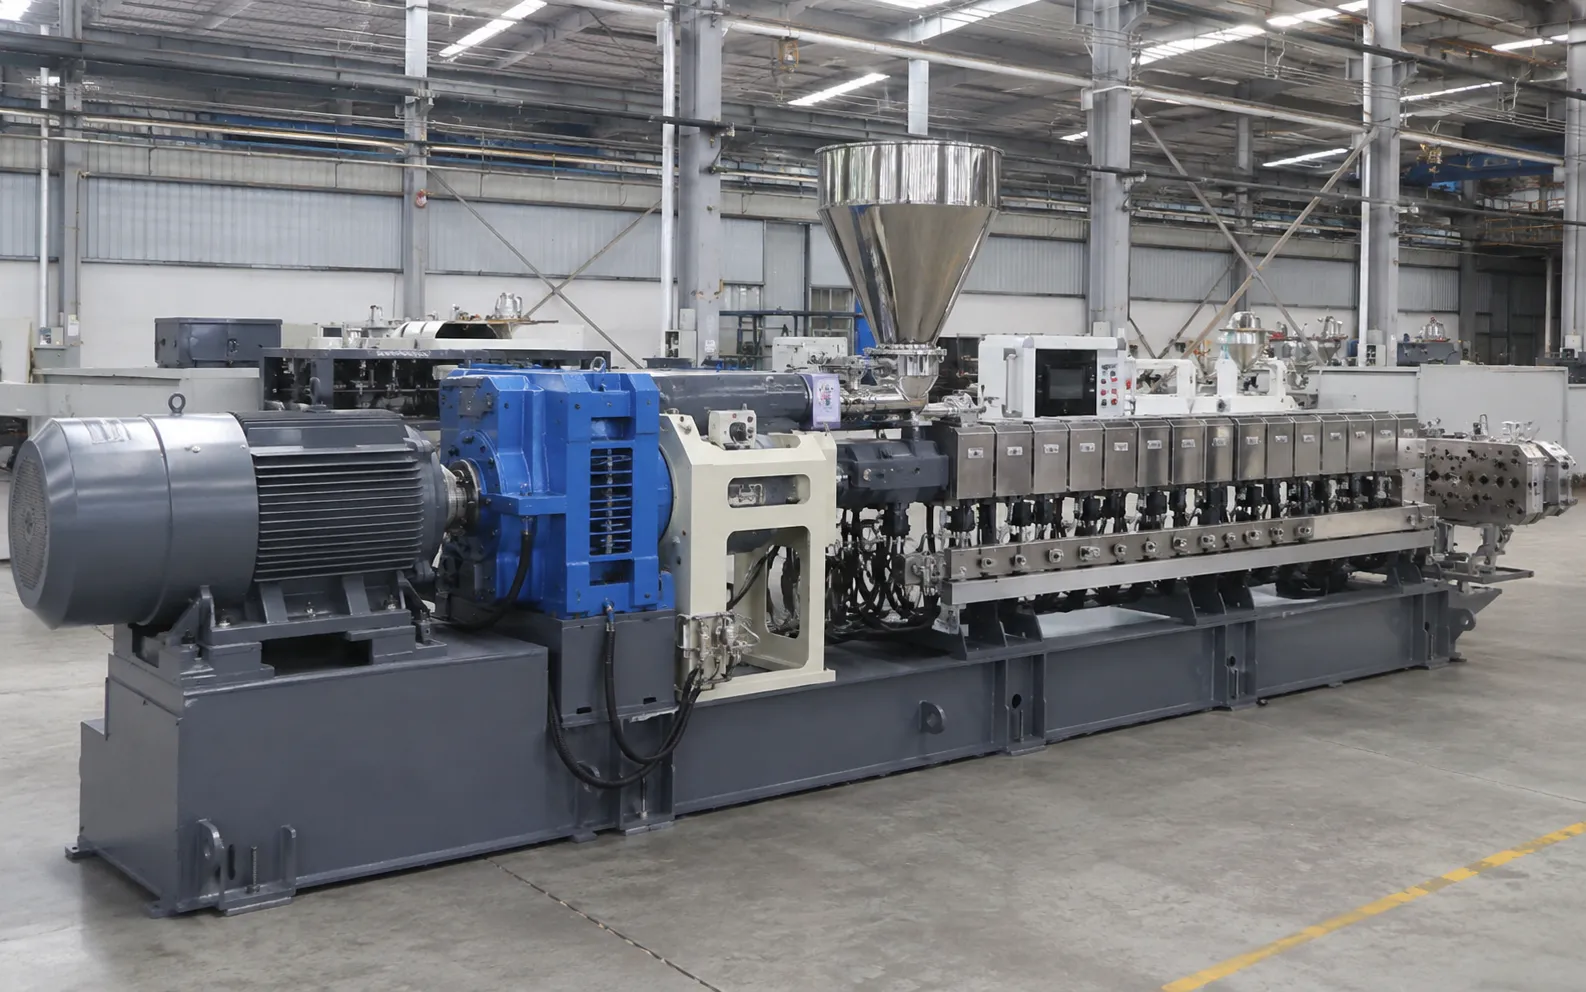
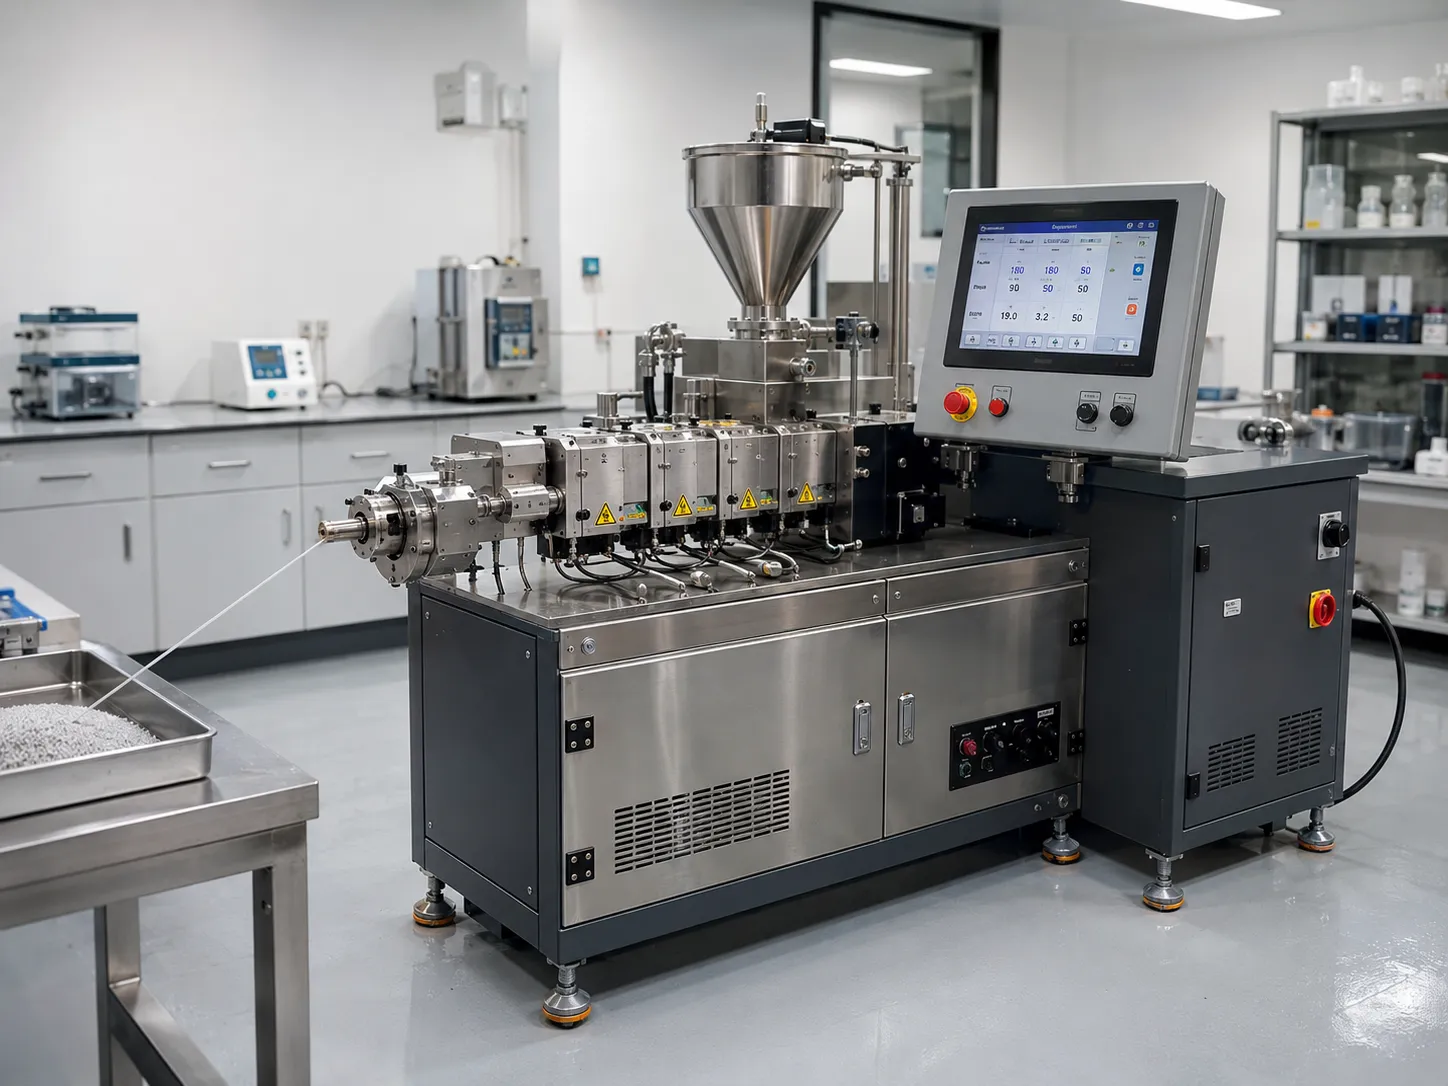
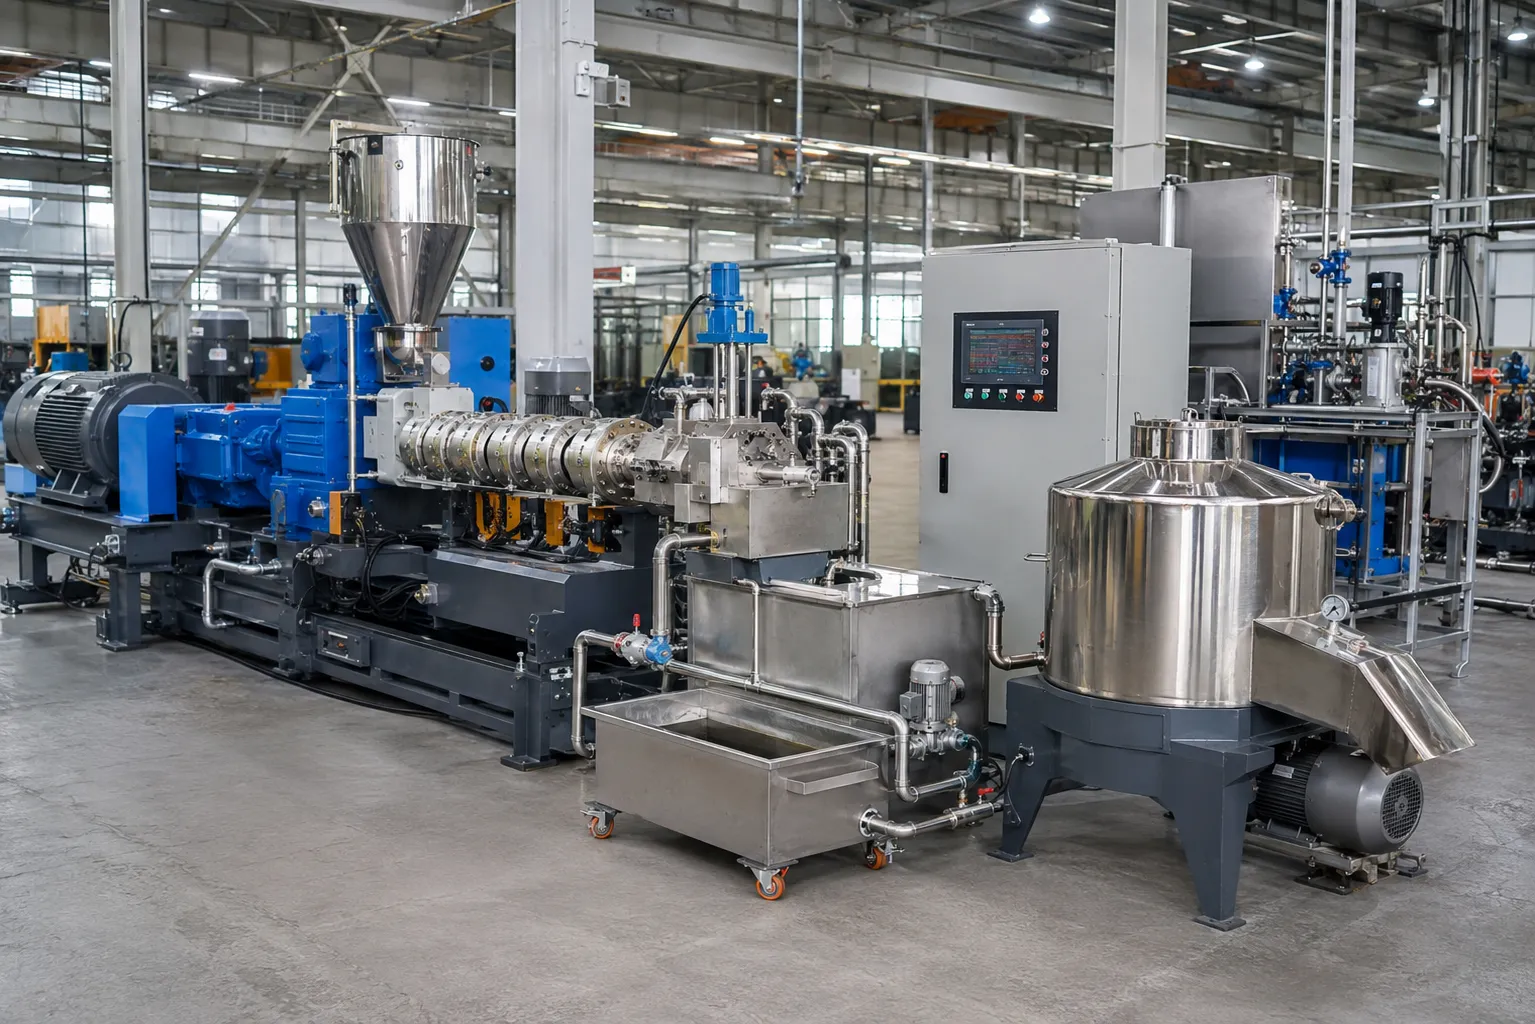
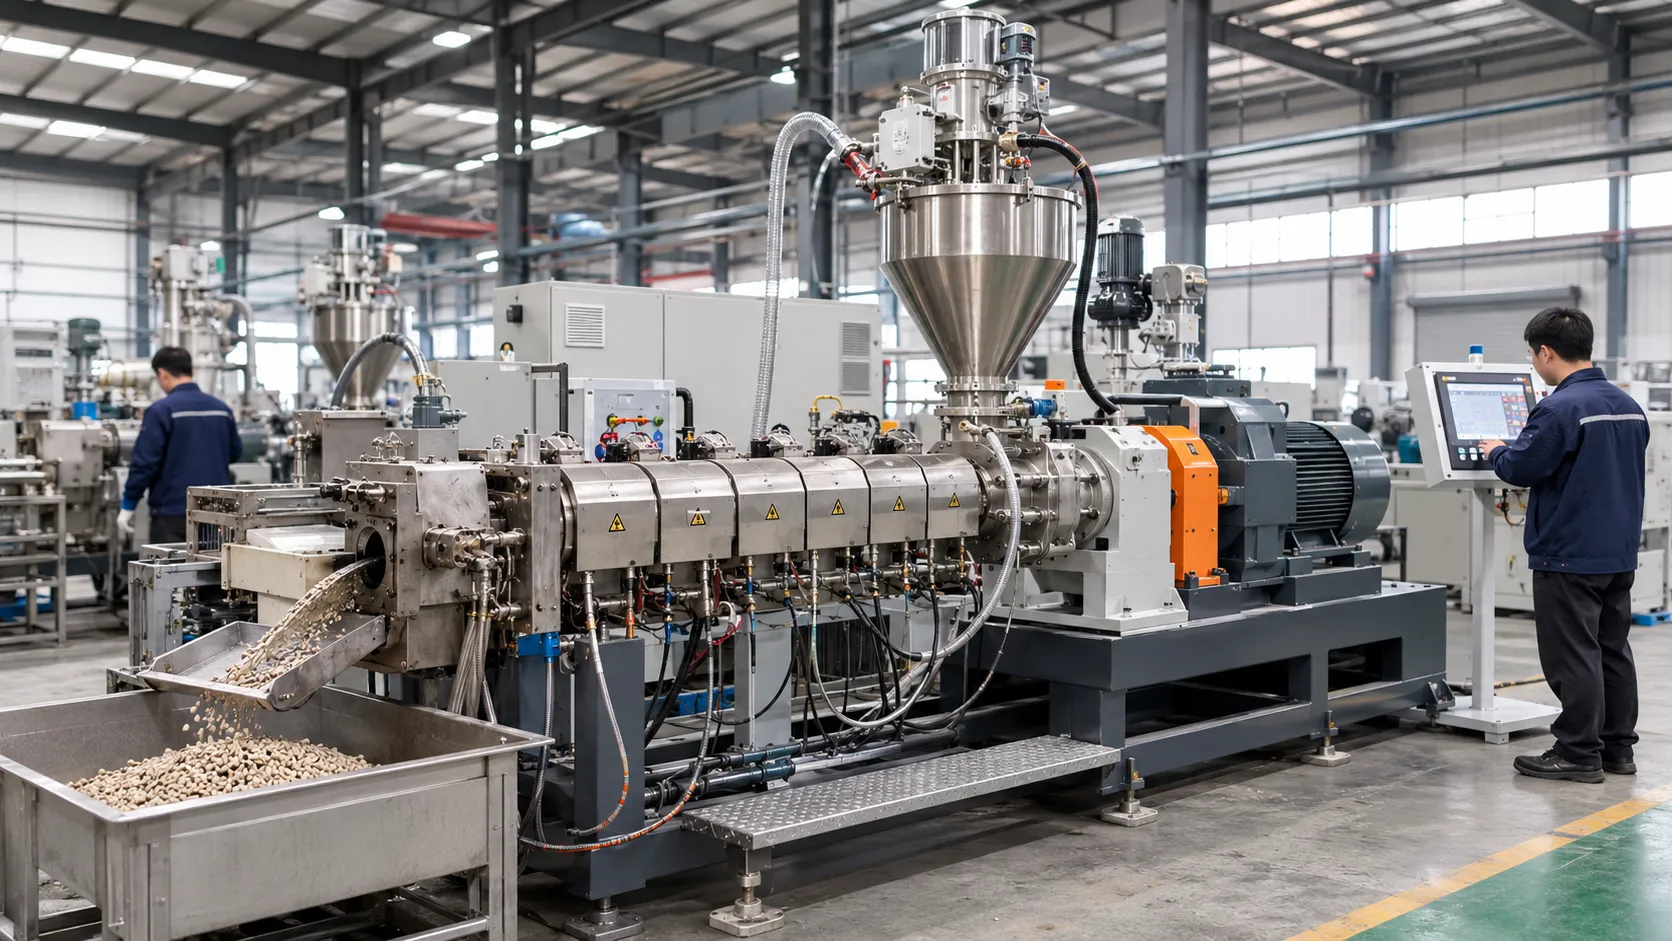
Four machines from our current range that complete a reactive extrusion line — platform, R&D, downstream and sister application.
Reactive Extruder FAQs: Technical & Commercial Answers
Straight answers from our application engineers — no sales talk.
A standard extruder only melts and shapes polymer. A reactive extruder goes further: it runs a chemical reaction — polymerization, grafting, cross-linking or compatibilization — inside the barrel while the material is being melted, mixed and pumped. In practice that means one machine replaces a reactor plus a finishing extruder, and the process runs continuously instead of batch by batch.
In our customers’ numbers: 30–40% lower specific energy, reaction times of minutes instead of hours, no solvent to recover, and much tighter batch-to-batch consistency because the process runs at steady state. Scale-up is also more predictable — a screw configuration proven on a lab machine transfers to production with far less re-optimization than a batch route.
The list covers most reactive chemistries we see in industry: TPU, PLA/PBAT/PBS biodegradables, PA/PC/PBT/ABS engineering plastics, PP/PE grafting (MAH, silane), PVC, EVA, reactive masterbatches, nanocomposites and recycled polymer purification. If your chemistry is unusual, send the formulation — we run a trial in our test lab before quoting.
Typical end products include TPU pellets for automotive and footwear, biodegradable resins for packaging, MAH-grafted compatibilizers, glass-fiber reinforced engineering compounds, functional masterbatches, nanocomposite granules, hot-melt adhesives and XLPE cable compounds. If a melt-phase chemical reaction is involved, REX can probably make it.
Because we build everything ourselves. Screws, barrels and gearboxes are machined in our 20,000 m² Nanjing plant; every machine runs a 72-hour full-load test plus a material trial before shipping; and you talk to the engineers who designed your line, not a sales middleman. 5,600+ machines in 80+ countries, CE and ISO 9001 certified, MOQ of one unit.
Yes — and we insist on it for reactive projects. Ship us your raw materials; our lab runs the chemistry on a pilot extruder and returns a test report covering output, energy, conversion and pellet quality, together with the recommended screw layout. You approve the process before the purchase order is signed.
One year on the whole machine, 24 months on core components (screws, barrels, gearbox). After that: lifetime technical support and spare parts at cost price. Commissioning on site or by video, five-day operator training, and a 24/7 engineer line — average response under two hours.