Industrial Extrusion Solutions
Engineering Plastic Extrusion Line
Twin-screw extrusion systems built for PA, PC, POM, ABS, PBT, and glass-fiber modified compounds. Hold ±0.03 mm profile tolerance, reach 99.8% melt homogeneity, and cut energy draw by 40% — backed by 20 years of compounding experience at our Nanjing factory.
99.8%Melt Homogeneity
±0.3℃Temp Precision
40%+Energy Savings
2000kg/h Max Output
Equipment Overview
What Is an Engineering Plastic Extrusion Machine?
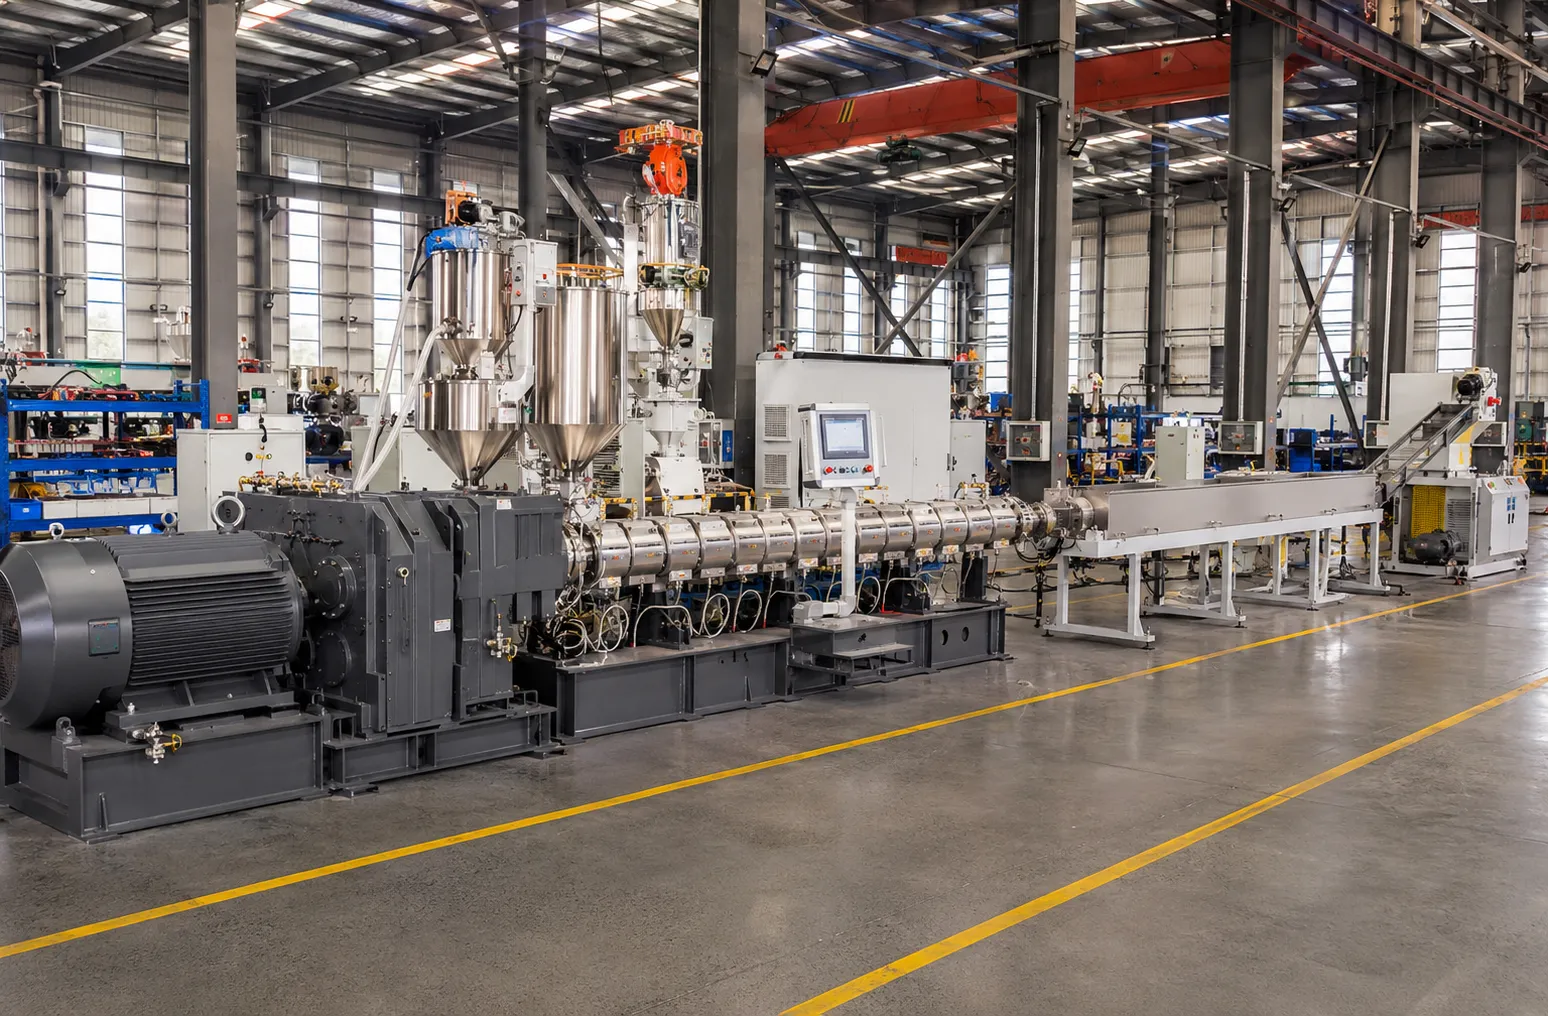
An engineering plastic extrusion line continuously melts, mixes, and shapes high-performance polymers — PA, PC, POM, PBT, PPS — into profiles, tubes, rods, or sheets. Where commodity extruders handle PE and PVC, our co-rotating twin-screw platform is purpose-built for the high melt viscosities, abrasive glass-fiber fills, and tight thermal windows that automotive, electronics, and aerospace parts demand.
Every line is engineered around your resin and your drawing: screw geometry, barrel metallurgy, die design, and downstream tooling are all matched to the part you need to ship — then proven on a material test-run before shipment.
- Continuous 24/7 ProductionPellets feed non-stop through melt, die, and cooling stages. One operator runs a full shift at throughput rates single-screw machines cannot match.
- Co-Rotating Twin-Screw DesignIntermeshing screws wipe each other clean every revolution, preventing dead spots where heat-sensitive resins like POM would degrade and blacken.
- ±0.03 mm Dimensional ControlVacuum calibration tanks pull the still-soft profile against precision sizing plates; closed-loop puller control holds automotive drawing tolerances.
Production Challenges
6 Production Problems This Engineering Plastic Extrusion Line Solves
Every solution below comes from real commissioning logs — issues our engineers diagnosed at customer plants before they switched to UET.
Inconsistent Melt Mixing
Wrong screw element sequencing causes filler streaks and weak spots. We map each recipe to a verified element layout, holding composition deviation under 3% across the full run.
Out-of-Tolerance Dimensions
Warped profiles and oversize walls mean scrapped parts. Our vacuum sizing plus laser gauge feedback keeps cross-section within ±0.03 mm — the spec your QC department signs off on.
Thermal Runaway at 280 ℃+
PC and PPS need barrel zones above 280 ℃ for hours on end. Cast-in cartridge heaters with PID tuning hold each zone at ±0.3 ℃ so the melt never cross-links or yellows.
Excessive Startup Scrap
Recipe recall from 150-slot PLC memory means the line hits spec in minutes, not hours. Customers report 25% less regrind after the first month of operation.
Narrow Material Window
One frame, twelve-plus formulations. Swap from PA6-GF30 to clear PC without changing screws — just load the stored recipe and adjust downstream tooling.
Frequent Unplanned Downtime
Modular barrel segments pull individually; no full disassembly. Vibration sensors flag bearing wear weeks ahead. Service intervals stretch 40% versus fixed-frame competitors.
How It Works
How the Engineering Plastic Extrusion Process Works: 6-Stage Flow
Follow the material path through the line schematic below — from resin pellet at the hopper to finished, cut profiles at the stacker. Each stage runs under its own closed-loop sensor control.
← Swipe horizontally to view the full line diagram →
1
Gravimetric Feeding
Loss-in-weight feeders dose resin, masterbatch, and glass fiber into the throat under recipe control — no manual trimming between batches.
±0.5% dosing accuracy2
Melting & Plasticizing
Cast-in heater bands with PID zone control bring the resin to melt temperature without overshooting heat-sensitive grades like POM.
180–310 ℃ · ±0.3 ℃ per zone3
Twin-Screw Compounding
Co-rotating intermeshing screws shear and fold the melt until fillers, colorants, and additives are fully dispersed.
99.8% melt homogeneity4
Die-Head Shaping
The homogeneous melt passes through a custom-machined die and takes its final cross-section: profile, tube, rod, or sheet.
Custom dies · 20–500 mm5
Vacuum Calibration & Cooling
Stainless sizing plates and graduated spray cooling lock the dimensions while the profile solidifies under vacuum.
±0.03 mm tolerance6
Cutting & Stacking
A servo haul-off pulls the profile, the flying saw cuts to set length, and the auto-stacker counts and bundles for packing.
Automatic length control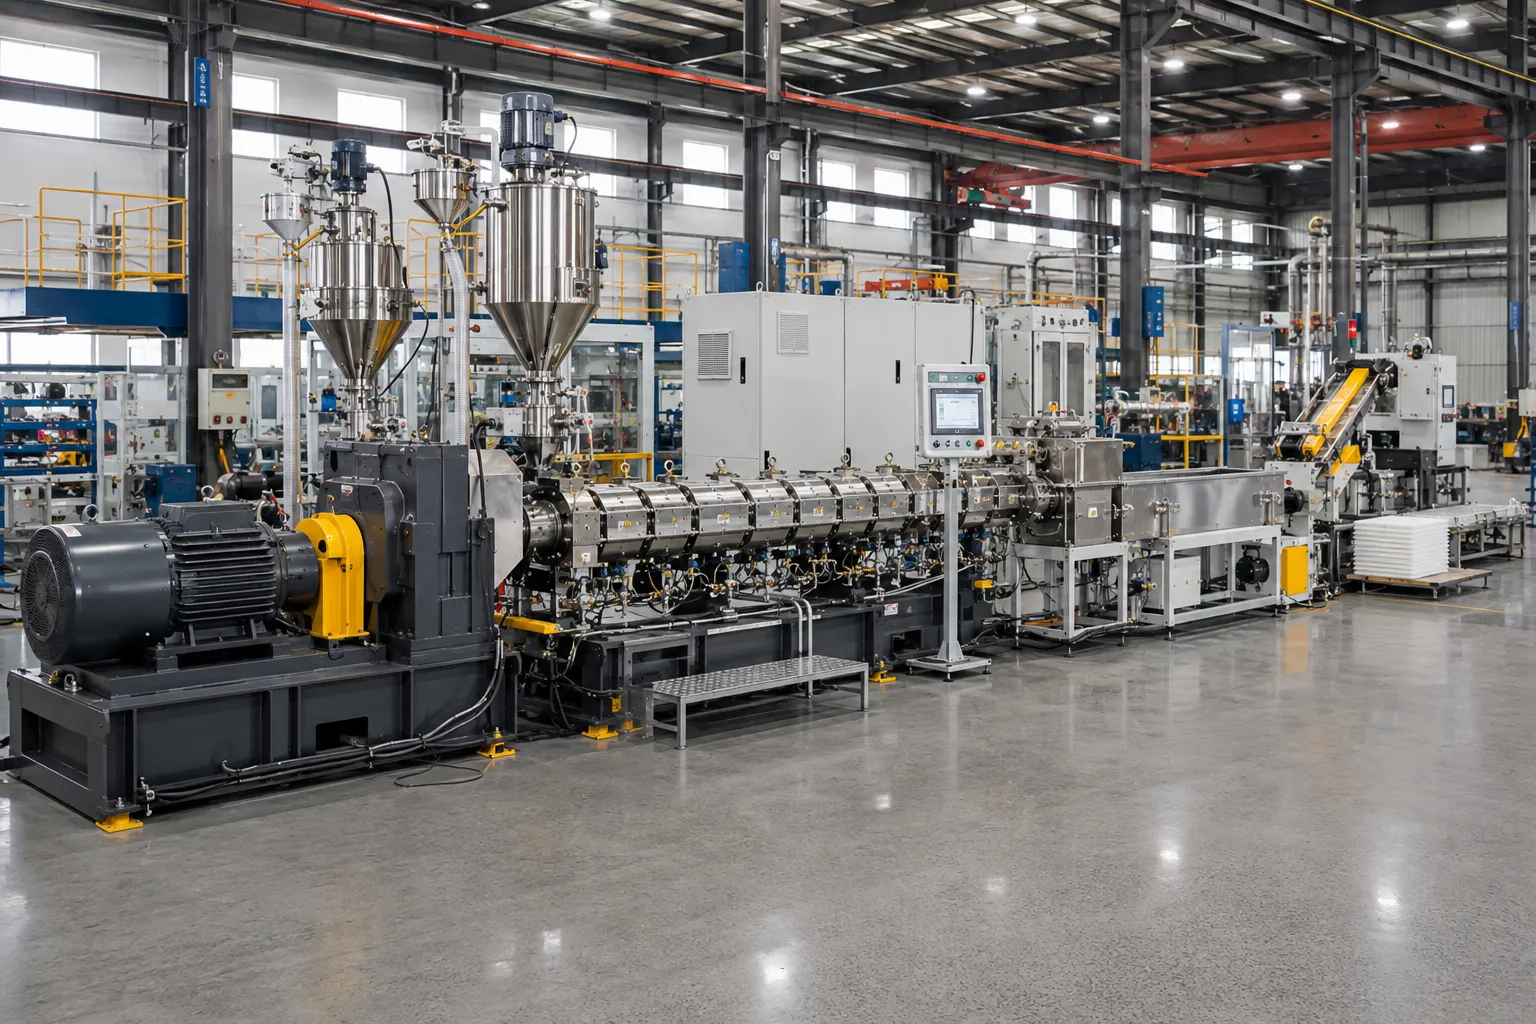
What’s Included
Complete Turnkey Engineering Plastic Extrusion Line Configuration
Every UET line ships as a factory-tested package. You receive a single packing list, one set of spares, and one point of engineering contact from layout drawing through commissioning.
- Twin-Screw Extruder UnitModular co-rotating screws, bimetallic barrel lined to HRC 58-62
- Loss-in-Weight FeedersUp to 6 gravimetric stations, ±0.5% dosing accuracy per channel
- Die Head & AdaptersQuick-change profile, pipe, or sheet dies machined to your drawing
- Vacuum Calibration & CoolingMulti-zone spray tank with stainless sizing plates
- Haul-Off, Cutter & StackerServo puller, flying saw or guillotine, pneumatic stacking table
- PLC & HMI Control CabinetSiemens S7 PLC, 15″ touchscreen, Ethernet remote diagnostics
Process Knowledge
Material Processing Parameters & Drying Guide for Engineering Plastics
The drying and melt data our application engineers pull up first when quoting your line. If your resin falls outside these ranges, we adjust barrel length, screw geometry, and venting accordingly.
| Material | Drying Before Processing | Melt Temperature | Typical Products |
|---|---|---|---|
| PA6 | 80 ℃ · 4–6 h (dew point ≤ −40 ℃) | 230–280 ℃ | Gears, fans, under-hood parts |
| PA66 | 80 ℃ · 6–8 h | 260–290 ℃ | GF-reinforced structural brackets |
| PC | 120 ℃ · 4–6 h | 260–310 ℃ | Housings, light diffusers, lenses |
| POM | 80 ℃ · 2–4 h | 180–210 ℃ | Precision gears, zipper tapes |
| ABS | 80 ℃ · 2–4 h | 200–240 ℃ | Enclosures, interior trim |
| PBT | 120 ℃ · 4–6 h | 240–260 ℃ | Connectors, relay sockets |
Dry First, Always
Even 0.1% surface moisture causes splay and drops molecular weight in PA and PC. We integrate desiccant-wheel dryers with inline dew-point monitors so resin enters the throat at spec, every cycle.
Match Screw to Resin
POM degrades under high shear; PC needs deep-channel conveying; GF compounds eat standard nitriding. We choose element profiles and barrel metallurgy per your recipe, not off a catalog default.
Cool for Crystallinity
POM and PBT crystallize within seconds of leaving the die. Graduated water temperature and vacuum sizing prevent sink marks, warpage, and the ovality that ruins press-fit assemblies.
End-Product Capabilities
Products You Can Produce: 8 Industry Applications
Parts our customers run daily on UET engineering plastic extrusion lines — from high-volume automotive clips to low-volume aerospace ducting.
Automotive Parts
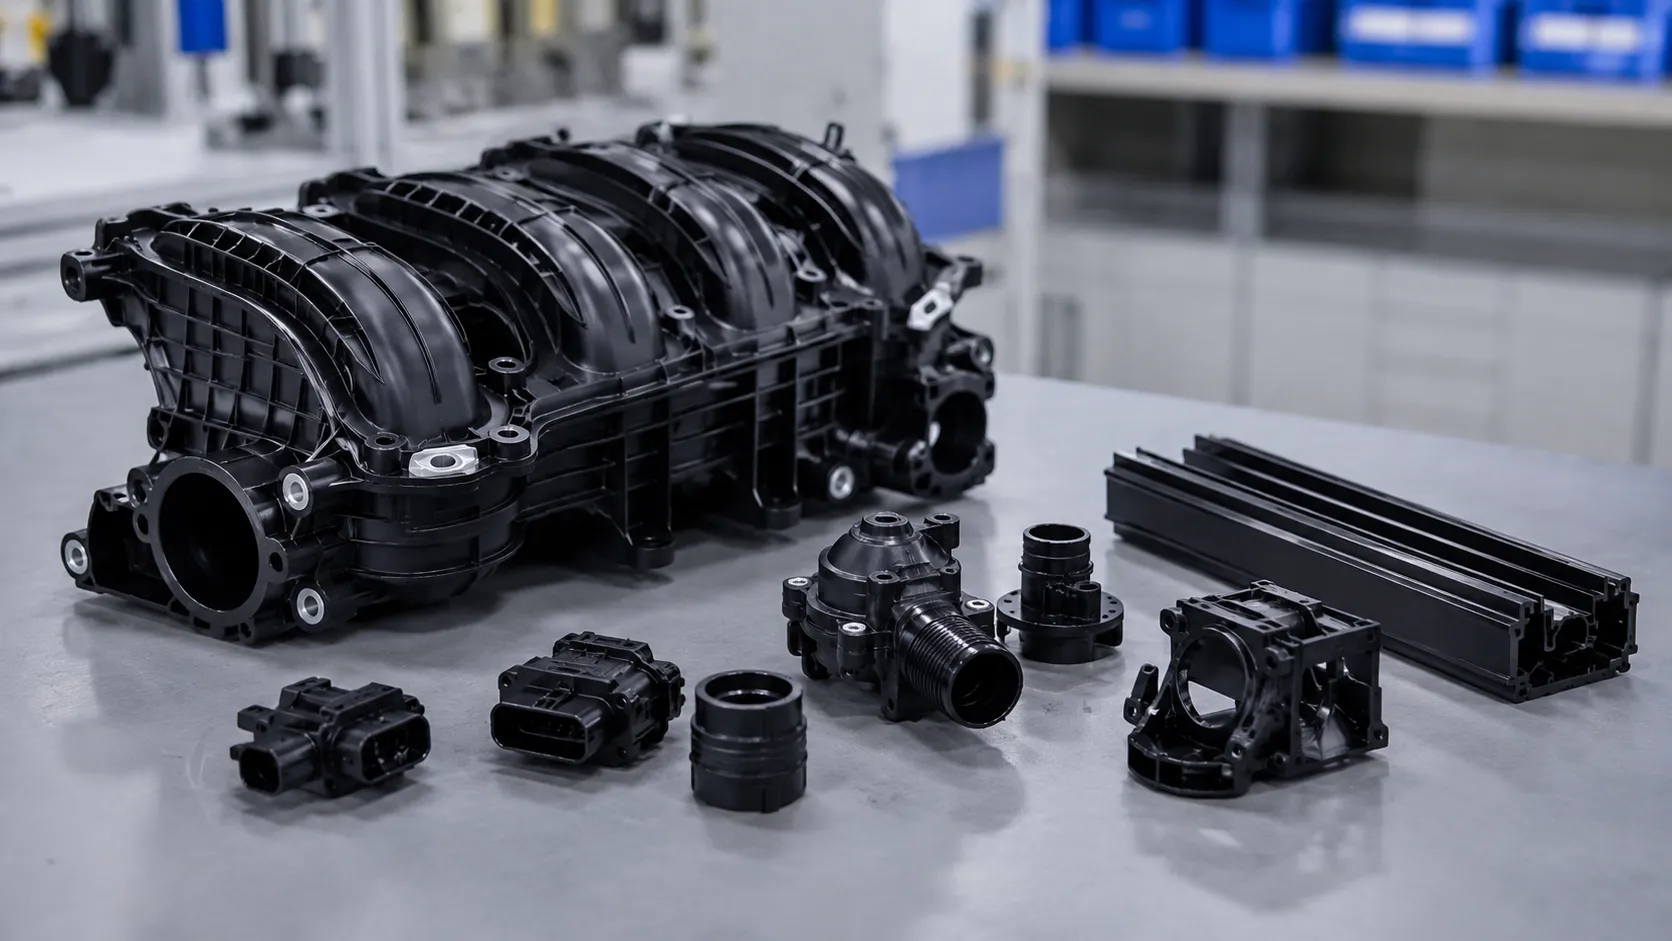
Intake runners, connector housings, rail profiles, under-hood brackets.
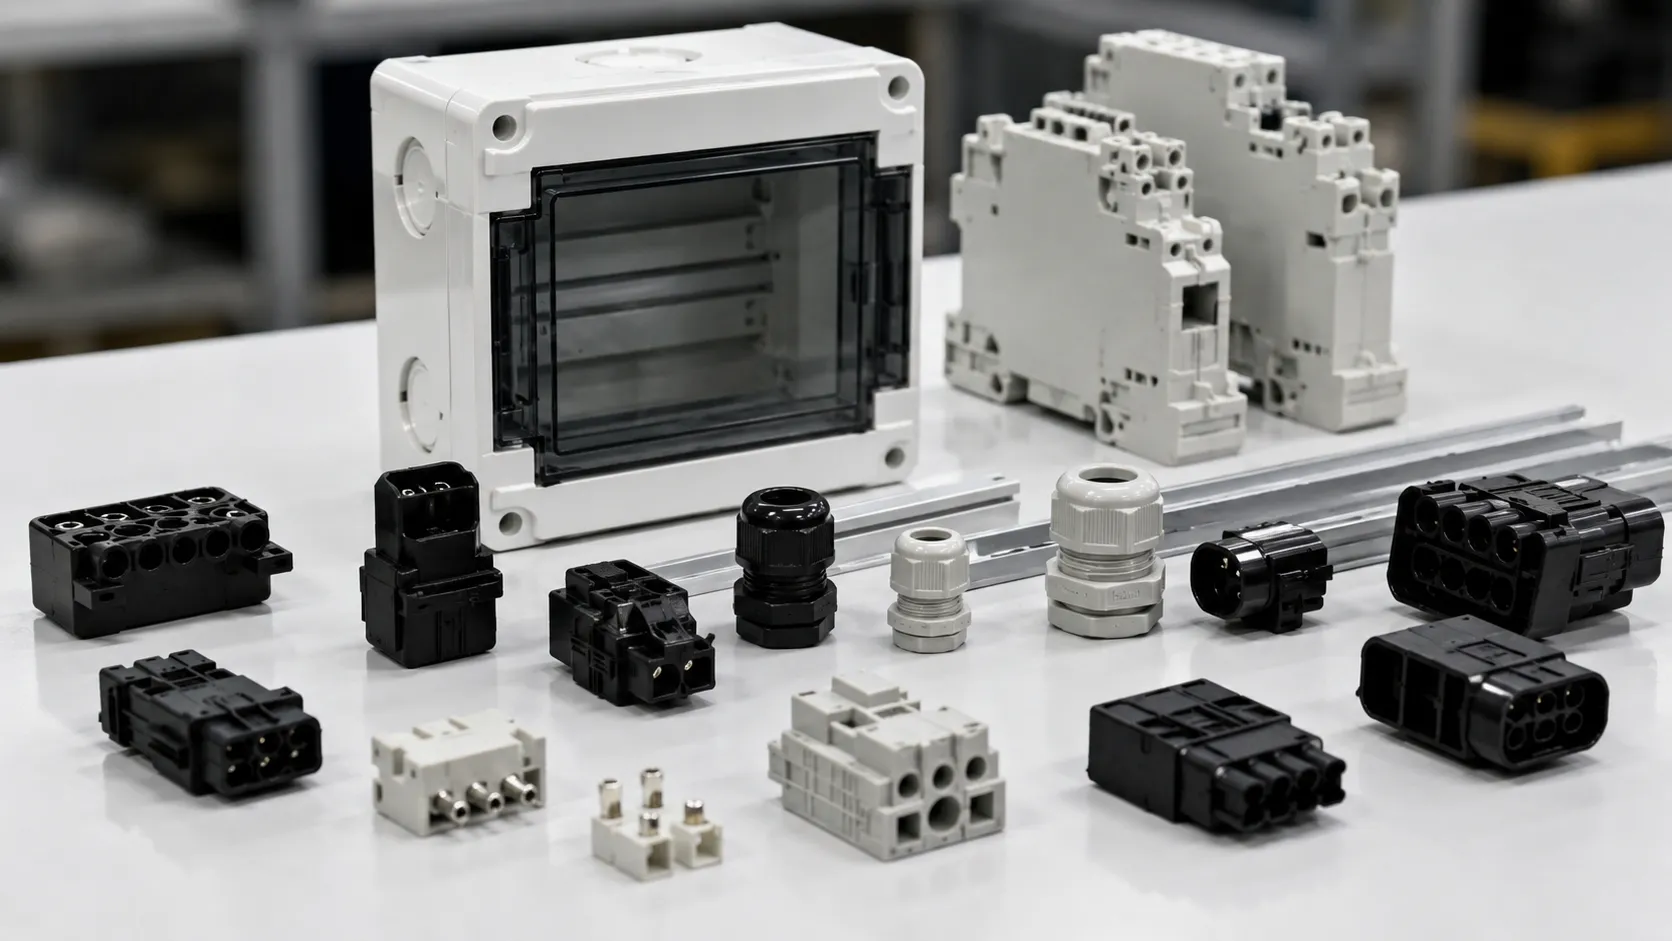
Electronics & Electrical
DIN-rail connectors, breaker housings, bus-bar insulators, LED profiles.
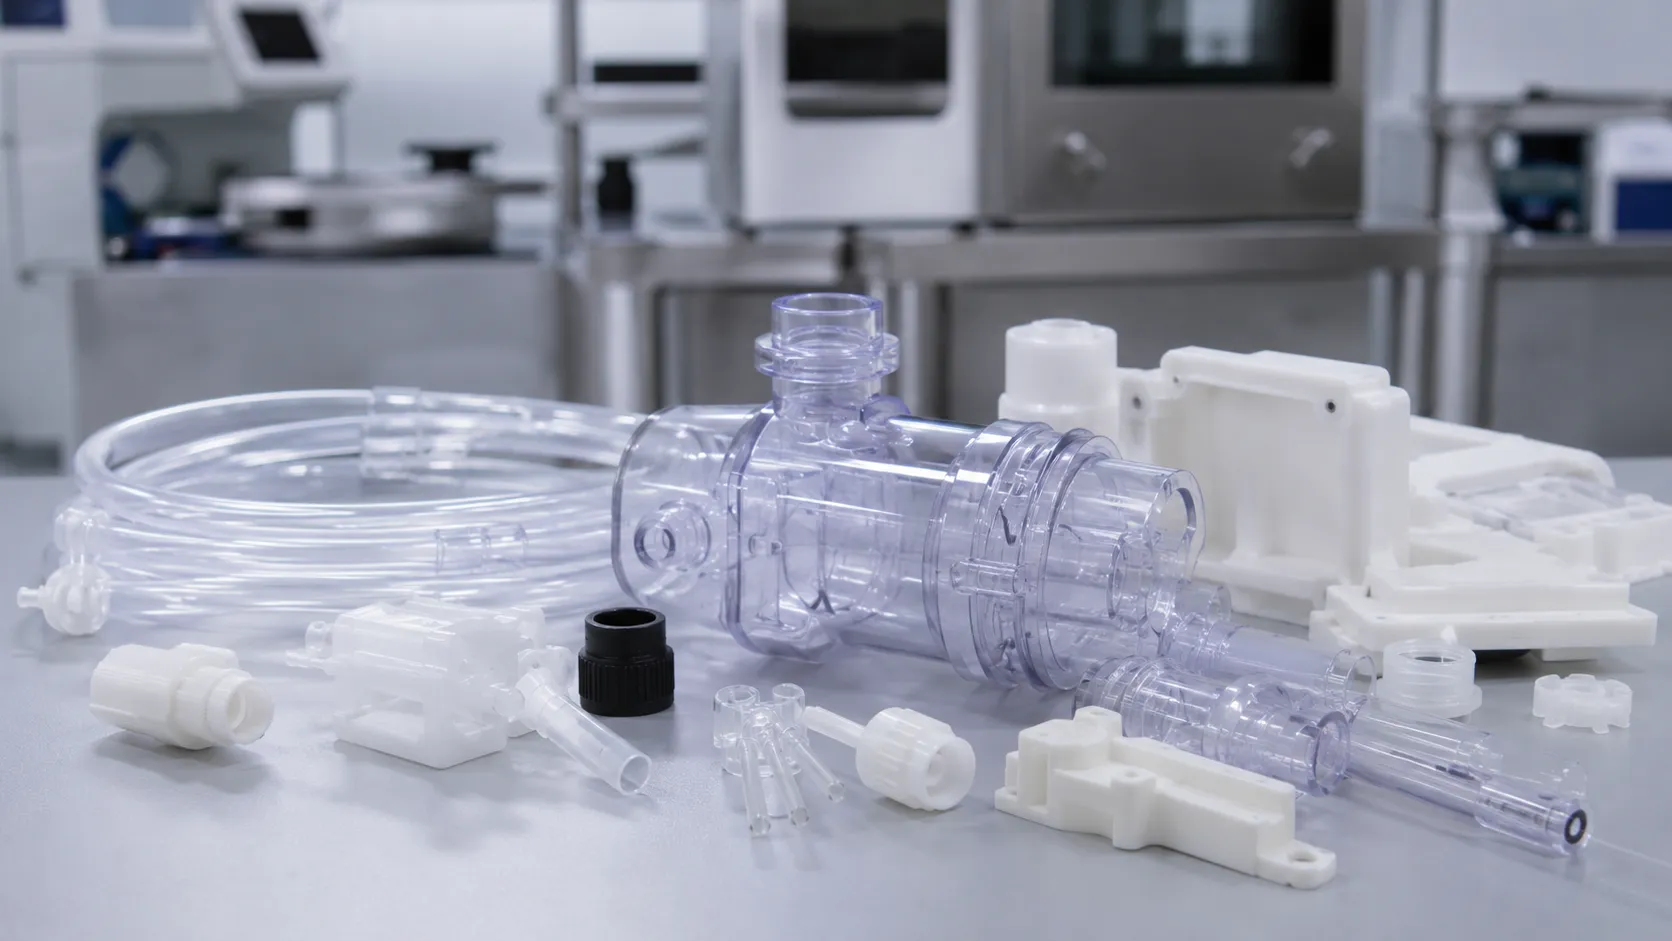
Medical Devices
Multi-lumen tubing, instrument handles, cleanroom-compatible profiles.
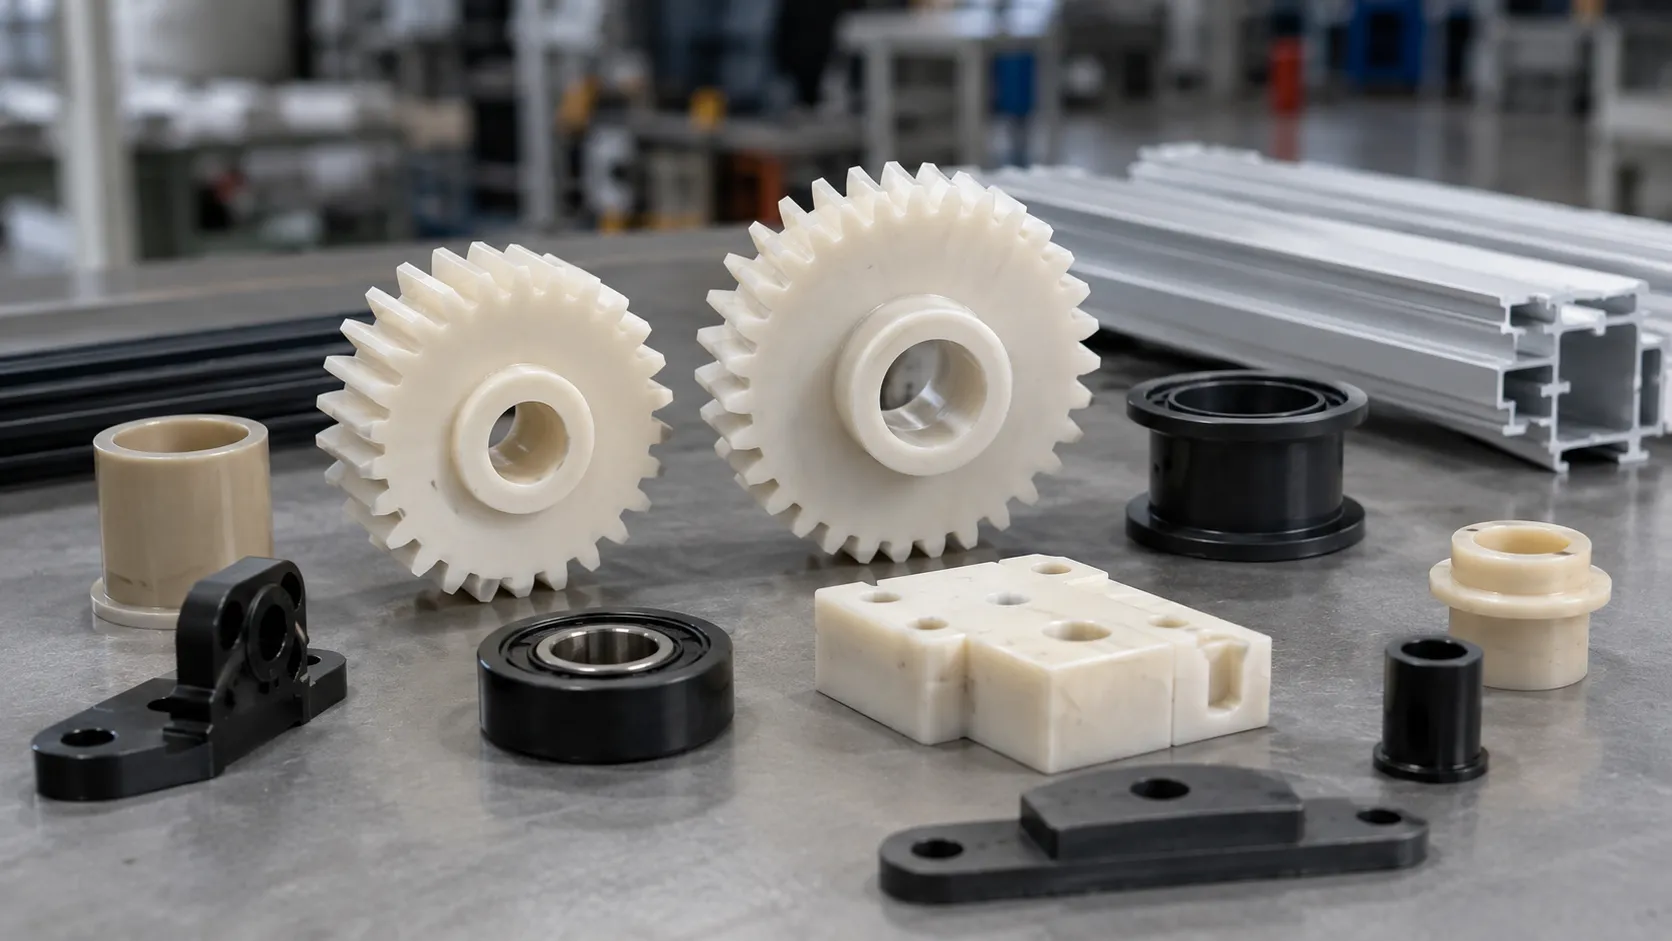
Industrial Components
POM gears, UPE wear strips, bearing cages, guide rails.
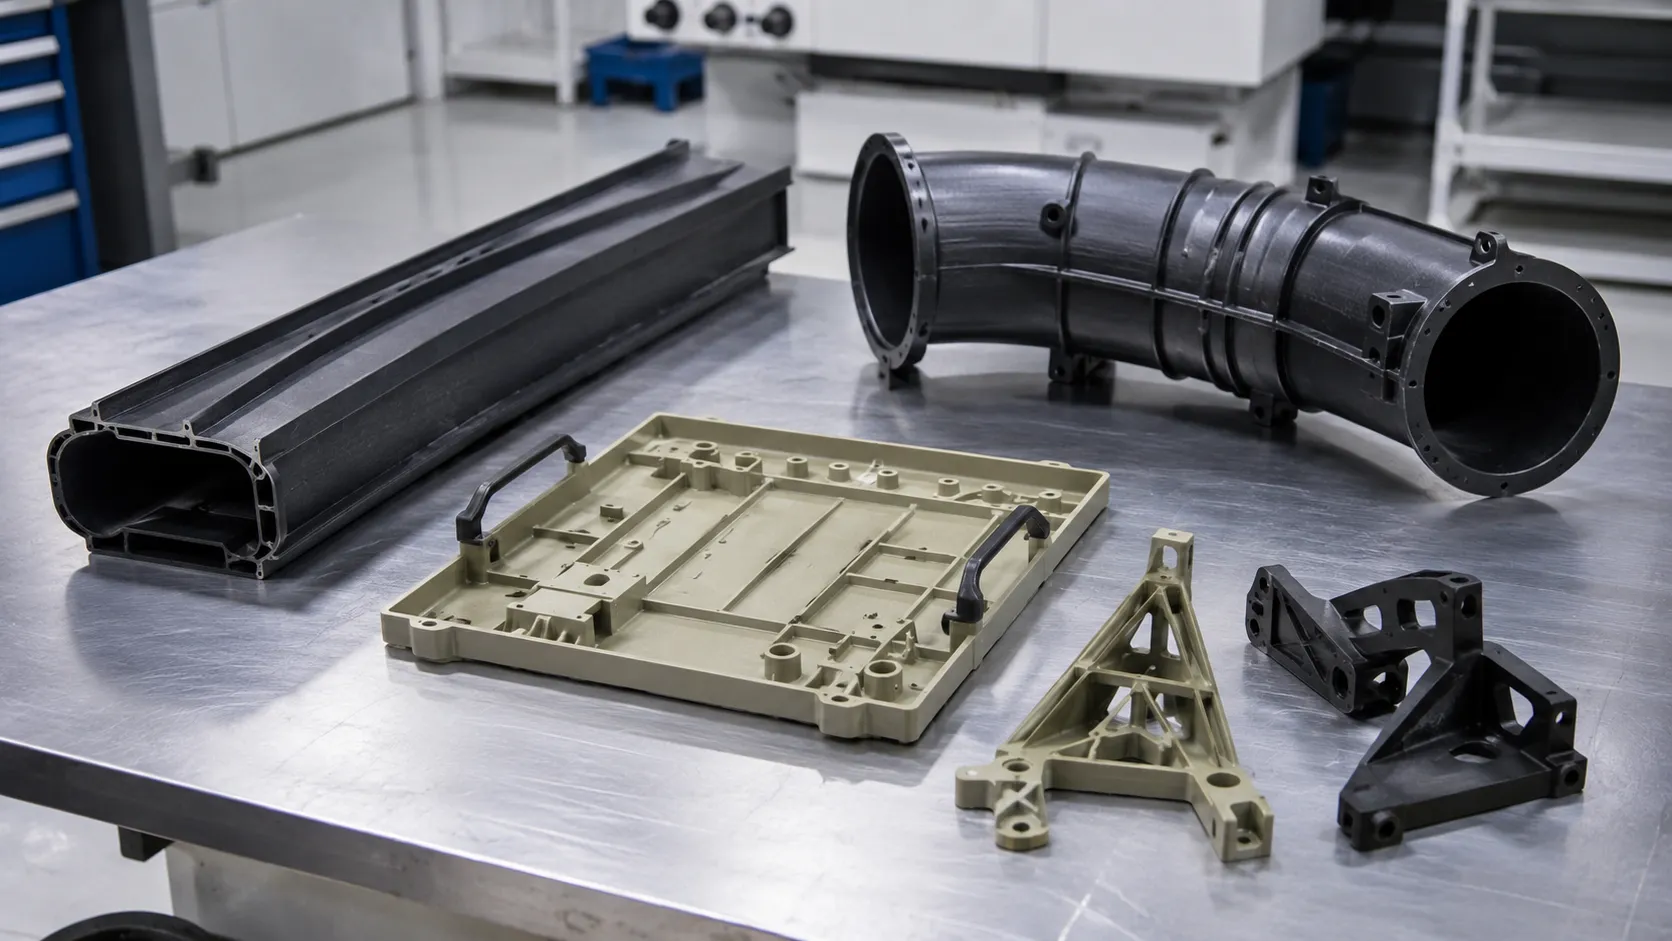
Aerospace
Cabin ducting, tray tables, cable conduits, lightweight brackets.
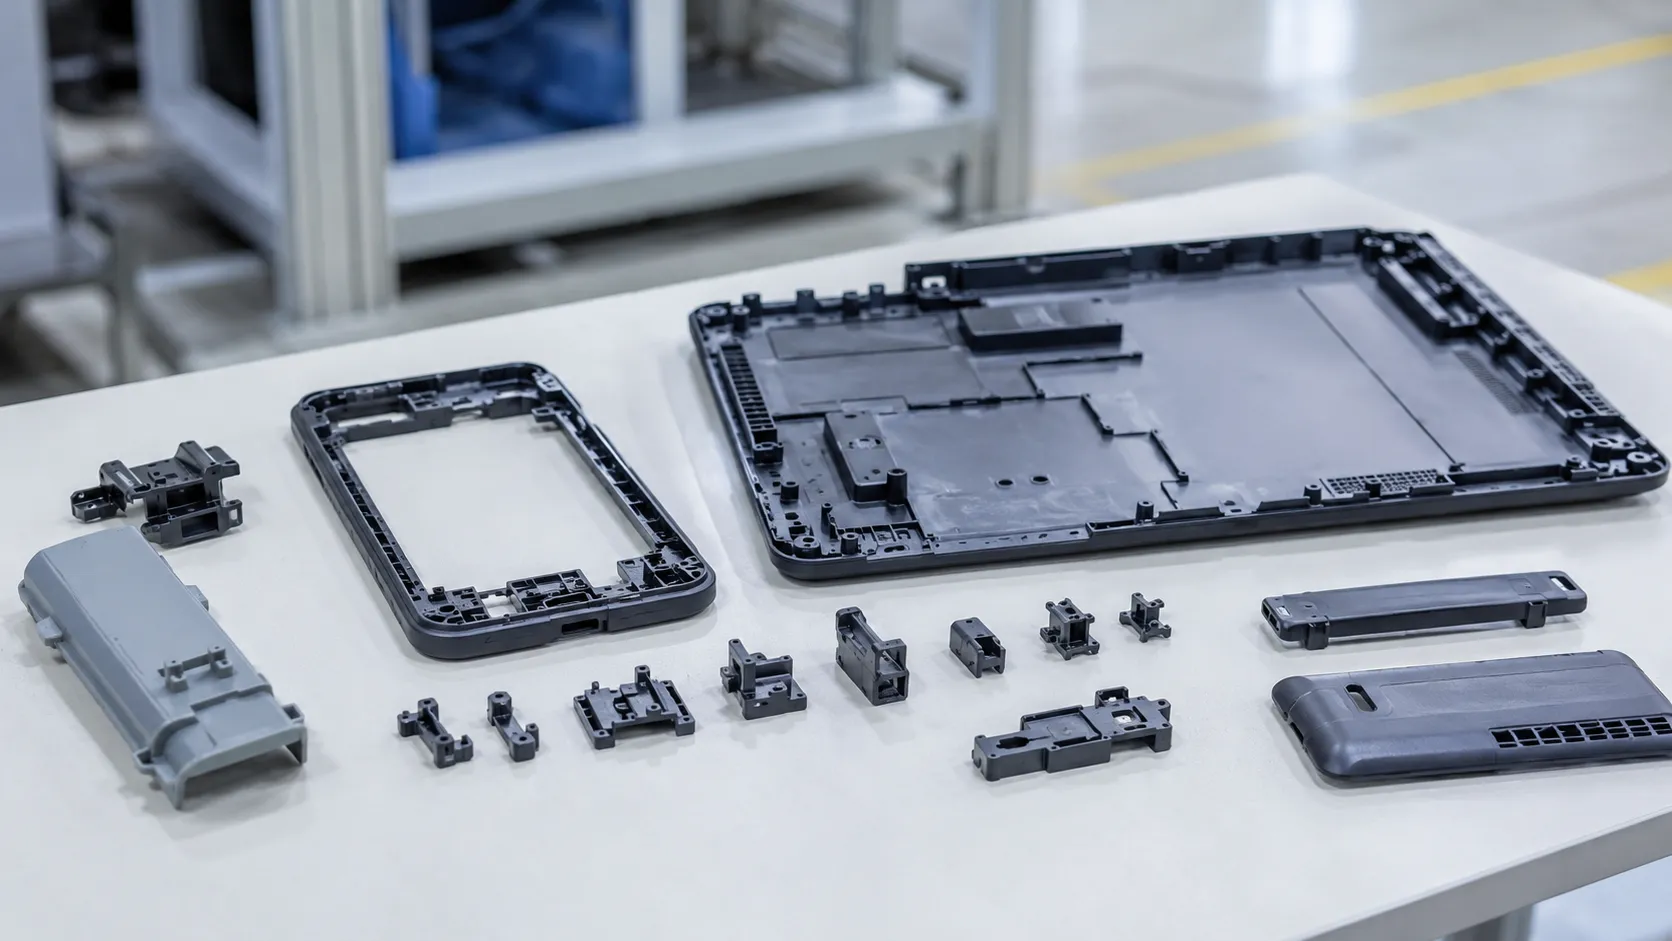
Consumer Electronics
Laptop bezels, speaker grilles, charging-dock profiles.
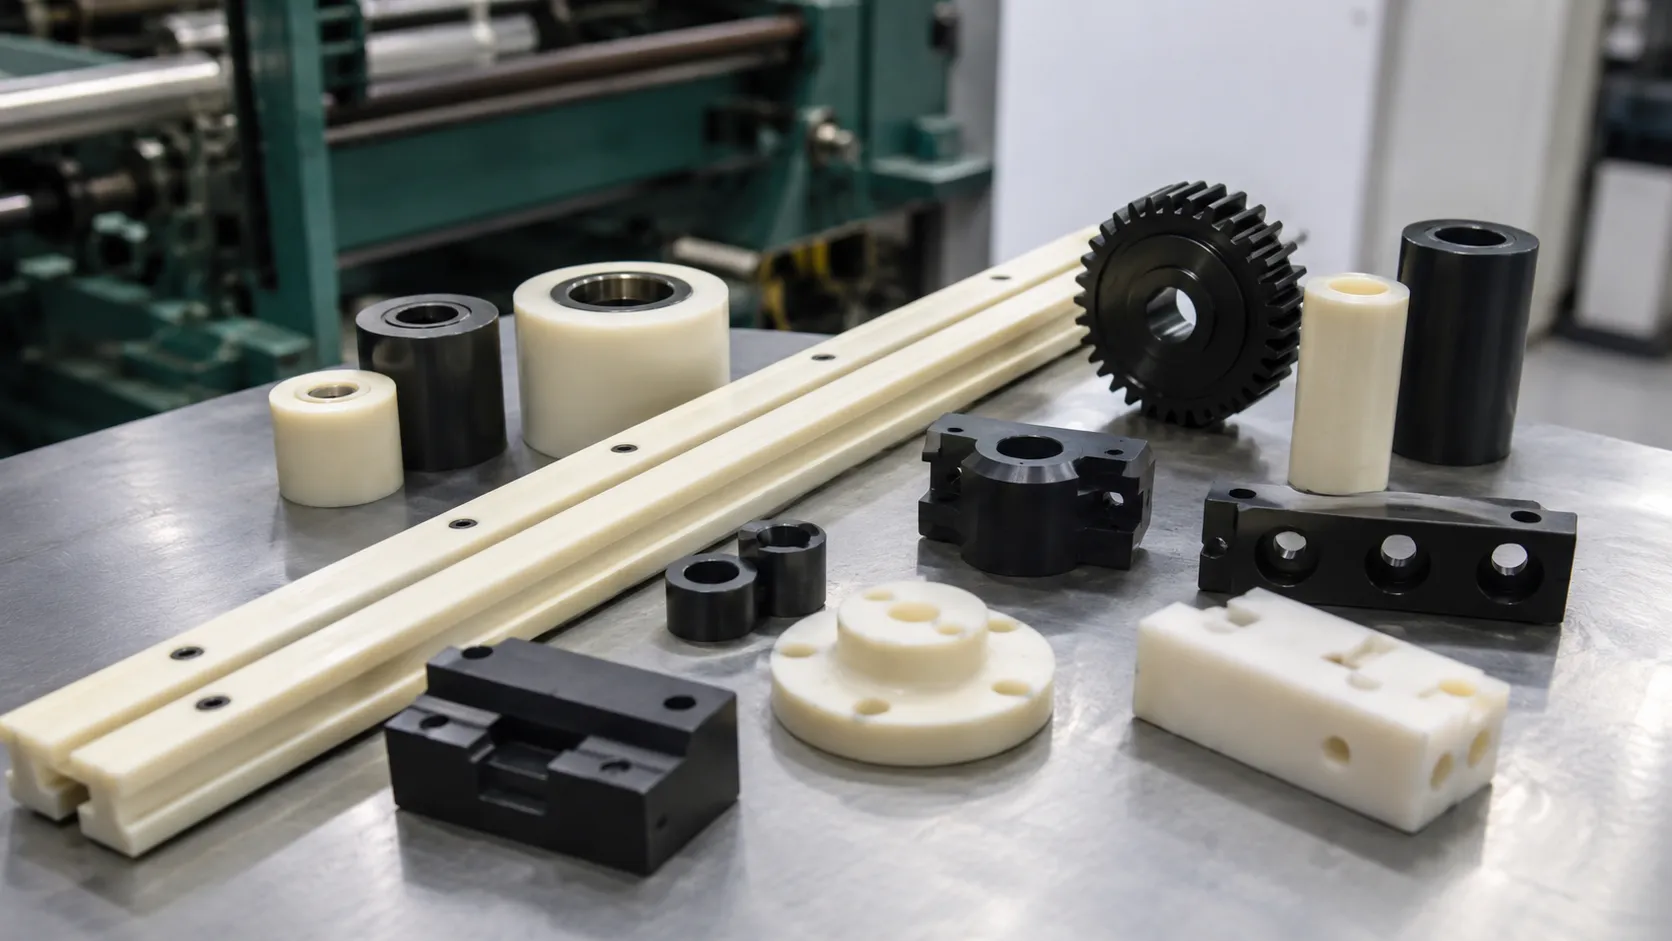
Machinery Parts
Conveyor rollers, chain guides, cam followers, custom bushings.
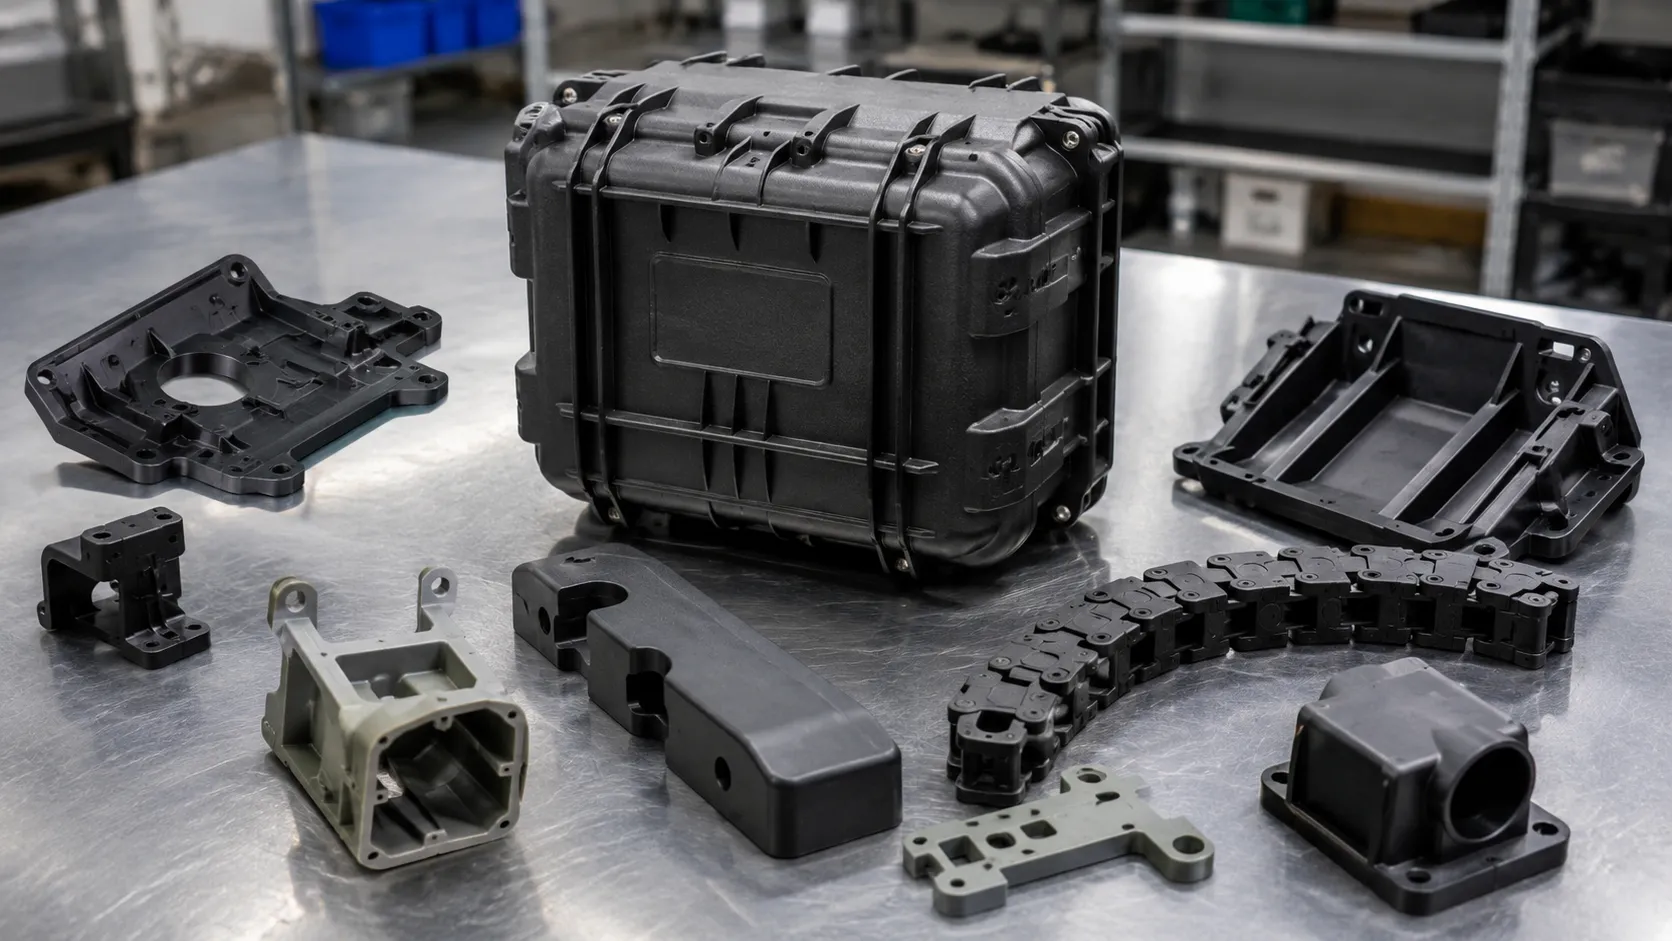
Defense & Military
Ruggedized enclosures, antenna radomes, field-equipment rails.
Product Range
Engineering Plastic Extrusion Lines for Sale: 3 Proven Configurations
Three configurations we build most often. Each ships with CE certification, FAT video report, and a 24-month core-component warranty. Need something outside these specs? Tell us your output target.
Best Precision
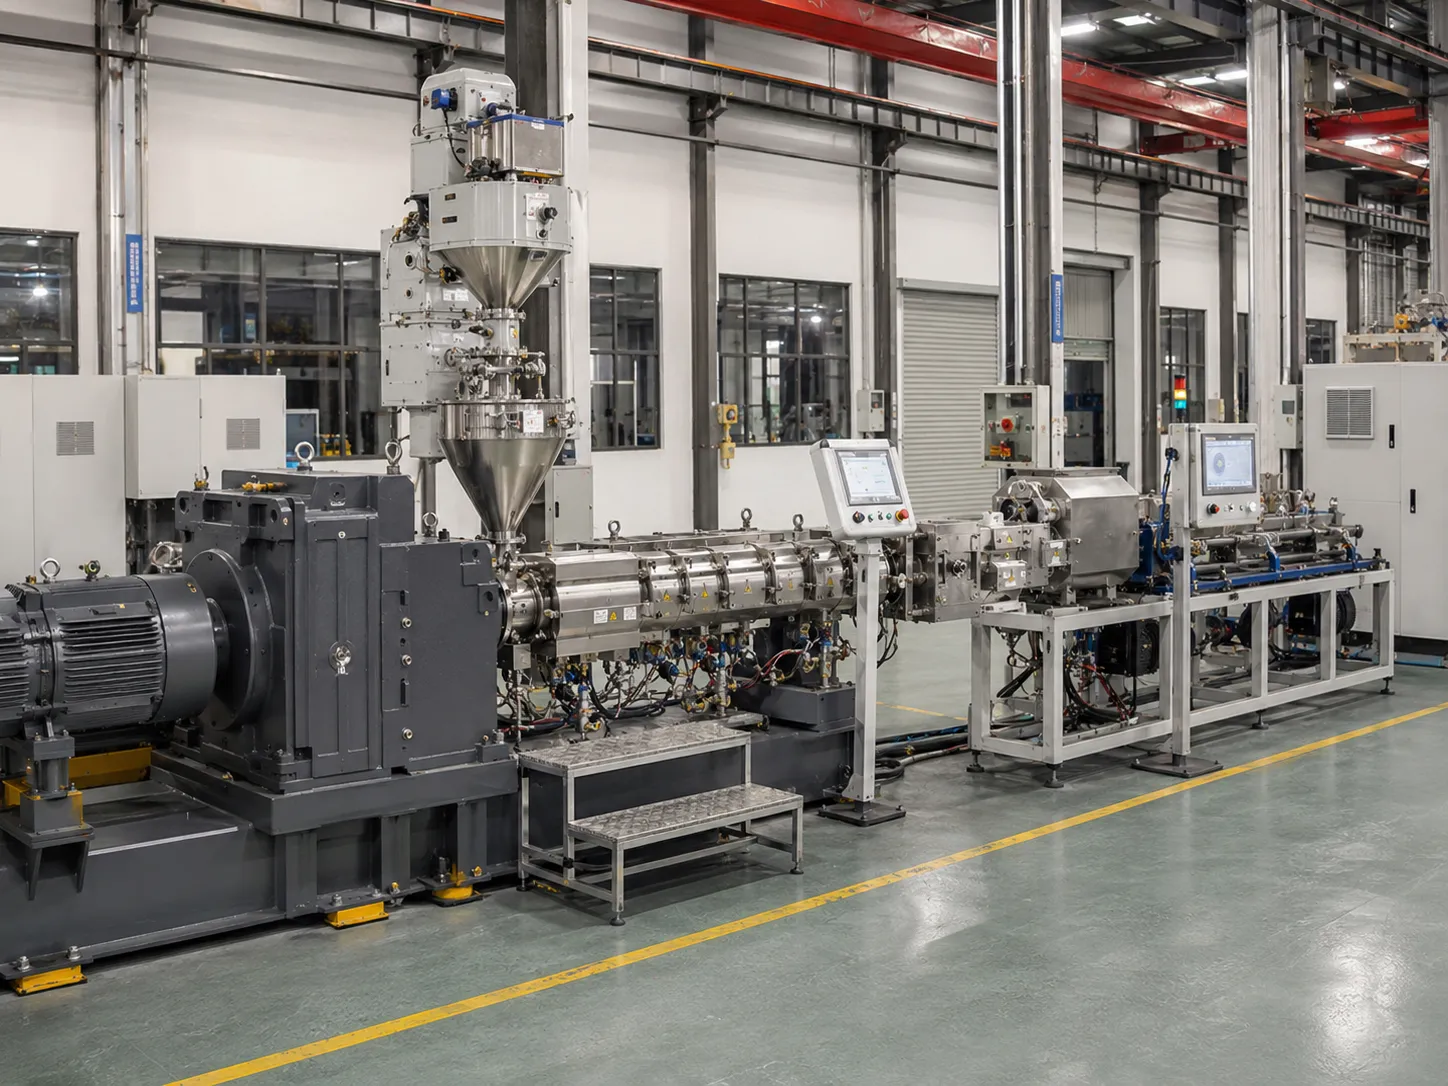
Precision Molding Extrusion Line
For auto clips, connector housings, and medical tubing where a tenth of a millimeter means a rejected lot. Laser gauge closes the loop on puller speed.
- Profile tolerance: ≤ ±0.03 mm
- Materials: PA, PC, POM, ABS
- UL & CE certified components
- Multi-language HMI interface
- Output: 300–600 kg/h
Best Value
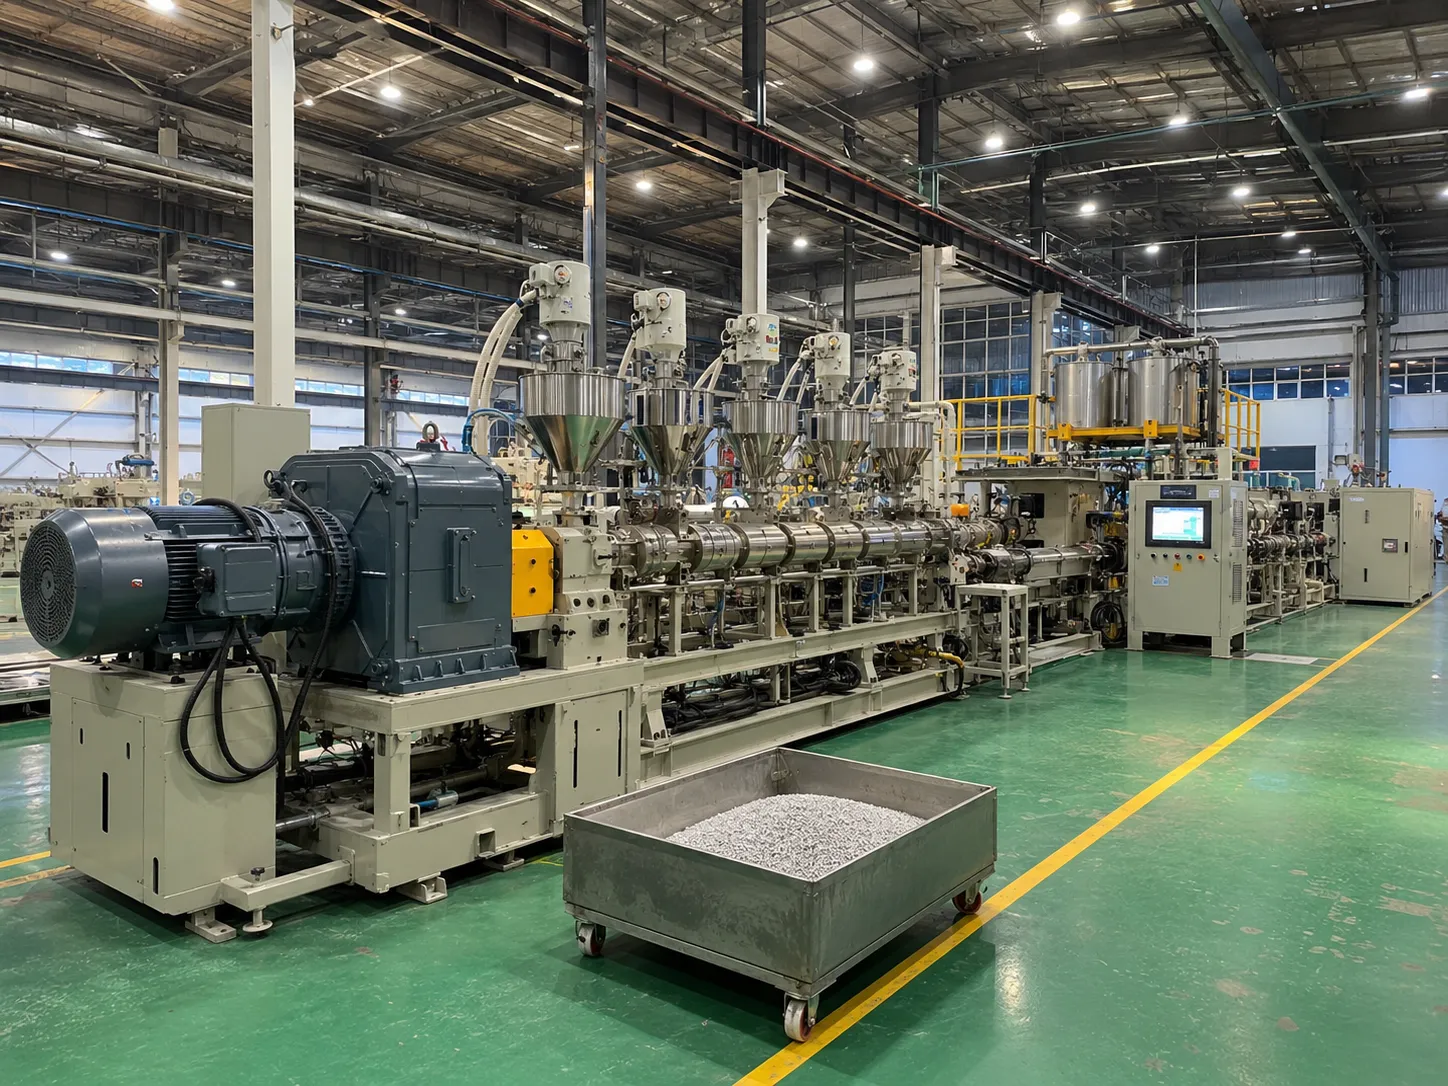
High-Efficiency Stable Extrusion Line
Designed for three-shift plants that need uptime above all. Optimized screw flight geometry cuts specific energy by 18% versus our previous generation.
- Energy savings: 18% vs. prior gen
- Die changeover: ≤ 15 minutes
- Noise at operator station: ≤ 73 dB
- Rated for continuous 24 h operation
- Output: 500–1000 kg/h
Most Versatile
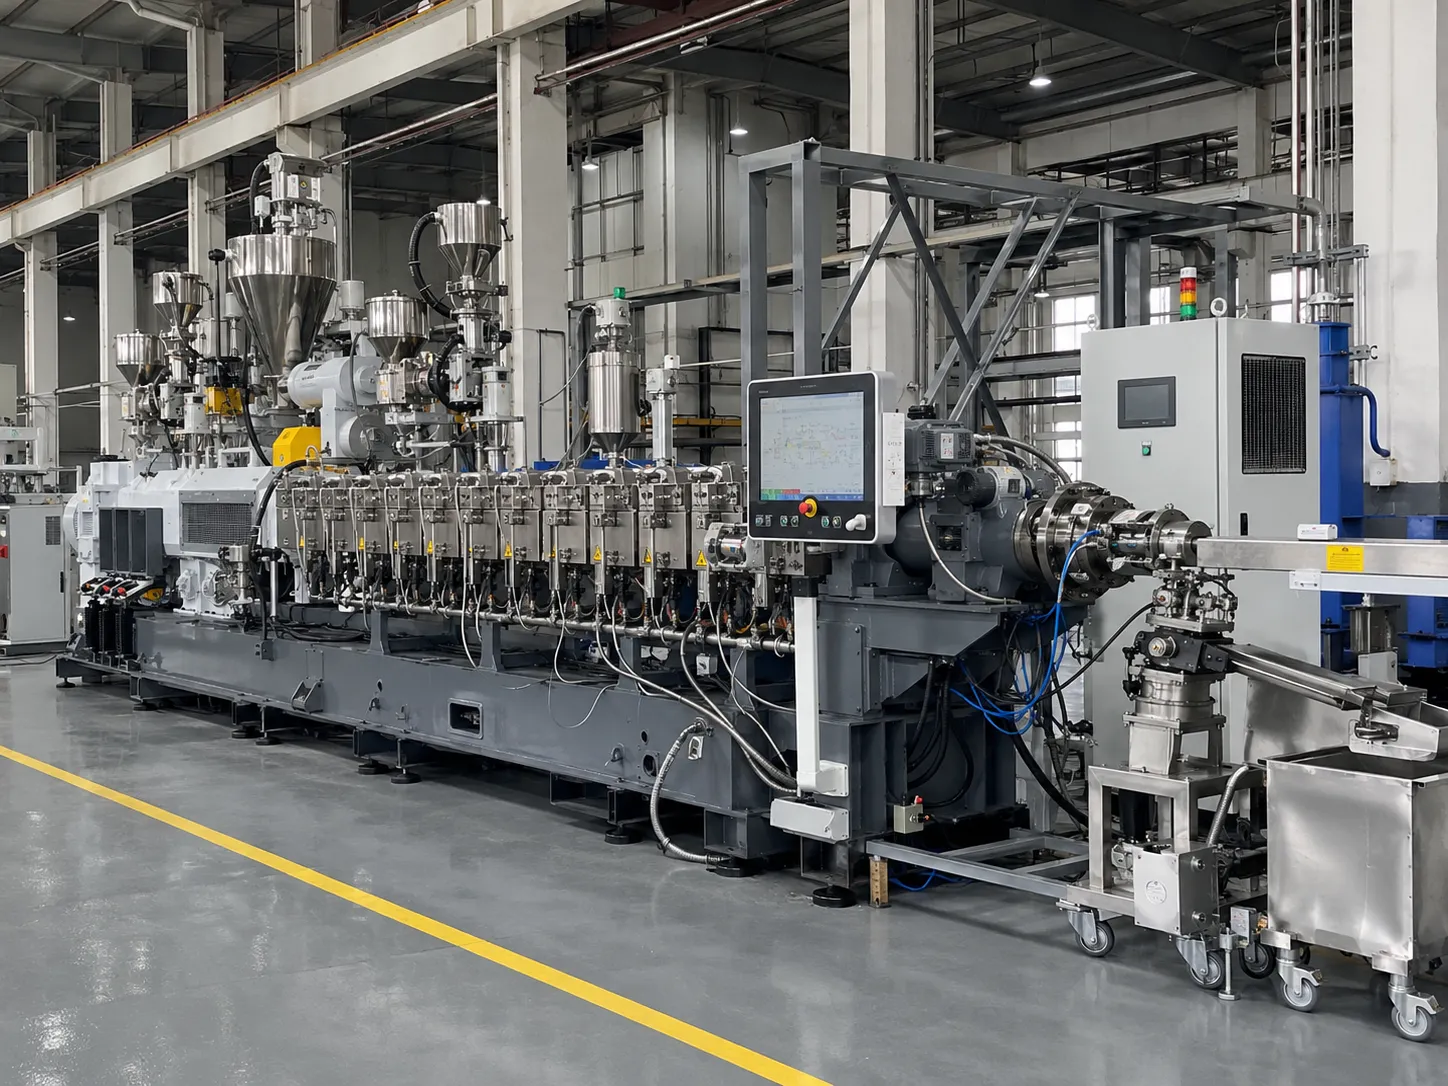
Multi-Formula Compatible Extrusion Line
Contract manufacturers and compounders run a dozen recipes a week. Store 150+ parameter sets; switch materials without touching the screw configuration.
- Handles 12+ formulations
- 150+ stored process recipes
- Corrosion-resistant barrel option
- Rated to 350 ℃ barrel zones
- Output: 400–1200 kg/h
Technical Data
Technical Specifications & Model Selection Guide
Standard configurations below. Screw diameter, L/D, and downstream are adjustable — send your product drawing and we confirm which model fits.
| Parameter | Specification |
|---|---|
| Brand / Origin | UET · Nanjing, China (own factory, not trading company) |
| Output Range | 120–2000 kg/h depending on model, resin, and product geometry |
| Screw Type | Co-rotating intermeshing twin screw; modular elements on splined shafts |
| Barrel Construction | Bimetallic centrifugal casting, hardness HRC 58-62, segmented design |
| Automation | Feeding → extrusion → cooling → cutting → stacking in one PLC sequence |
| Certifications | CE machinery directive, ISO 9001:2015, UL components (optional) |
| Warranty | 18 months from B/L date; 24 months on screws, barrels & gear box |
| Electrical Components | Siemens / ABB inverters, Schneider contactors, Siemens S7-1500 PLC |
| Compatible Resins | PA6, PA66, PC, POM, ABS, PBT, PET, PPS, PEEK, GF up to 50% |
| Product Forms | Profiles, tubes, rods, sheets, pellets (with strand or underwater cut) |
| Dimension Range | 20–500 mm cross-section; custom dies beyond 500 mm on request |
| Control & Connectivity | 15″ HMI, 150-recipe storage, OPC-UA / Modbus TCP for MES linkage |
Available Model Configurations
| Model | Screw Dia. (mm) | L/D | Speed (rpm) | Motor (kW) | Output (kg/h) | Torque |
|---|---|---|---|---|---|---|
| UET-35E | 35.6 | 32–40 | 400–600 | 22–45 | 120–220 | 10.5 |
| UET-50E | 50.5 | 36–40 | 400–600 | 55–75 | 300–400 | 11.3 |
| UET-65E | 62.4 | 36–40 | 400–600 | 110–160 | 500–700 | 11.3 |
| UET-75E | 71 | 40–44 | 400–600 | 160–250 | 700–1000 | 11.3 |
| UET-95E | 93 | 40–48 | 400–600 | 280–450 | 1000–1500 | 11.3 |
| UET-110E | 110 | 40–48 | 350–500 | 500–710 | 1500–2000 | 12.0 |
Need a lab-scale 20 mm trial unit or output beyond UET-110E? Send your target kg/h — we match the smallest frame that does the job.
Comparison
UET vs. Other Engineering Plastic Extrusion Line Manufacturers
Side-by-side specs from real quotations we have seen cross our desk. Numbers are for 65 mm class lines processing PA6-GF30.
| Feature | Typical Supplier | UET Machine |
|---|---|---|
| Melt Homogeneity | 92–95% | 99.8% |
| Zone Temperature Accuracy | ±2 ℃ | ±0.3 ℃ |
| Profile Tolerance | ±0.1 mm | ±0.03 mm |
| Specific Energy | Industry baseline | 10–18% lower |
| Material Compatibility | 3–5 recipes | 12+ recipes |
| Core Warranty | 6–12 months | 24 months |
| Engineer Response | 3–7 days | < 72 hours |
| Factory Acceptance Test | ✗ Not always | ✓ With your resin |
| Screw / Barrel Hardness | Nitriding HV 950 | Bimetallic HRC 58-62 |
| Recipe Storage | Manual write-down | 150 digital slots |
Transparent Process
Order Process: From Enquiry to Commissioning Your Extrusion Line
Four steps, fixed timelines. Standard models ship from stock; custom lines get the engineering hours they need — no shortcuts on screw design.
1
Consult & Quote
Send resin type, target output, product drawing, and plant voltage. An application engineer replies with an itemized quotation — no bundled mystery pricing.
Reply within 2 hours2
Engineering & Approval
We size the screw, pick barrel zones, design the die, and lay out downstream. You approve the GA drawing before a single part is cut.
2–5 working days3
Build & Factory Test
Machining, assembly, and a full-load run with your material on site. Watch via live video or fly in — we record torque, amps, and tolerance data for your sign-off.
Stock: 1–2 weeksCustom: 4–6 weeks4
Ship & Commission
Seaworthy crating, fumigation cert, and full doc pack. Our engineer guides installation, trains your operators, then stays on WhatsApp for life-of-machine support.
7–15 days transit
Timeline summary: stock lines ship in 1–2 weeks, custom lines in 4–6 weeks. Add 7–15 days for ocean freight door-to-door.
Customer Proof
Customer Reviews: Real Feedback from Extrusion Line Operators
Unedited feedback from buyers running UET engineering plastic extrusion lines in daily mass production. Names published with permission.
★★★★★
Six months in, zero unplanned stops. We run PA66-GF30 automotive clips and the laser gauge holds 0.02 mm without us touching the puller. New operators were productive by the second shift — the HMI walk-through screens actually make sense.
Mike Thompson
Production Manager · Automotive Tier-2★★★★★
We process PA, PC, and POM on the same frame — recipe change takes ten minutes including purging. Temperature stability is noticeably tighter than our old line; tensile test variance dropped and our reject rate fell 18% in the first quarter.
Lisa Müller
Technical Supervisor · Electronics Compounder★★★★★
Compared five suppliers before choosing UET. Their quote was the only one that broke down every component line-by-line. Machine arrived on schedule, energy meter reads 12% below our previous 65 mm line, and the commissioning engineer stayed until we ran 8 hours of good product.
Juan García
Purchasing Director · Building Materials
Explore More
Explore Related Extrusion Equipment
Pair your engineering plastic line with complementary systems — all built in the same Nanjing factory, all on one after-sales contract.
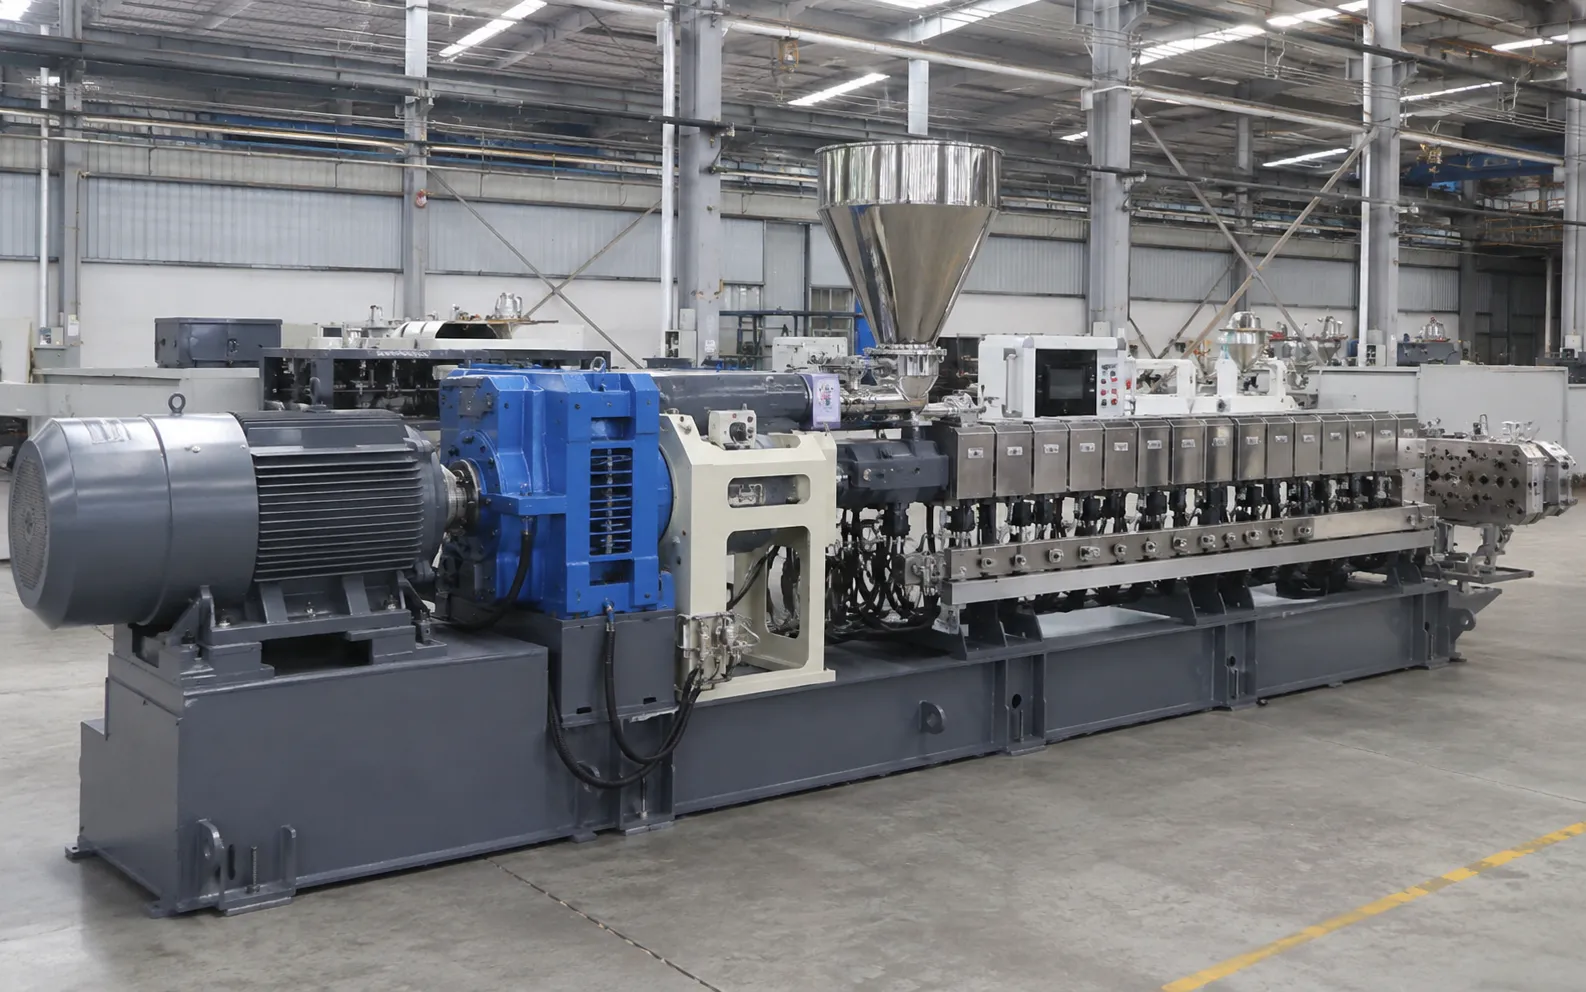
Twin Screw Extruder
High-torque compounding for masterbatch, color concentrates, and modified plastics.
View Details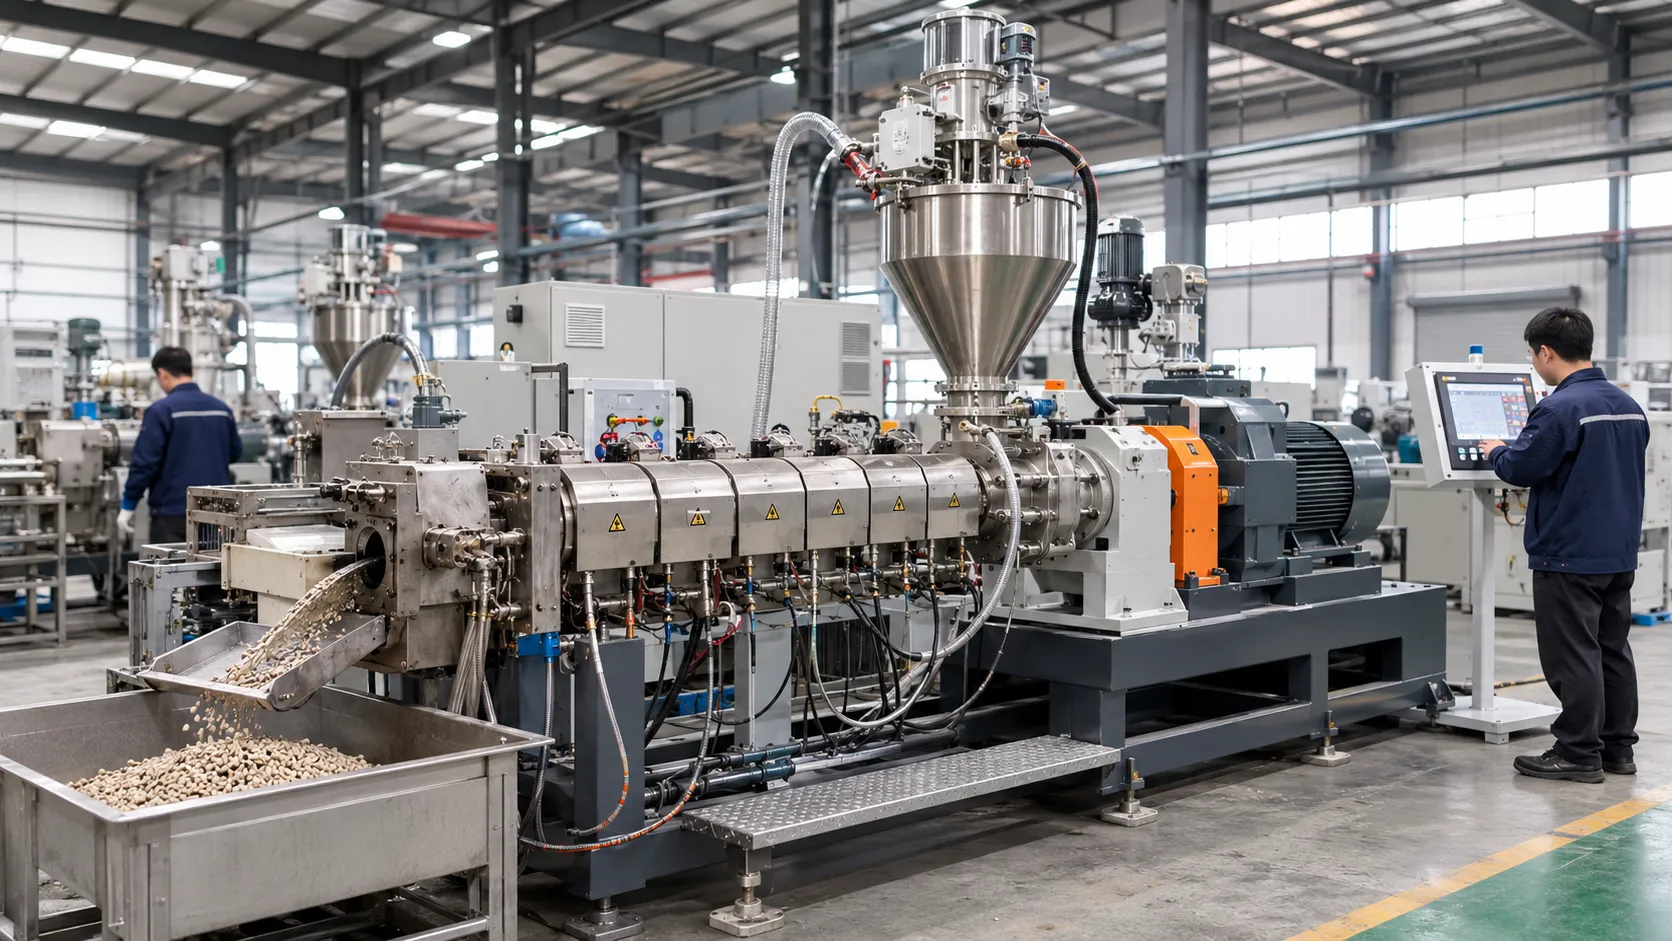
Bio Extruder
Gentle, low-temperature processing for PLA, PBAT, and starch-blend resins.
View Details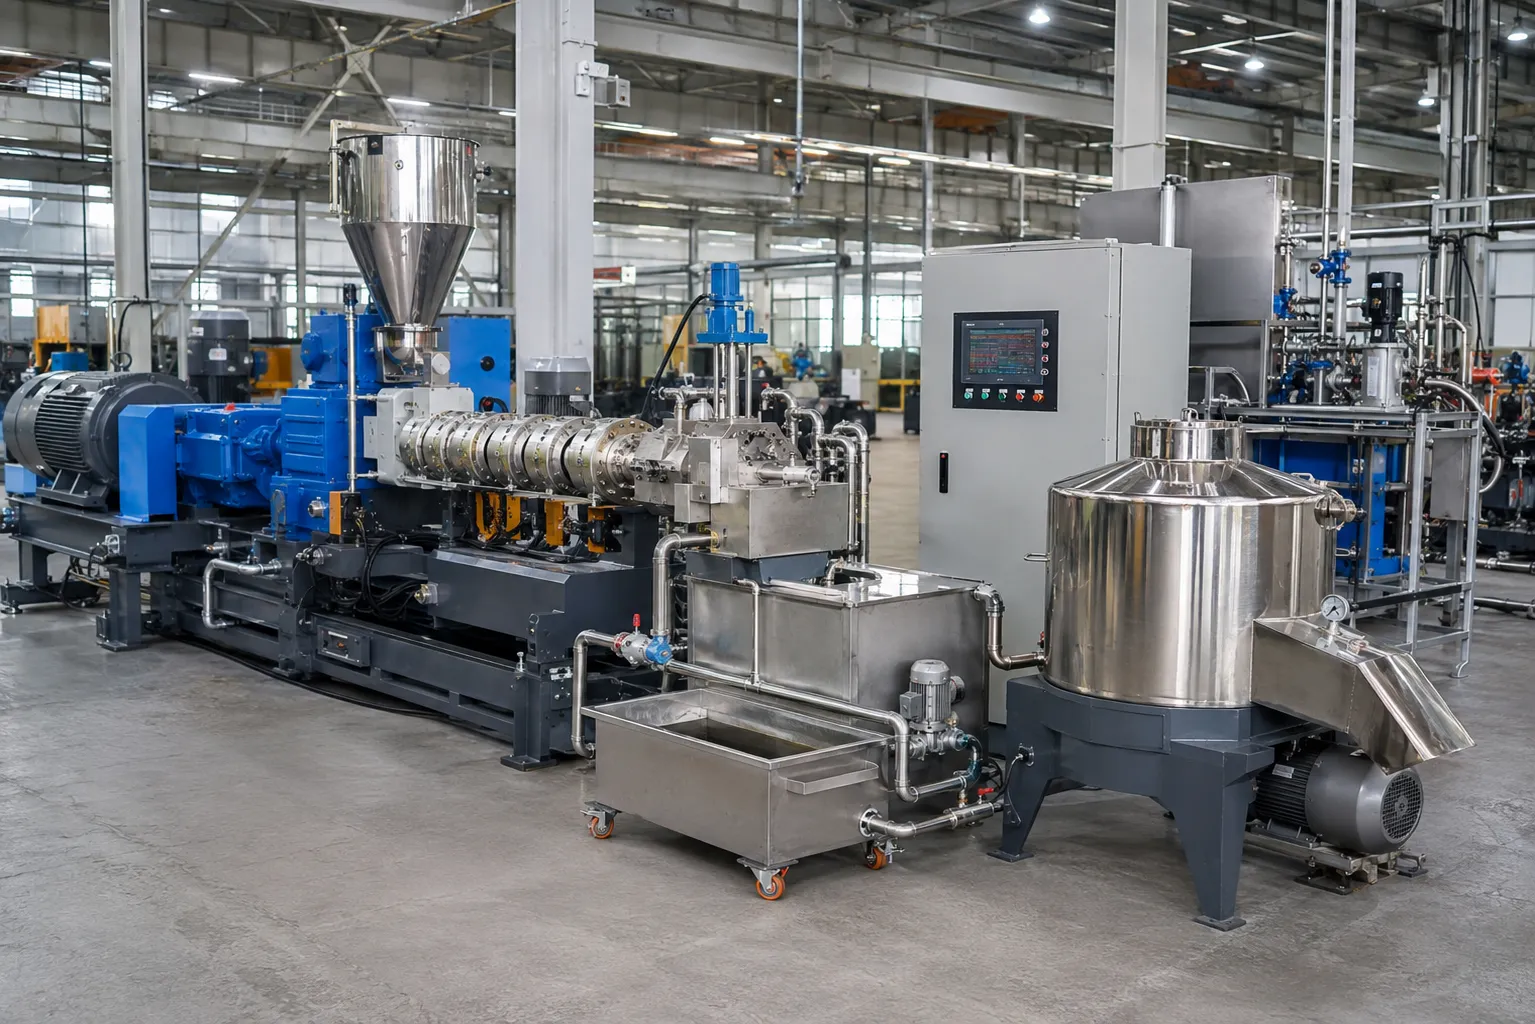
Underwater Pelletizing
Spherical, low-fines pellets with integrated face-cut, cooling, and centrifugal drying.
View Details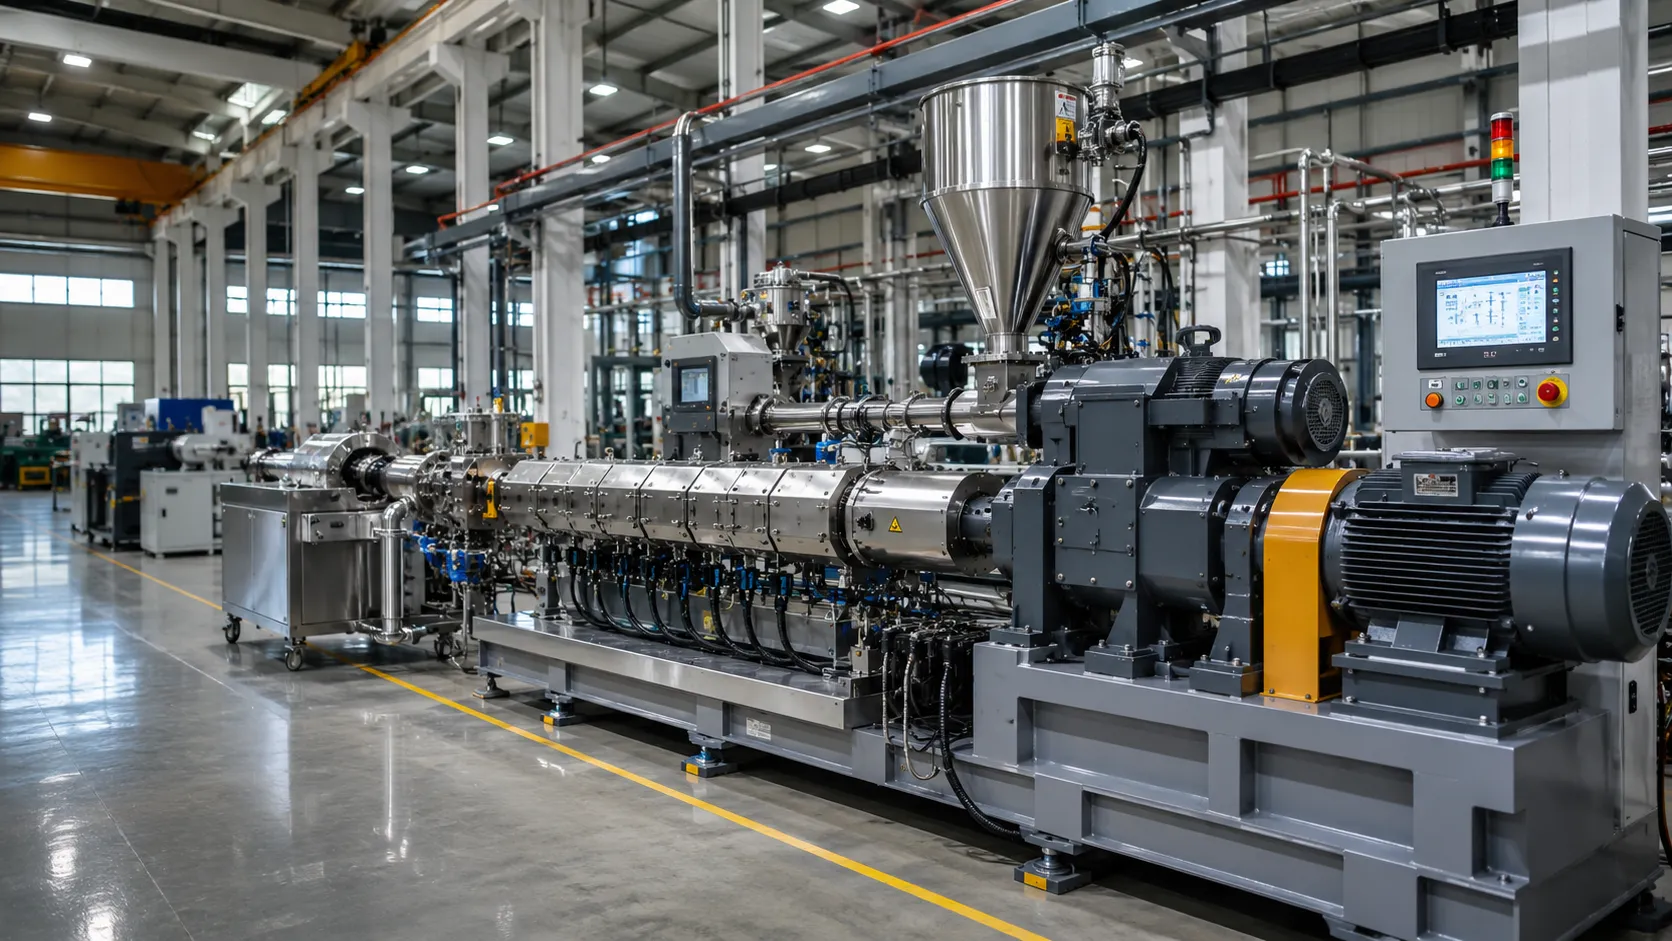
Reactive Extruder
In-line polymerization, grafting, and chain-extension under vacuum devolatilization.
View Details
Technical Support
Engineering Plastic Extrusion Line FAQ
Questions our application engineers field most often. If yours is not here, send it directly — a human replies within two working hours.
General engineering grades — PA6, PA66, PC, POM, ABS, PBT, PET, PPO — run on our standard screw packages. For high-temperature specials like PEEK, PPS, PEI, and PI we fit hardened tool-steel elements, extend the L/D to 48, and add liquid-nitrogen purging on the vents. Glass fiber up to 50% loading is handled with bimetallic barrels and chrome-plated feed throats. Tell us your exact grade and filler percentage; we confirm compatibility before you sign anything.
Up to 15% GF the standard nitrided set lasts 12–18 months. Above 20% we specify bimetallic-lined barrels (HRC 58-62) and tungsten-carbide-overlay screw tips as standard. Customers running PA6-GF50 report 3× the service life versus their previous supplier’s nitrided screws. The transmission box is also uprated to handle the extra torque glass fiber demands.
Stock models (UET-50E, UET-65E in common configurations) leave the factory in 1–2 weeks. Custom screw designs, special dies, or exotic metallurgy push that to 4–6 weeks. Ocean freight adds 7–15 days depending on port. Warranty runs 18 months from bill-of-lading date or 12 months from commissioning, whichever comes first. Screws, barrels, and the gear box carry 24 months. During warranty we ship replacement parts by air at our cost.
Each shift: purge residual melt from the die land, wipe the sizing plates, and check vacuum pump oil level. Weekly: grease haul-off bearings, verify heater-band amperage, and inspect the cutter blade. Monthly: pull the screen pack, measure screw flight clearance at three points. The PLC logs cumulative run-hours and triggers service reminders so nothing is left to memory. Most plants budget 20 minutes of operator time per shift — no dedicated maintenance crew required.
Yes. We pre-wire for laser micrometers (Zumbach or Beta LaserMike), X-ray wall-thickness sensors, and surface-defect cameras. The Siemens S7-1500 PLC exposes OPC-UA and Modbus TCP endpoints, so your MES pulls cycle data directly. Flying saws, guillotine cutters, and coil winders all communicate via Profinet — the line adjusts puller speed in real time based on gauge feedback.
Five factors in practice: screw diameter and L/D set the volumetric ceiling; resin MFI determines how fast the melt can be conveyed without overheating; gear-box torque caps shear input; die flow length restricts pressure drop; and cooling capacity governs how fast the profile solidifies. When we quote, we simulate all five against your product geometry. A UET-95E running PA6 profile typically sustains 1200 kg/h; the same frame on PC sheet may top out at 900 kg/h because of cooling limits, not screw capacity.
FR additives decompose if they sit too long above their onset temperature. We use low-shear distributive mixing elements, keep residence time under 90 seconds in the melt zone, and add side-feeders downstream so the FR enters after peak shear. For formulations that off-gas (aluminum trihydrate, intumescent systems), twin vacuum vents at 28D and 36D pull volatiles below 200 ppm. Customers running UL94 V-0 connector stock report consistent certification pass rates after switching to this configuration.
Three things move the needle fastest. First, recipe storage — operators call up a validated parameter set instead of dialing in by hand, which eliminates the bulk of startup scrap. Second, closed-loop gauge control — the puller auto-corrects wall thickness drift before it becomes an out-of-spec part. Third, stable drying — inline moisture monitoring stops the splay-and-bubble rejects that plague PA and PC runs. Plants that adopt all three typically move from 92% to 97%+ first-pass yield within 60 days.