20+ Years Extruder Manufacturing Expert
Industrial-Grade Recycled Plastic Extruder for High-Efficiency Processing
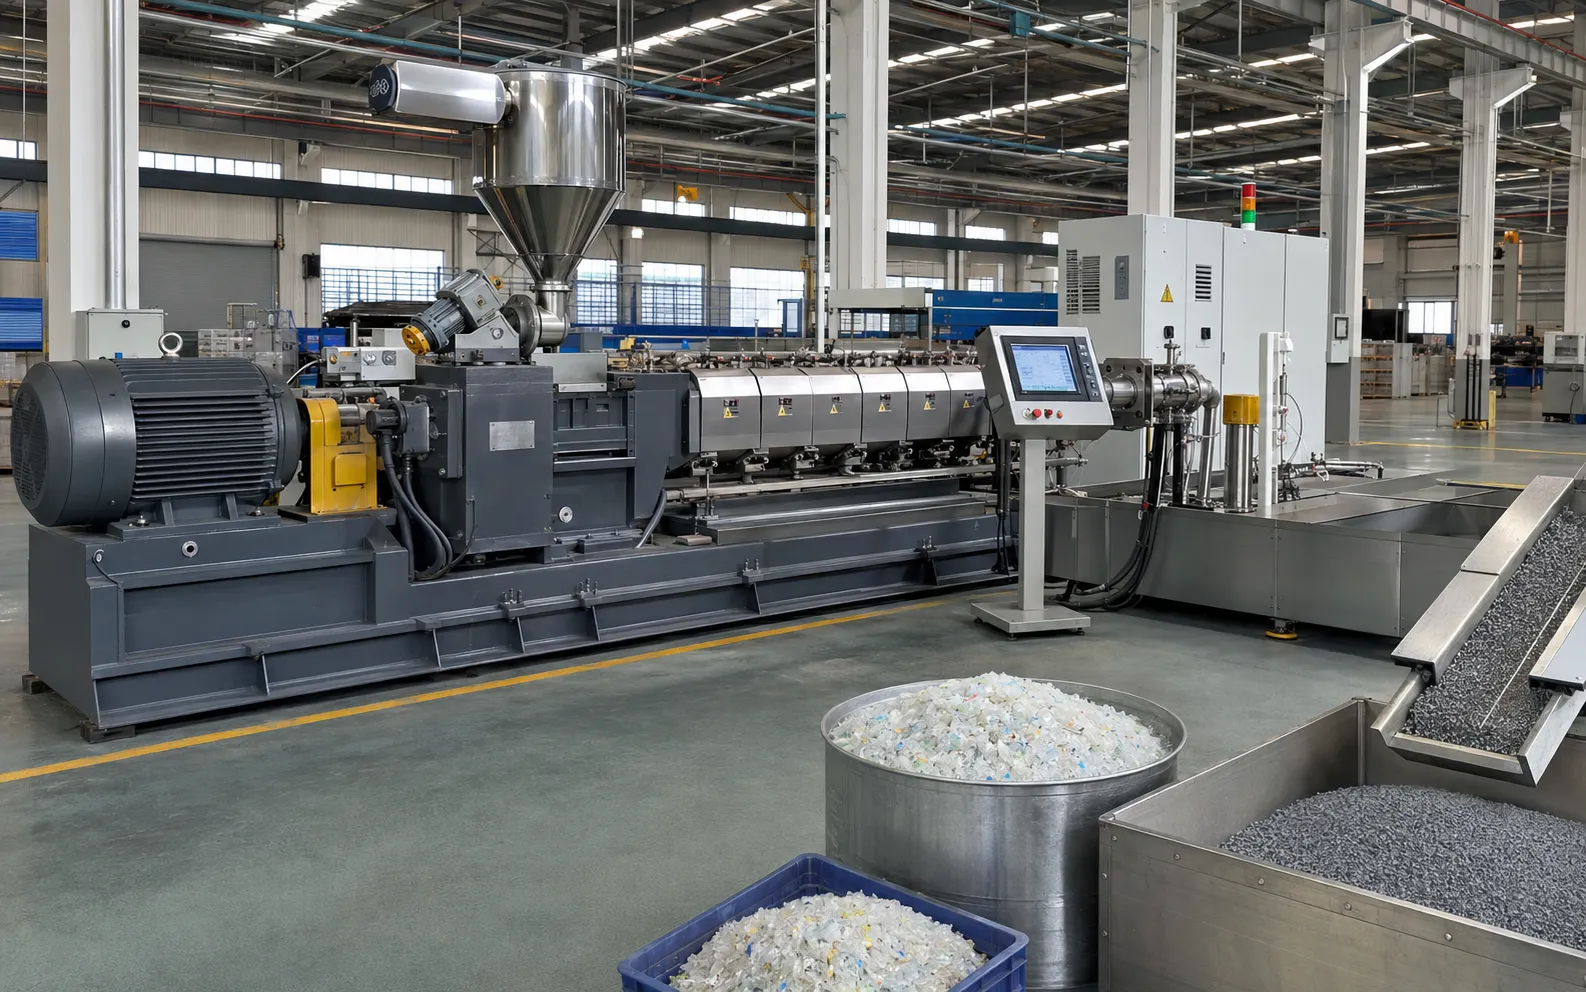
Real recycling material is dirty, mixed and unpredictable. Our twin-screw lines are built for exactly that: they run around the clock on flakes with up to 35% impurities, draw 20% less power than conventional drives and hold pellet quality within ±1°C, shift after shift.
CE Certified
ISO 9001:2015
RoHS Compliant
REACH Certified
SGS Verified
20%+Energy Savings
99%+Yield Rate
±1°CTemp Precision
35%Impurity Tolerance
Product Overview
What Is a Recycled Plastic Extruder?
The short answer: it is the machine that turns plastic waste back into usable raw material. The longer answer is below.
In Plain Terms
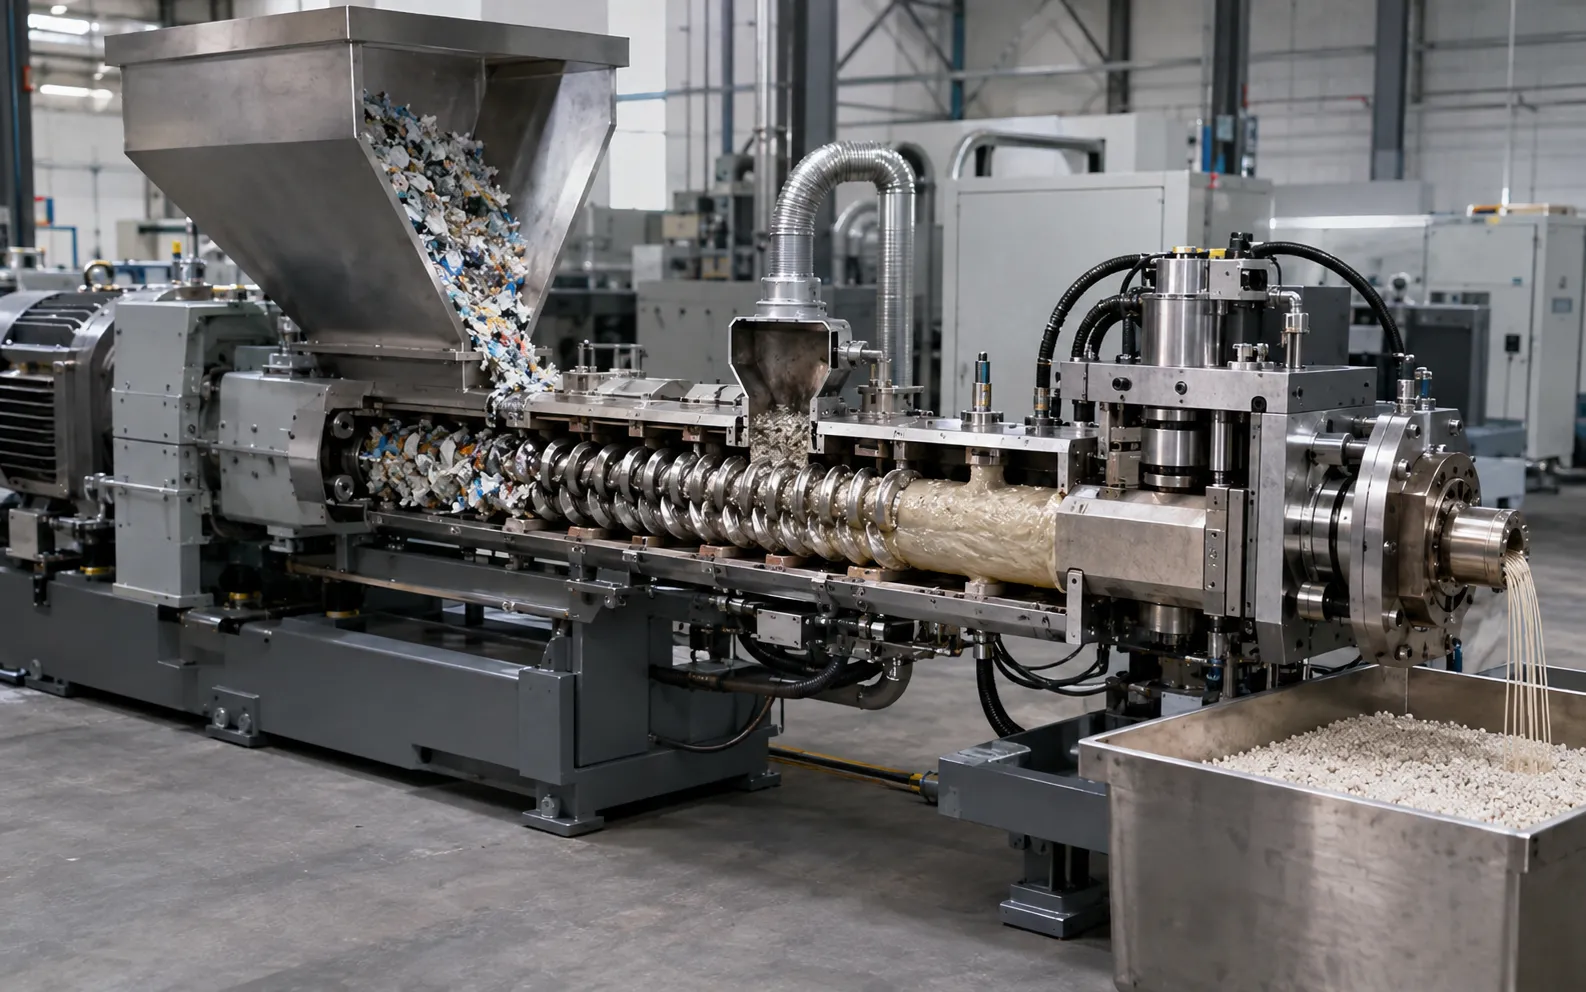
A recycled plastic extruder sits at the heart of a pelletizing line. It takes shredded plastic waste (bottles, film, pipe offcuts, factory scrap), melts it, filters out whatever does not belong, and pushes the clean melt through a die so it can be cut into pellets that manufacturers buy and use again.
Recycling is harder than running virgin resin. The feedstock is uneven, often damp, and contaminated with paper, glue and dust. A recycling extruder therefore is not a standard machine with a new nameplate: it needs a tougher feeding section, vents to pull out moisture, and a melt filter you can change without stopping the line. UET machines are designed around exactly these three points.
Co-rotating twin screw
±1°C zone control
35% impurity tolerance
50–1600 kg/h
Hydraulic screen changer
How It Works, Briefly
Two intermeshing screws turn in the same direction inside a heated barrel. As the plastic travels toward the die it is compressed, sheared and melted zone by zone, while vents let steam escape and a screen changer catches solid contaminants.
- 1Feed: flakes are metered into the barrel without bridging.
- 2Melt & clean: shear melts the polymer; vents and filters remove moisture and solids.
- 3Pelletize: the die forms strands that are cooled and cut into uniform pellets.
What You Can Make
- Recycled pellets for injection & blow molding
- Modified & compounded engineering granules
- Color & additive masterbatch
- HDPE / PP / PVC pipes and profiles
- Recycled sheet, film & WPC compounds
- High-fill CaCO₃ compounds for packaging
Core Solutions
Recycled Plastic Extruder Solutions for Processing Challenges
What recycling plants actually struggle with, and how our machines answer it.
Runs Dirty Feedstock
Paper labels, glue, dust and moisture are daily reality in regrind. Wear-resistant screws plus a hydraulic screen changer keep the line running while ordinary machines stop to clean screens.
Cuts the Power Bill
A variable-frequency drive and insulated barrel heating cut power draw by 20% or more. On a line running 6,000 hours a year, that is often the difference between profit and loss.
Same Pellets at 8 a.m. and 8 p.m.
±1°C zone control and even shear keep melt viscosity stable all shift long, so your customers receive one specification, not a range.
Passes EU / US Compliance
Vents and filtration hold VOC emissions below RoHS and REACH limits, so the pellets you sell enter regulated supply chains without extra paperwork.
Switches Materials Without Drama
PP today, ABS tomorrow, a high-fill blend next week. Stored recipes and a configurable screw layout turn changeovers into hours, not days.
180+ Days Between Stops
Wear-resistant alloy screws and barrels, filters that swap in minutes, and spare parts we keep in stock. Most customers run half a year between planned maintenance stops.
Product Line
Recycled Plastic Extruder Configurations
Three configurations cover most recycling tasks. Not sure which one fits? Send us your material list and we will recommend one.
Standard Configuration
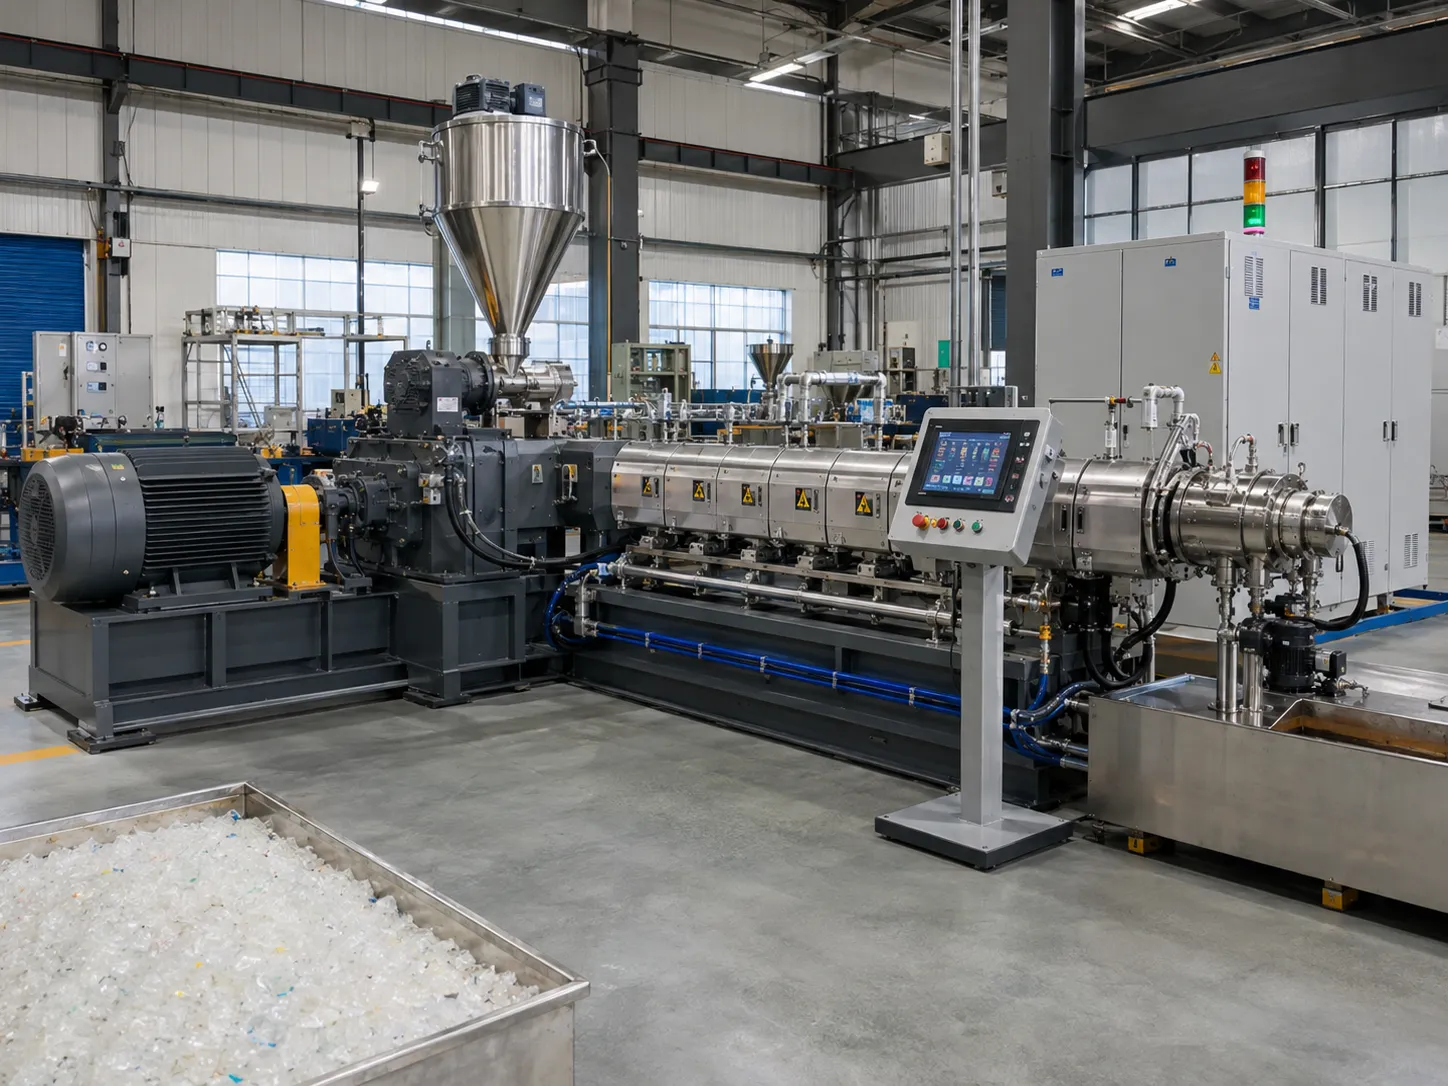
Energy-Saving Precision Extruder
Our most-ordered line for clean to medium regrind. The VFD drive and ±1°C control keep the pellet spec tight while the power meter stays quiet.
- PLC touch screen, one-operator running
- 20% lower energy than fixed-speed drives
- Front-access design for fast screen changes
High Capacity
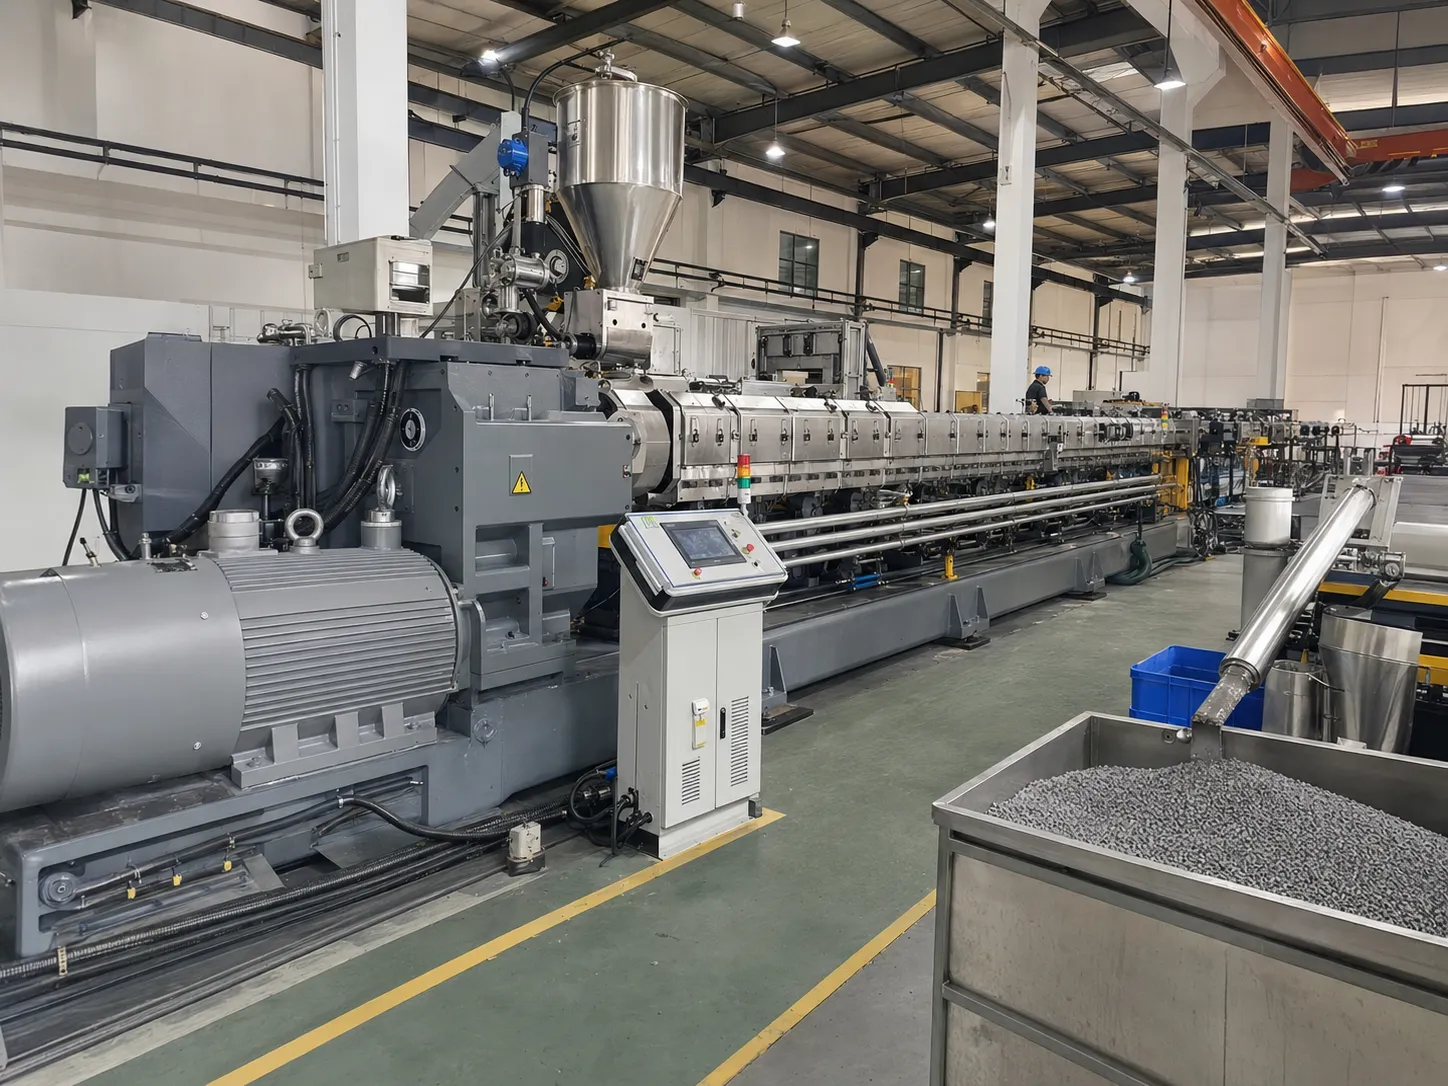
High-Capacity Smart Extruder
For plants moving 500 to 2,000 kg per hour. Twelve stored recipes let an operator switch material without re-tuning the line by hand.
- 500–2000 kg/h adjustable output
- Recipe recall in seconds
- Built for three-shift operation
Versatile
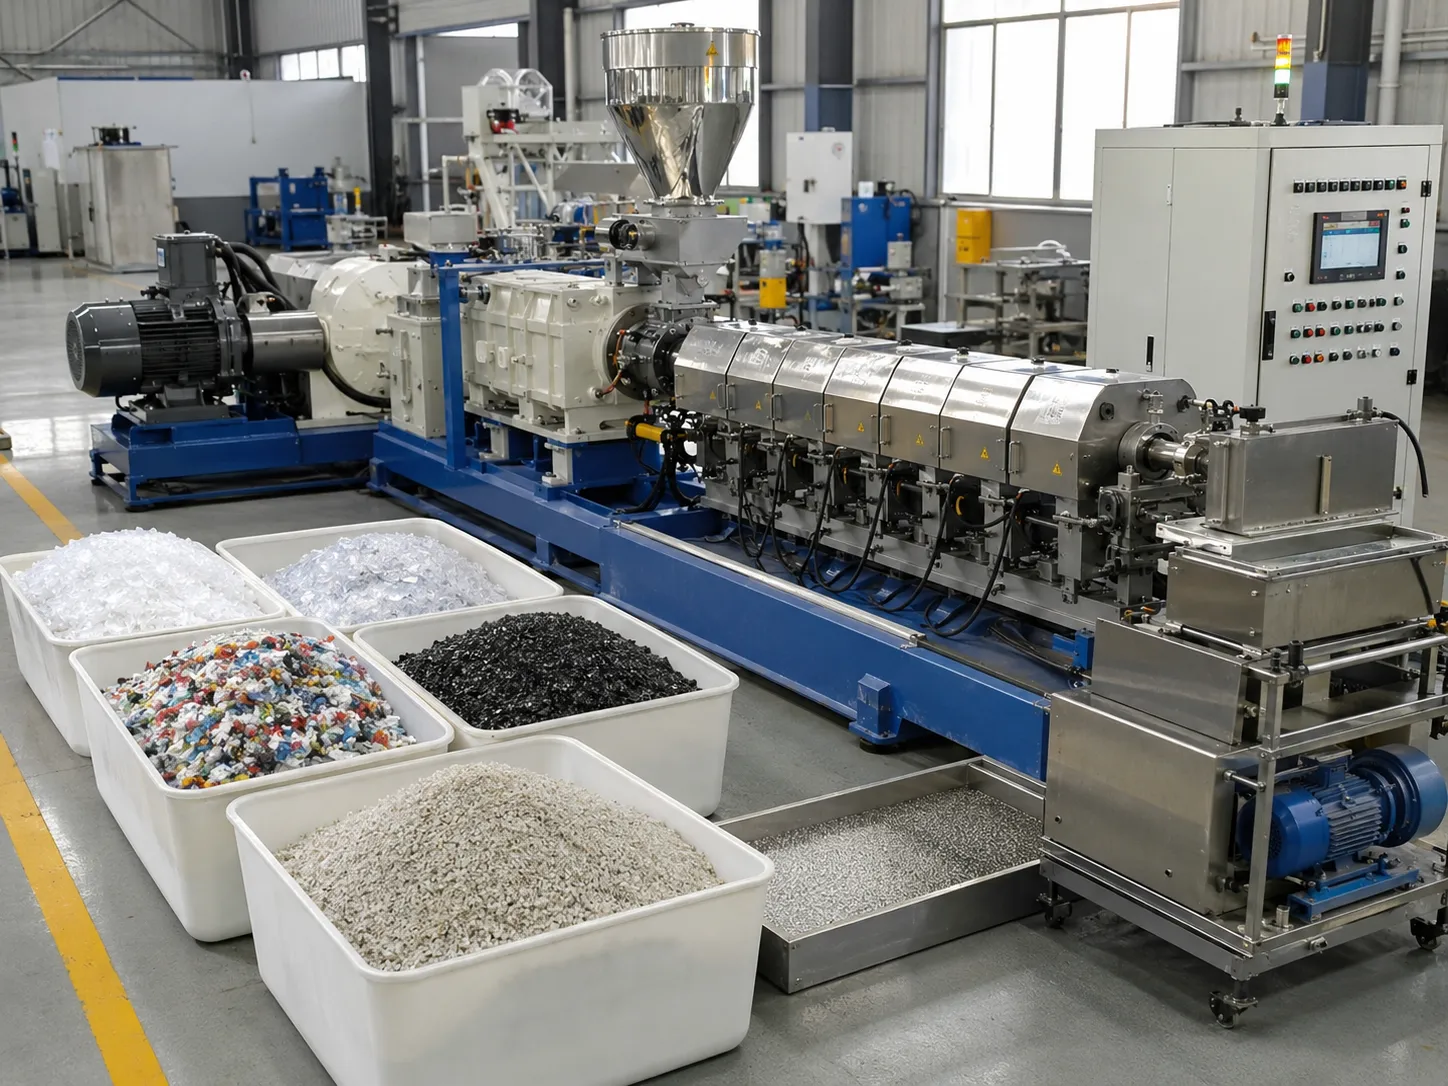
Multi-Material Compatible Extruder
The choice for toll recyclers who never know what arrives next week. Six-plus polymer families, ten preset programs, corrosion-resistant barrel.
- PP, PE, ABS, PS and high-fill blends
- 10+ preset switching programs
- Corrosion-resistant barrel lining
Technical Data
Recycled Plastic Extruder Specifications
Numbers first, adjectives later. These are the figures buyers check before asking for a quotation.
General Specifications
Material CompatibilityPP / PE / ABS / PS + High-Fill Blends
Screw ConfigurationTwin-Screw, Wear-Resistant Alloy
Automation LevelFull-Automatic, 12+ Smart Presets
CertificationCE, ISO9001:2015, RoHS
Processing Capacity600–2000 Kg/H Adjustable
Impurity ToleranceUp to 35% (Dry Materials)
Energy EfficiencyClass A (20% Saving)
Electric ComponentsSiemens / Schneider (ABB Opt.)
Control SystemPLC + 10″ Touch Screen
Transport PackageSeaworthy Crate + Pallet
Model Comparison
| Parameter | UET-25 | UET-40 | UET-55 | UET-70 | UET-85 | UET-130 |
|---|---|---|---|---|---|---|
| Screw Diameter (mm) | 25.2 | 40.8 | 55.3 | 70.2 | 85.1 | 130.4 |
| Central Distance (mm) | 20 | 34 | 46 | 58 | 72 | 108 |
| L/D Ratio | 30–55 | 30–55 | 30–55 | 30–55 | 30–55 | 28–52 |
| Main Motor (kW) | 5–7.5 | 25–50 | 80–120 | 120–200 | 170–300 | 95–170 |
| Max Speed (RPM) | 600 | 600 | 600 | 600 | 580 | 550 |
| Torque/Shaft (N.m) | 35–48 | 180–370 | 620–900 | 900–1500 | 1300–2300 | 900–1600 |
| Output (Kg/H) | 50–80 | 30–100 | 90–220 | 160–380 | 320–650 | 850–1600 |
Machine Anatomy
Key Components of the Recycled Plastic Extruder
Six core modules, in the order the material meets them. Every photo below is from our own workshop.
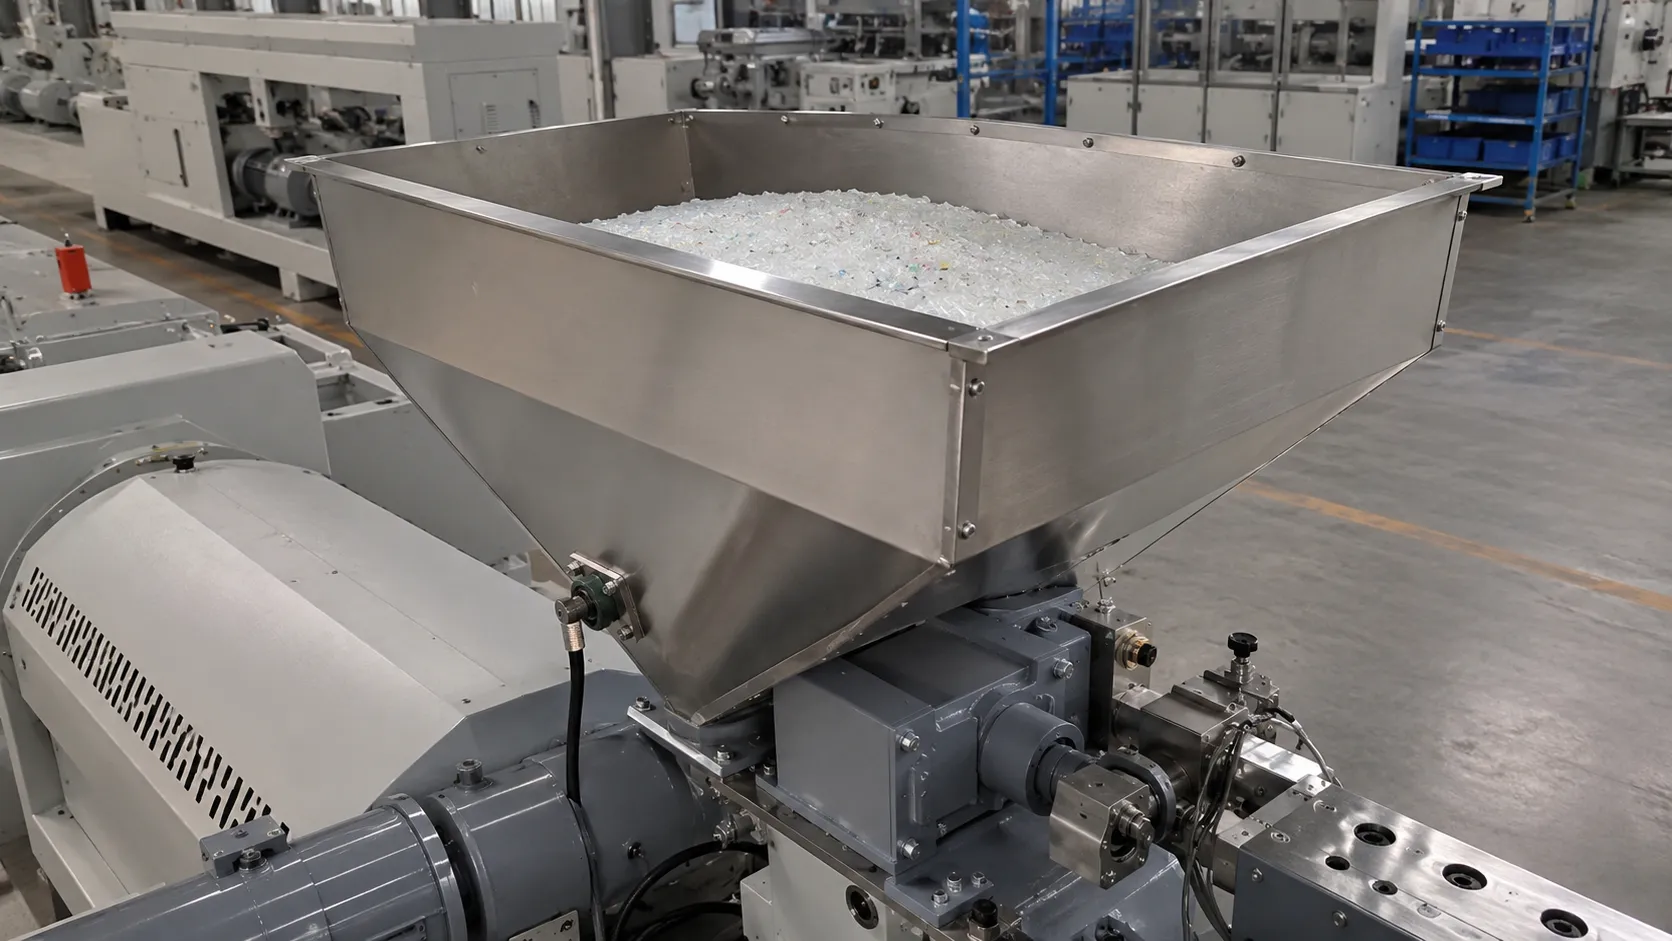
Hopper & Feeding System
Forced-feed hopper with volumetric metering. Low-density flakes and film scrap go in steadily, with no bridging and no surging.
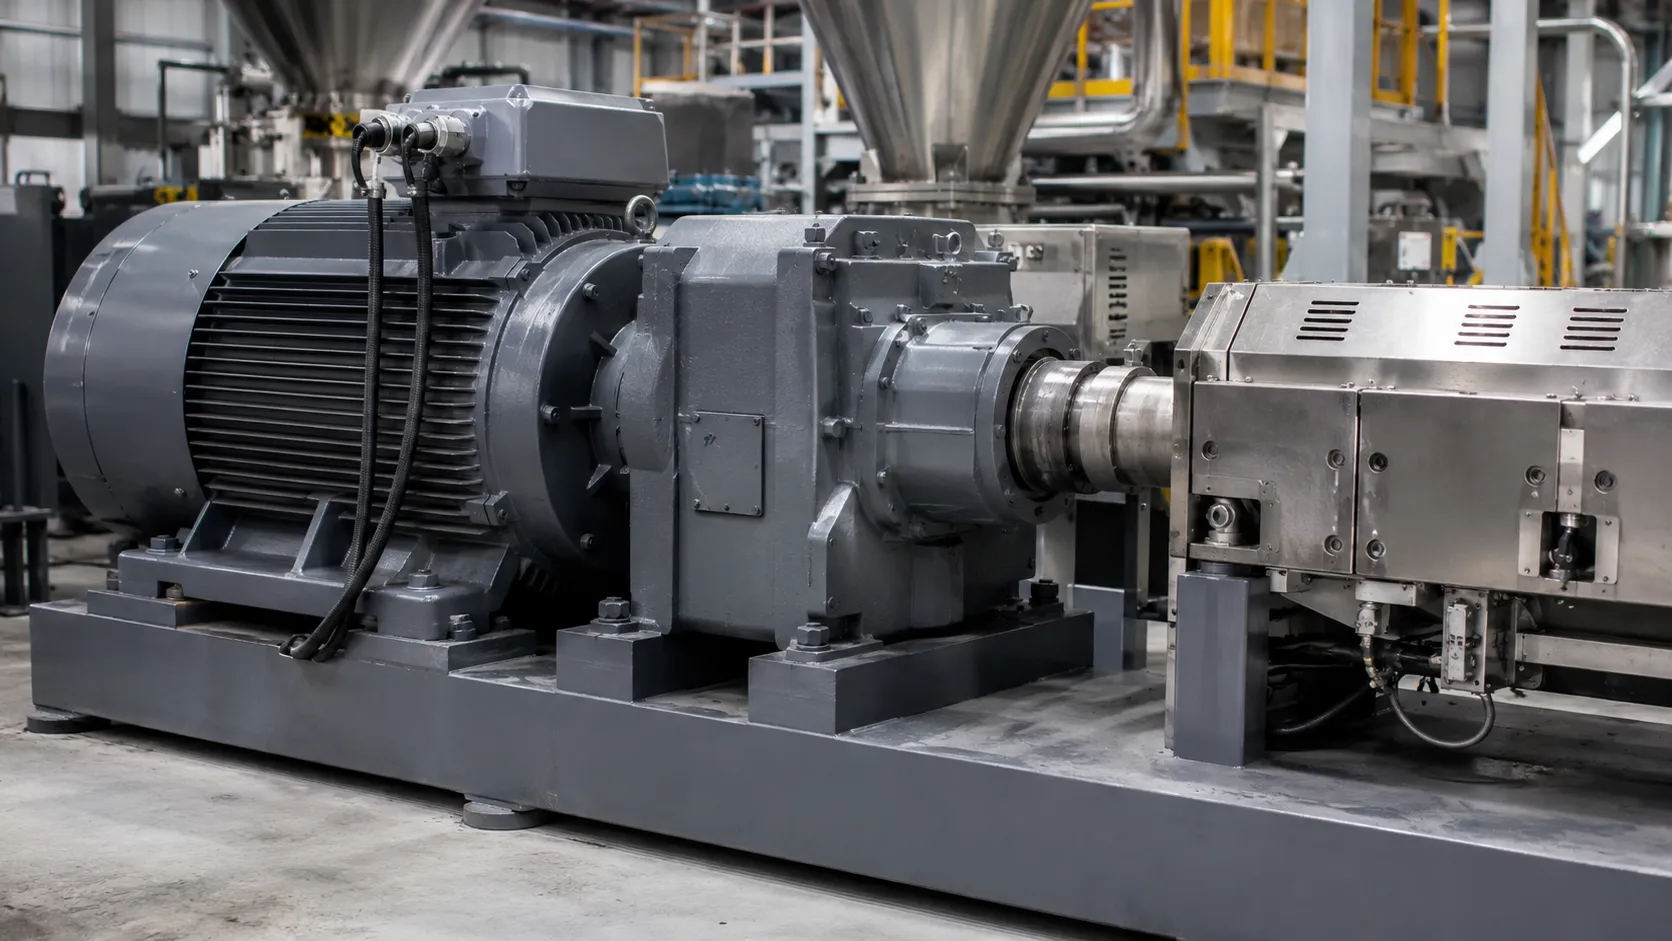
Motor & Gearbox Drive
Siemens / ABB motor with VFD, matched to a hardened helical gearbox that splits torque evenly between the screws. Rated for 20,000+ hours under load.
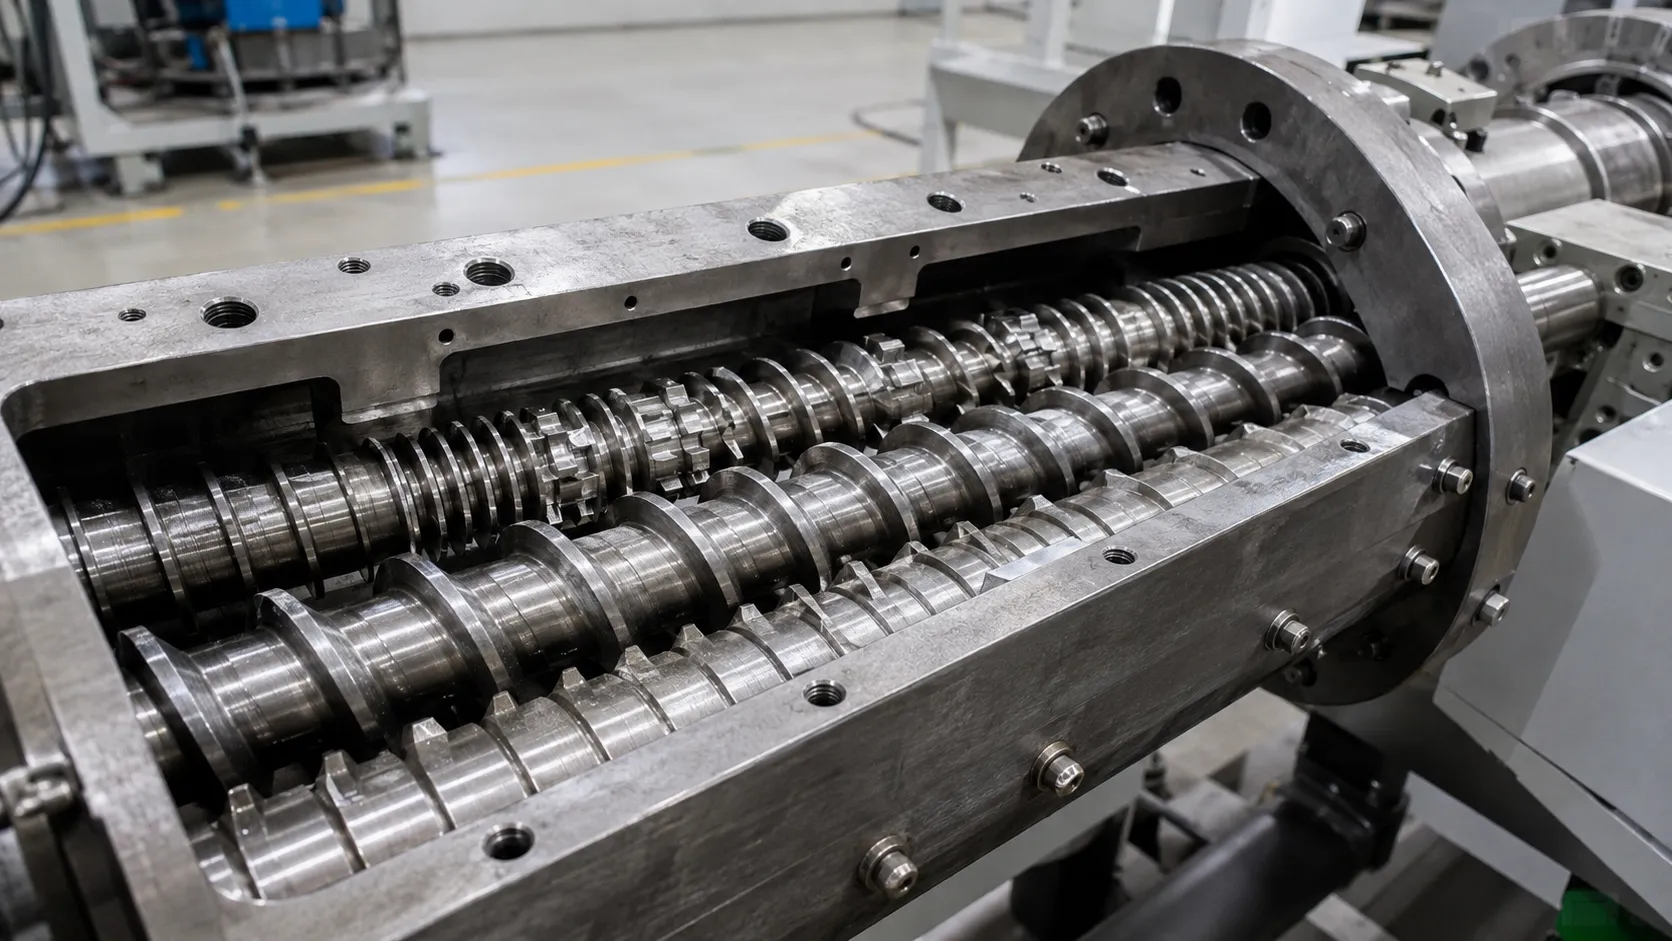
Twin Screw & Barrel
Modular co-rotating screws in wear-resistant alloy, inside a bimetallic segmented barrel. Conveying, mixing and shear zones are rearranged per recipe.
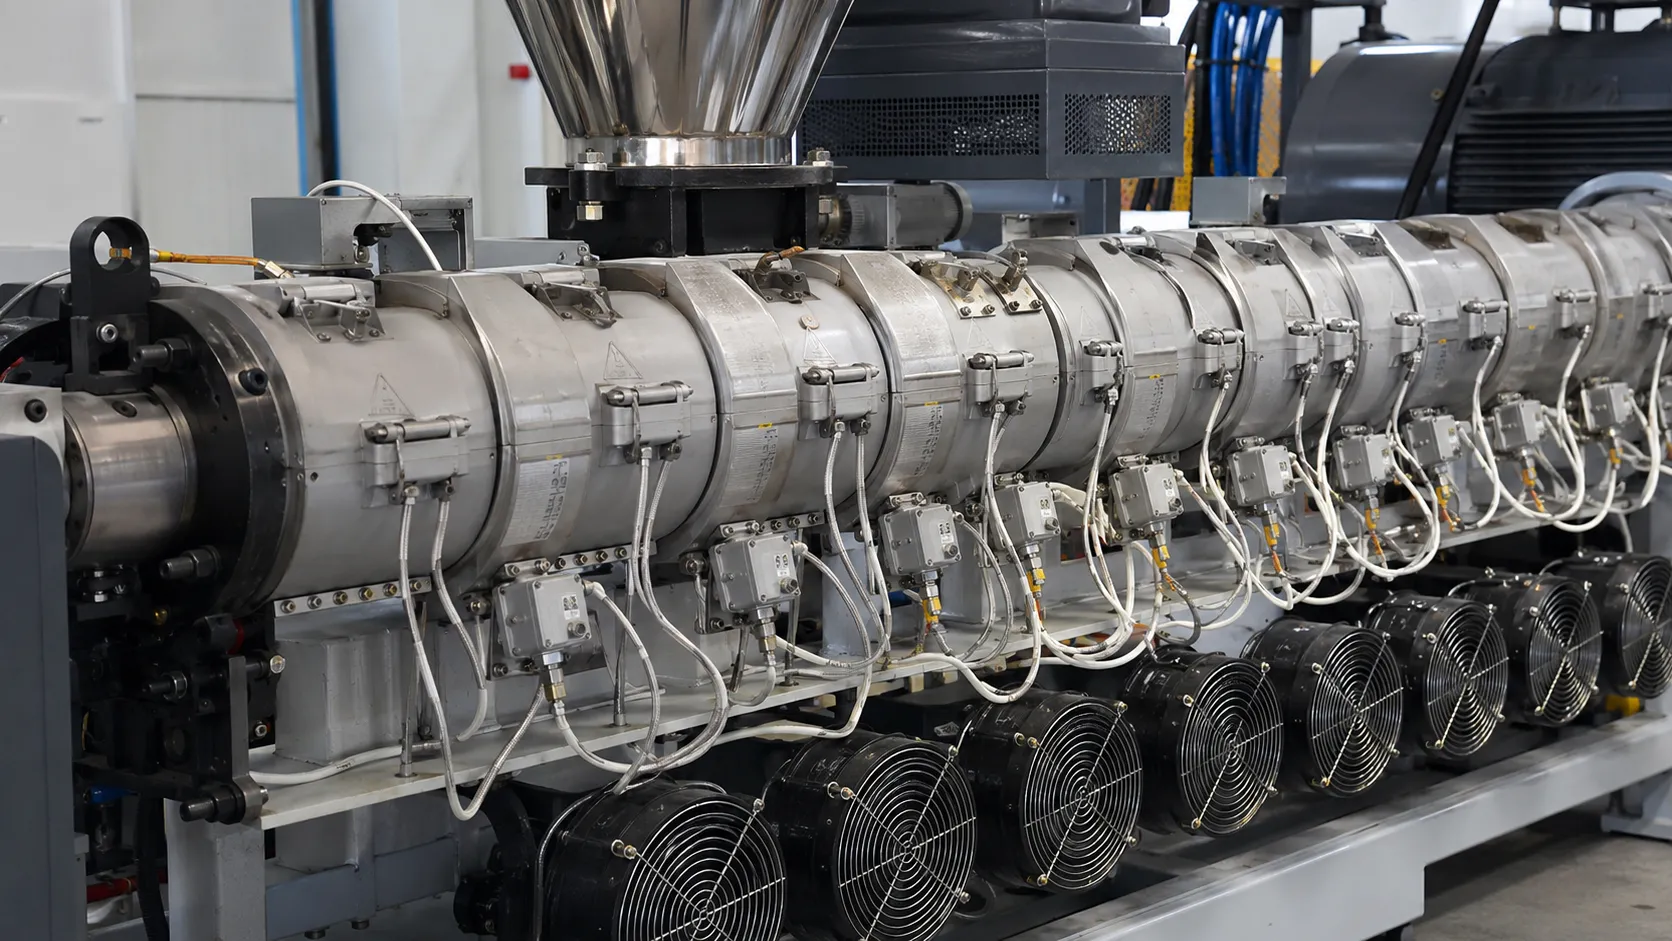
Heating & Cooling Zones
Cast-aluminum heaters with forced-air cooling on every zone, holding ±1°C so melt viscosity stays even along the whole barrel.
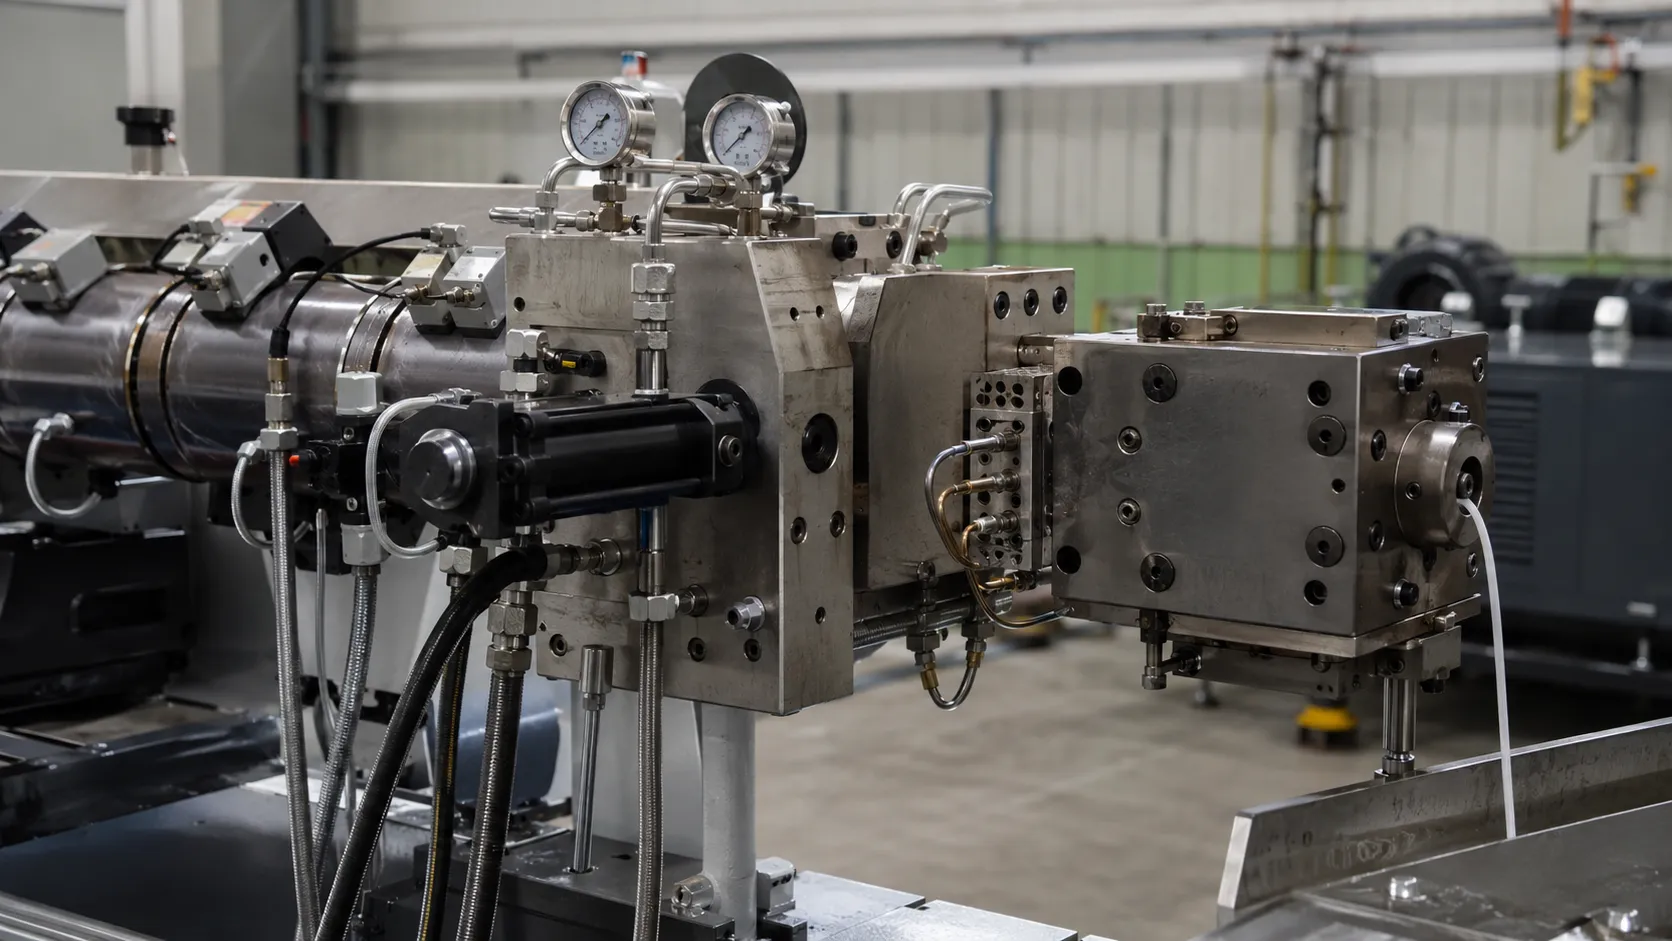
Melt Filter & Die Head
Hydraulic screen changer down to 40 mesh, swapped without stopping; hardened tool-steel die forms strands, sheets, pipes or profiles.
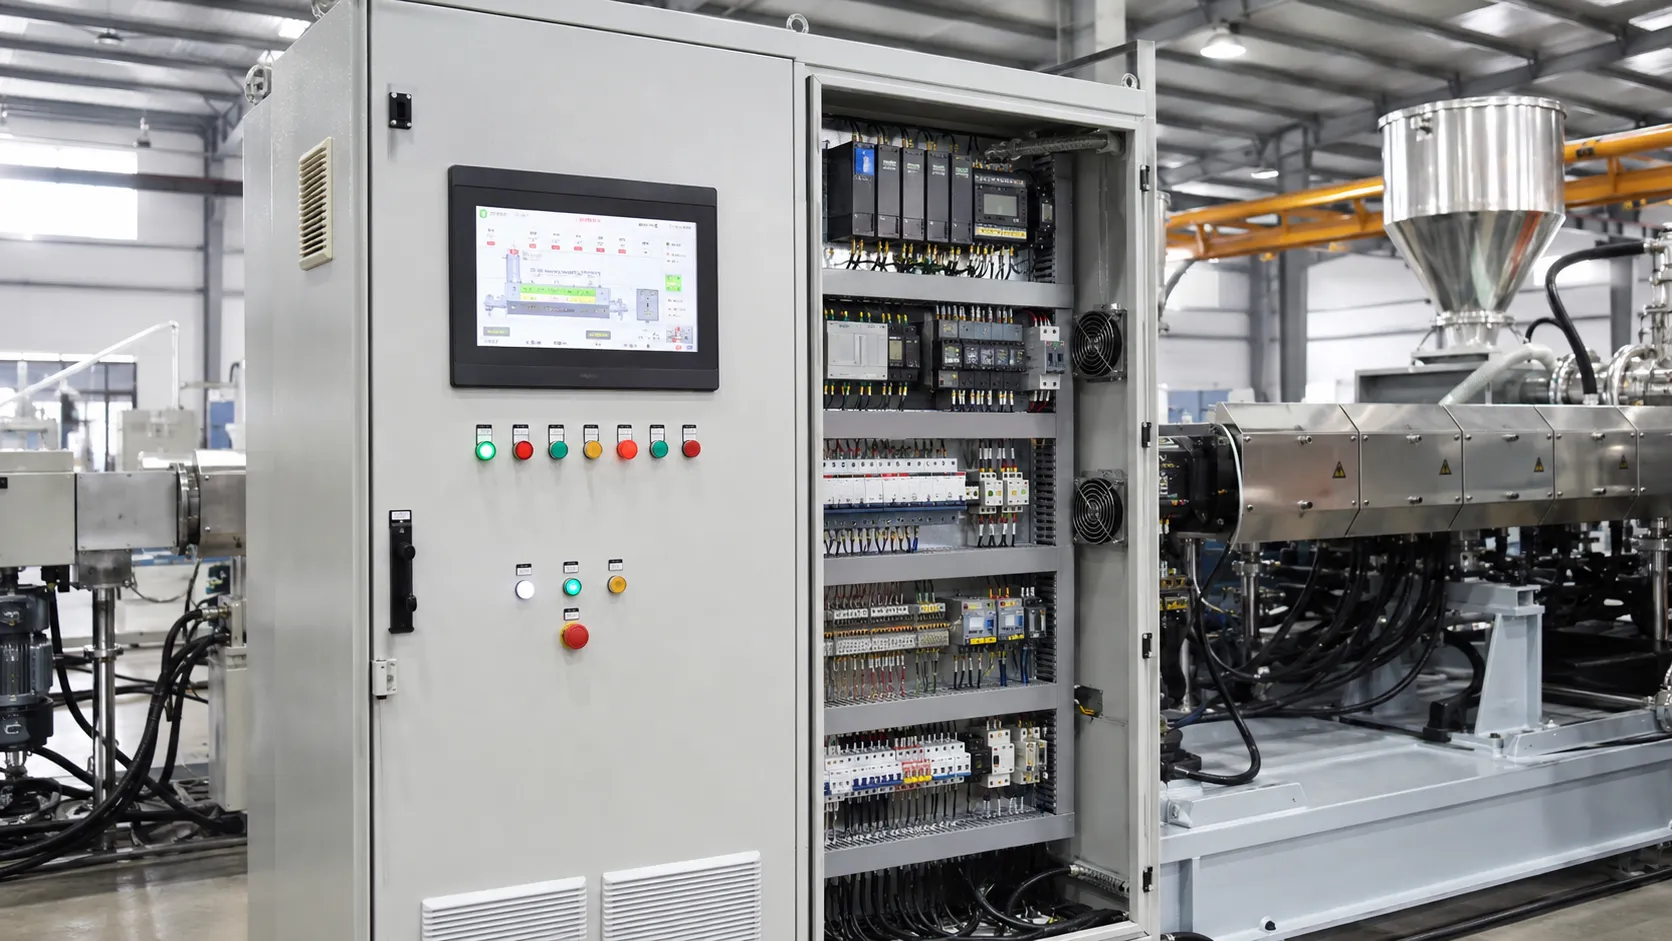
PLC Control Cabinet
10-inch touch HMI, 12+ stored recipes, live temperature, pressure and torque readouts. One operator runs the whole line.
Working Principle
How the Recycled Plastic Extruder Works: 6-Stage Process
Follow one flake through the line, from the washing floor to a bag of saleable pellets.
Step 1
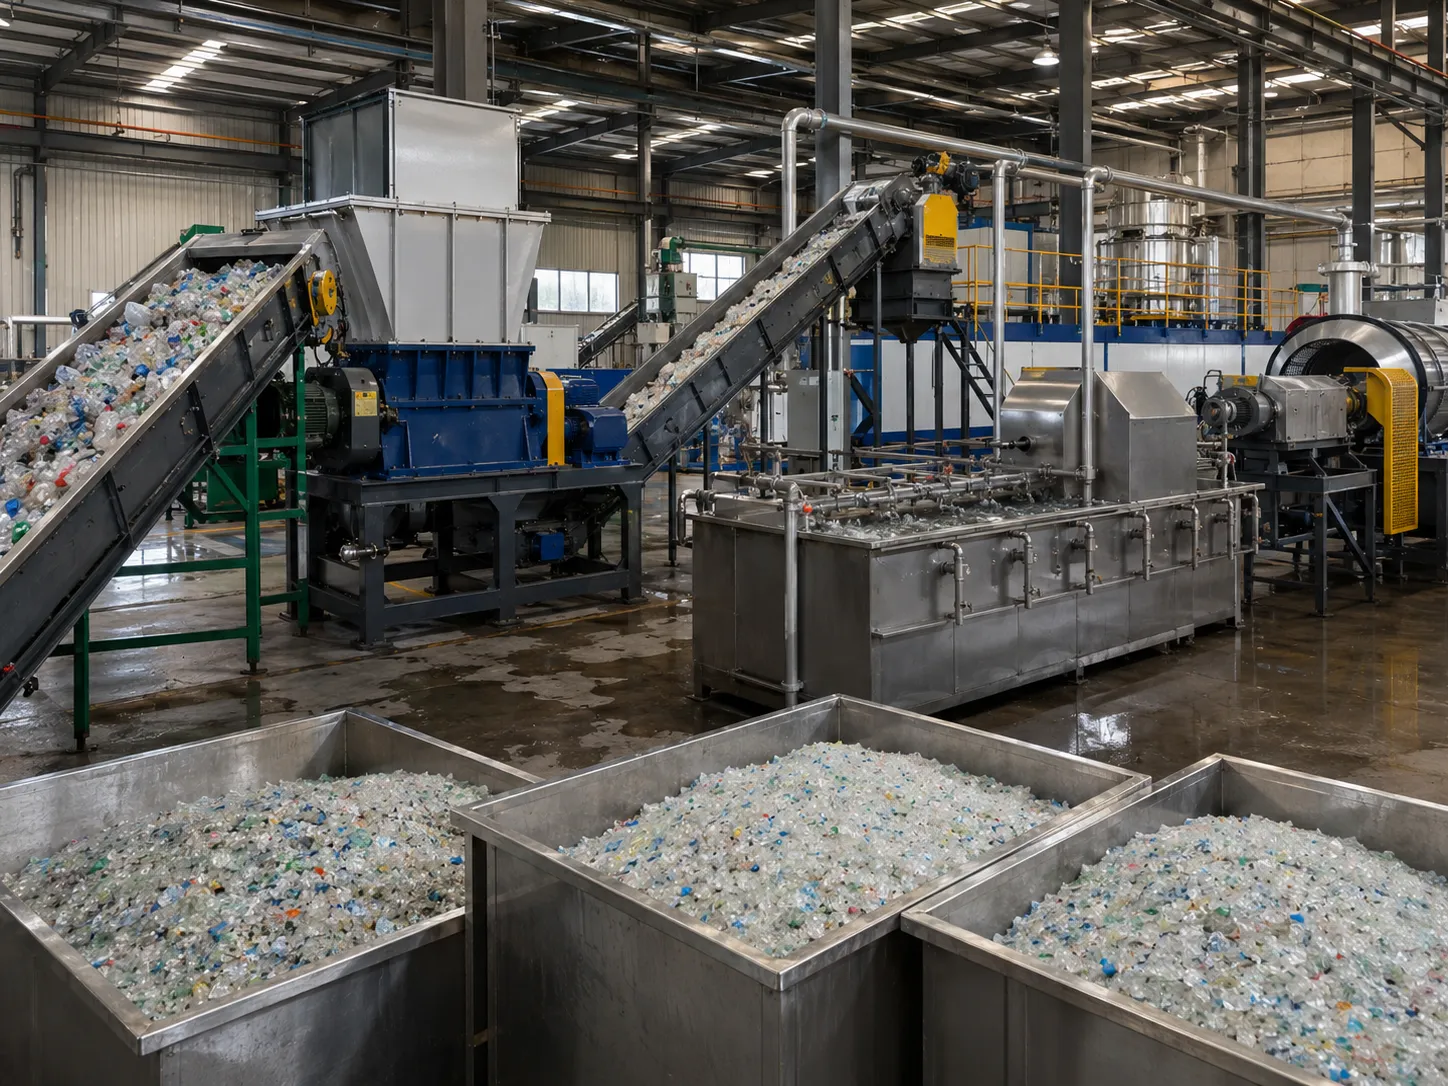
Material Preparation
Waste plastic is sorted, shredded, washed and dried. Better input here means fewer screen changes later.
Step 2
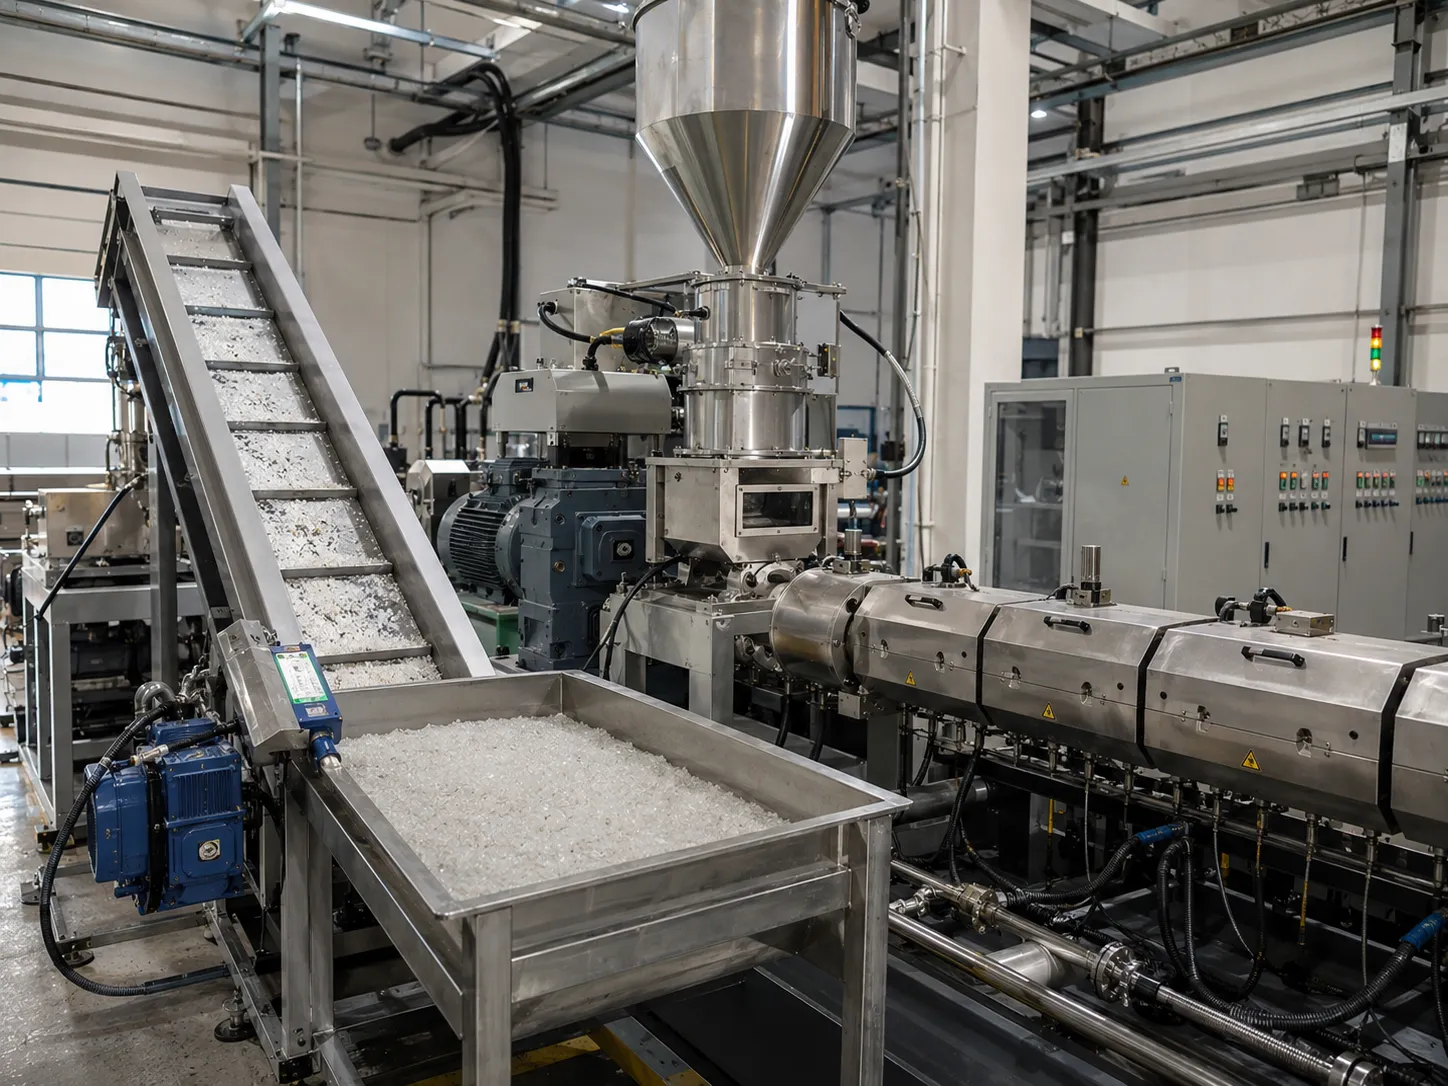
Feeding & Conveying
A metered feeder pushes flakes into the barrel at a steady rate, so the screws never starve or flood.
Step 3
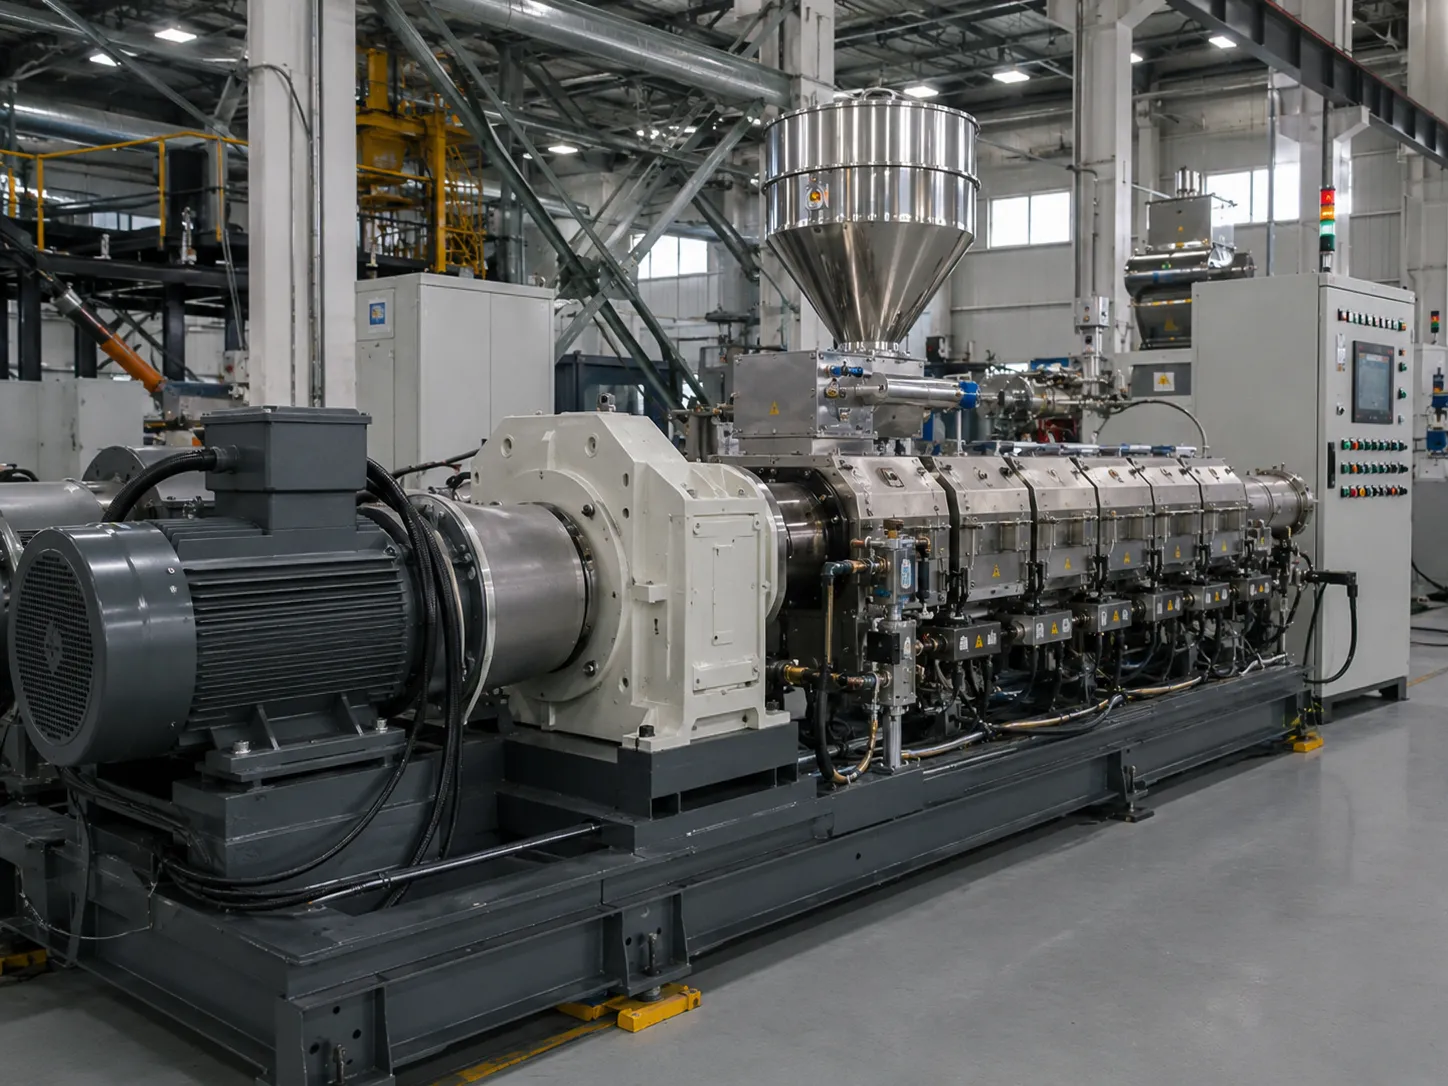
Melting & Mixing
The twin screws shear and compress the material zone by zone until it is a uniform melt.
Step 4
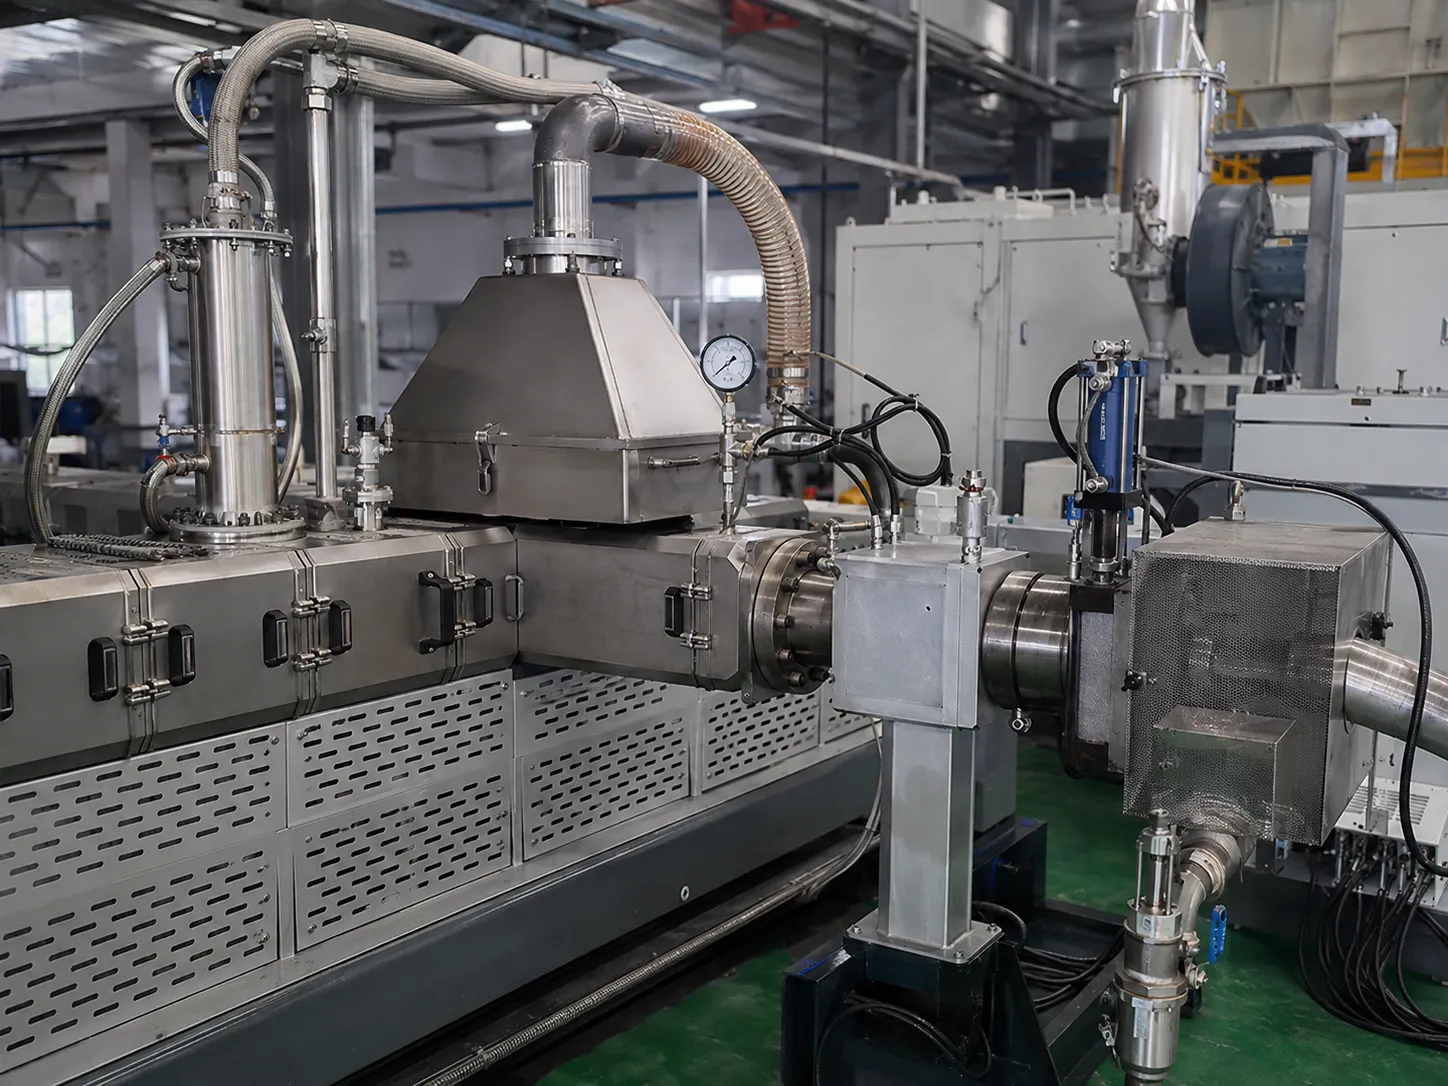
Degassing & Filtration
Vents pull out steam and volatiles; the hydraulic screen changer catches whatever solids remain.
Step 5
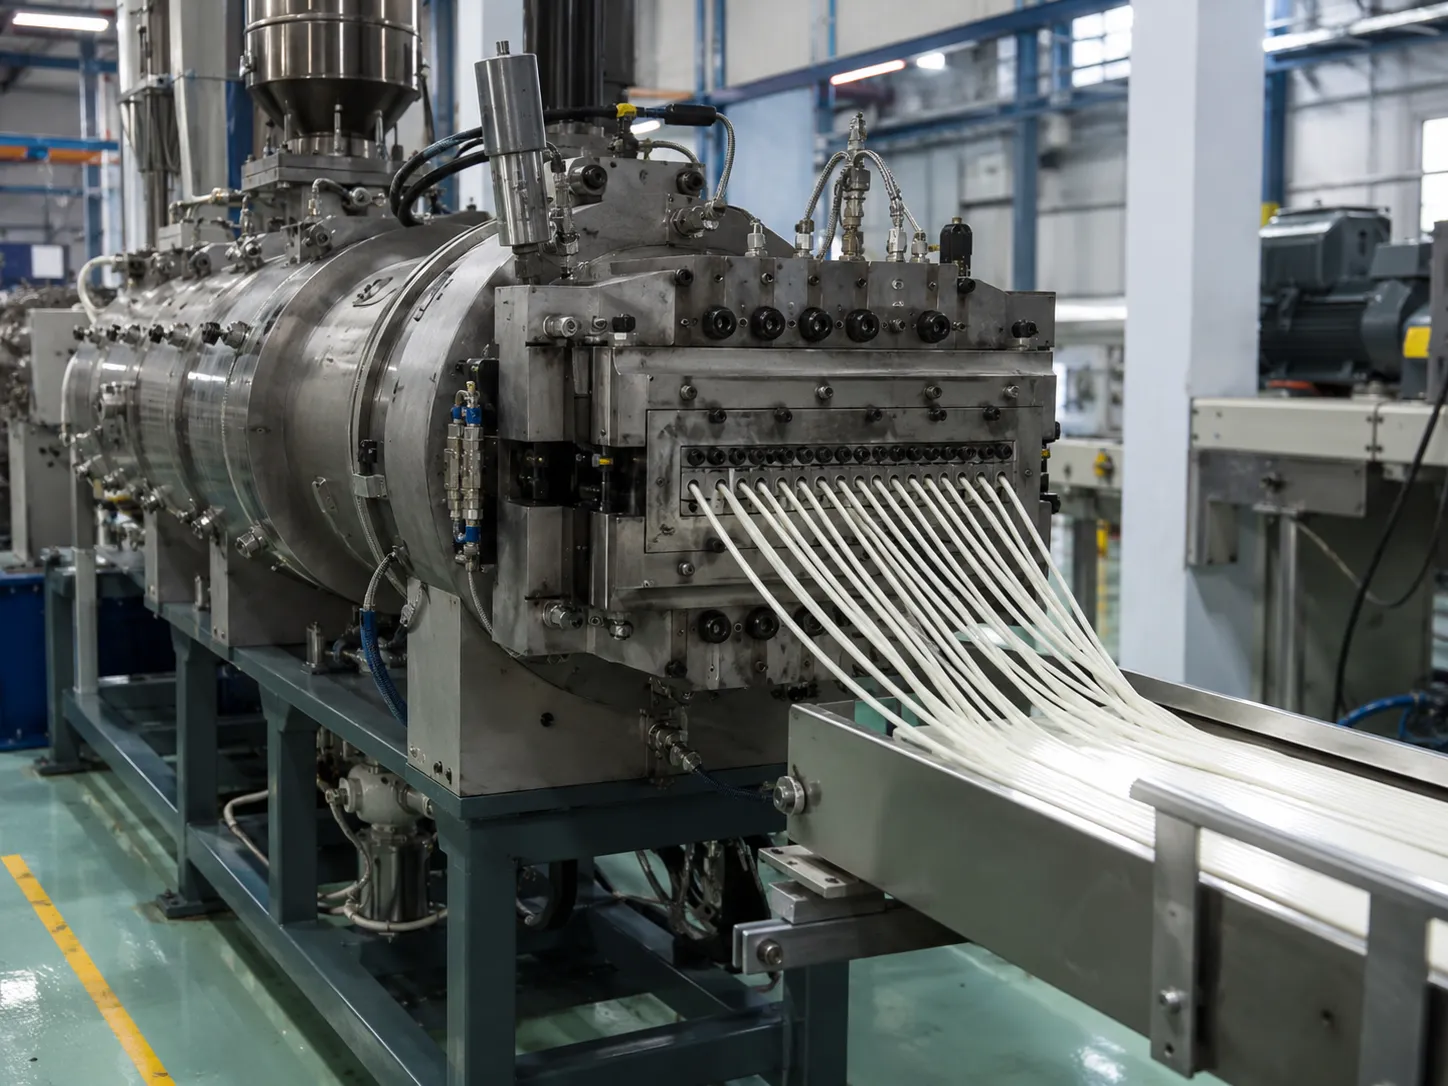
Extrusion & Shaping
The clean melt leaves the die as continuous strands, ready for the cooling tank.
Step 6
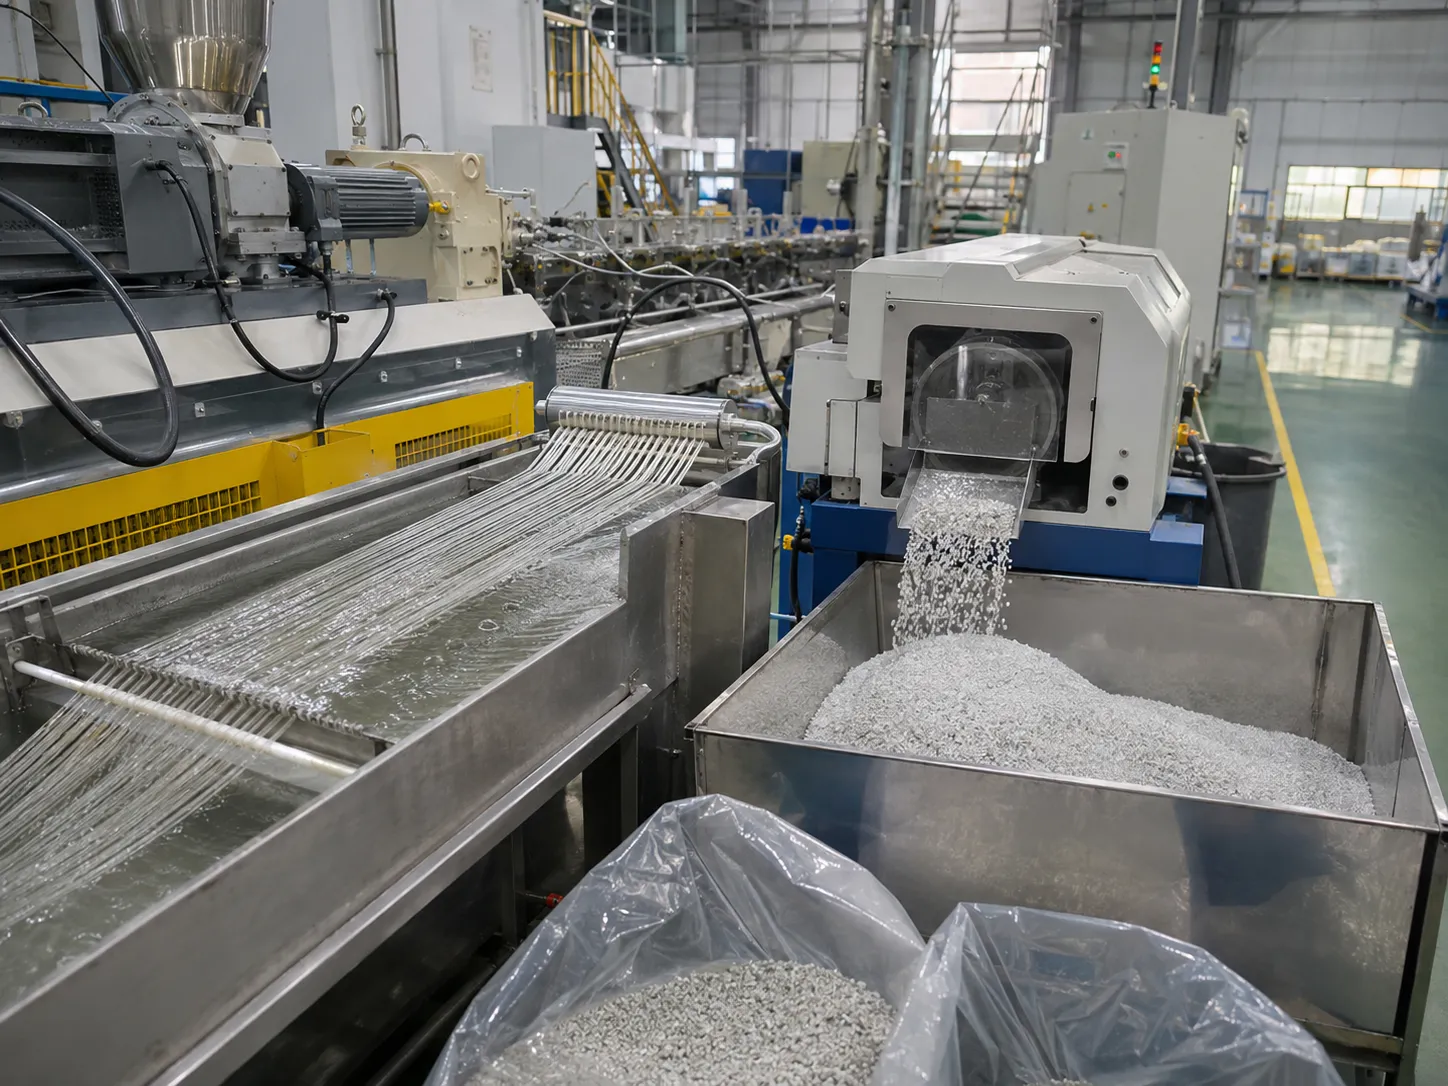
Cooling & Pelletizing
Strands are cooled, cut into even pellets, checked and packed. That bag is your product.
Applications
Recycled Plastic Extruder Applications: Materials & End Products
If it was plastic once, we can probably melt it again. These are the feedstocks our lines run every week.
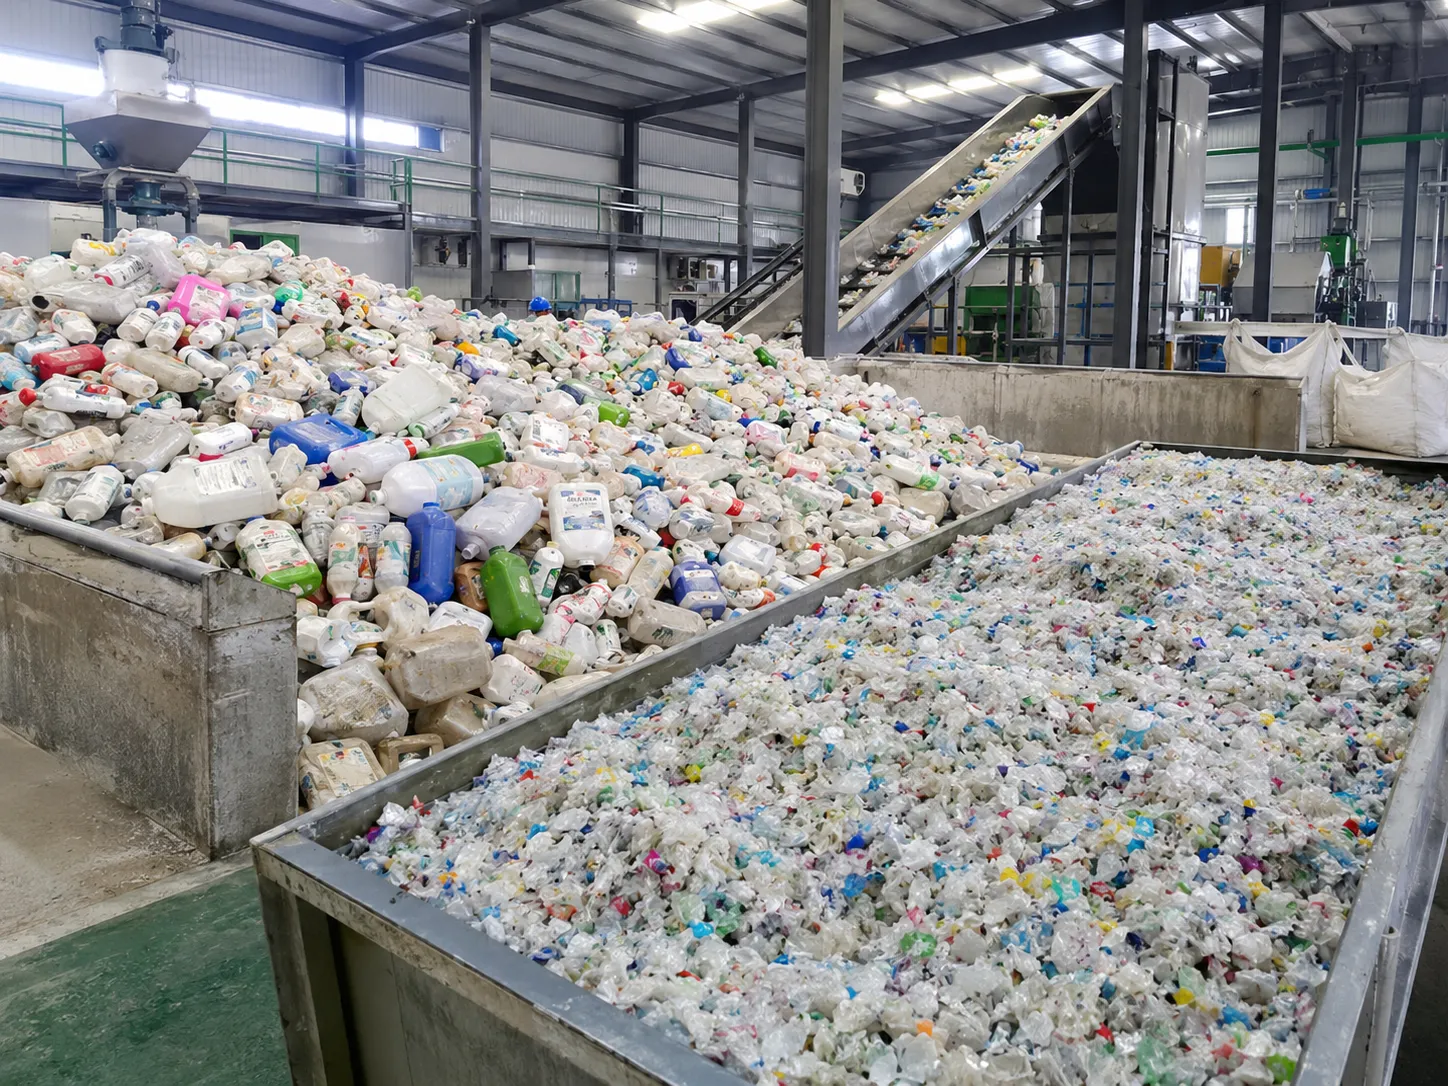
PP / PE Bottles & Flakes
Post-consumer packaging regrind
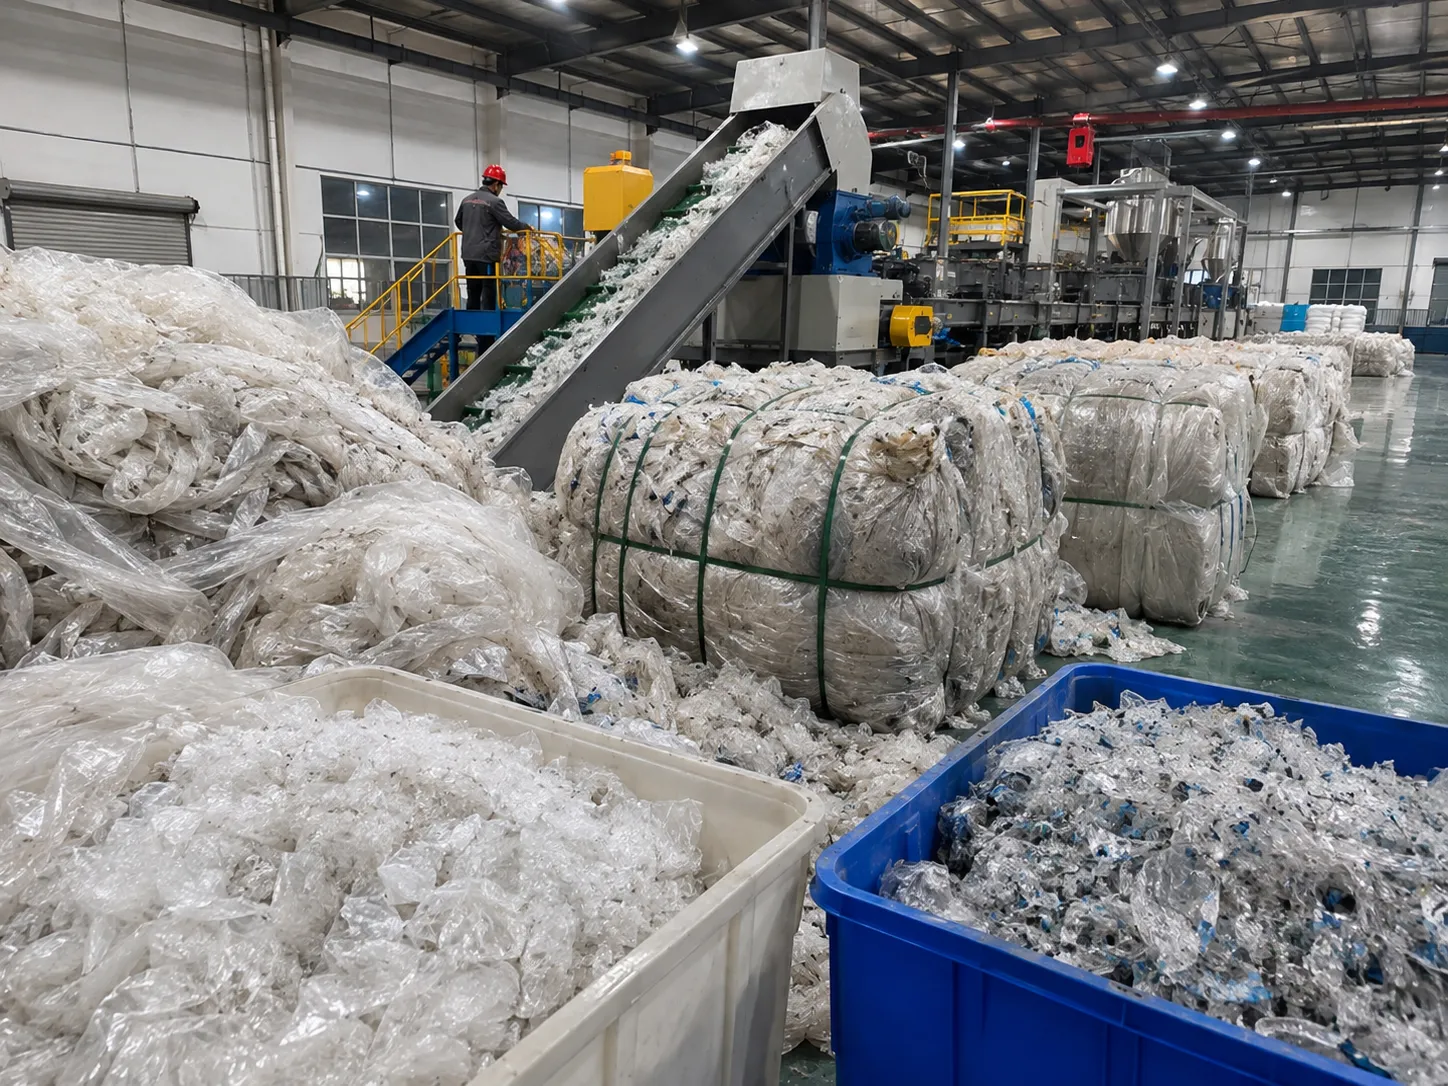
Films & Compressed Bales
Agricultural & packaging film scrap
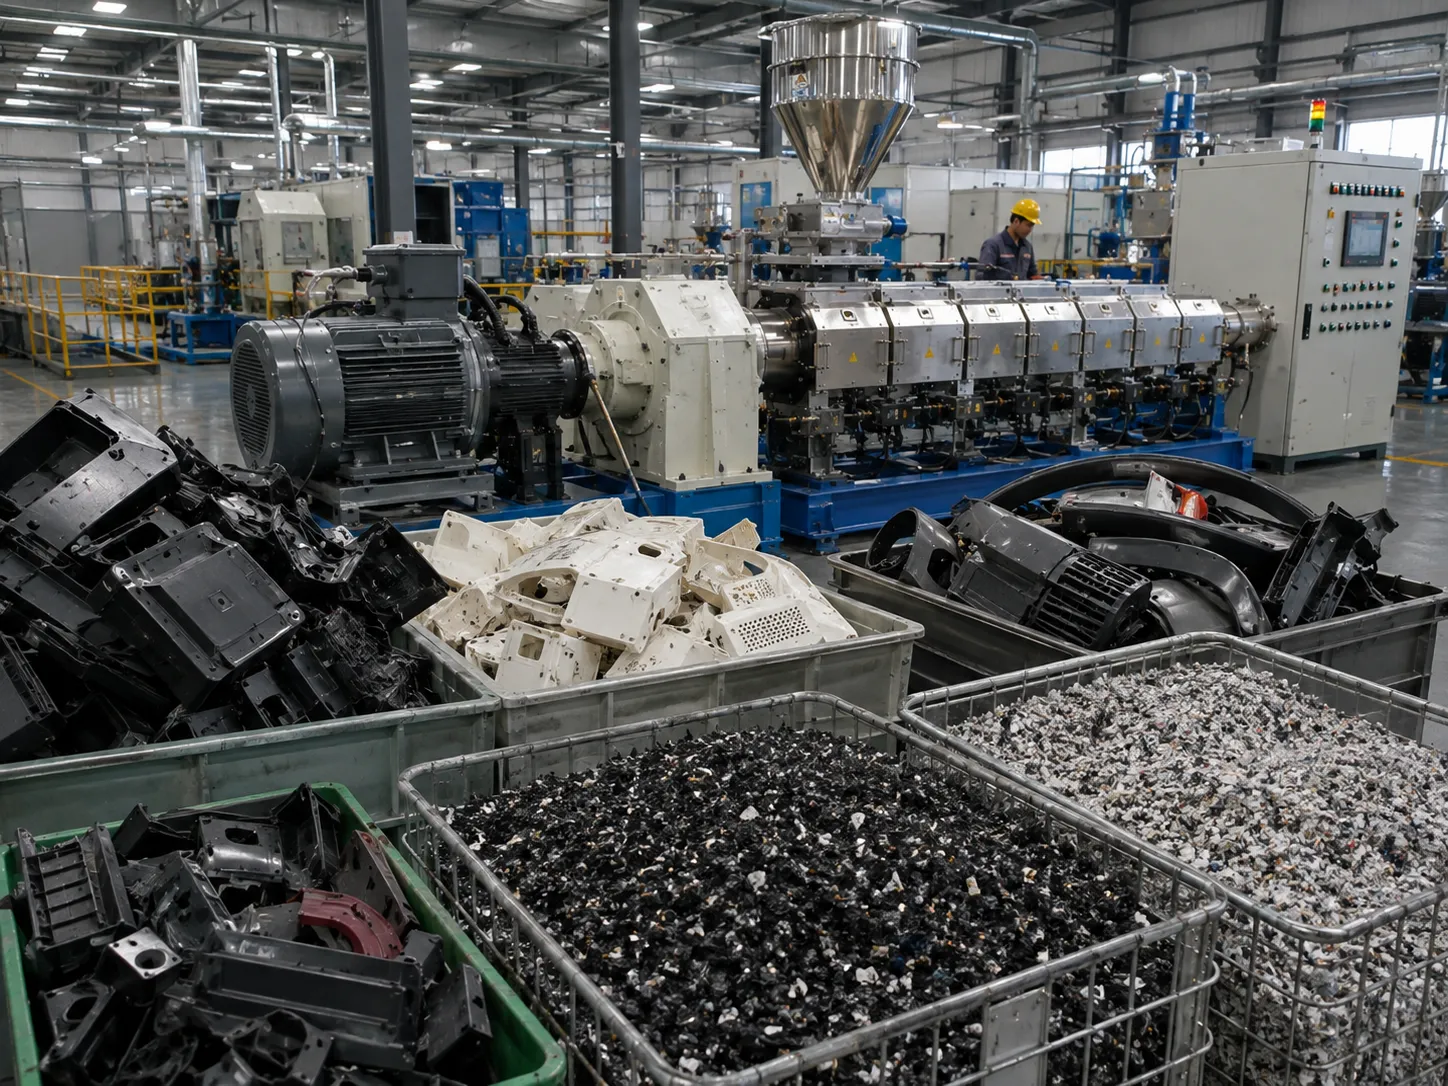
ABS & Engineering Parts
Electronics & automotive housings
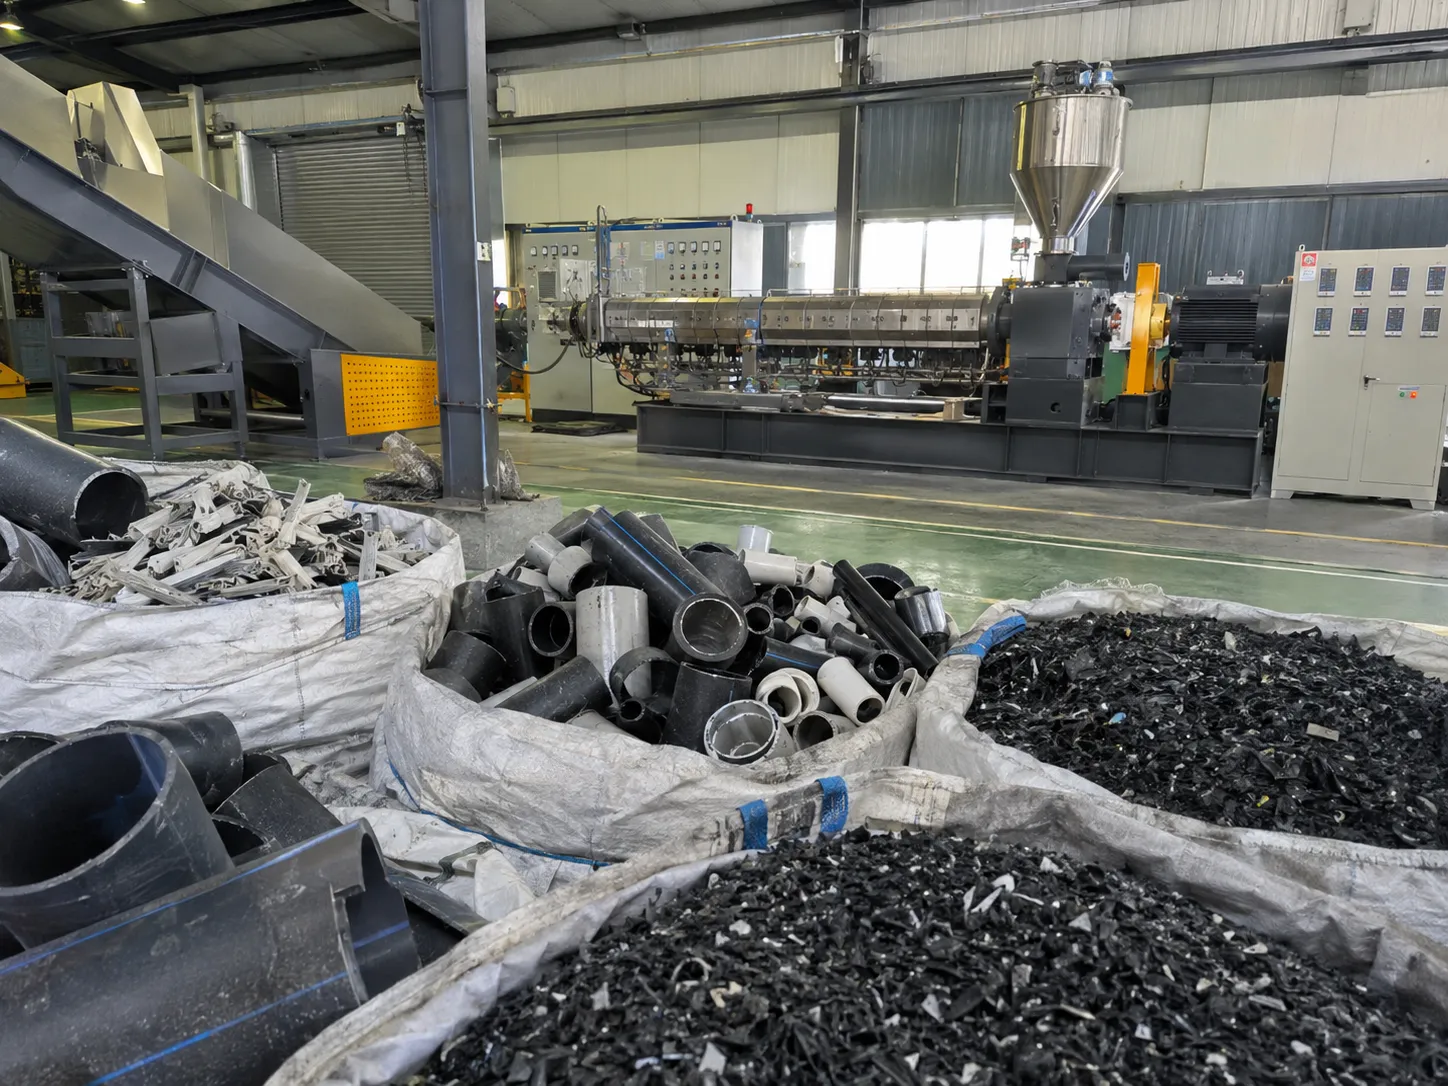
PVC / PE Pipes & Profiles
Construction pipe & fitting regrind
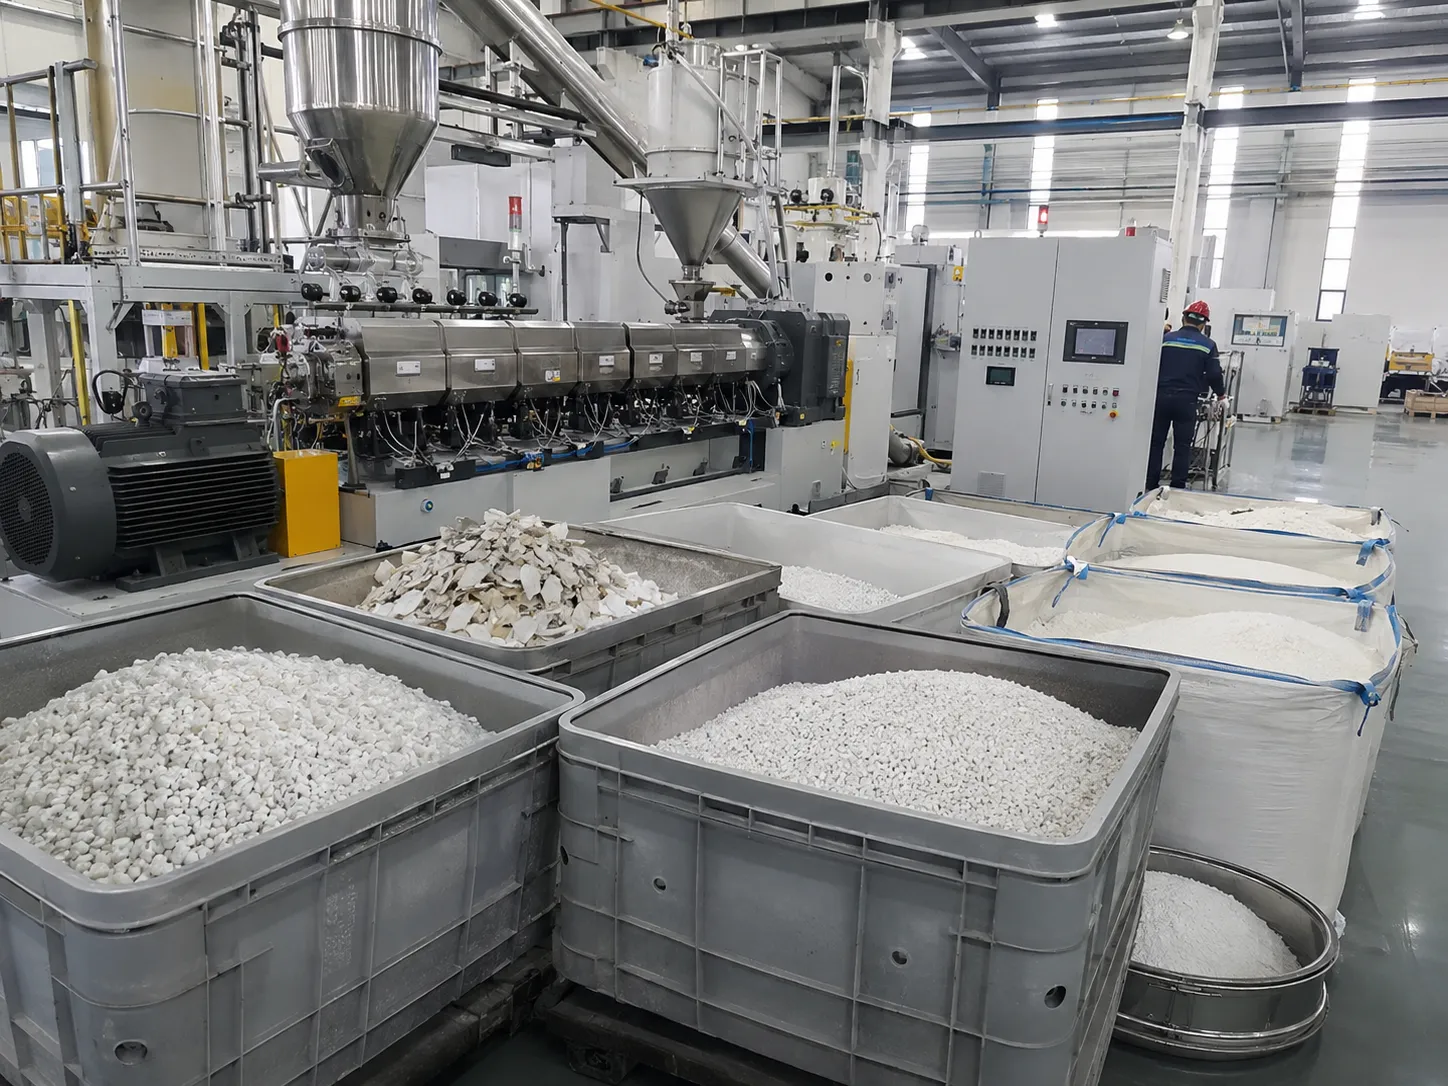
High-Fill Compounds
CaCO₃ filled & white granules
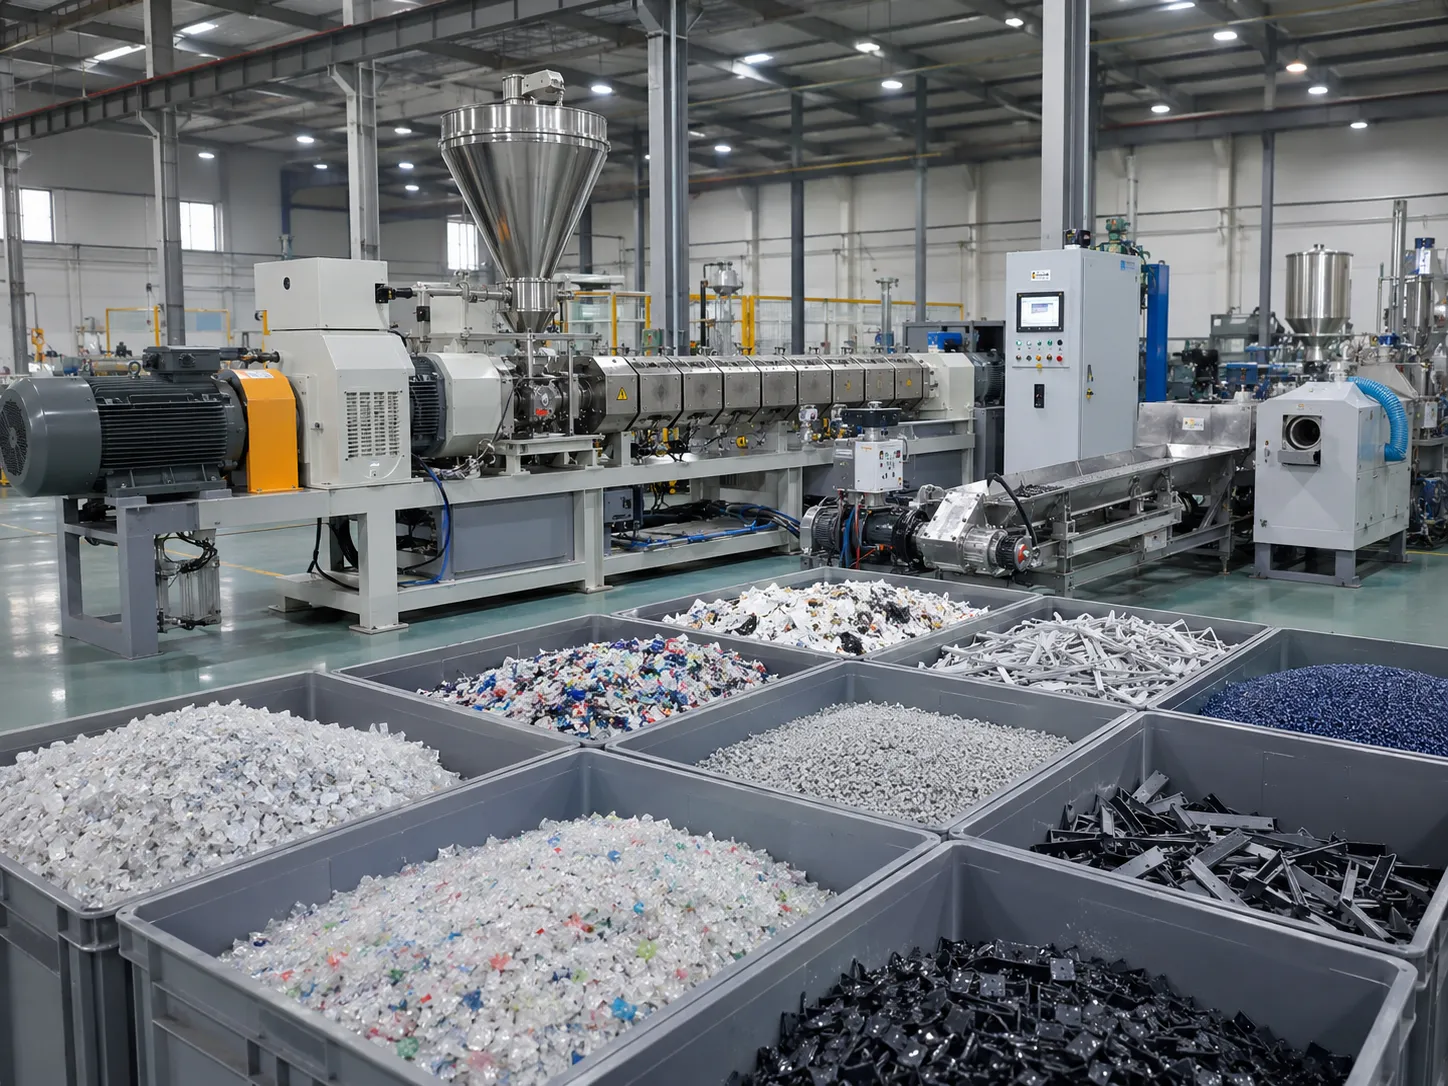
Mixed & Post-Industrial
Multi-polymer blends & factory scrap
Our Facility
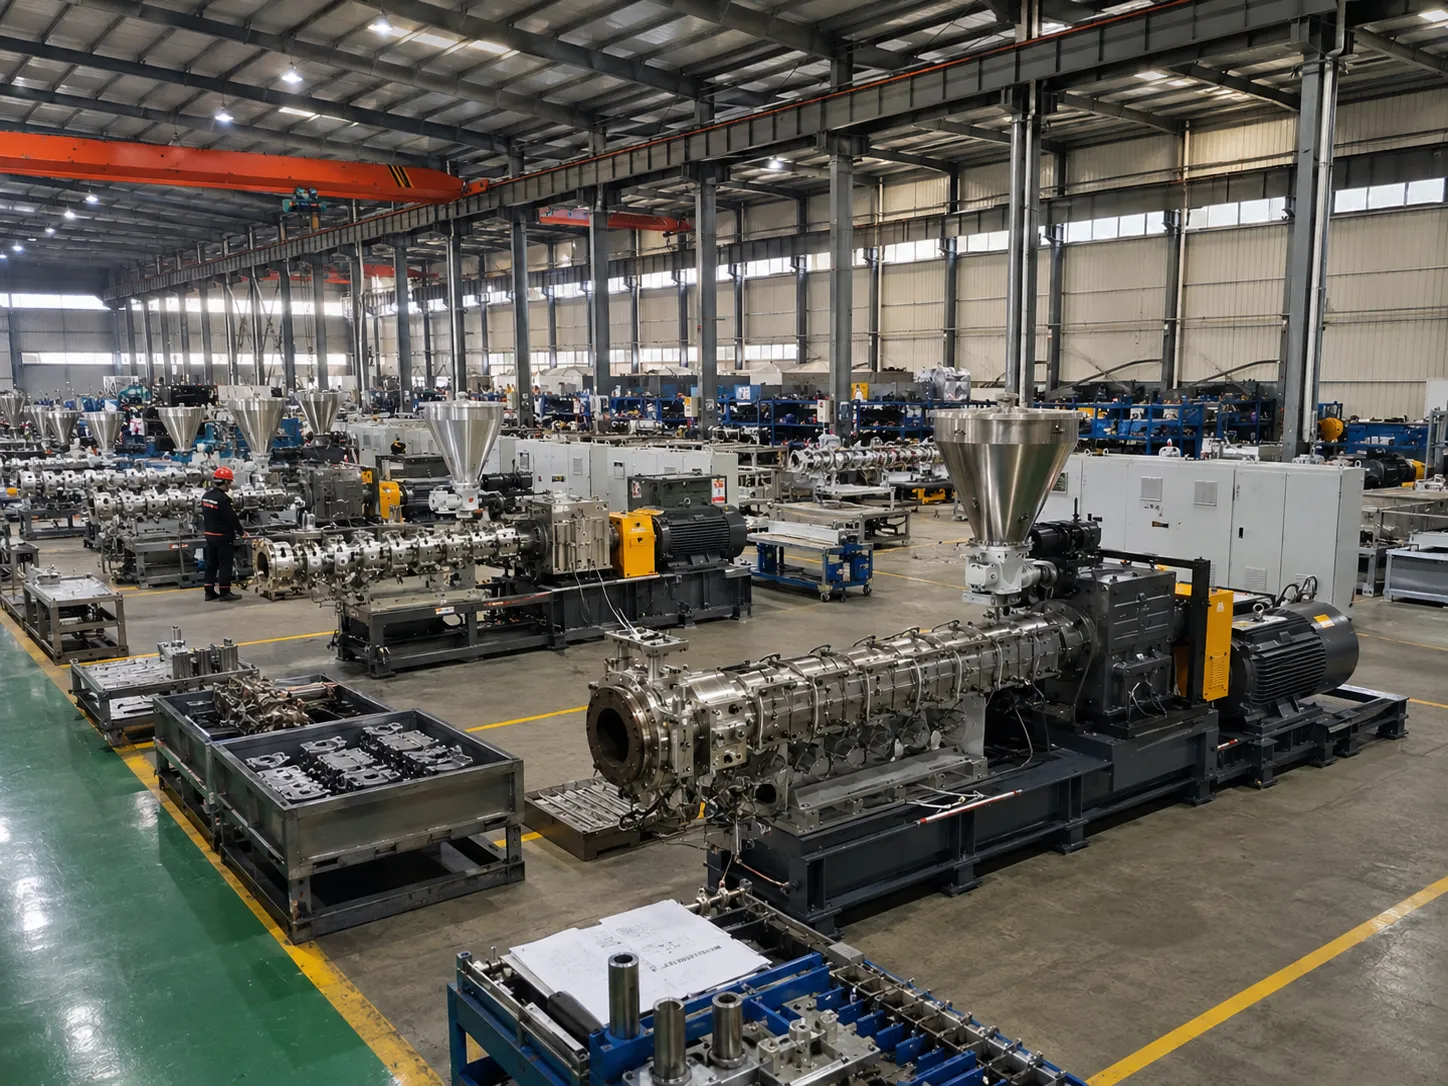
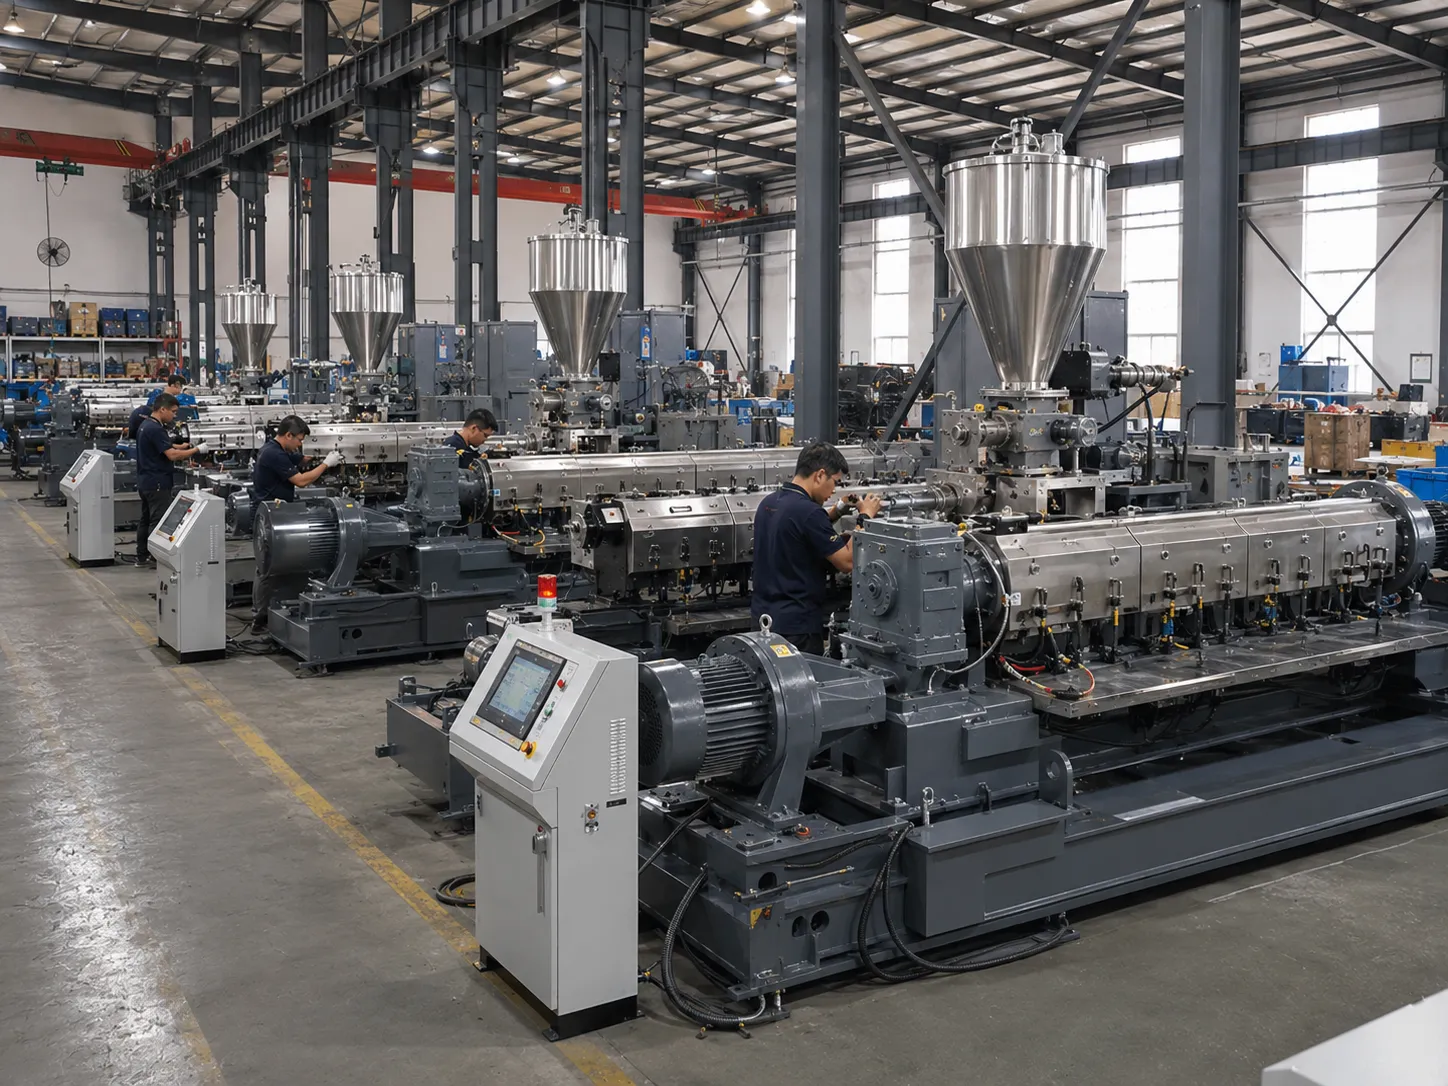
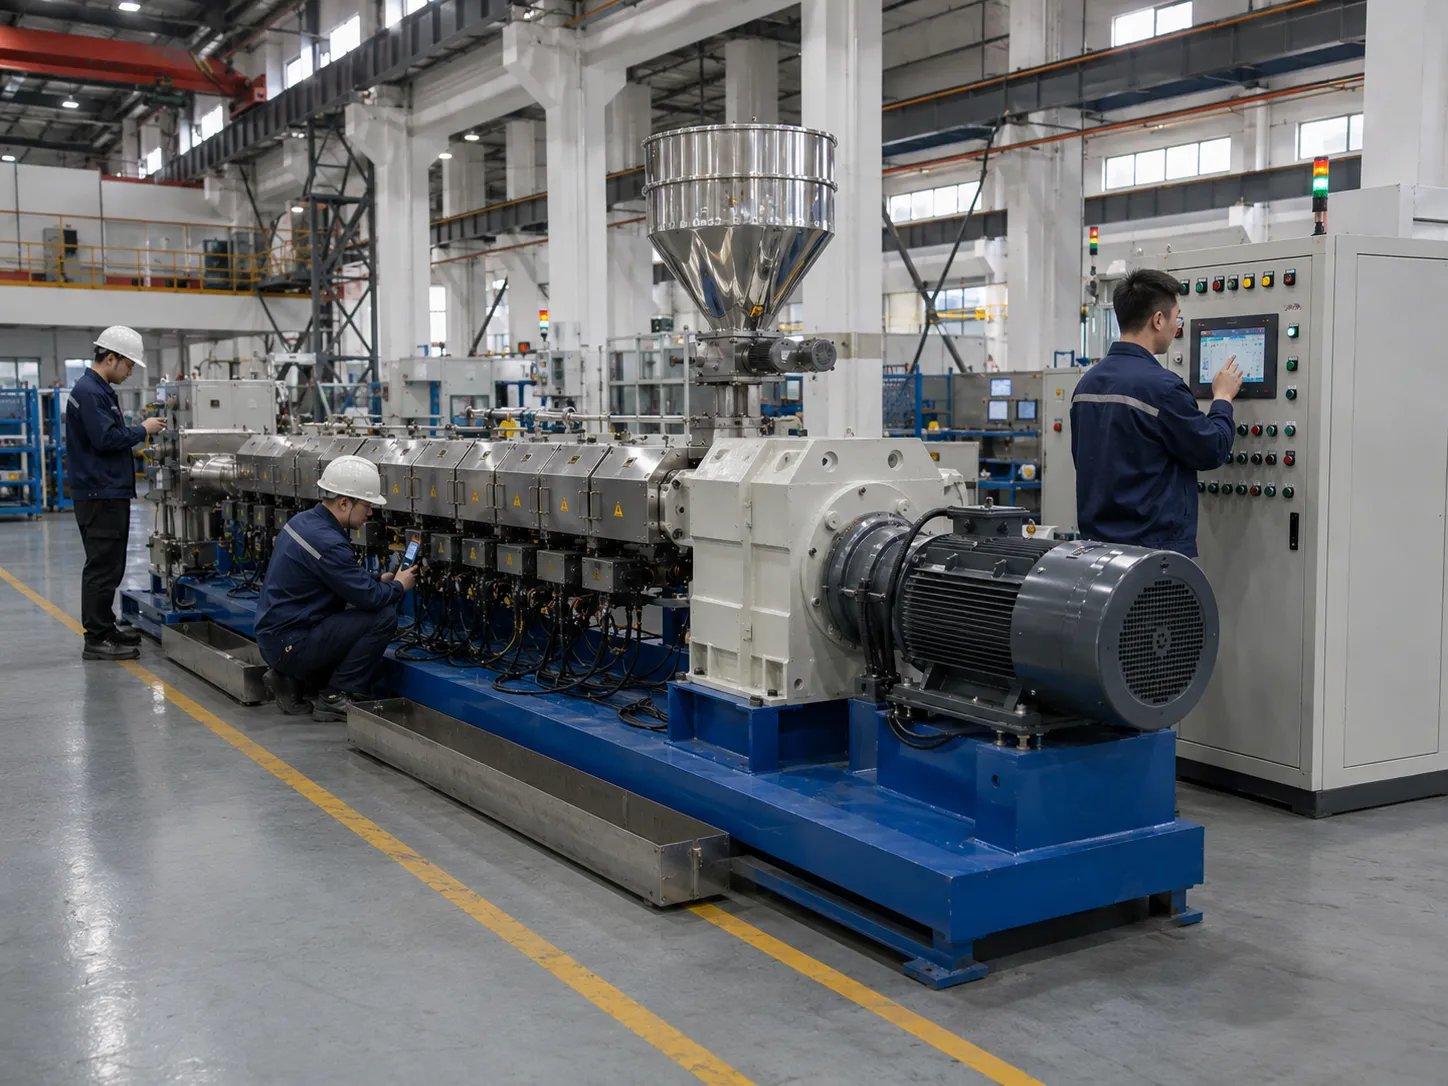
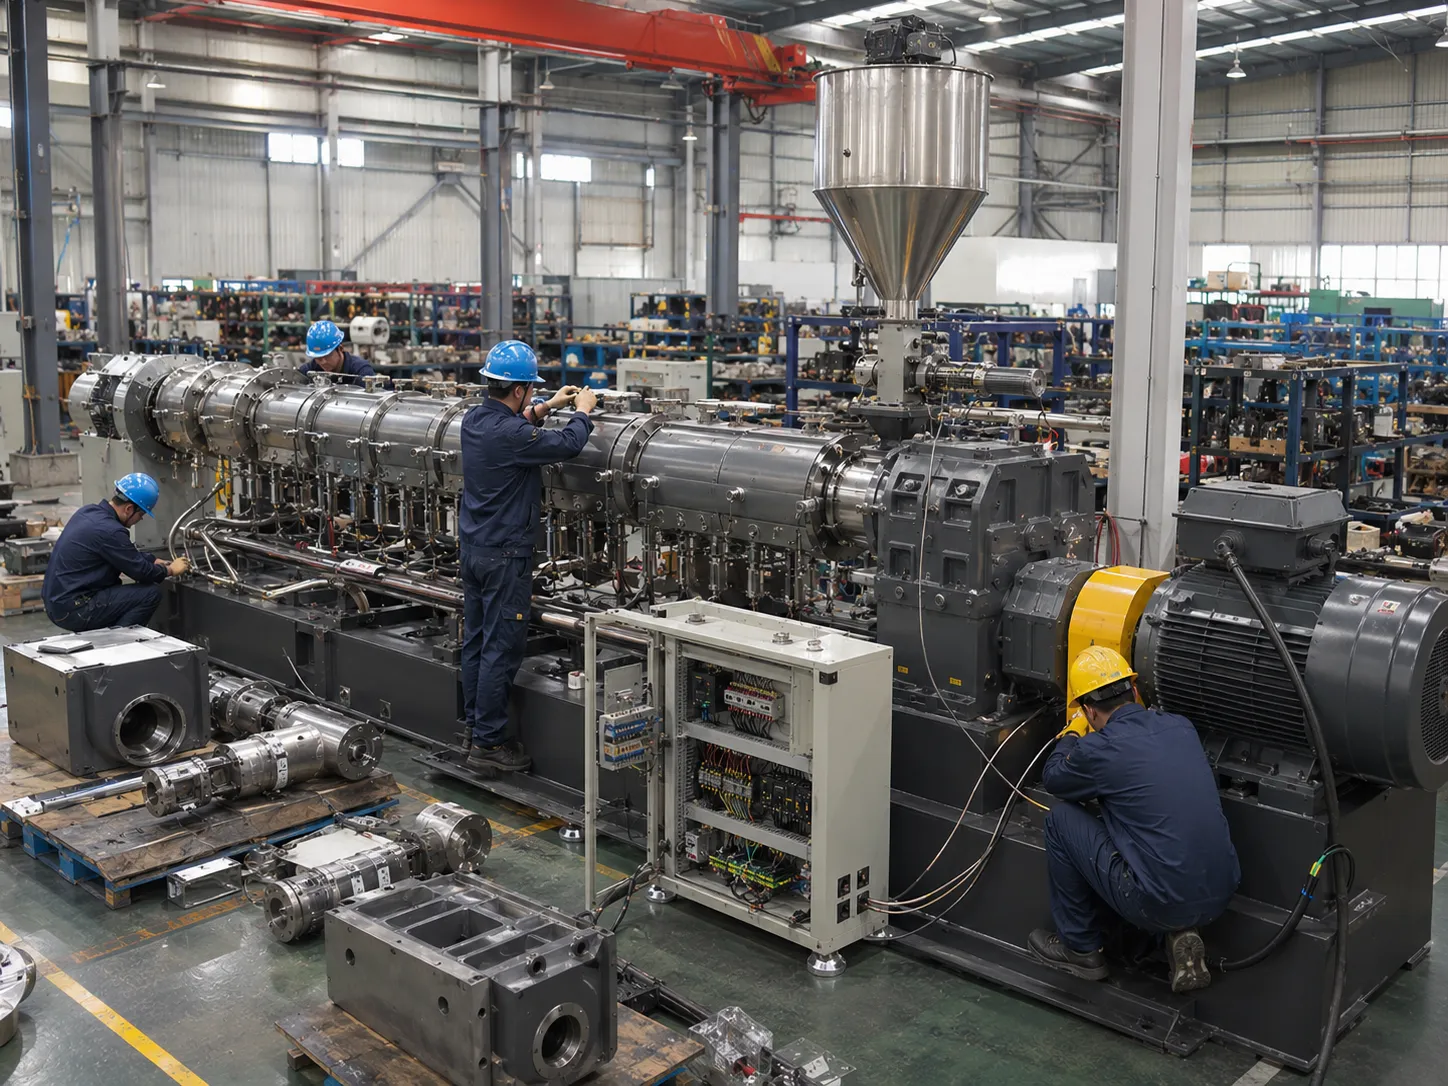
UET Recycled Plastic Extruder Factory in China
Every picture below is a real machine in our workshop, photographed before crating, not a rendering.
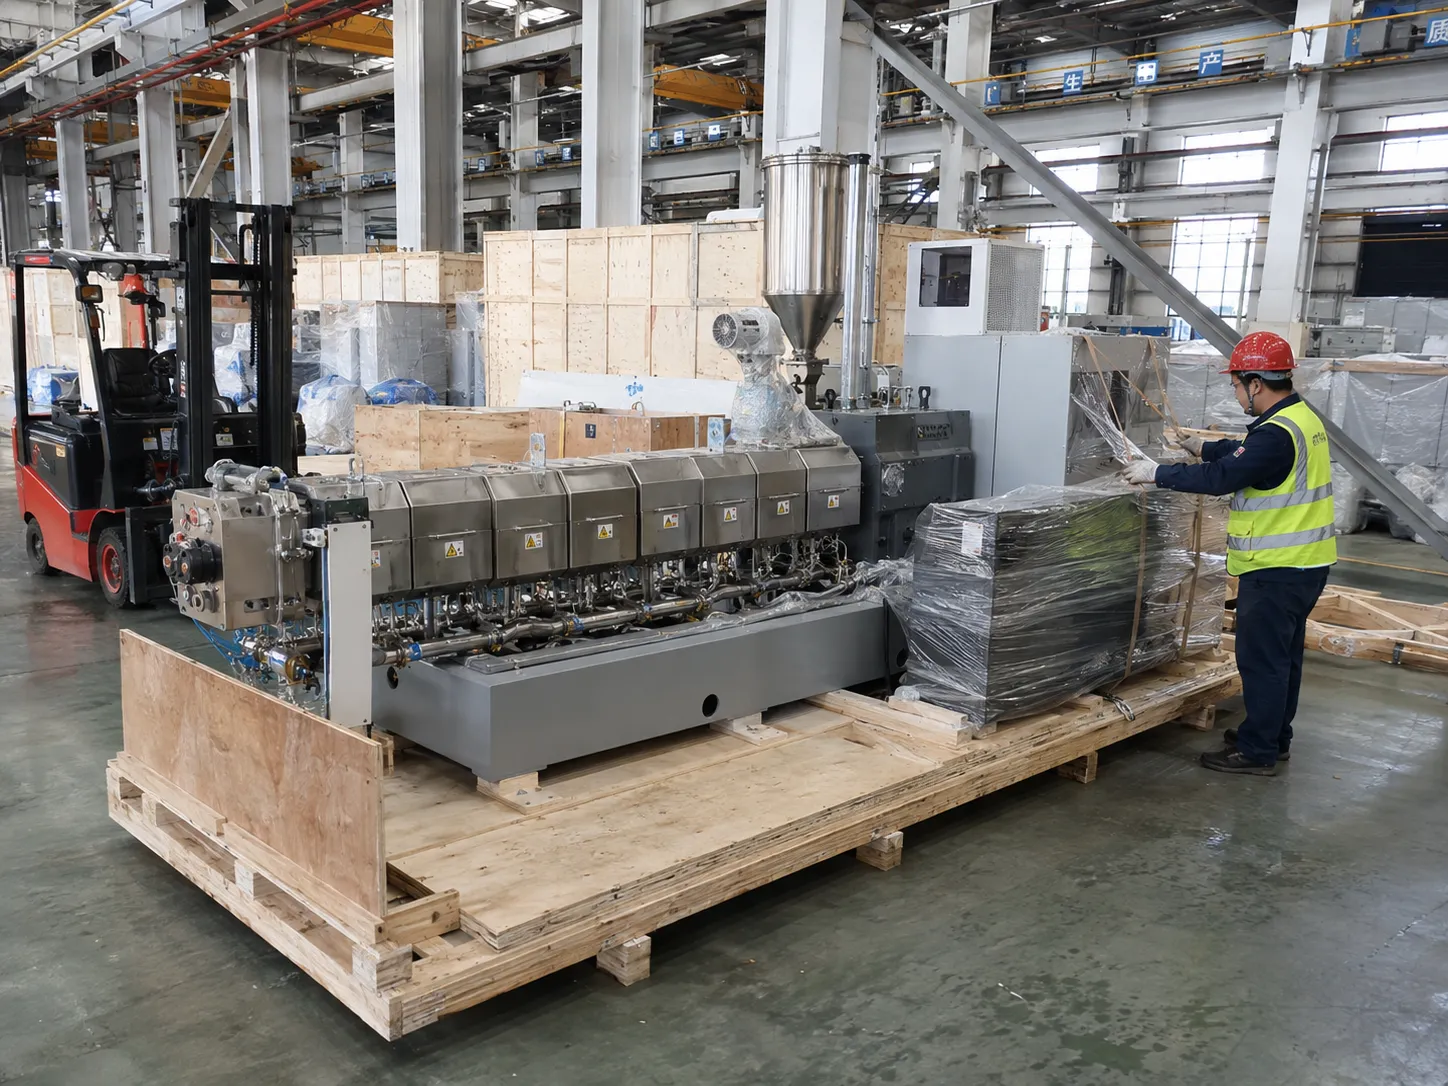
China Manufacturer & Supplier
Your Trusted China Recycled Plastic Extruder Manufacturer
Buying machinery from China should not feel like a gamble. Here is how we make it predictable.
OEM Custom Design
Send a drawing, a sample or just a material data sheet. Our engineers return a screw layout, barrel configuration and 3D drawing within 48 hours.
ODM Turnkey Lines
Crusher, washer, dryer, extruder, pelletizer, packing: one supplier, one responsibility. We commission the whole line before you pay the balance.
Private-Label Branding
Your nameplate, your colors, your manuals. Distributors and trading companies use this to build their own machine range without owning a factory.
Certification Paperwork
CE, ISO 9001:2015, RoHS, REACH and SGS documents prepared for your market and included with the shipment, so import inspection goes smoothly.
Proven Export Record
5,600+ machines delivered to 80+ countries since 2005. Seaworthy crating, full export paperwork and a container-loading photo report with every order.
After-Sales That Answers
Remote support in English and Chinese, on-site commissioning where needed, and spare parts shipped from stock within 24 hours, at cost price, for the life of the machine.
Ready to Upgrade Your Recycling Line?
Tell us your material, your hourly output and your target pellet spec. An engineer, not a sales script, replies with a configuration and quotation within 2 hours.
Why UET
Why Choose UET Recycled Plastic Extruders
Six reasons recycling plants stay with us after the first machine.
20+ Years in Extrusion
Building extruders since 2005: 5,600+ machines delivered, 3,500+ customers in 80+ countries, many on their third or fourth line.
Engineered From Your Material
We start from your feedstock and your target pellet, not from a catalog page. Screw layout, L/D ratio and downstream are matched to your recipe.
Compliance as Standard
CE, ISO 9001 and RoHS come with the machine, so it passes import inspection in the EU, the US and most other markets.
Factory-Direct Pricing
No trader margin. You pay for steel and engineering, not for a middleman, and the quotation itemizes every component.
Support for the Machine’s Life
7×24 remote diagnostics, operator training at commissioning, and lifetime spare-parts supply at cost price.
Delivery Dates in Writing
Standard models leave the factory in 1–2 weeks, customized lines in 4–6 weeks, and the date goes into the contract.
Customer Stories
What Recycling Plants Say About UET
Feedback from plants running our lines, with names and countries.
“Nearly a year running PP regrind with mixed impurities and it has never jammed. It draws noticeably less power than the brand we used before, and when a small part failed the replacement was arranged the same day.”
Jessica MillerPlastic Recycling · USA
“Eight months of continuous running without a single fault. Our qualified-product rate went from 92% to 98%, which our auditors noticed immediately.”
Amina SchulzPackaging Materials · EU
“We feed it 50% calcium carbonate regrind and it plasticizes evenly all day. Measured output is 25% above the machine it replaced, and it is quieter too.”
Oliver ThompsonConstruction Materials · UK
“Processing efficiency up 30%, cost per ton down 12%. We switch between ABS and PS several times a week and the changeover no longer eats a whole shift.”
Lena WeberAutomotive Parts · Germany
Explore More
Related Extruder & Pelletizing Equipment
The machines that usually sit next to a recycled plastic extruder in a working line.
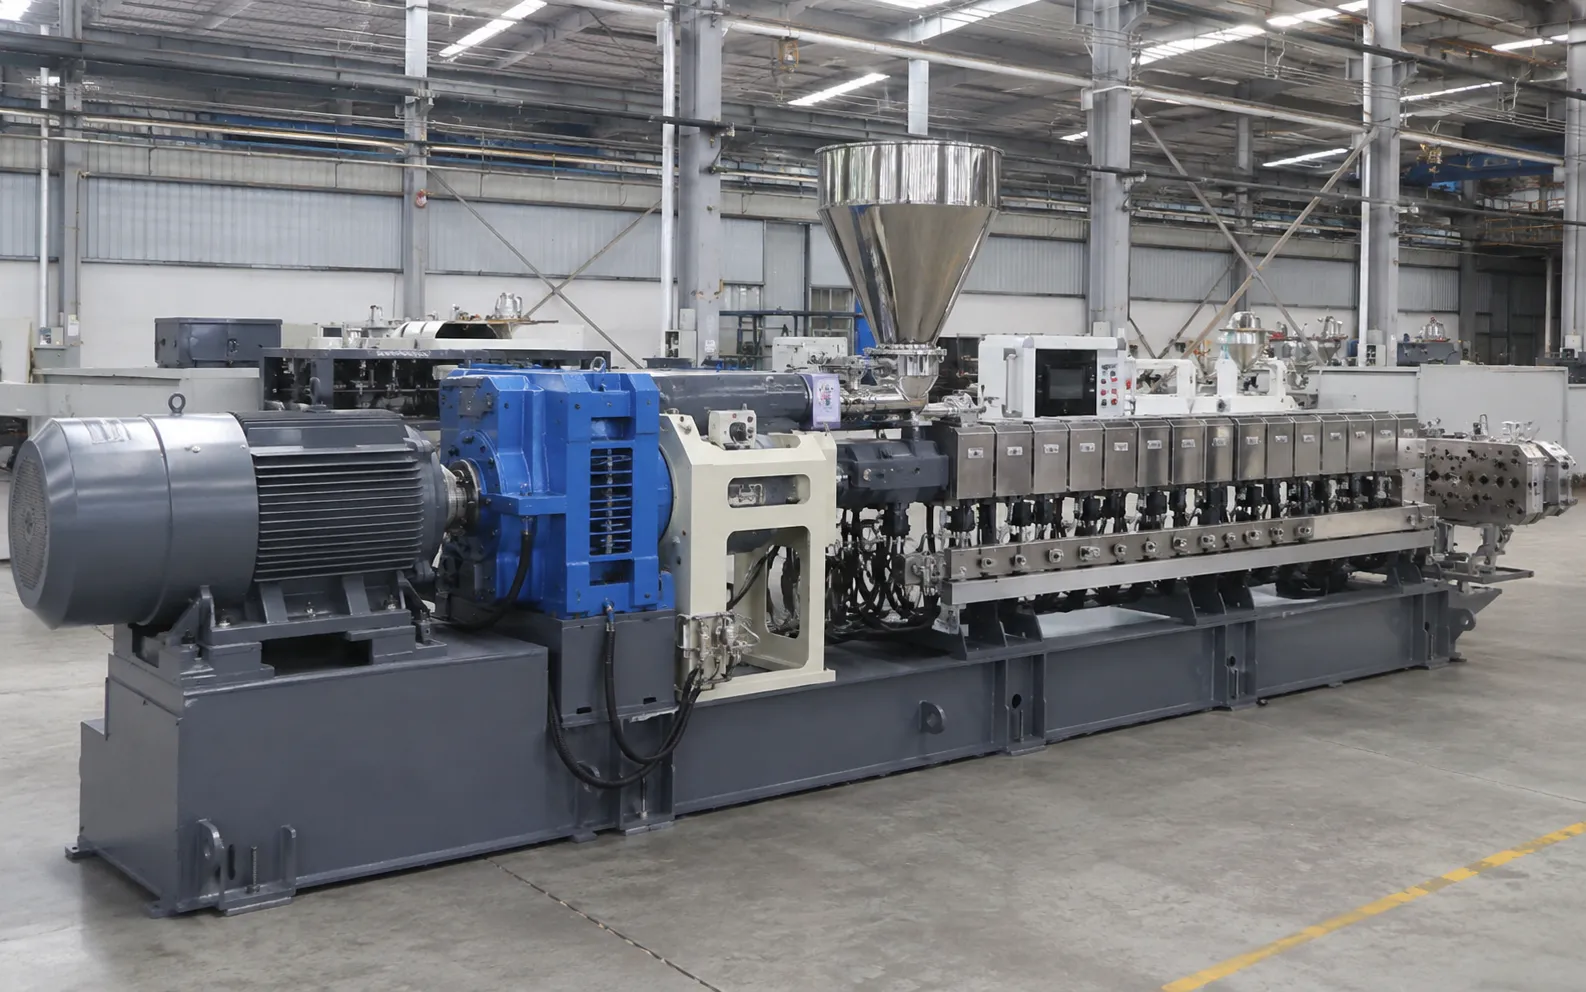
Twin Screw Extruder
The compounding platform behind our recycling lines: high-shear mixing for contaminated regrind.
Learn More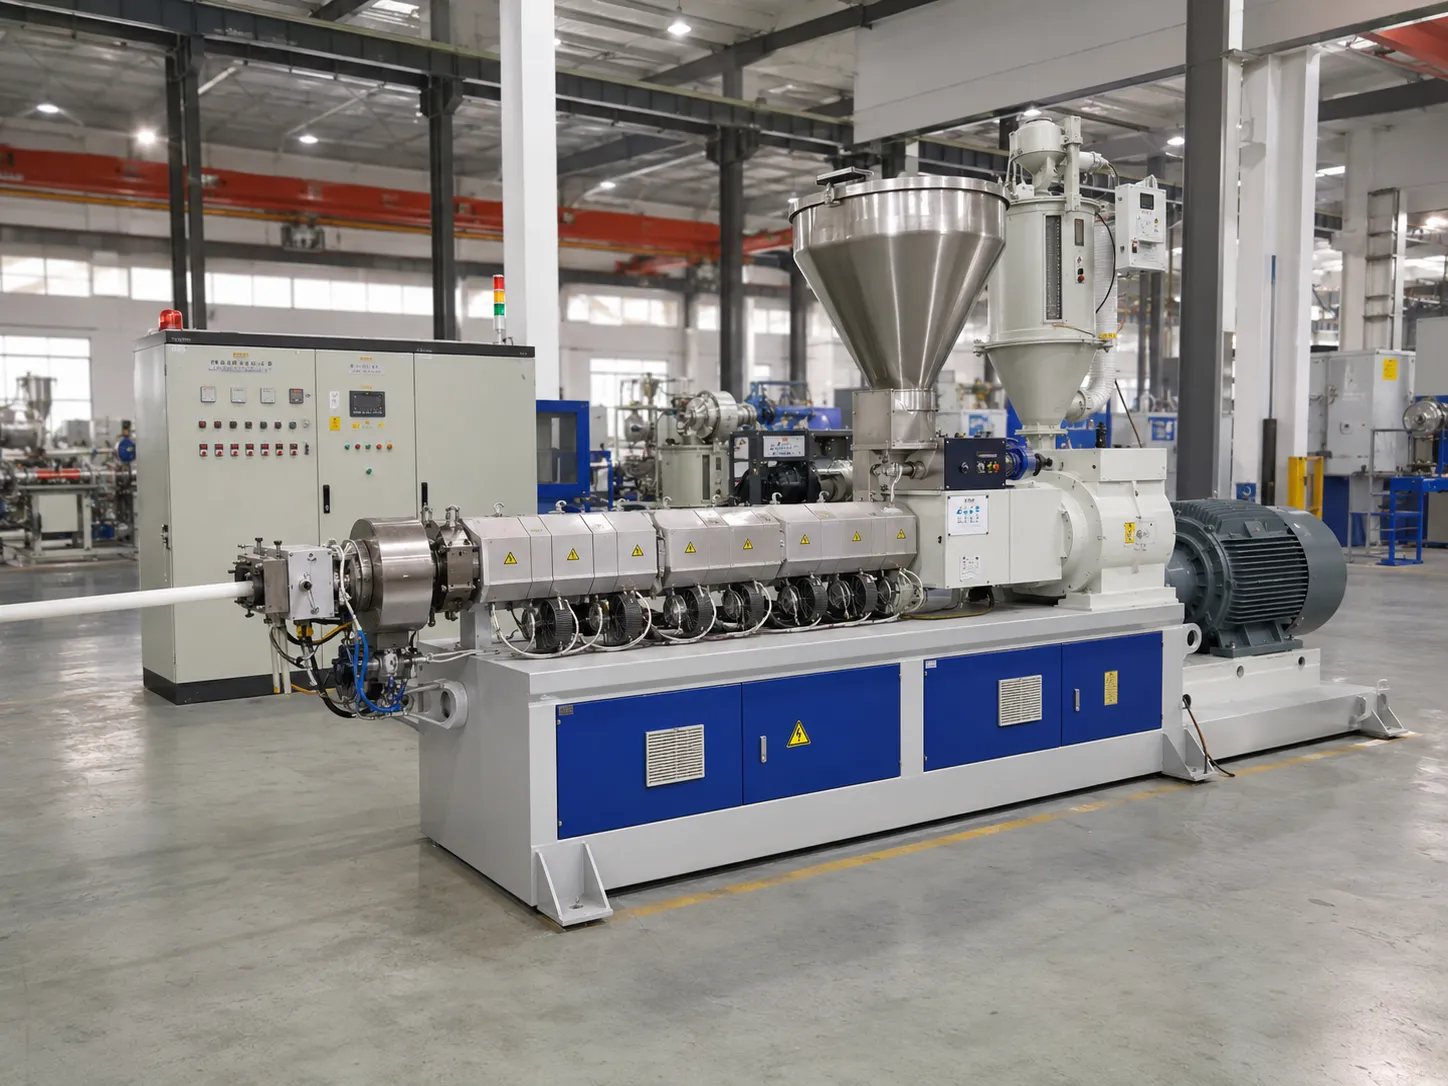
Single Screw Extruder
Cost-effective re-melting of clean recycled PE / PP flakes into pipes, sheets, films and profiles.
Learn More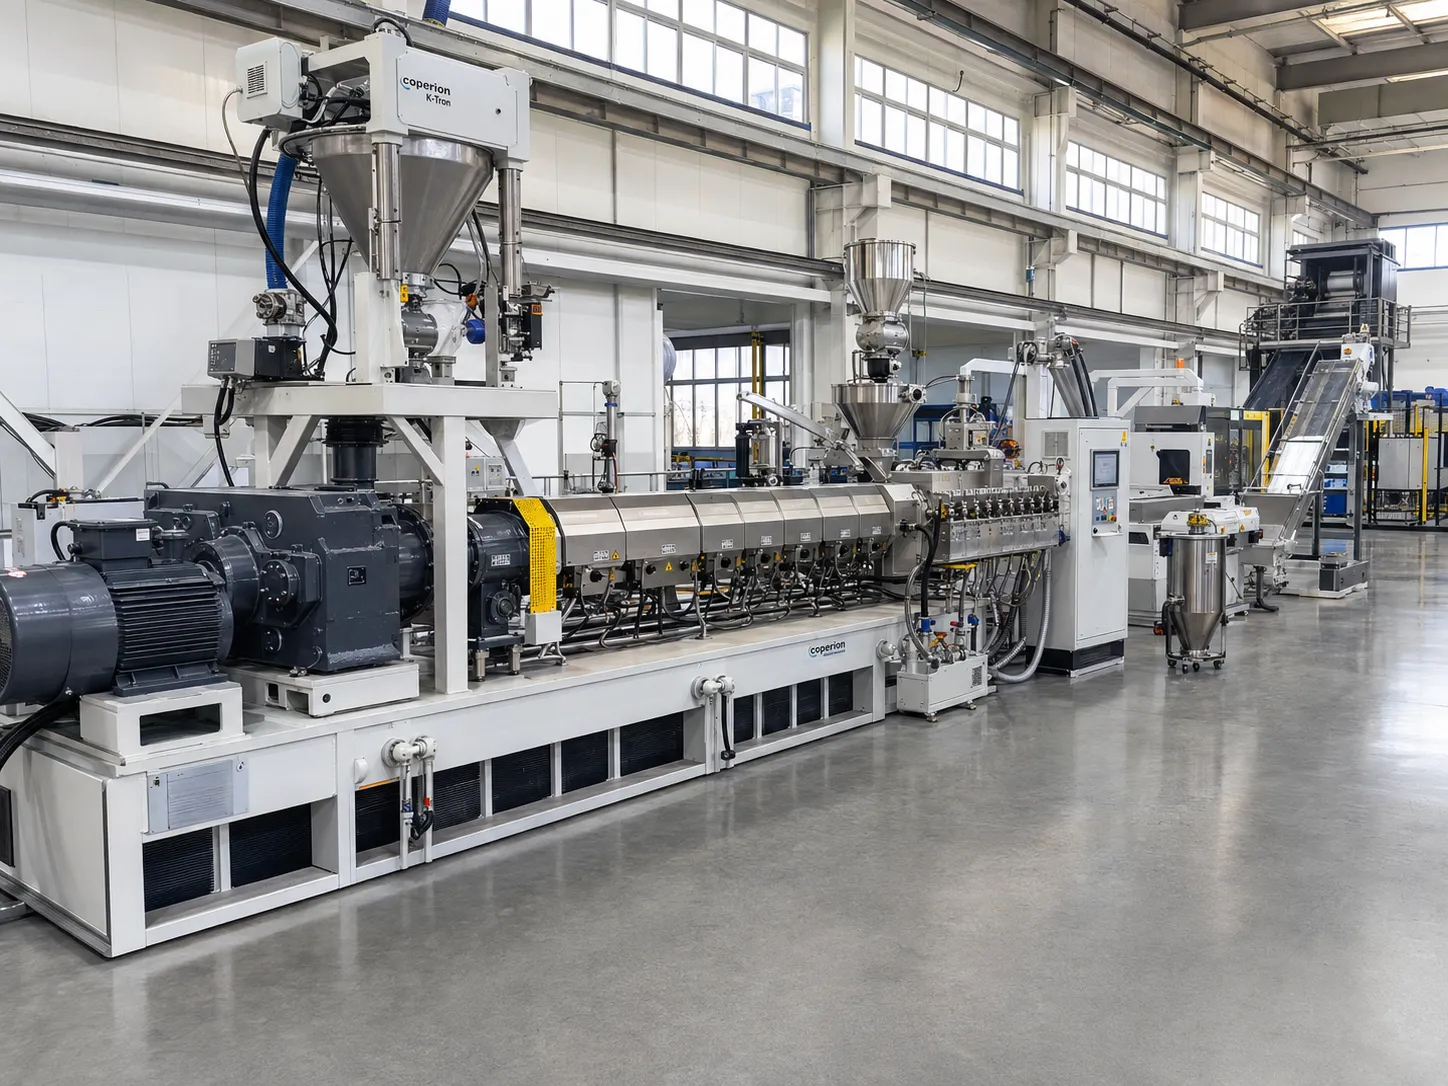
Compounding Machine
High-strength mixing for high-fill recycled compounds such as CaCO₃ and talc formulations.
Learn More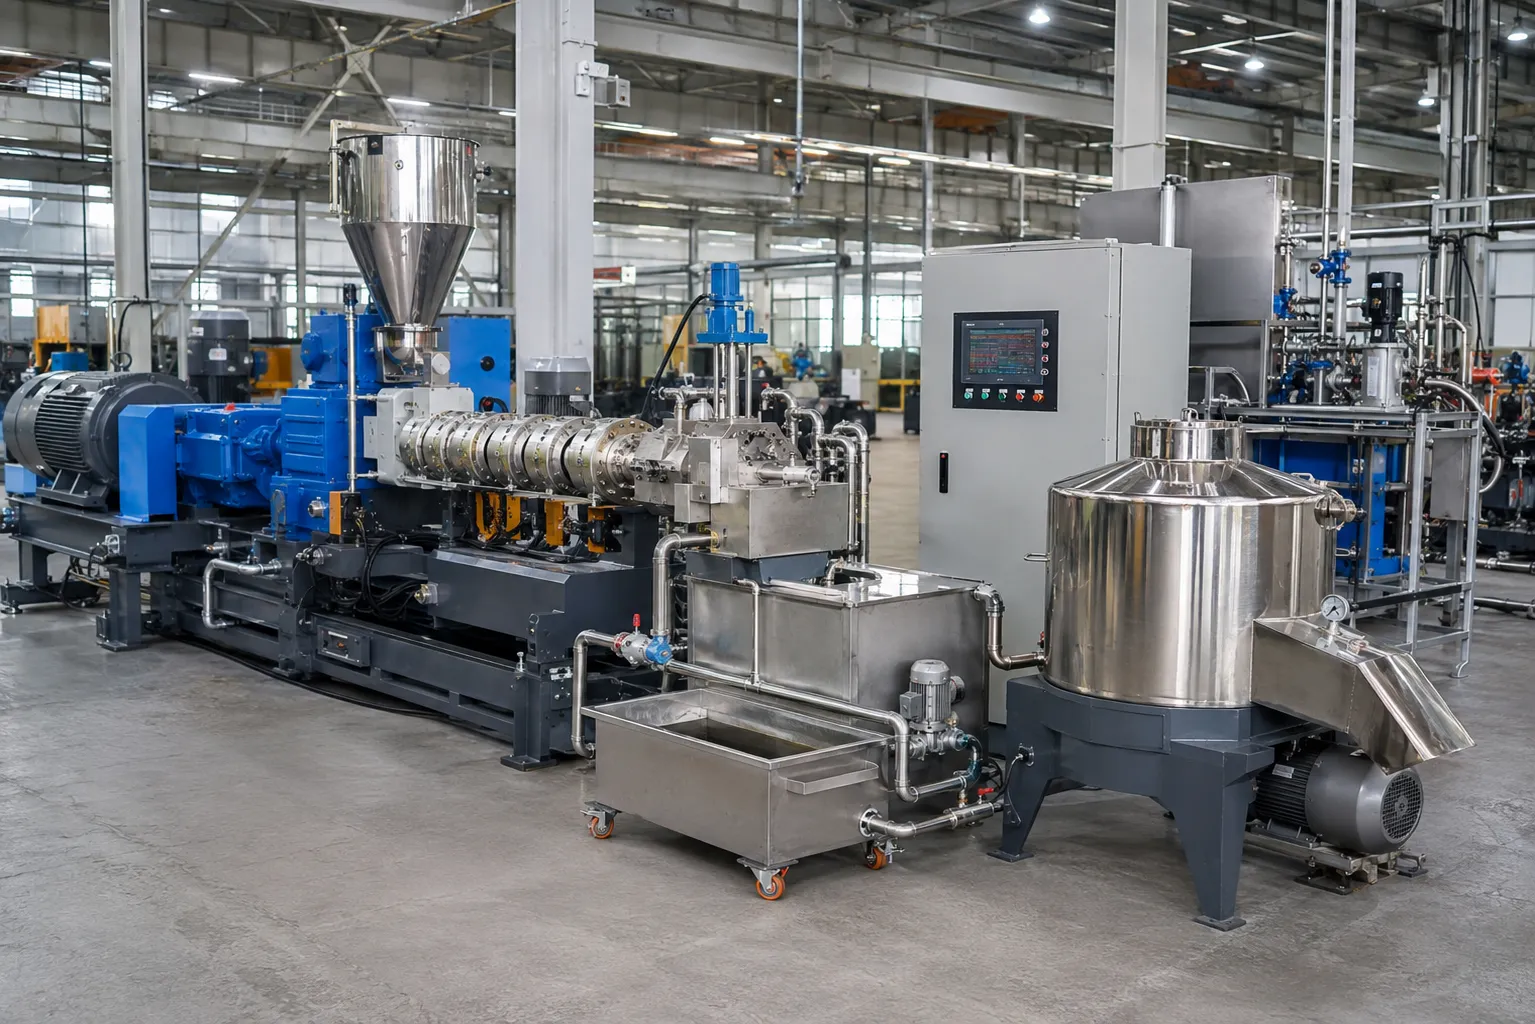
Underwater Pelletizing System
Recommended downstream for recycled PE / PP / PET: spherical, low-dust pellets at high throughput.
Learn More
Technical FAQ
Recycled Plastic Extruder FAQ
The questions every buyer asks us, answered the same way we answer them on a call.
What types of recycled materials can the Recycled Plastic Extruder process?
PP, PE, ABS, PS and PVC regrind, high-filled material with up to 50% CaCO₃ or talc, mixed regrind with up to 30% impurities, and physical forms from crushed flakes to film scraps and runner material. If you are unsure about your stream, send us a sample and we will run a trial.
What is the minimum order quantity for a Recycled Plastic Extruder?
One unit for standard models; we encourage trial orders. Customized configurations (special screw layouts or capacity designs) start at three units, and volume orders carry stepped discounts.
What is the warranty period of the Recycled Plastic Extruder?
One year on the whole machine and 24 months on core components (screws, barrels, motor, PLC). After warranty we keep supplying spare parts at cost price and support stays free for the life of the machine.
Do you provide installation and training for the Recycled Plastic Extruder?
Yes. Remote commissioning guidance and operator training are included free; on-site engineer visits are available on request. You also receive English and Chinese manuals plus video tutorials.
What payment methods do you accept for Recycled Plastic Extruder orders?
T/T, L/C and Western Union. The standard schedule is 30% advance and 70% before shipment; long-term partners and large orders can negotiate more flexible terms.
What is the typical delivery time for a Recycled Plastic Extruder?
Standard models ship in 1–2 weeks. Customized lines take 4–6 weeks, and expedited production is possible when your project is urgent.
How do I prevent material blocking in the Recycled Plastic Extruder?
Screen and dry the regrind first, match barrel temperatures to the material, clean screws and barrels on schedule, change clogged filters promptly and keep the feed rate steady. Our commissioning team sets these parameters with your operators on site or remotely.
What is the wearing parts replacement cycle of the Recycled Plastic Extruder?
Screws and barrels typically last 6–12 months depending on how abrasive your material is; filters and seals should be checked every 3–6 months; motors and bearings run 3–5 years with normal maintenance. We stock all of these for same-week dispatch.