PVC Extrusion Technology
PVC Extruder Machine for Rigid, Flexible and Foamed PVC Production
We have built PVC extruders in our own factory in China for the last 20 years and shipped more than 5,600 extrusion lines to 80+ countries. Every machine is set up around one goal: keep the melt steady so your pipes and profiles hold tolerance, shift after shift.
±0.8°C closed-loop control keeps PVC inside its safe window, so you don’t see black specks or brittle walls.
Nitrided 42CrMo screw and barrel (≥600 HV) stand up to the HCl that PVC releases when it degrades.
Around 35% less energy per kg than the older extruders most buyers replace.
Overview
What Is a PVC Extruder Machine?
A plain-language look at the machine, what it runs and what it makes.
The short version
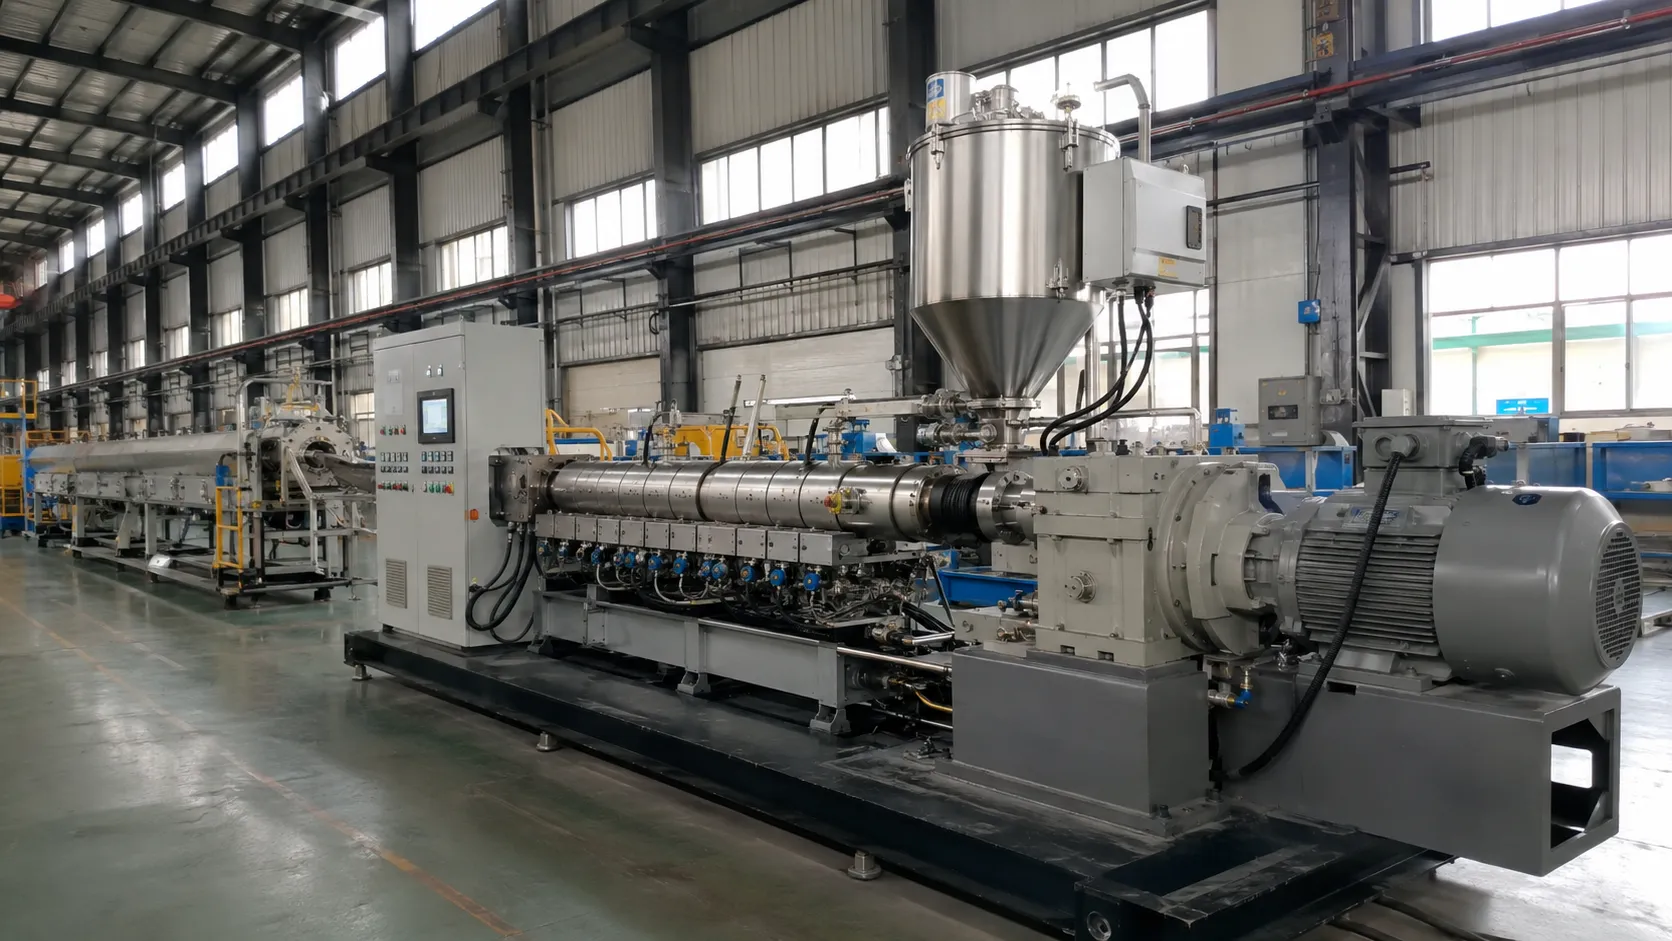
A PVC extruder melts PVC compound and pushes it through a shaped die to make a continuous product: pipe, window profile, sheet, conduit or pellet. Everything else on the line, from the feeder to the cutter, exists to support that one step.
PVC is not a forgiving material. It degrades if it gets too hot and it corrodes ordinary steel, so a PVC extruder runs slower and cooler than a general-purpose machine, with a nitrided screw and barrel built to take the attack. That is the real difference between a PVC extruder and a PE machine with a PVC label on it.
We are a China PVC extruder manufacturer based in Qingdao, and every machine we sell is run with real material in our workshop before it ships. You get factory-direct pricing, a 2-year core warranty and spare parts for the life of the machine.
What it processes
Rigid PVC (uPVC)Flexible PVCFoamed PVCPVC compoundsRecycled PVCHigh-fill PVC (CaCO₃)
What it makes
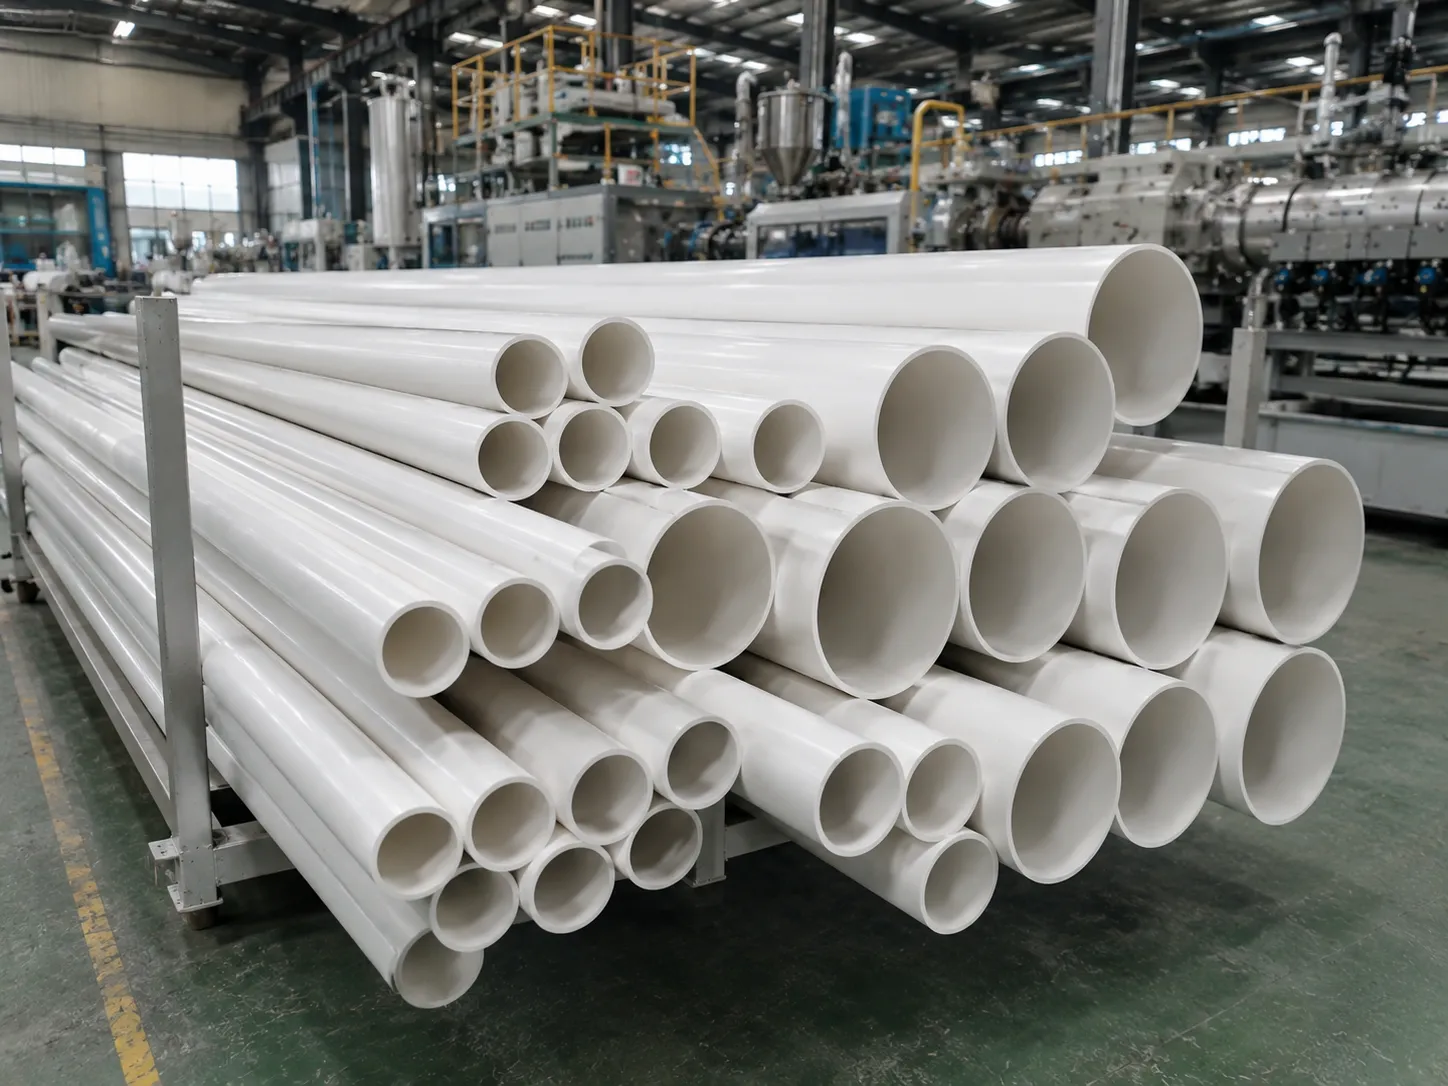
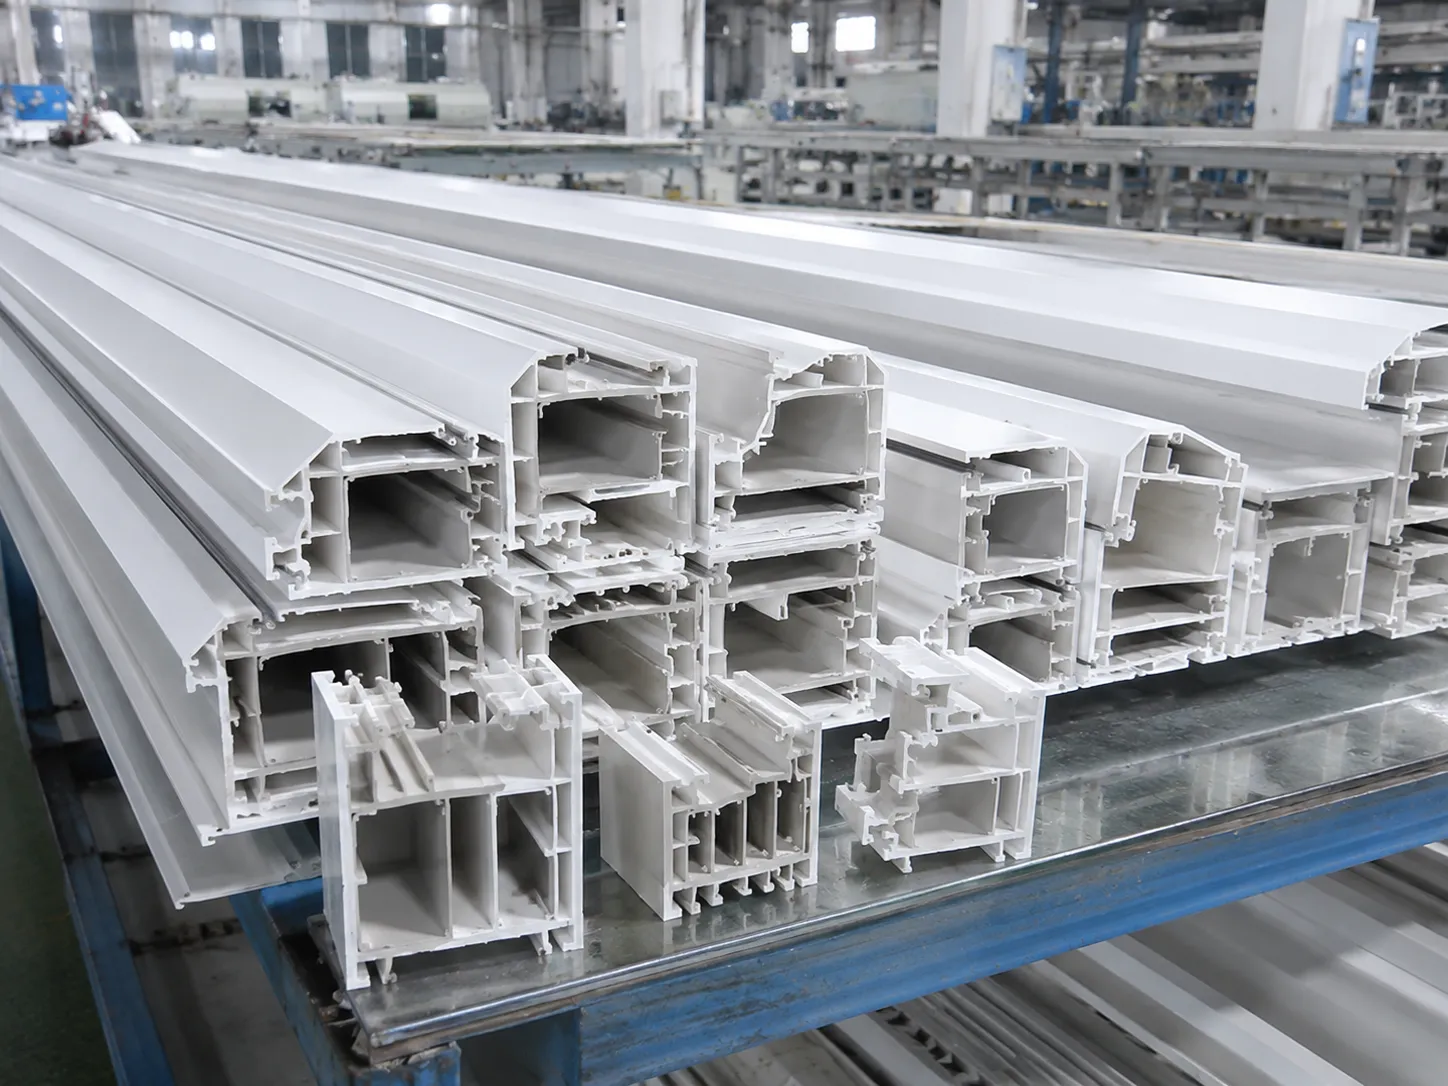
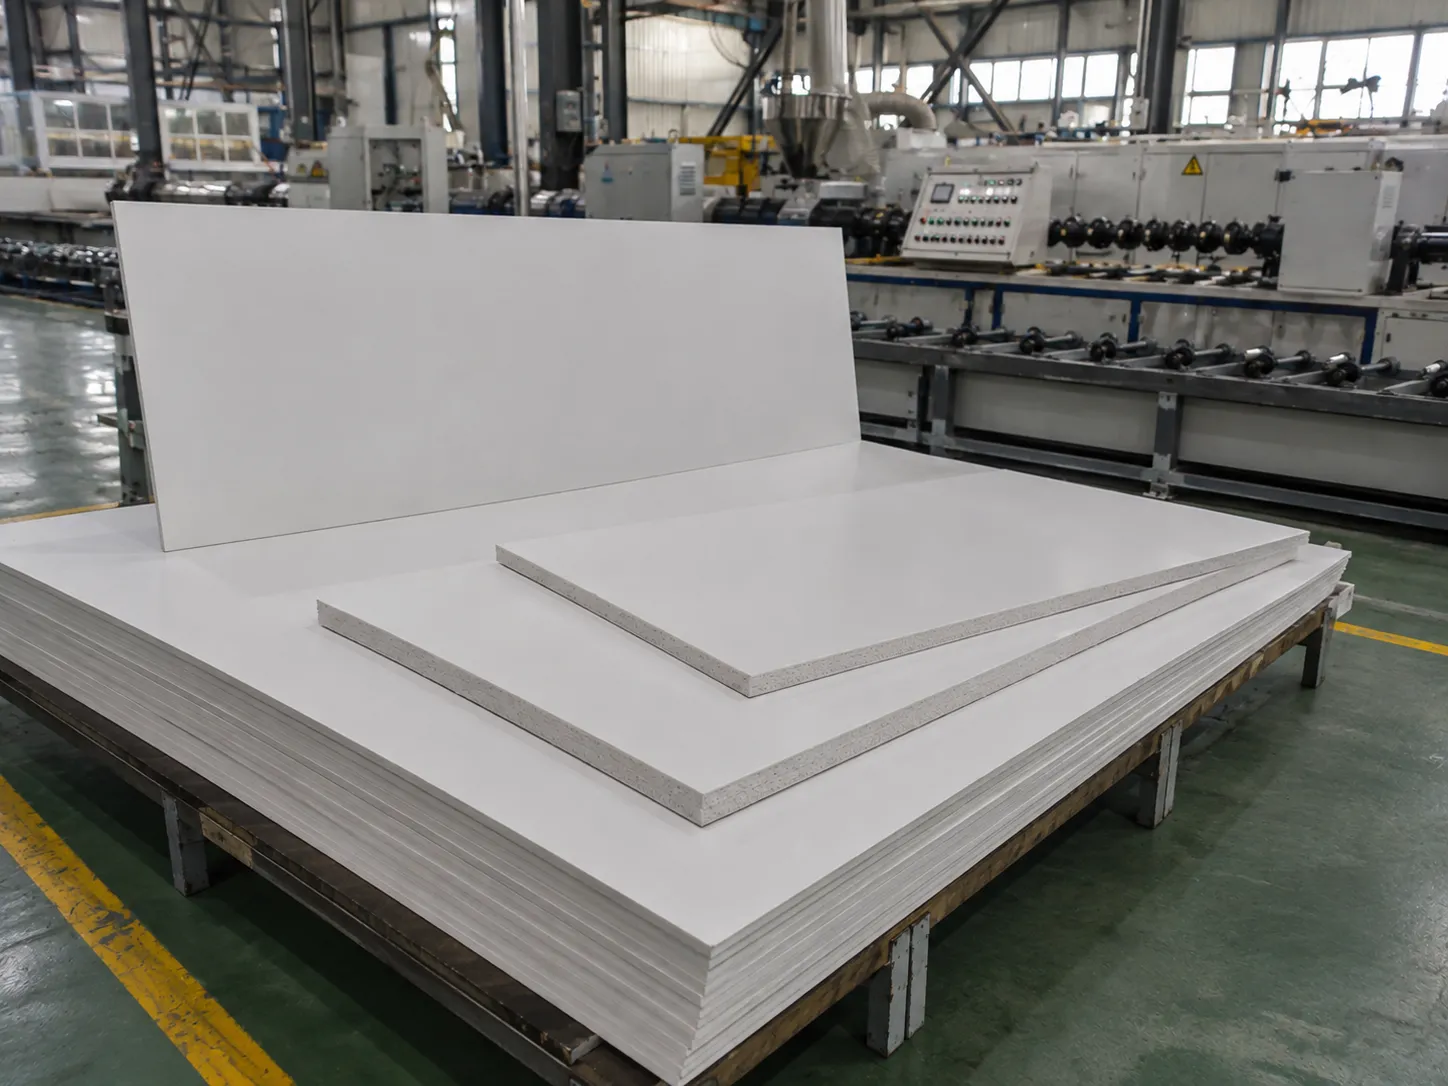
Pipes Ø20–630mmWindow & door profilesFoamed boardsElectrical conduitsDecorative trimsPVC pellets
Engineering Answers
Where PVC Lines Usually Go Wrong, and What We Do About It
These are the six failure modes we see most on site, and the engineering choice that prevents each one.
01
Thermal degradation
PVC starts to break down above 200°C. We hold each barrel zone within ±0.8°C so the melt never sits in the danger window, and you don’t get black specks or char lines.
±0.8°C stability02
Dimensional drift
Wall thickness and outer diameter drift when the puller and the melt temperature fight each other. Our dies are calibrated and the haul-off runs in closed loop, so profiles stay within ±0.02mm.
±0.02mm tolerance03
Poor gelation
Unmelted grains show up as weak spots and rough surfaces. The screw geometry is matched to PVC powder so the melt gels fully without over-shearing.
Full gelation, low shear04
Power bills
Heating and drive power are most of your running cost. Efficient motors, ceramic heaters and a standby mode cut energy per kg by roughly a third.
−35% kWh per kg05
Slow changeover
Switching from one profile to another should not eat a whole shift. Quick-clamp dies and stored recipes bring changeover under 12 minutes.
≤12 min changeover06
Screw wear
HCl from degrading PVC eats ordinary screws in months. Nitrided 42CrMo at 600 HV or harder keeps the screw and barrel in service for years.
≥600 HV screw hardness
PVC Extruder Machine for Sale
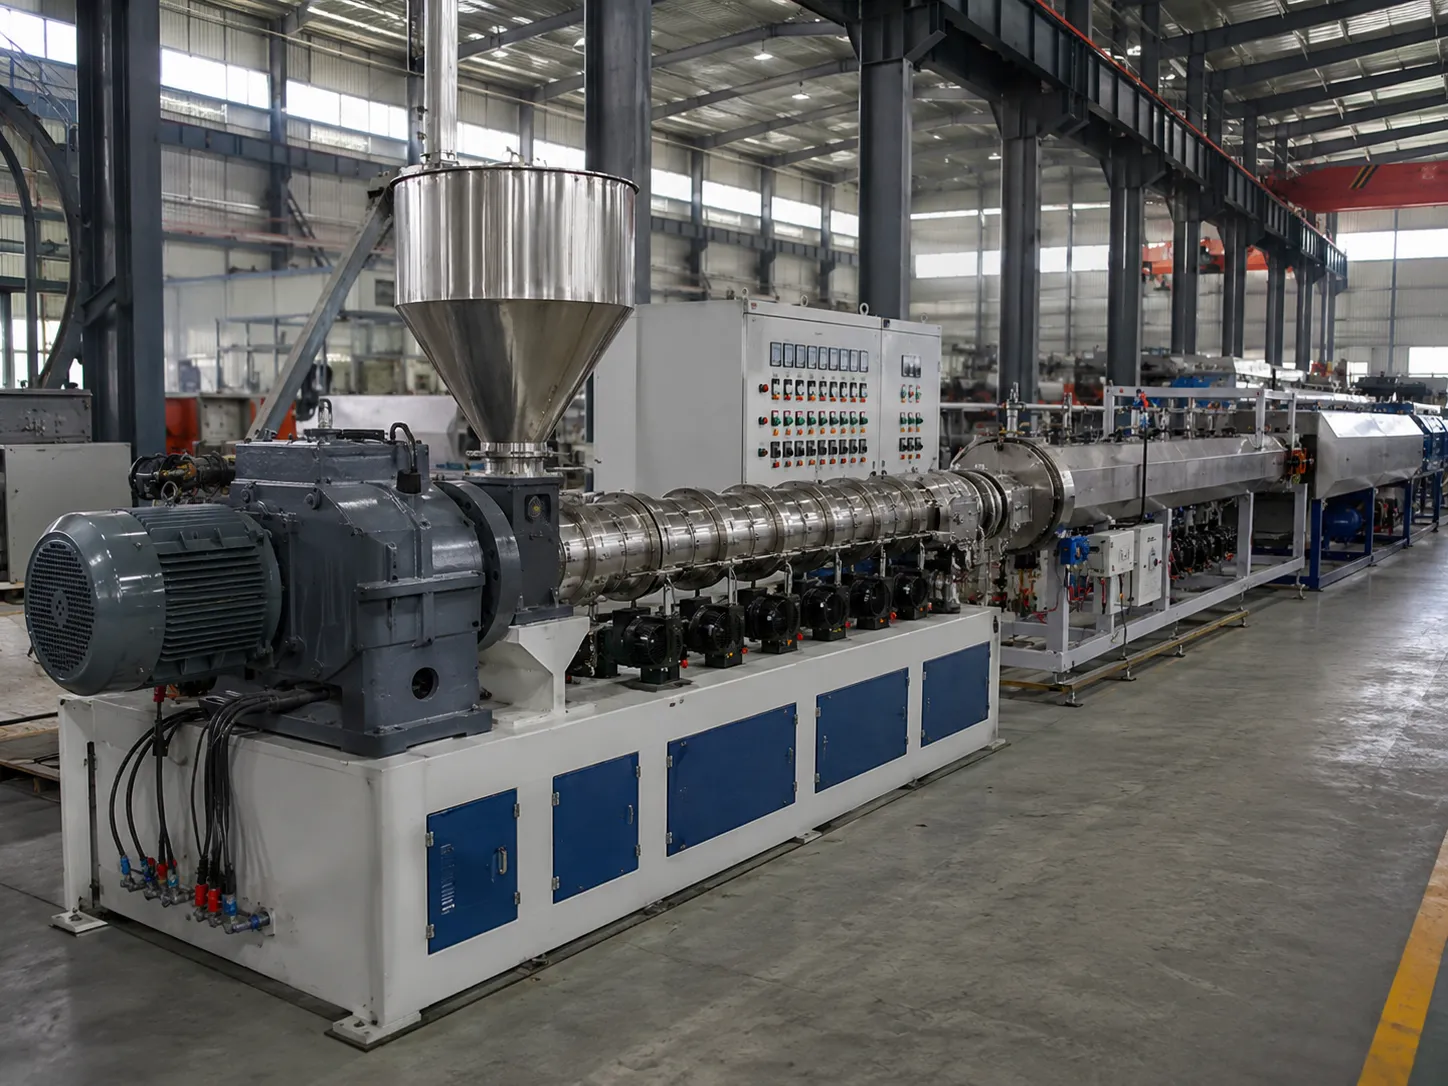
PVC Extruder Models for Every Pipe Diameter
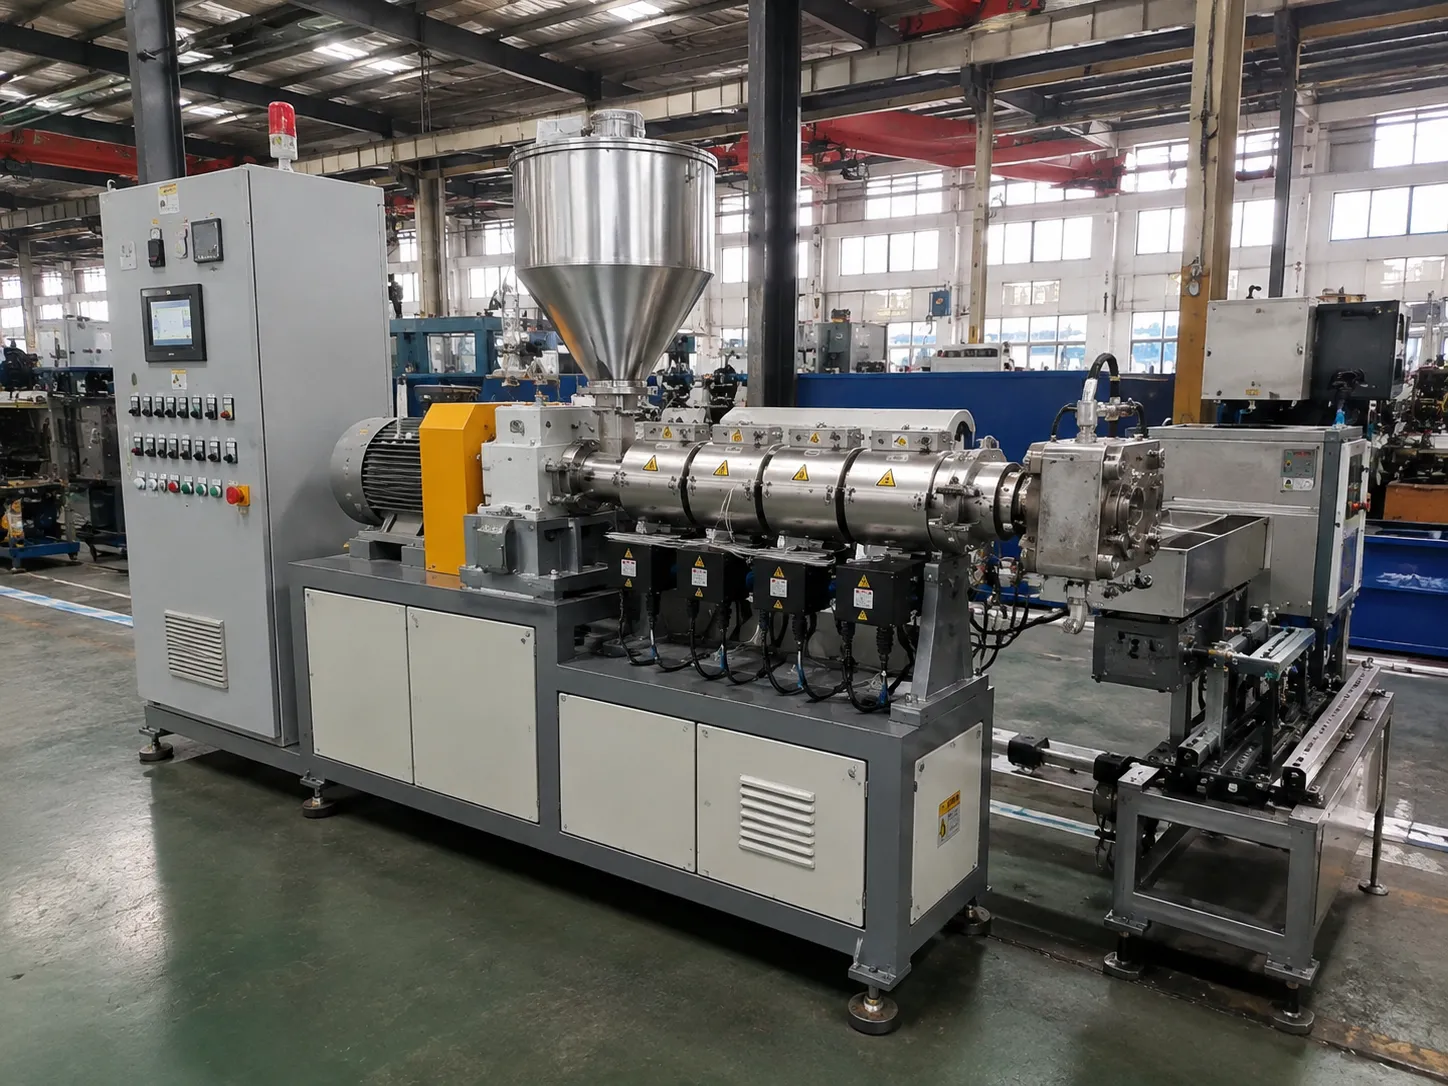
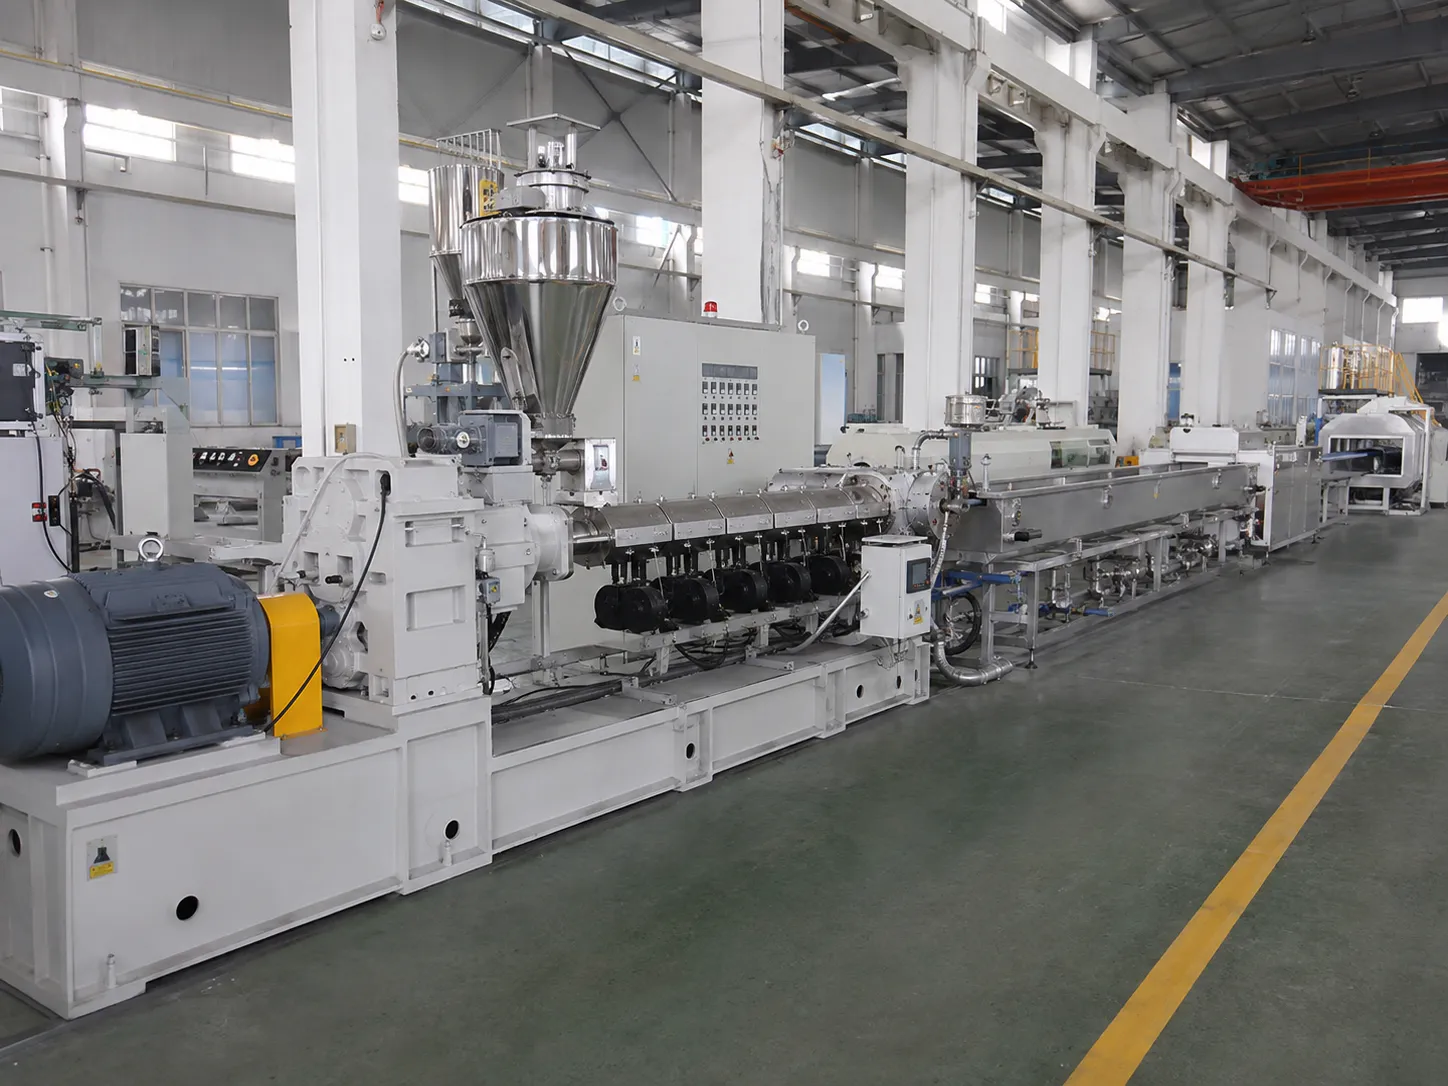
Five frames cover Ø20 to 630mm. The three best sellers are below; the full table adds the two large municipal frames.
Compact
UET-50
Output50–100 kg/h
ScrewØ50mm · 25:1
Main motor18 kW
Product rangeØ20–63mm
Best Seller
UET-65
Output100–200 kg/h
ScrewØ65mm · 28:1
Main motor30 kW
Product rangeØ63–160mm
High Output
UET-80
Output200–350 kg/h
ScrewØ80mm · 30:1
Main motor45 kW
Product rangeØ160–300mm
Need Ø315–630mm municipal pipes? UET-90 and UET-110 large-diameter lines are available. See the full specification table ↓
Datasheet
PVC Extruder Technical Specifications
The full parameter sheet for all five frames. Custom screw, die and downstream configurations are quoted on request.
| Parameter | UET-50 | UET-65POPULAR | UET-80 | UET-90 | UET-110 |
|---|---|---|---|---|---|
| Screw diameter | 50 mm | 65 mm | 80 mm | 90 mm | 110 mm |
| Screw L/D ratio | 25:1 | 28:1 | 30:1 | 30:1 | 32:1 |
| Screw speed | 100–180 rpm | 120–200 rpm | 100–160 rpm | 90–140 rpm | 80–120 rpm |
| Production capacity | 50–100 kg/h | 100–200 kg/h | 200–350 kg/h | 300–500 kg/h | 500–800 kg/h |
| Main motor power | 18 kW | 30 kW | 45 kW | 55 kW | 90 kW |
| Product diameter range | Ø20–63 mm | Ø63–160 mm | Ø160–300 mm | Ø315–450 mm | Ø450–630 mm |
| Temperature accuracy | Closed-loop PID, ±0.8°C stability, auto feed adjustment, melt-break alarm | ||||
| Heating / cooling | Ceramic + cast-aluminum heaters, independent zones with air cooling | ||||
| Screw & barrel material | 42CrMo nitrided (≥600 HV), corrosion-resistant for PVC melt | ||||
| Processable materials | Rigid PVC, flexible PVC, foamed PVC, PVC compounds | ||||
| Machine dimensions (L×W×H) | ≈6.0×1.5×1.9 m | ≈6.5×1.8×2.0 m | ≈7.0×1.9×2.1 m | ≈7.5×2.0×2.2 m | ≈8.0×2.2×2.4 m |
| Machine weight | ≈2,500 kg | ≈3,200 kg | ≈4,000 kg | ≈4,800 kg | ≈6,000 kg |
| Voltage | 380V / 50Hz / 3-phase (customizable to local standard) | ||||
| Warranty | 1-year machine · 2-year core components · lifetime spare parts | ||||
Need a special configuration (twin-screw, conical screw, higher output)? Talk to our engineers →
Machine Anatomy
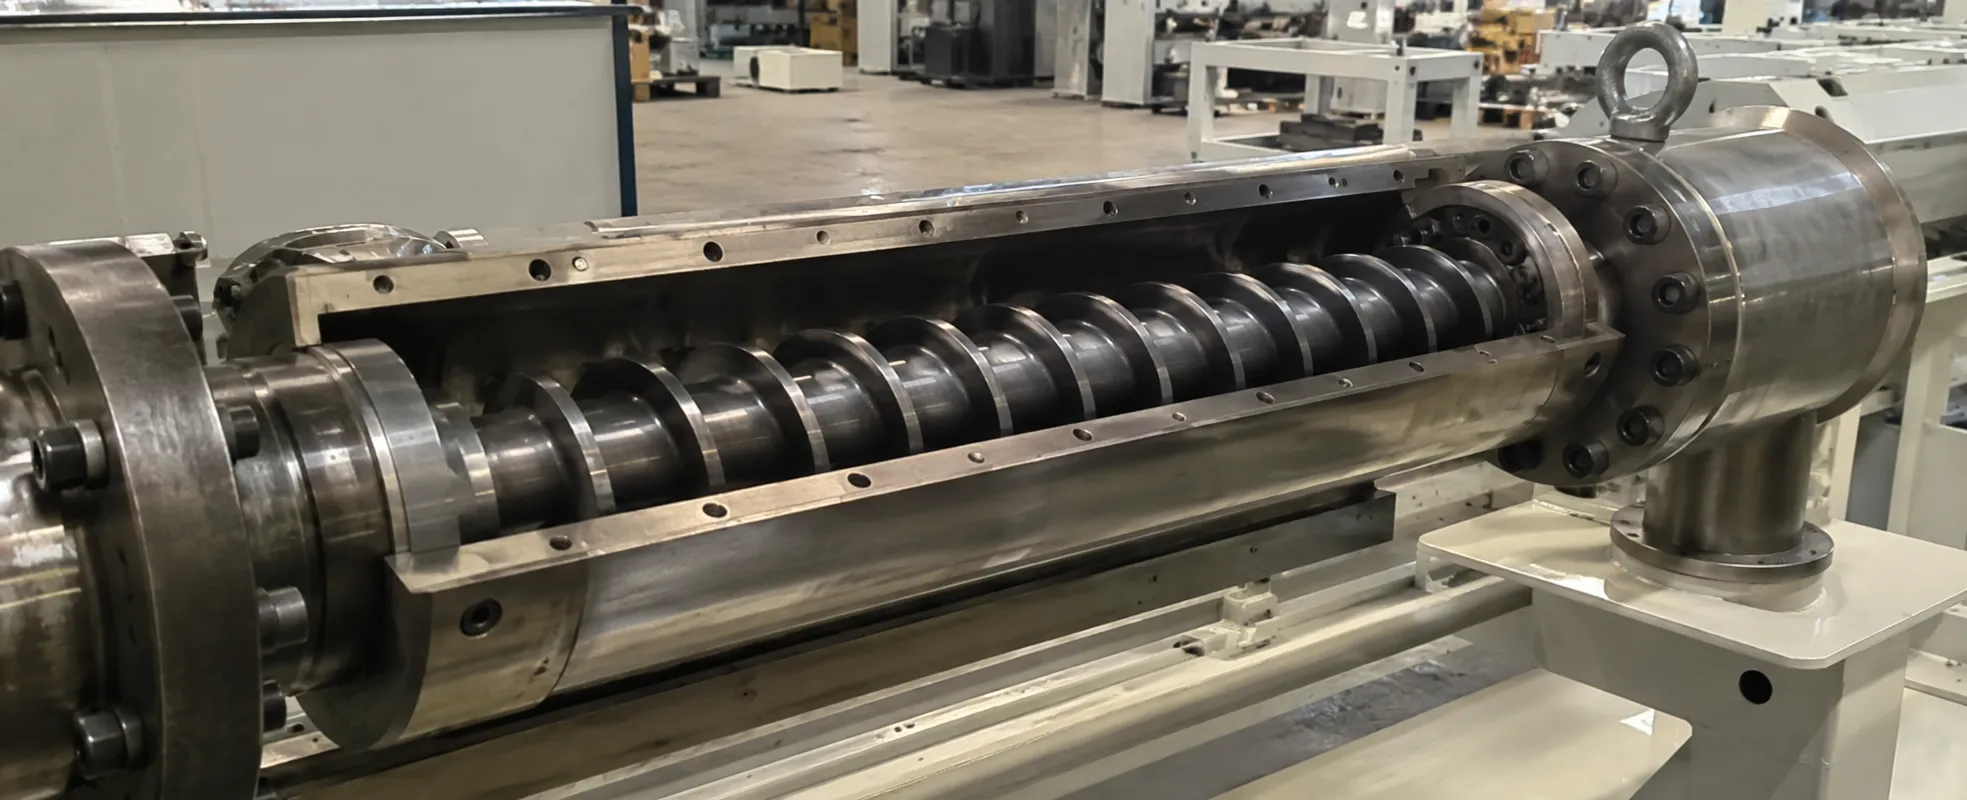
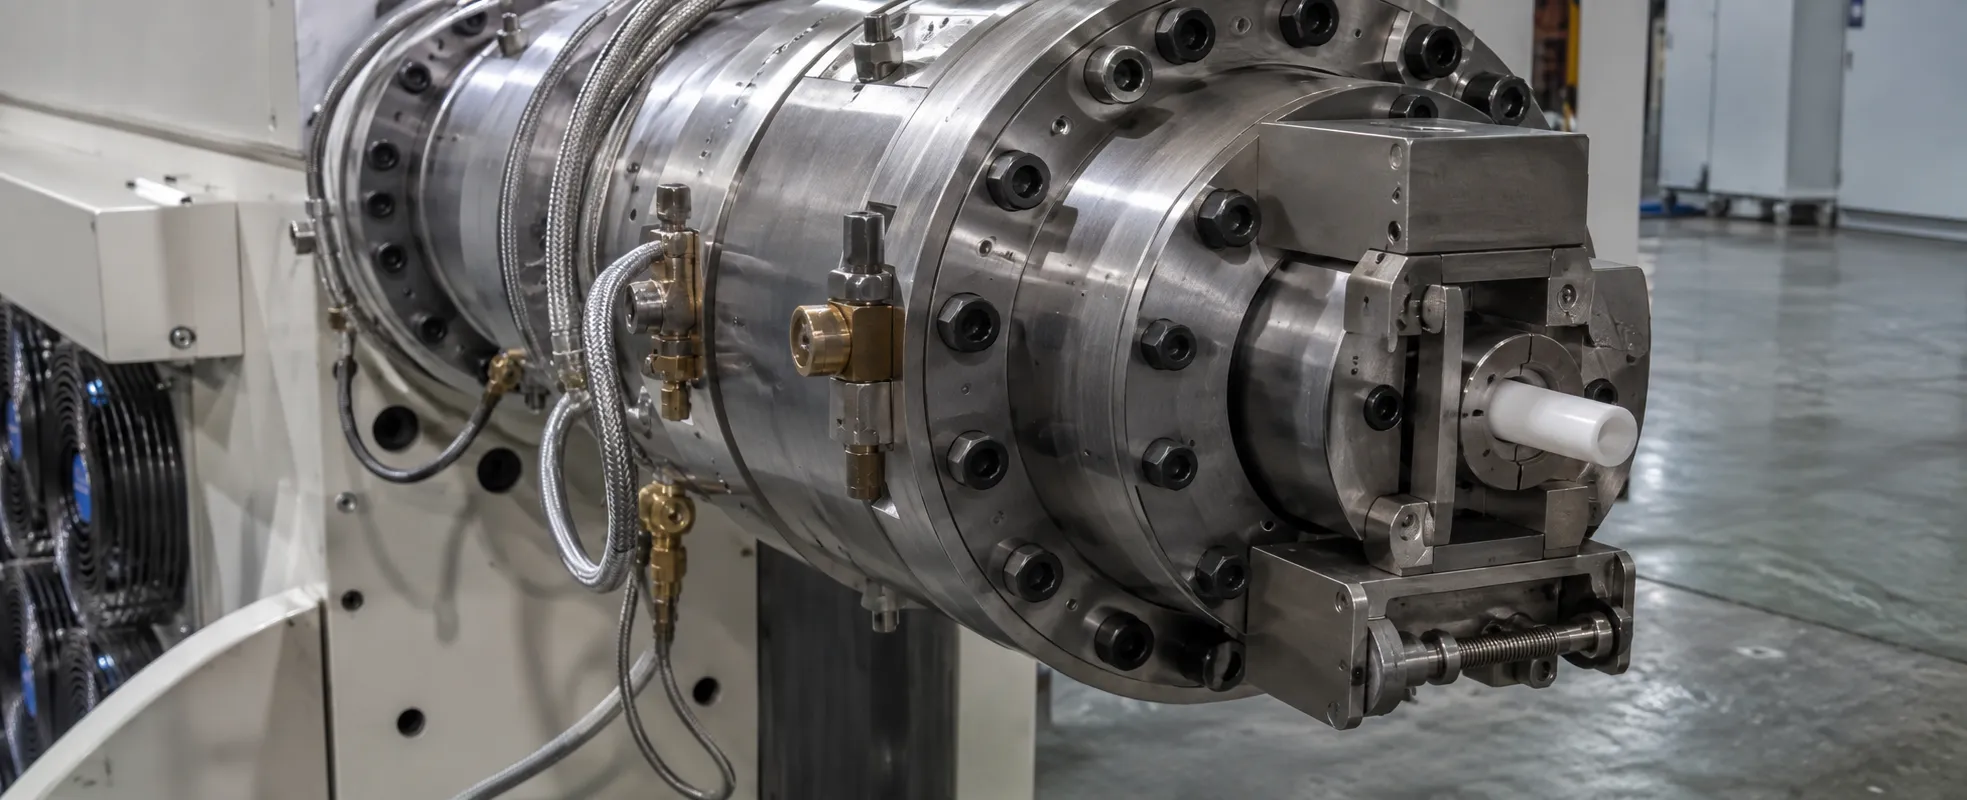
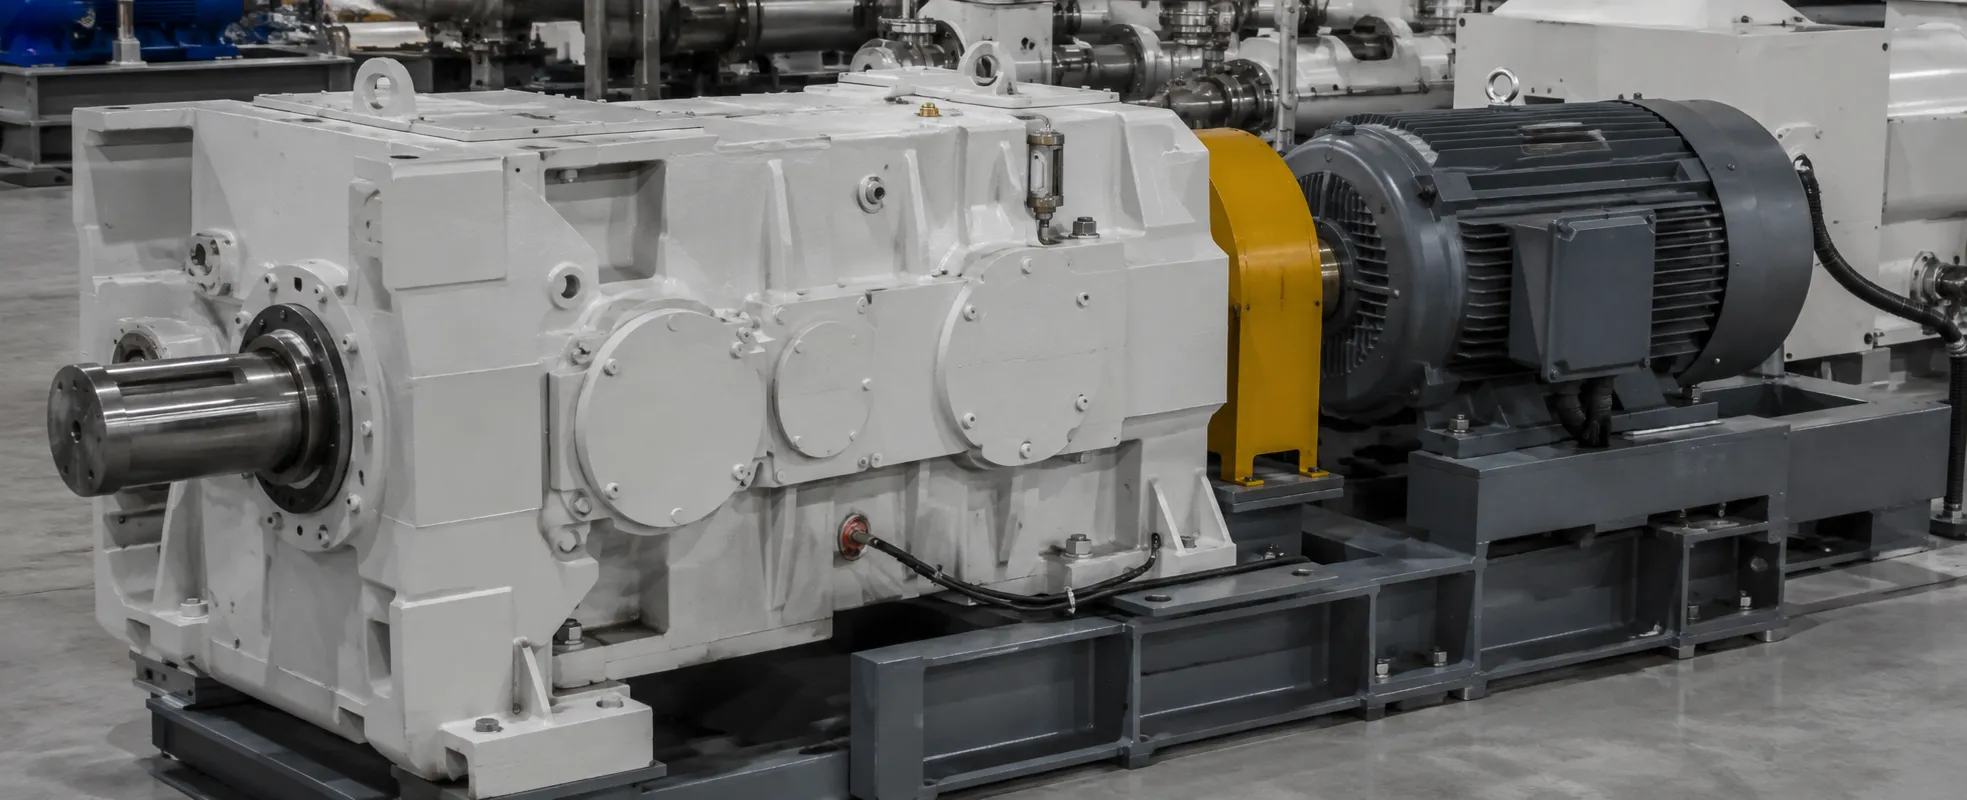
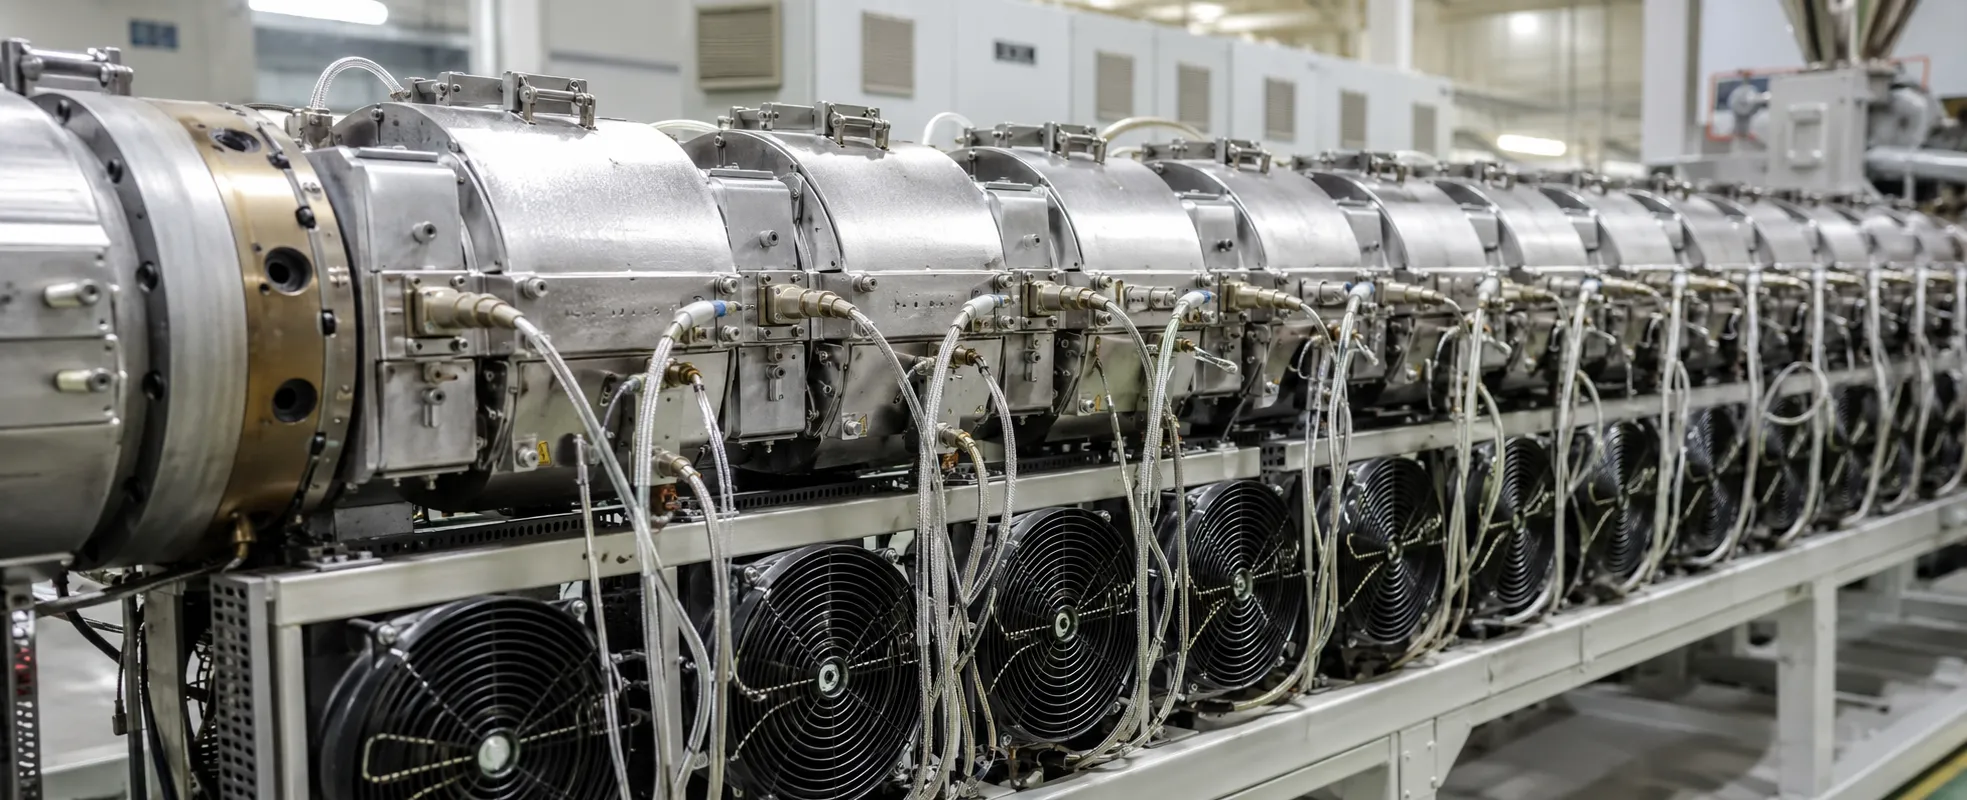
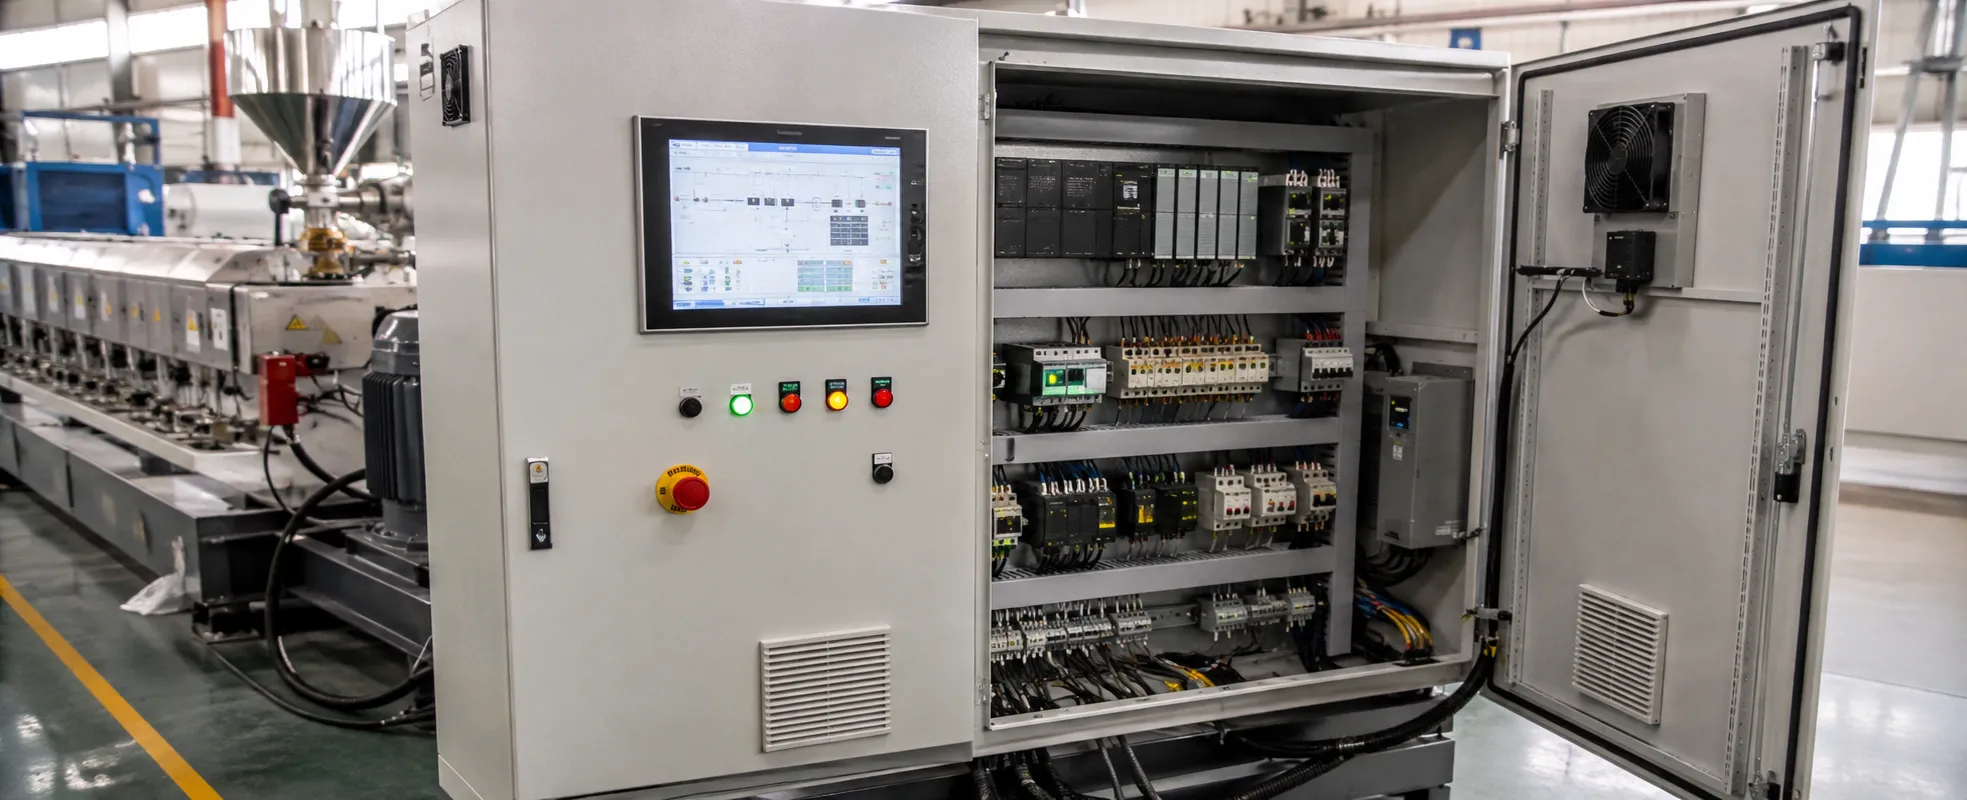
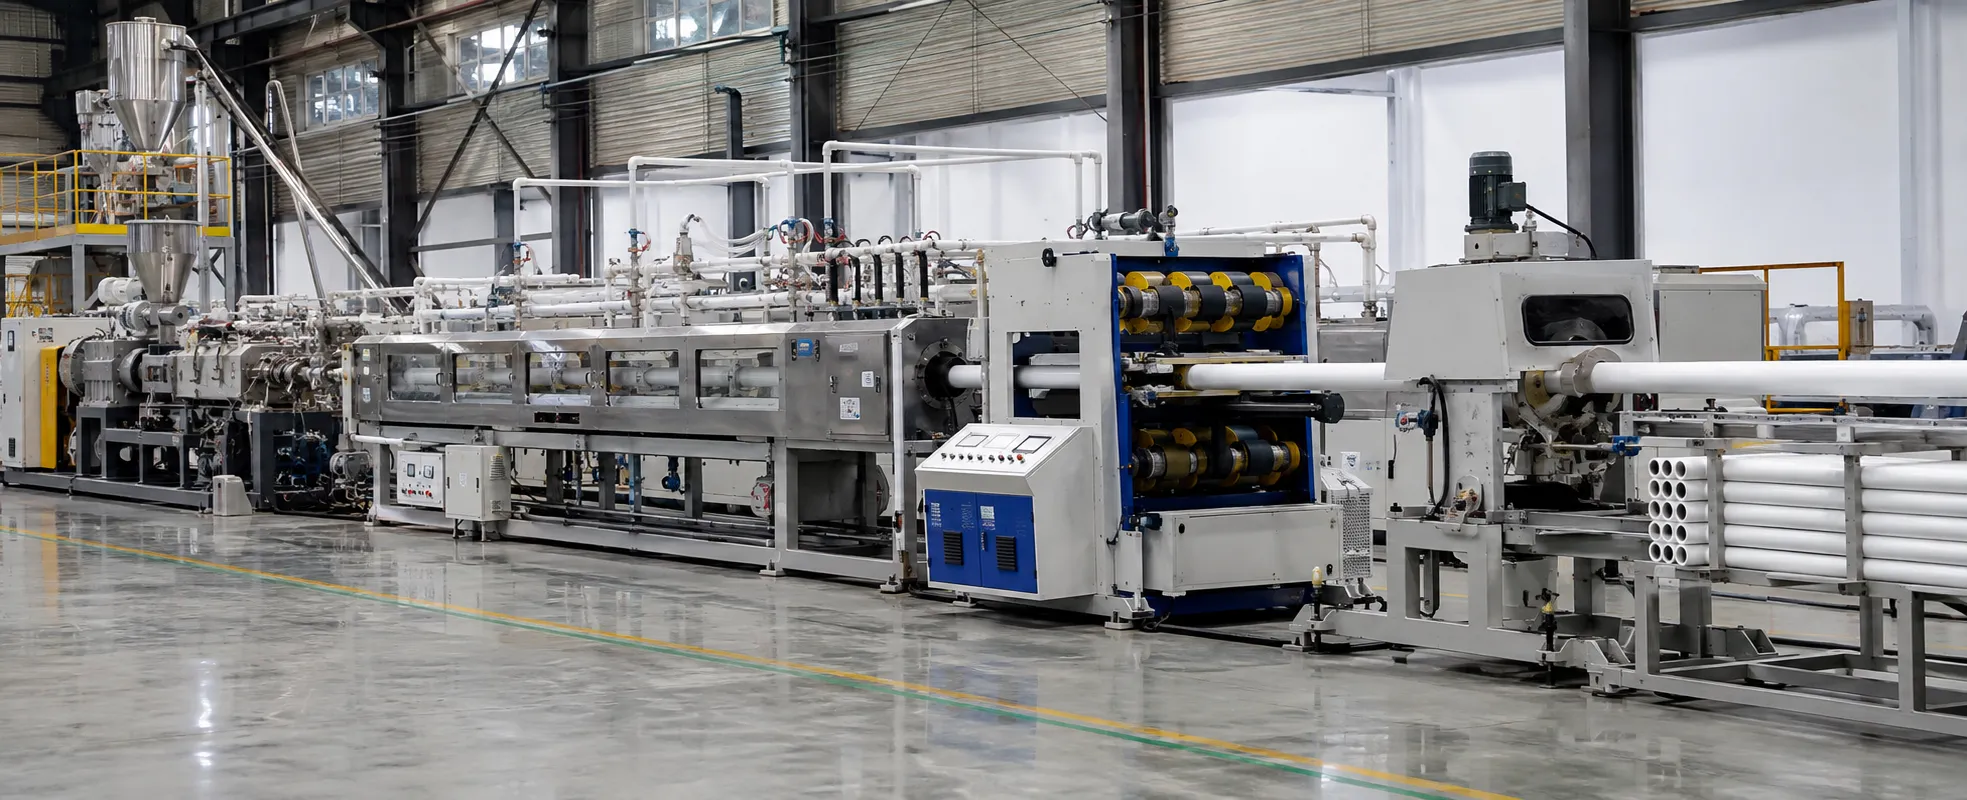
What Is Inside a UET PVC Extruder
Six parts decide whether a PVC line makes money. Here is what we put in each one, and why.
Screw & barrel
42CrMo steel, nitrided to 600 HV or harder, with a low-shear PVC profile. This is the part that decides melt quality, and the part cheap machines get wrong first.
Die head
Flow-balanced, multi-flange design with a quick-clamp base. A good die is the reason your profile comes out straight the first time.
Gearbox
Hardened gears sized for steady torque at low speed. PVC wants slow, steady turning, not high rpm.
Heating & cooling
Ceramic heaters with air cooling on each zone, held by PID loops at ±0.8°C. PVC only has a ~40°C window to work in.
PLC control cabinet
Touchscreen PLC with 120+ saved recipes, melt-break alarm and automatic feed sync. Your operators run it in their own language.
Downstream line
Vacuum tanks, haul-off, saw and stacker matched to the extruder as one line, not bolted-on extras. We commission the whole line and train your crew.
Buyer’s Guide
How to Pick the Right PVC Extruder
Three questions settle most selections. Answer them in order.
1
Start from your material form
Running PVC powder straight from the mixer? A conical twin-screw handles it directly. Feeding pre-made pellets? A single screw gives you the lowest cost per meter.
Powder vs. pellet2
Match the screw to the product
The outside size of your product picks the screw: Ø20–63mm on the UET-50, up to Ø450–630mm on the UET-110. When in doubt, send us a drawing and we will size it for you.
Ø20–630mm coverage3
Check output and plant power
Tell us your target kg/h and your supply, for example 380V/50Hz/3-phase, and we match the motor, heaters and inverter before the machine ships.
kg/h + voltage standard
Working Principle
 1
 2
 3
 4
 5
 6
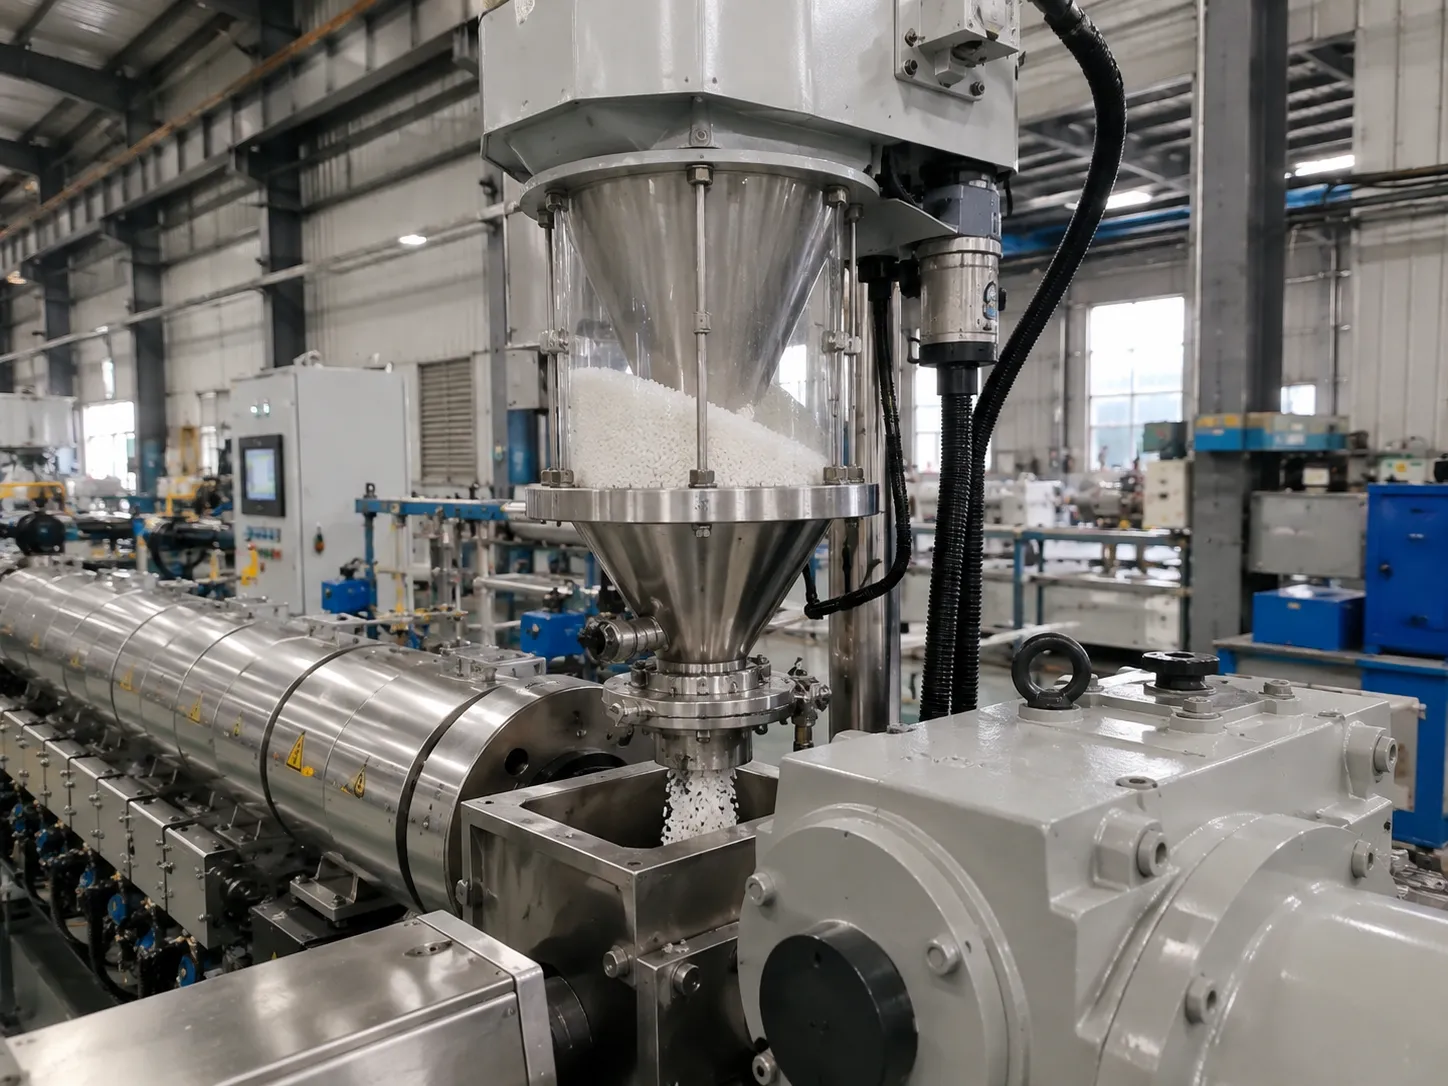
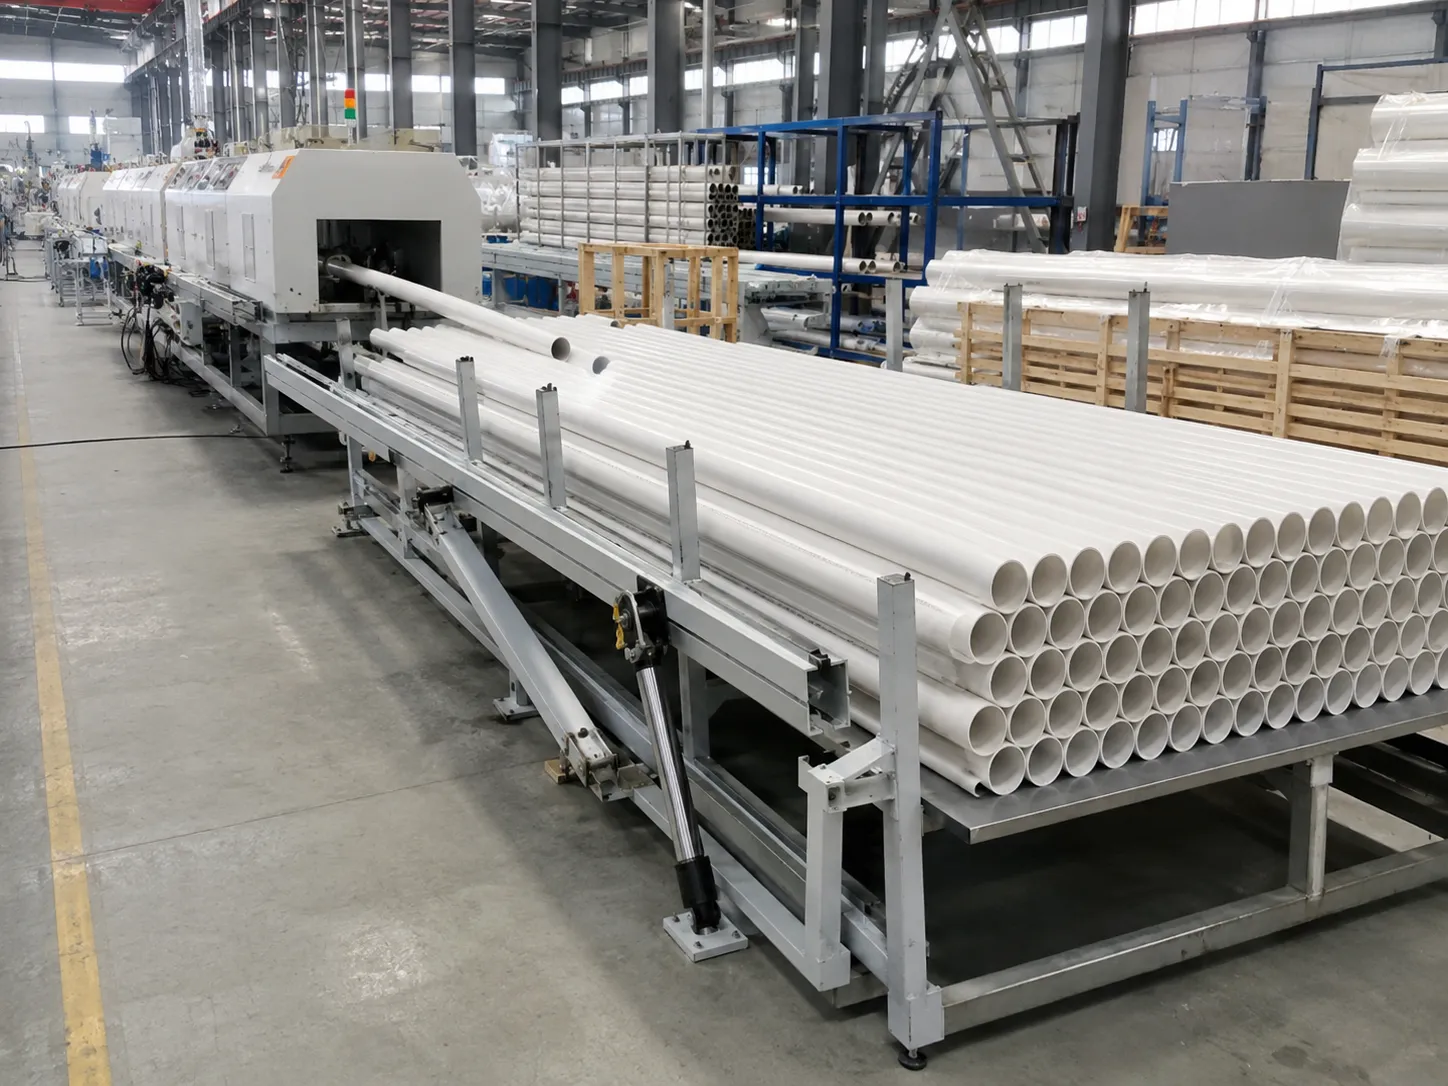
How the Line Runs, Step by Step
Six continuous stages turn PVC compound into finished product.
1
Feeding
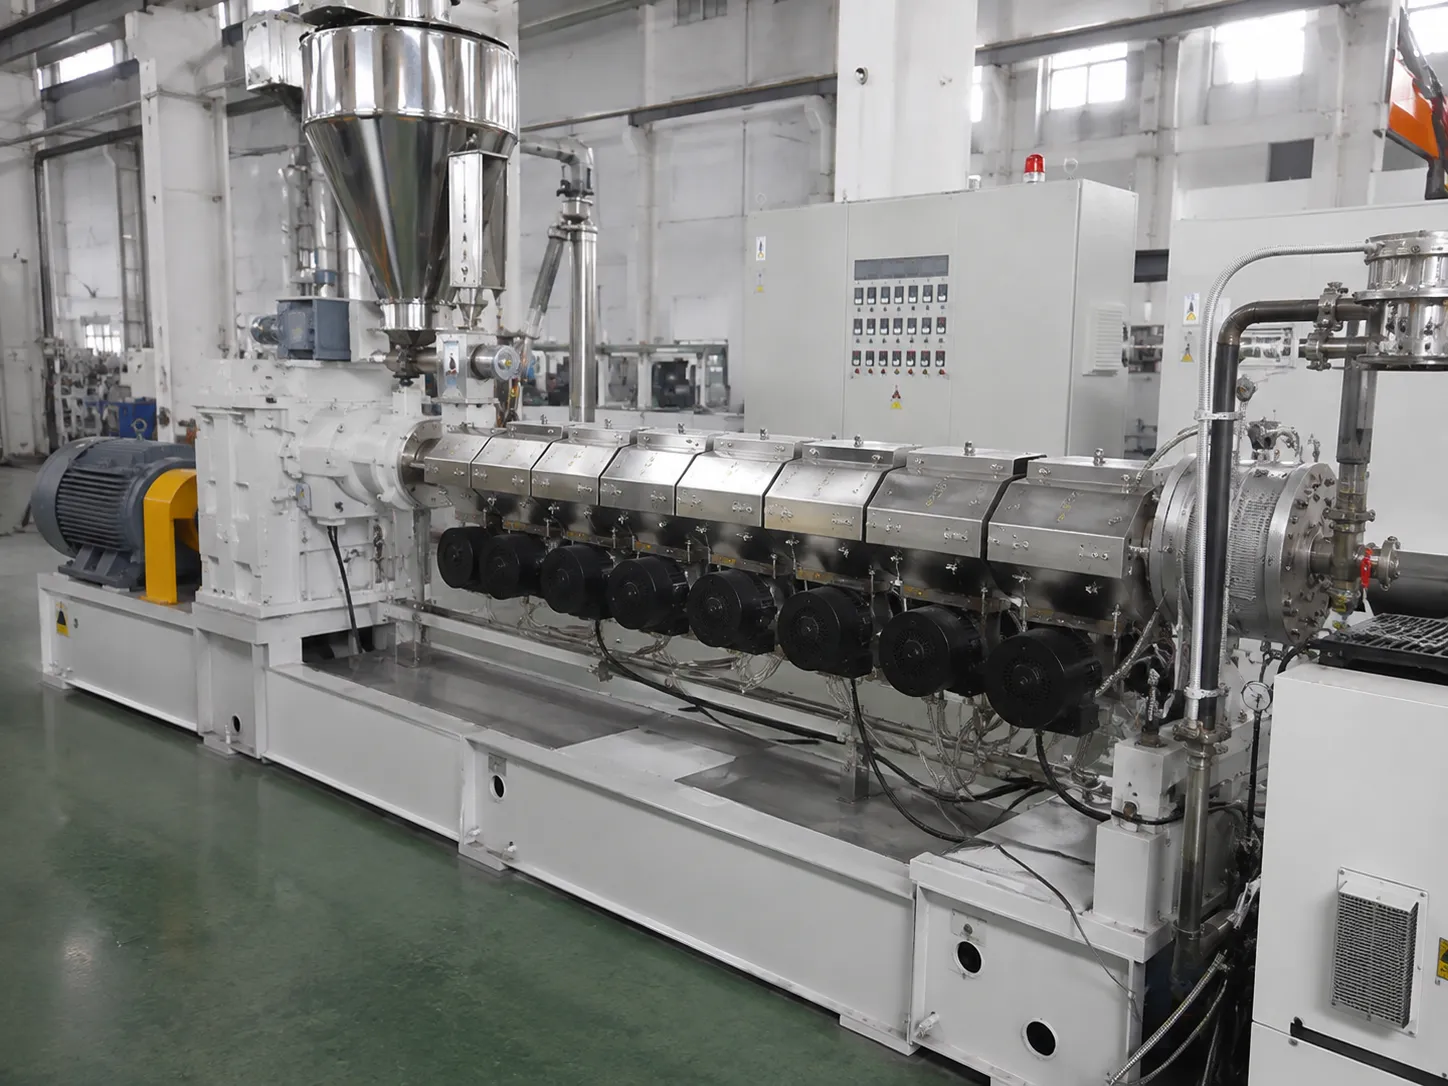
A gravimetric feeder meters powder or pellets into the throat at a controlled rate.
2
Plasticizing
The screw conveys, compresses and melts the compound at 160–200°C across PID zones.
3
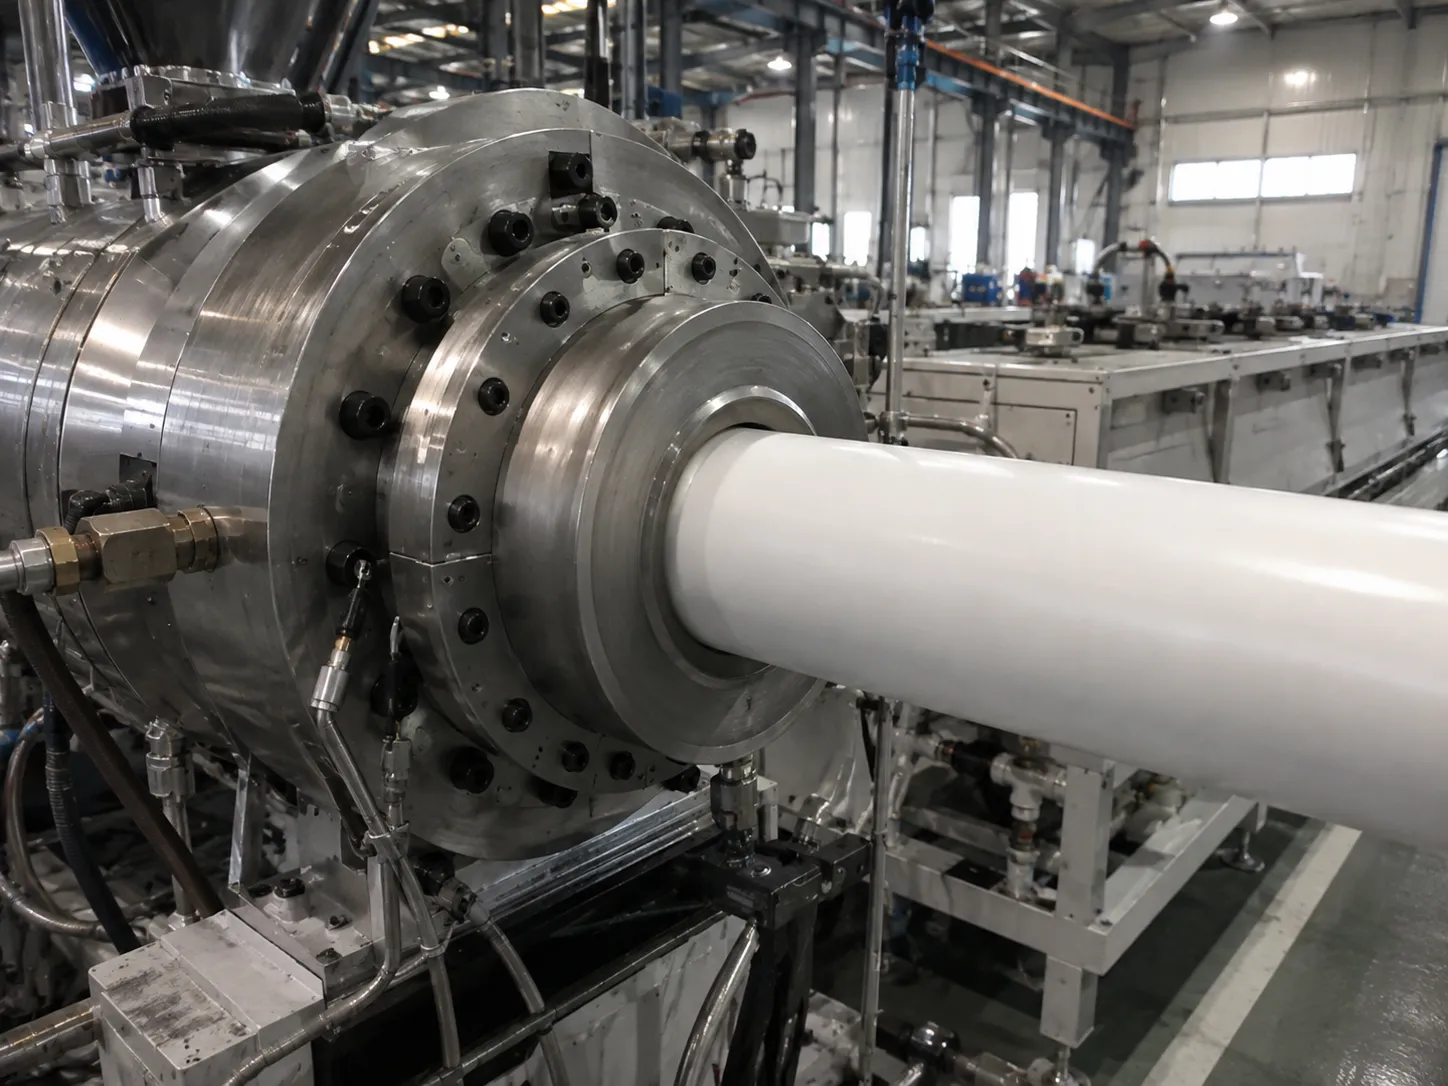
Die forming
Molten PVC passes through a precision die that forms the pipe or profile cross-section.
4
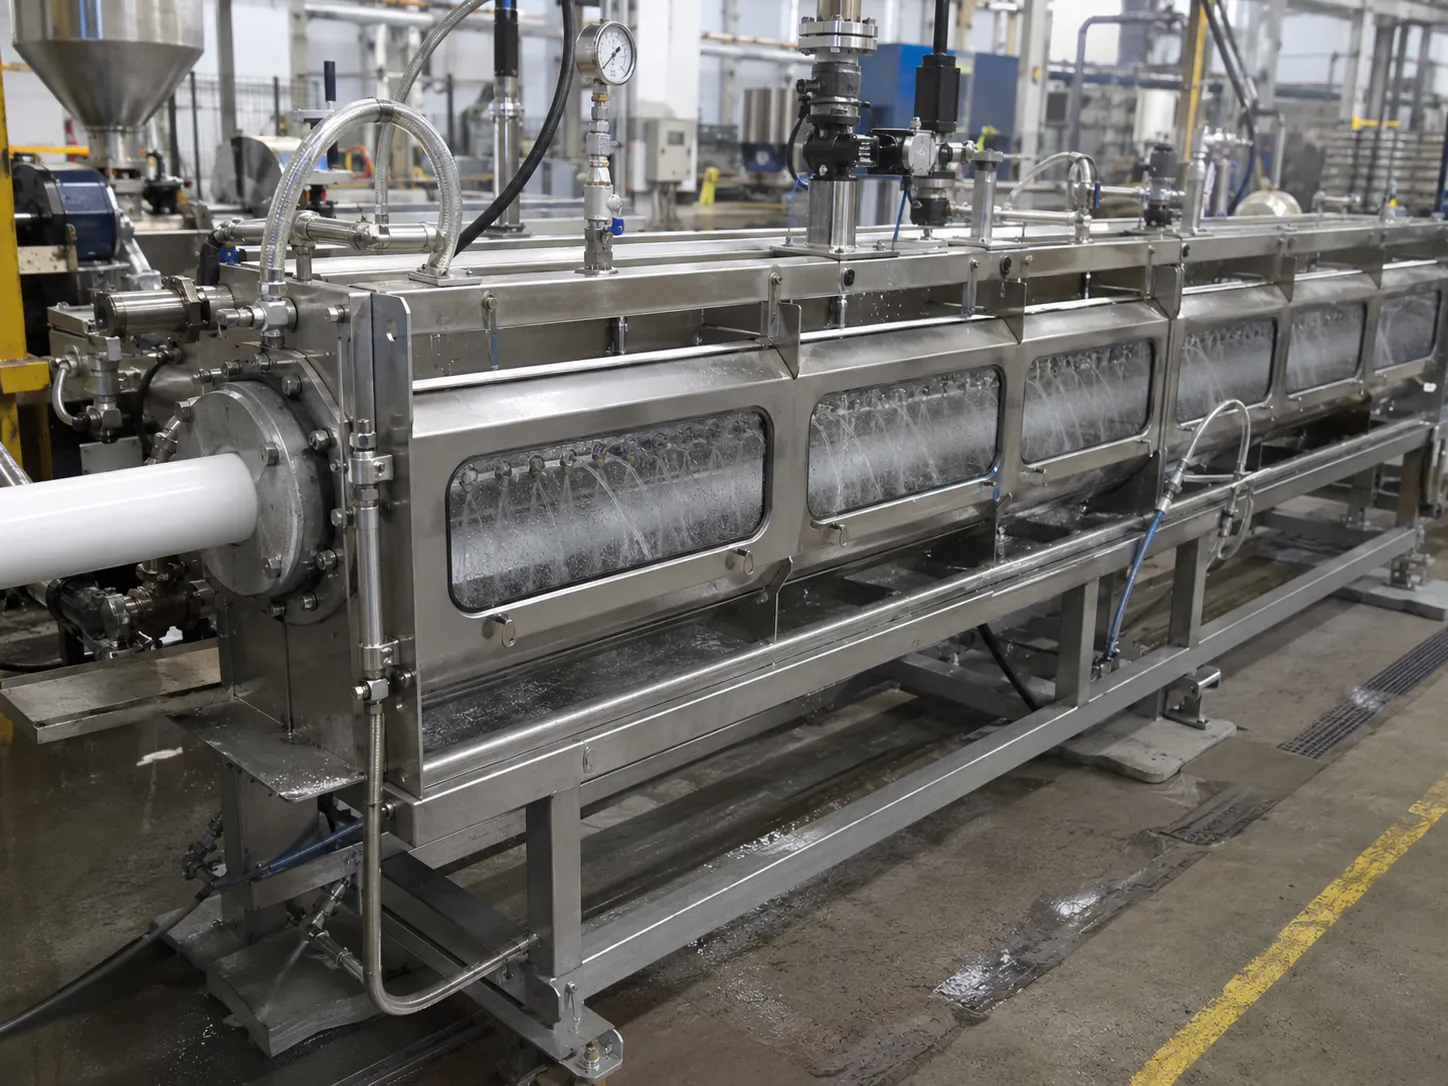
Vacuum calibration
Vacuum tanks with spray cooling lock the outer dimensions while the profile solidifies.
5
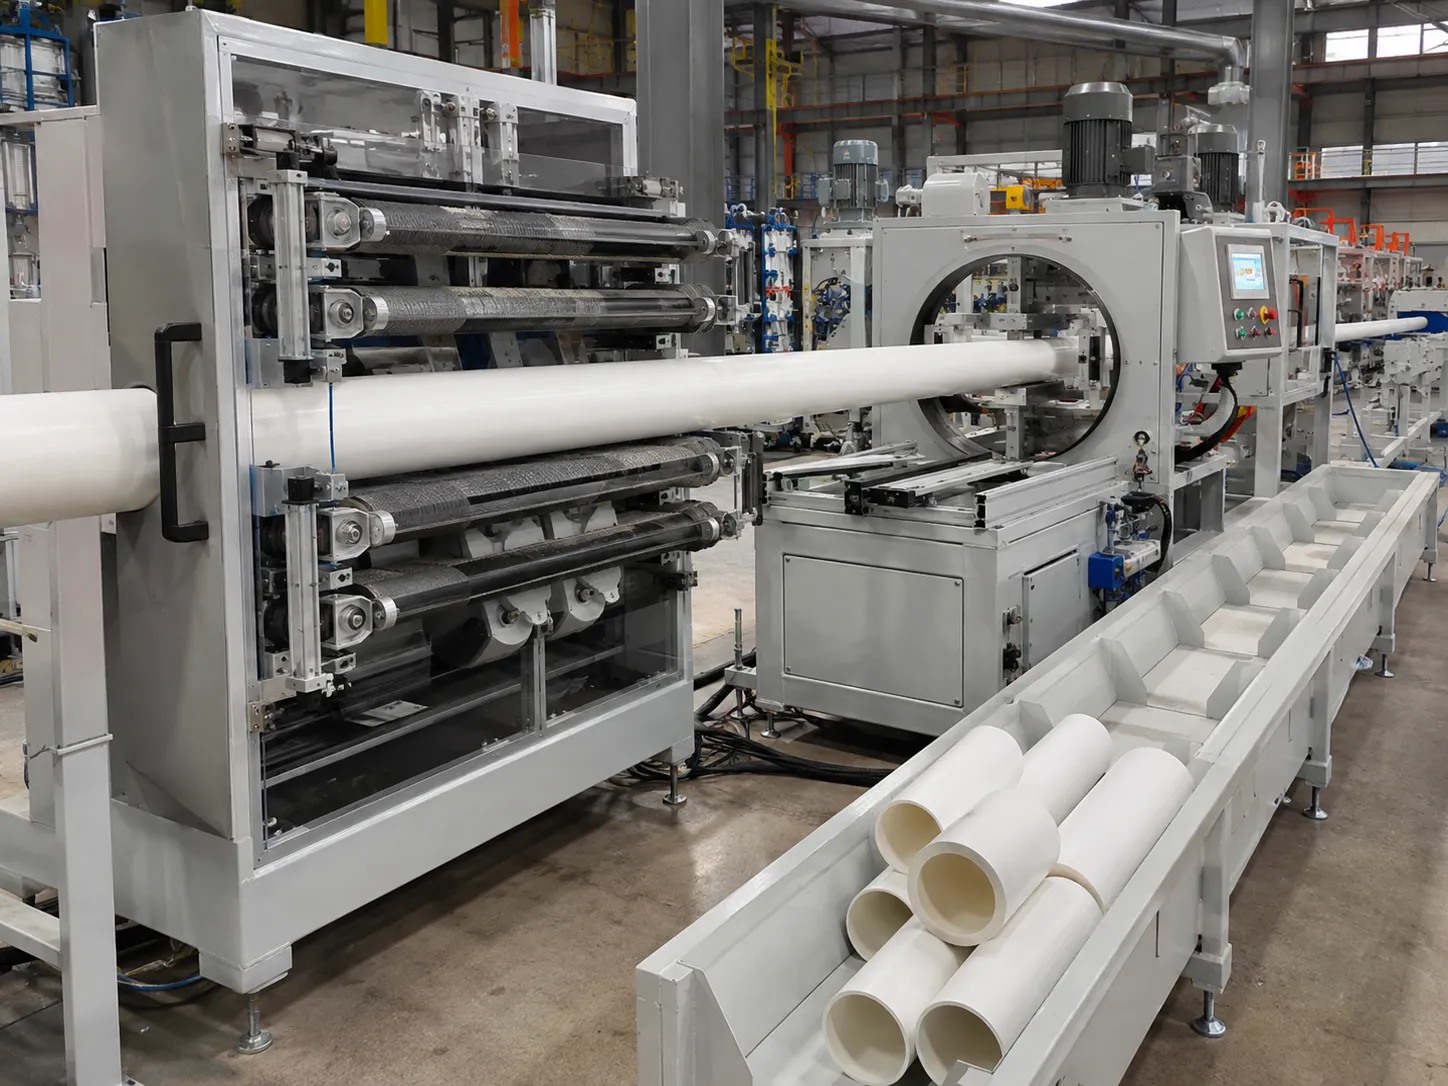
Haul-off & cutting
A synchronized puller and planetary saw hold ±1mm cutting accuracy at full line speed.
6
Stacking & packing
An auto stacker or coiler collects finished product, ready for export packing.
End Products
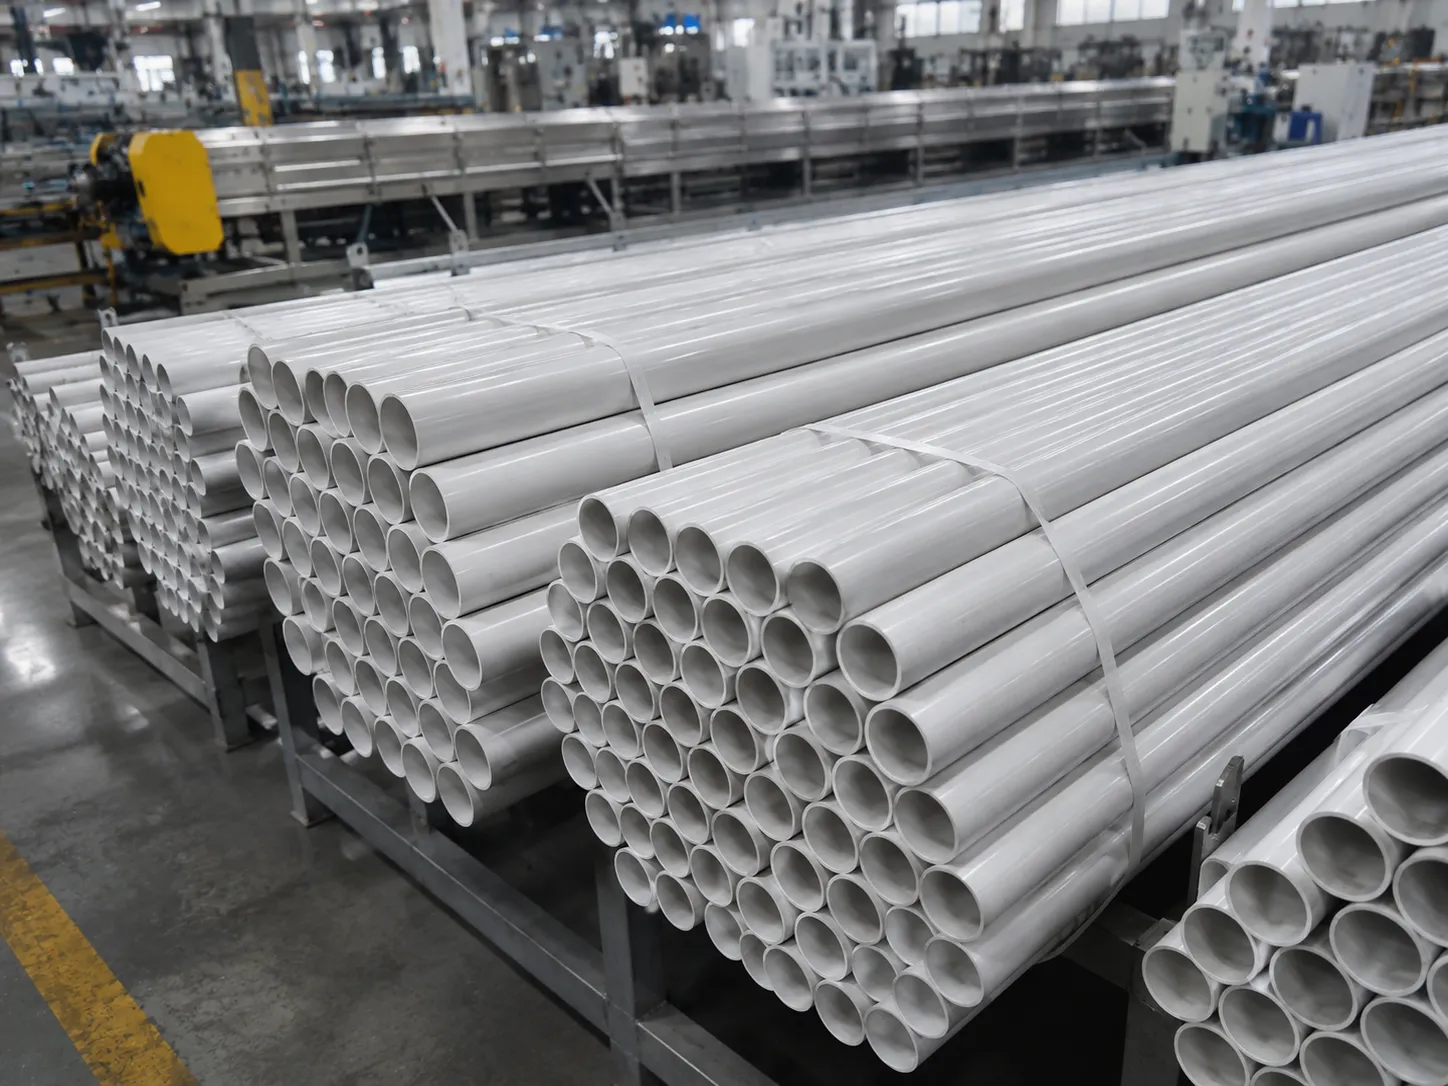
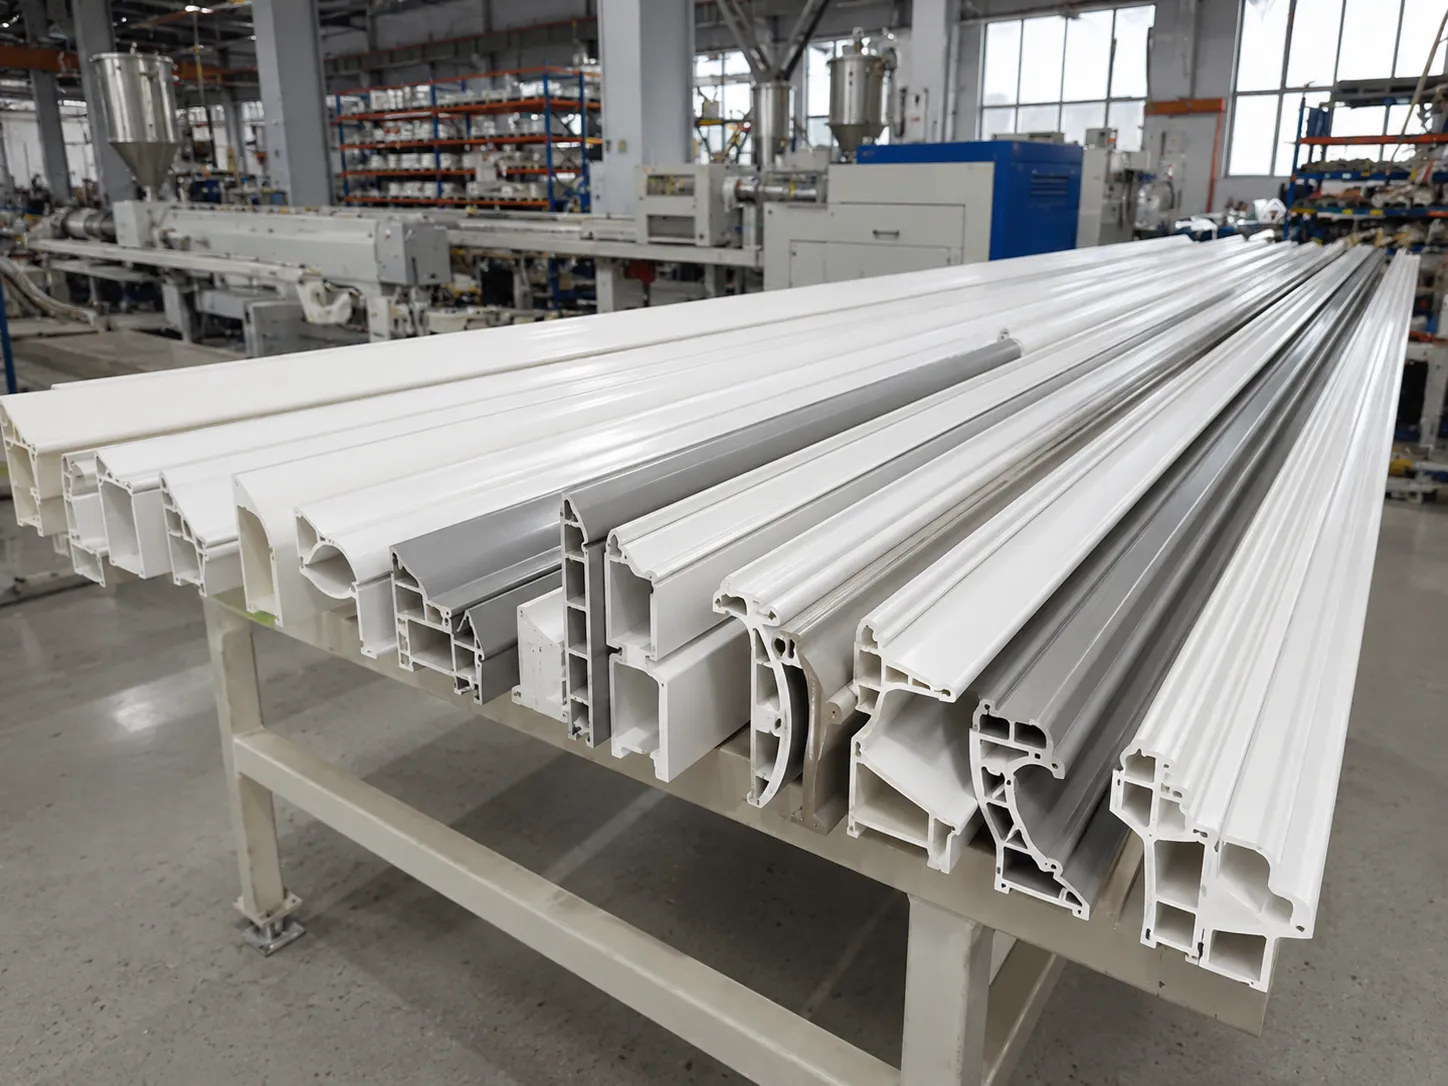
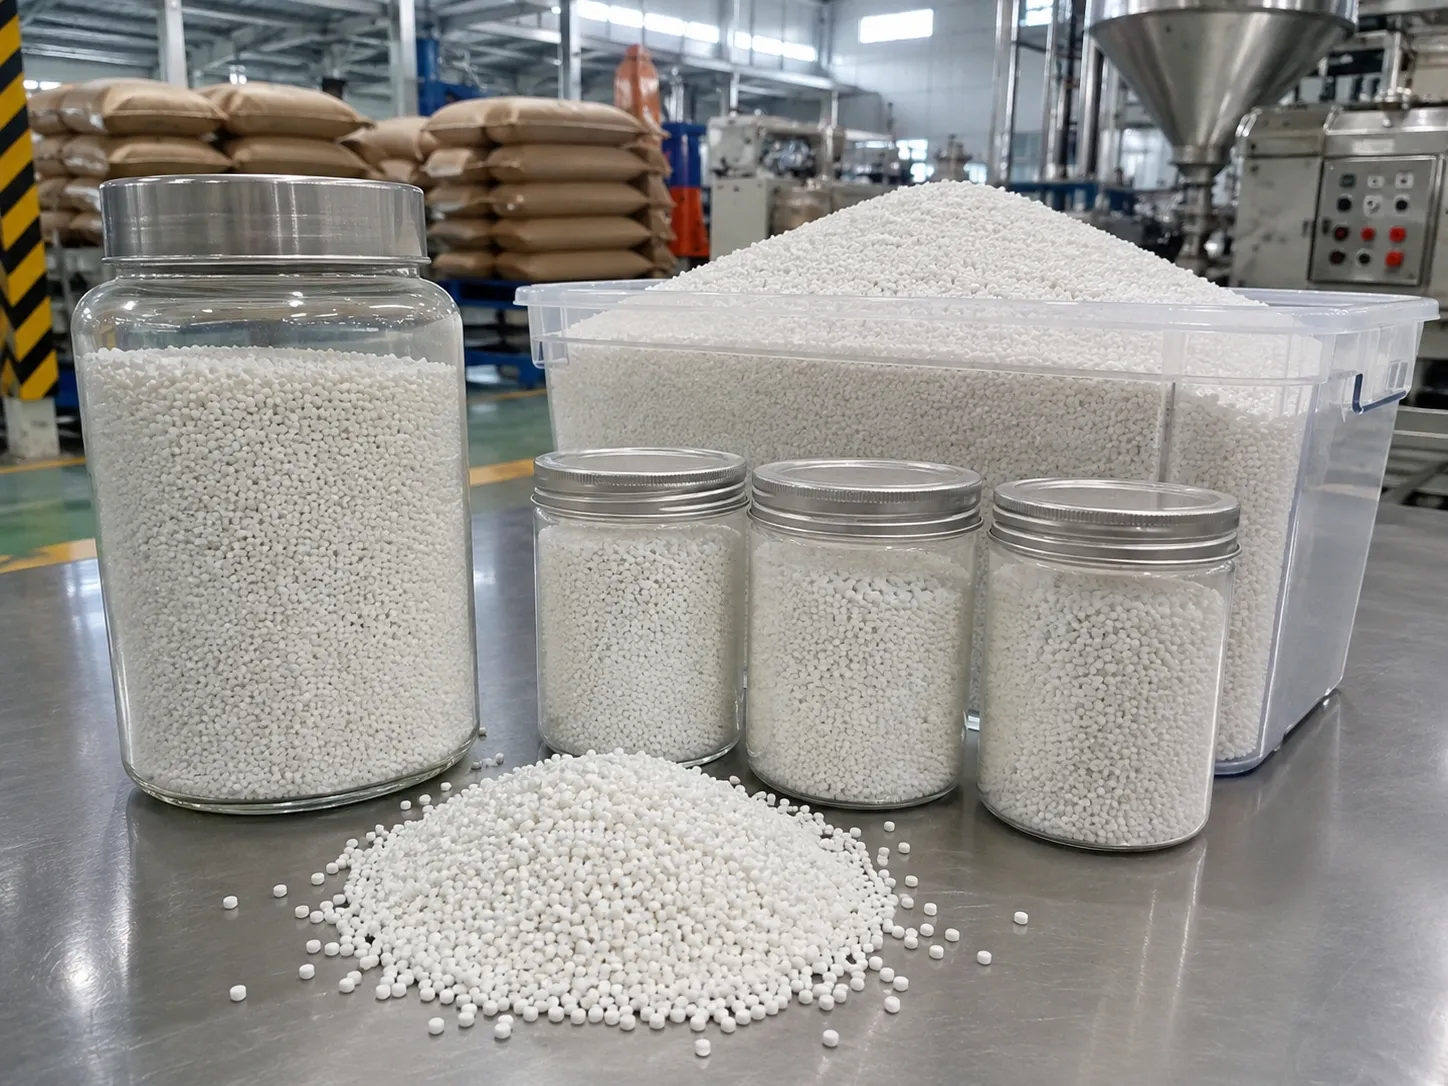
What You Can Run on This Machine
One platform, many markets. Change the die head and downstream and you change product.
Serving construction, electrical, municipal and furniture industries. Related: Single Screw Extruder · Twin Screw Extruder
China PVC Extruder Manufacturer
Why Buyers Source PVC Extruders from UET
We are a factory, not a trading company. That changes what you pay and what you get.
Certified quality
CE and ISO 9001, plus 7+ export certifications. Every machine is test-run with material before it leaves.
In-house machining
Screws, barrels and gearboxes are machined under our own roof, so we control the tolerances and the delivery date.
Global service
We have commissioned lines on five continents. Remote video commissioning or on-site engineer, your choice.
Lifetime support
24/7 engineer response, 2-year core warranty, and spare parts at cost price for as long as you run the machine.
Customer Proof
Customer Success Stories
Verified feedback from manufacturers running UET PVC extruders.
“Eight months of continuous operation without fault. Pipe precision meets municipal standards and capacity is up 25% versus our old equipment. After-sales support is responsive and efficient.”
Leo CarterPlant Production Supervisor
“We compared several suppliers and chose UET. Rigid and foamed PVC plasticizing is excellent, window profiles come out smooth with no secondary sanding, and defect rates dropped sharply.”
Sophia MendezQuality Control Manager
“We bought three UET extruders for our Asian and South American factories. Modular design enables quick switching and operating costs run 12% lower than comparable equipment. Excellent value.”
Jasper HaleGlobal Procurement Manager
Field Reference
Problems We Get Called About, and the Fixes
These are the six calls our service team takes most often, and what we check first.
Black specks / discoloration
Likely causeMaterial sitting too long in a dead spot, or a zone running hot.
FixDrop the affected zone a few degrees, purge and clean the die. The ±0.8°C loops stop it coming back.
Dimensional drift
Likely causePuller speed out of step with the melt, or a leaking vacuum seal.
FixRe-calibrate the die and check the vacuum, then put the haul-off back in closed loop.
Rough / matt surface
Likely causeMelt too cold, or damp compound.
FixRaise melt temperature 5–10°C and dry the compound. Check the feeder for moisture.
Low output
Likely causeWorn screw, bridging at the feed throat, or a dead heater band.
FixMeasure screw clearance, cool the feed throat, test the bands. The melt-break alarm catches this early on UET lines.
Melt fracture (sharkskin)
Likely causeToo much shear at the die land.
FixWarm the die, slow the screw, open the gap. Polish the land if it persists.
Feed blockage
Likely causeDamp or clumped material, or a feed zone running too hot.
FixScreen the material, check the throat cooling water, and balance feed speed against screw speed.
Explore the Lineup
Other Extruders Buyers Usually Look At Next
If a PVC line is not the whole answer, these are the machines that sit next to it in a plant.
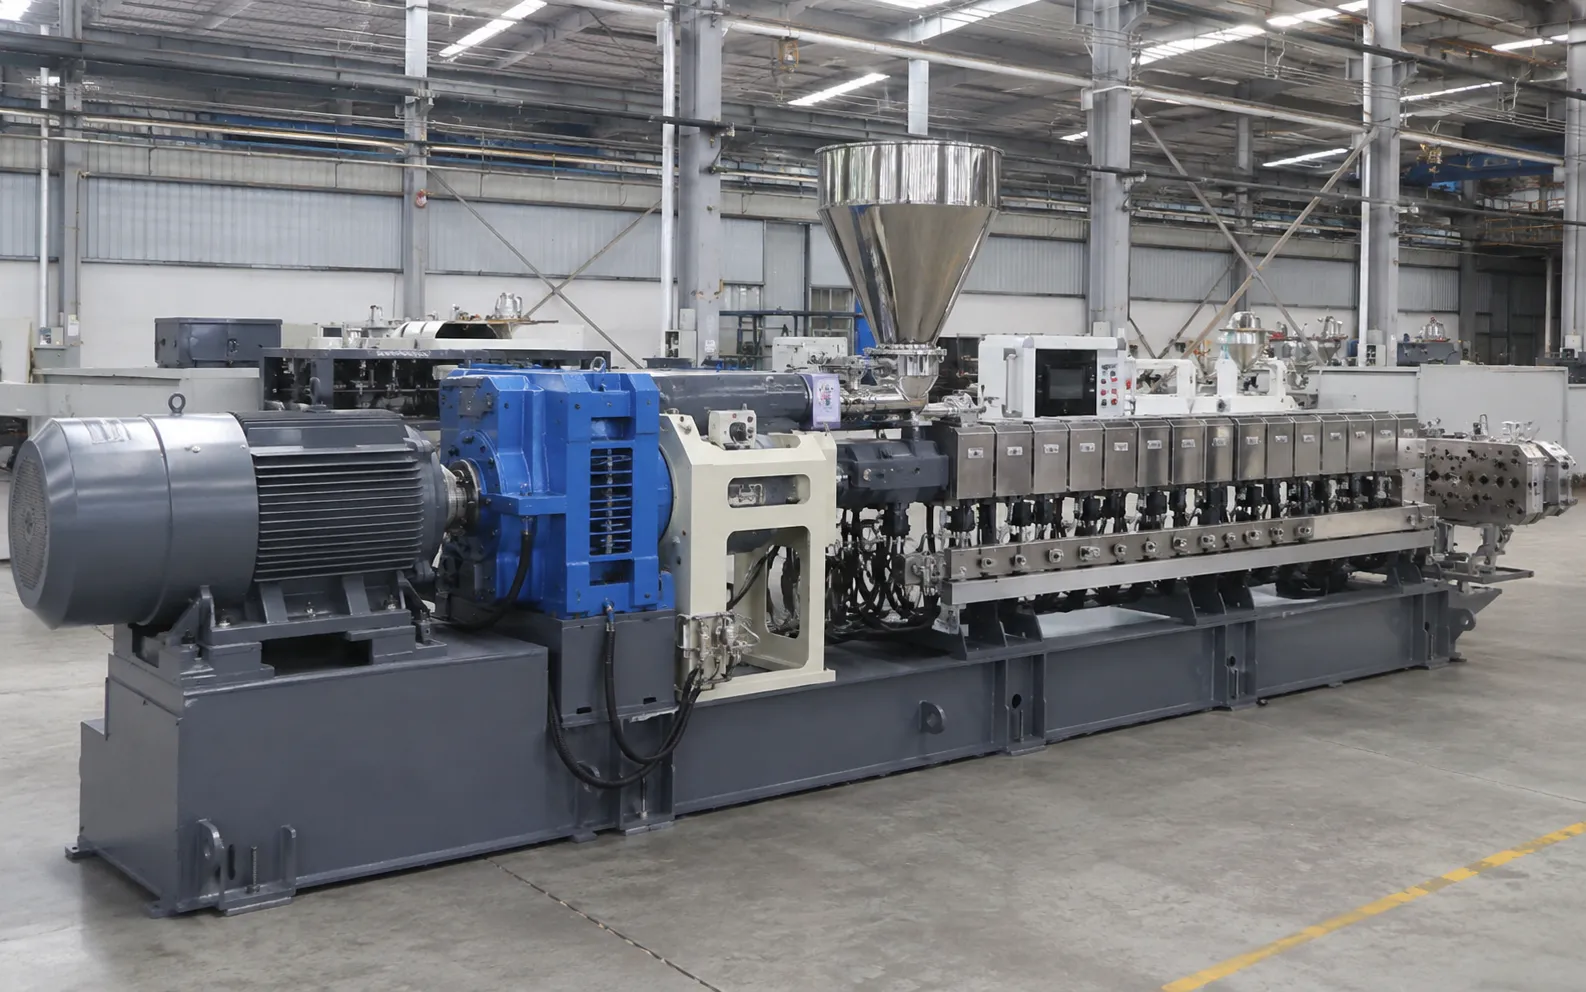
Twin Screw Extruder
Conical and parallel twin screws for PVC powder compound, masterbatch and modified plastics.
View Details
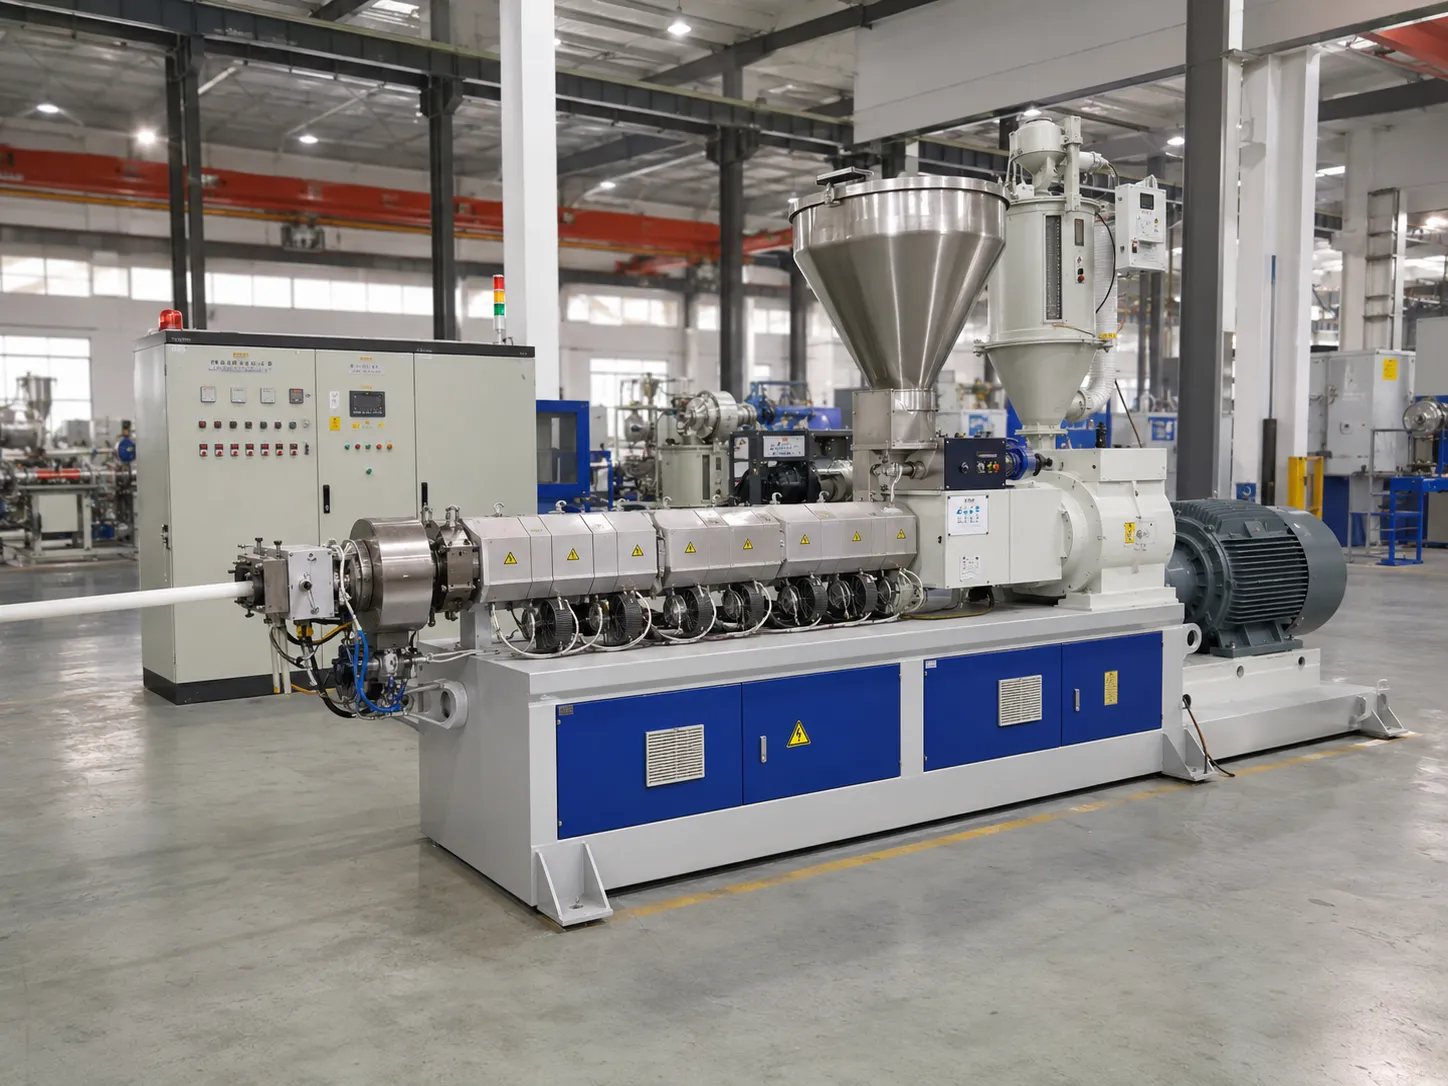
Single Screw Extruder
The workhorse for PE, PP and pellet-fed PVC pipe, sheet and film lines.
View Details
Compounding Machine
High-fill mixing lines for PVC compound and CaCO₃ masterbatch preparation.
View Details
Recycled Plastic Extruder
Two-stage filtering lines that turn post-consumer regrind into saleable product.
View Details
Laboratory Extruder
Bench and pilot scale screws for recipe development before you commit to a production line.
View Details
Filler Masterbatch Extruder
Dedicated lines for CaCO₃ and additive masterbatch at high load.
View Details
Technical FAQ
PVC Extruder: Frequently Asked Questions
Straight answers about the machine, from the engineers who build it.
How does a PVC extruder work?
A PVC extruder feeds compound (powder or pellet) into a heated barrel where a rotating screw conveys, compresses and melts it at 160–200°C. The melt is pushed through a die to form the target shape, then sized in a vacuum calibration tank, cooled, hauled off and cut to length.
What makes a PVC extruder different from a general-purpose single screw extruder?
A PVC extruder runs at lower screw speed with a gentler compression ratio and more heating zones, keeping the melt inside PVC’s narrow 160–200°C window. Its screw and barrel are nitrided to resist HCl corrosion. General-purpose extruders run faster with higher shear, which would overheat and degrade PVC.
Why is temperature control so critical in a PVC extruder?
PVC has a narrow processing window and degrades above ~200°C, releasing HCl and causing discoloration or black specks. UET’s closed-loop PID control holds ±0.8°C across every heating zone of the PVC extruder, keeping the melt stable and degradation-free.
What products can a UET PVC extruder produce?
Rigid and flexible PVC pipes from 20 to 630mm, window and door profiles, wall panels and foamed boards, electrical conduits, decorative trims, and PVC compounds/pellets. Switching products mainly requires changing the die head and downstream auxiliaries.
How much output does a UET PVC extruder deliver?
The UET-50 delivers 50–100 kg/h up to the UET-110 at 500–800 kg/h. Actual output varies with formulation, die design and downstream equipment; guaranteed output is confirmed in every proposal.
Can a PVC extruder process recycled PVC?
Yes, within limits. Recycled PVC with stable melt flow can be blended with virgin material; for high regrind ratios we recommend an adjusted screw geometry and melt filtration on the PVC extruder. Share your regrind percentage and we will specify the right configuration.
How long does a PVC extruder screw last and what maintenance does it need?
The nitrided 42CrMo screw (≥600 HV) and hardened barrel resist PVC’s corrosive melt for years of service. Routine PVC extruder maintenance: clean the die at changeover, check heater bands and thermocouples, and follow the gearbox oil schedule.
What auxiliary equipment connects to a PVC extruder to form a complete line?
A typical line adds a die head, vacuum calibration tank, cooling section, haul-off, cutter and stacker to the PVC extruder; compounding lines may also add mixers and auto loaders. UET supplies complete turnkey lines with installation, commissioning and operator training.