20+ Years Extruder Manufacturing Expert
High-Precision Triple Screw Extruder for High-End Compounding
Engineered for multi-component and high-fill materials — 98%+ dispersion uniformity, 20% lower energy consumption and 30% longer stable operation versus conventional twin screw lines. Intelligent control lets new operators reach proficiency after simple guidance.
- CE Certified
- ISO 9001:2015
- RoHS Compliant
- REACH Certified
- SGS Verified
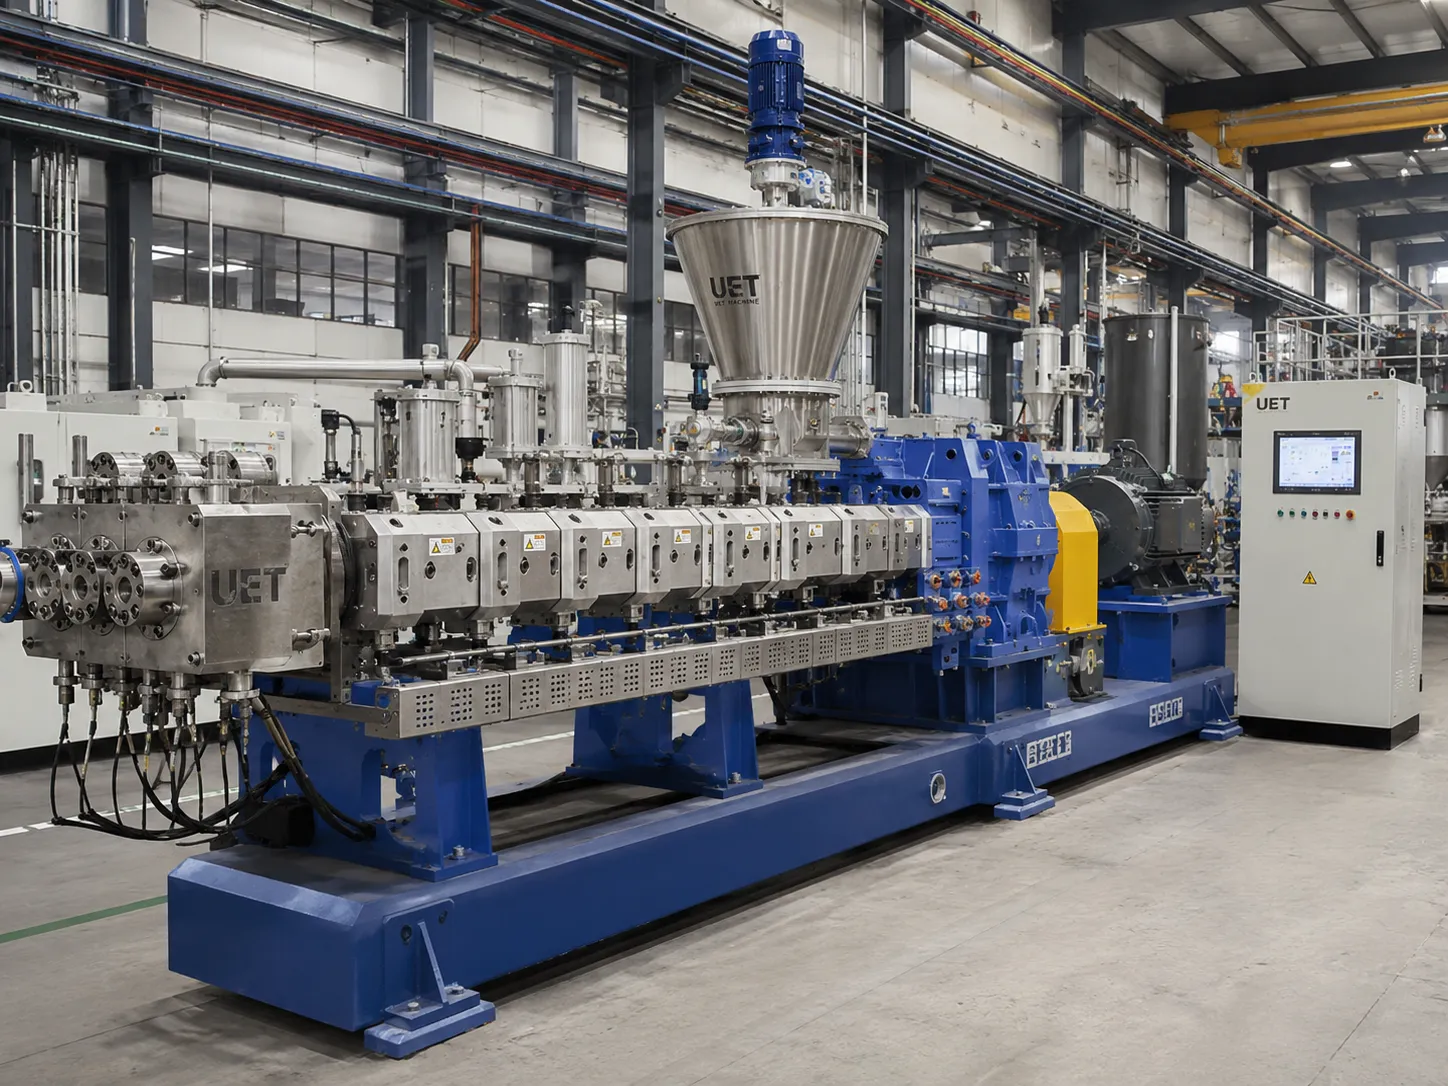
±1.5°C Melt Control
Triple Meshing
98%+Dispersion Uniformity
0.02mmScrew Machining Precision
75%Max Filler Ratio
99.9%Operation Stability Rate
The Basics
What Is a Triple Screw Extruder?
A plain-English definition before you compare models, prices and suppliers
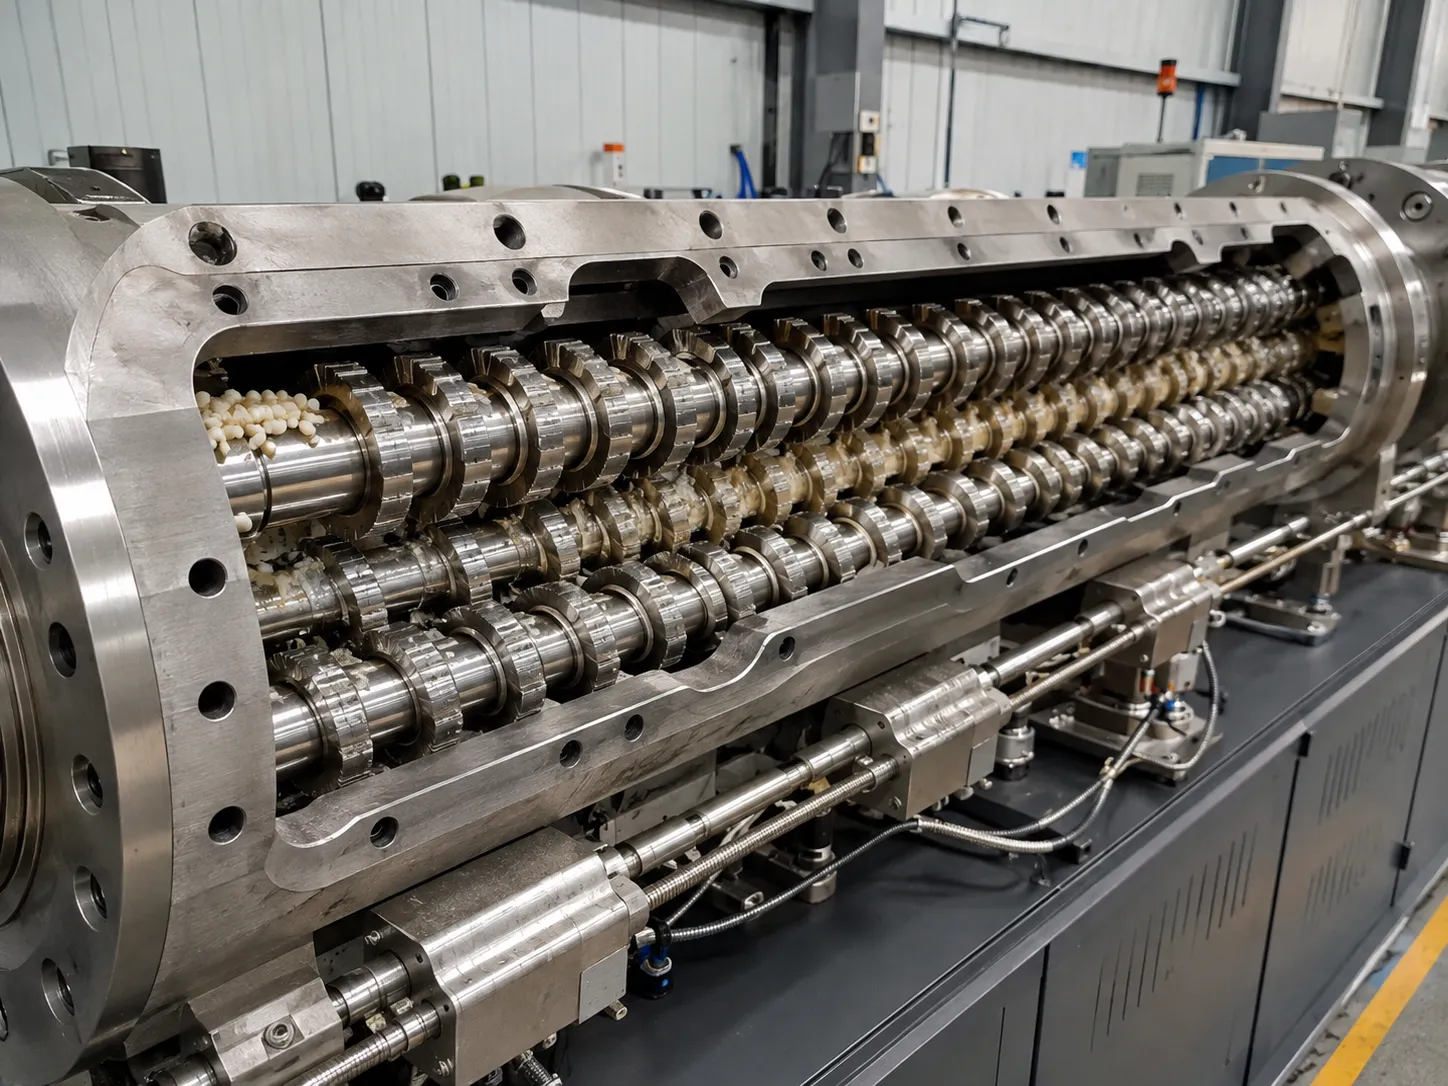
A triple screw extruder is a compounding machine with three co-rotating, intermeshing screws running side by side in one barrel. Line it up against a twin screw and the difference shows immediately: the third screw opens a second meshing zone, so the melt gets twice the shear, twice the surface renewal and roughly 40% more free volume for feeding powders.
What does that buy you on the shop floor? More kg/h at the same screw diameter, a melt temperature that stays inside ±1.5°C, and fillers dispersed fine enough for color-critical and medical-grade work. Plants running high-fill masterbatch, PLA/PBAT and cable compounds are the ones switching to triple screw fastest.
Screw arrangement3 co-rotating, intermeshing screws
Meshing zones2 (twin screw has 1)
L/D ratio26–85, modular barrel
Output range50–3,300 kg/h (UET-29 to UET-92)
Core Advantages
Why a Triple Screw Extruder Outperforms Twin Screw
Six numbers we log on every factory test run — the same figures your acceptance test will check
25% Better Dispersion
Triple meshing structure delivers superior distributive & dispersive mixing versus twin screw systems — consistent quality batch after batch.
20% Energy Savings
Optimized screw geometry and efficient heat transfer cut specific energy consumption — saving $8,000+ per year on electricity at mid-range output.
30% Longer Uptime
Enhanced mechanical stability and reduced wear extend continuous running time after startup, maximizing throughput and ROI.
75% High-Filler Capacity
Stable processing at 60–80% filler loading (CaCO₃, talc, glass fiber) while retaining excellent dispersion and mechanical properties.
±1.5°C Melt Control
Independent zoned heating/cooling with PID control protects heat-sensitive resins such as PLA, PBAT and medical-grade polymers.
Intelligent Operation
Recipe-based control system lets new operators reach proficient operation after simple guidance — lower labor cost, fewer errors.
Product Series
Triple Screw Extruder Models
Lab bench to 3.3 t/h production — pick the platform, then tune the configuration
High Torque Series
Large-scale continuous production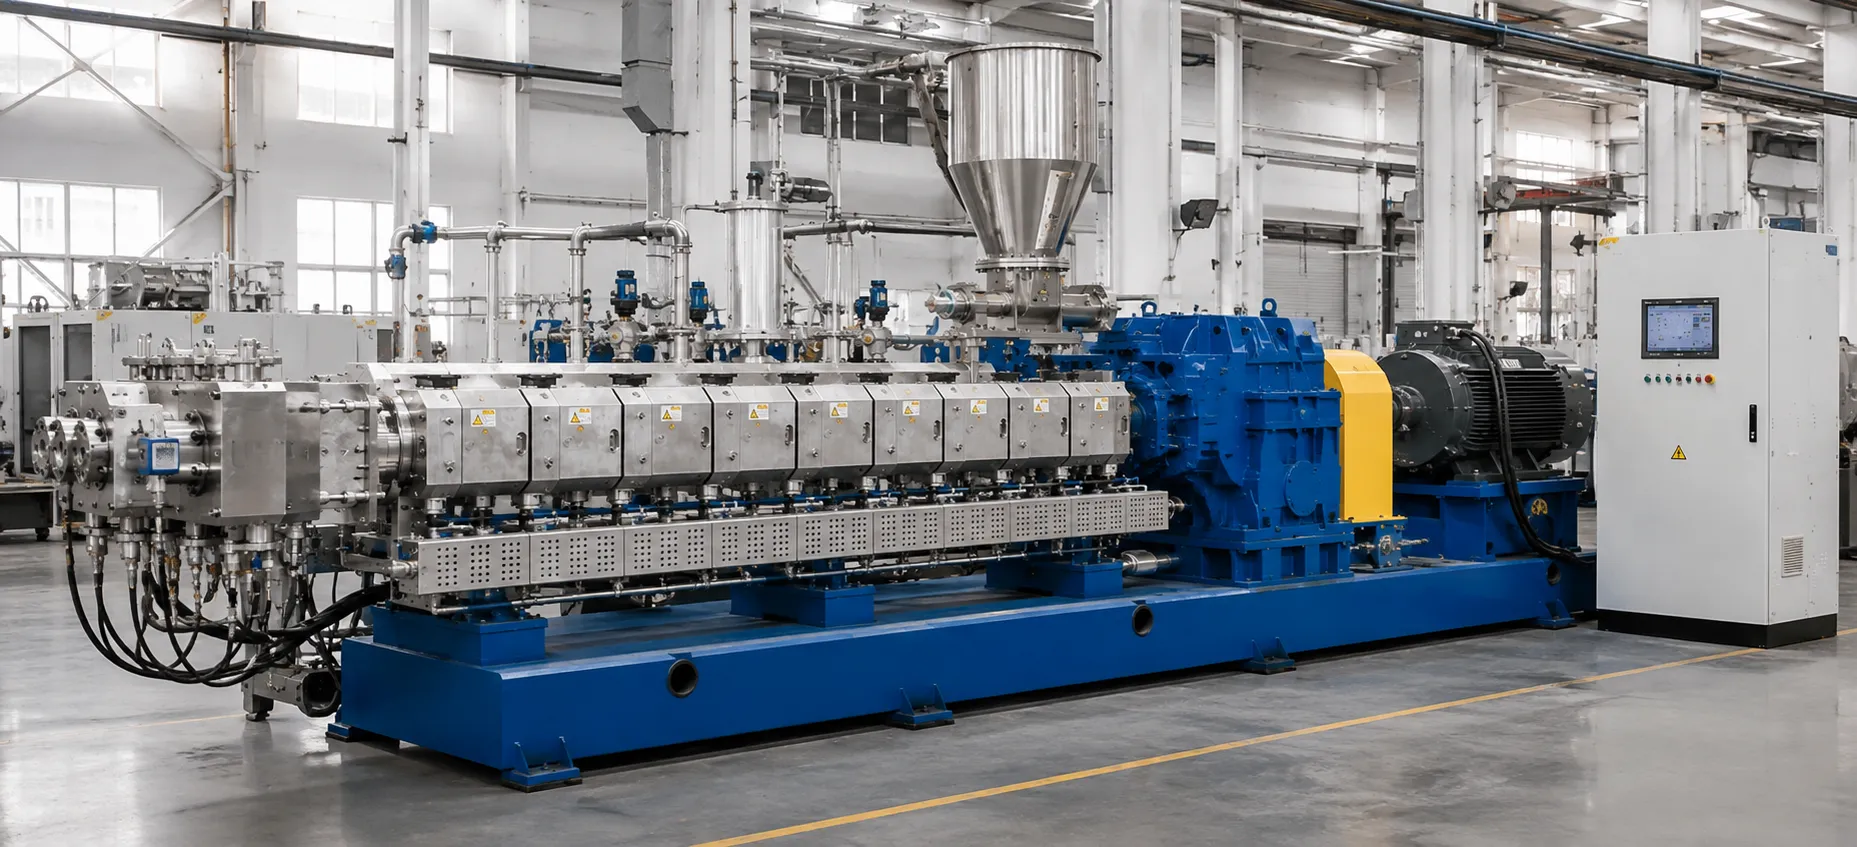
For glass-fiber filled materials, masterbatch and biodegradable plastics at industrial scale.
- Output 550–3,300 kg/h · 550–650 rpm
- High-torque gearbox, low-shear design
- 30% better mixing uniformity
Composite Series
Flexible multi-variety production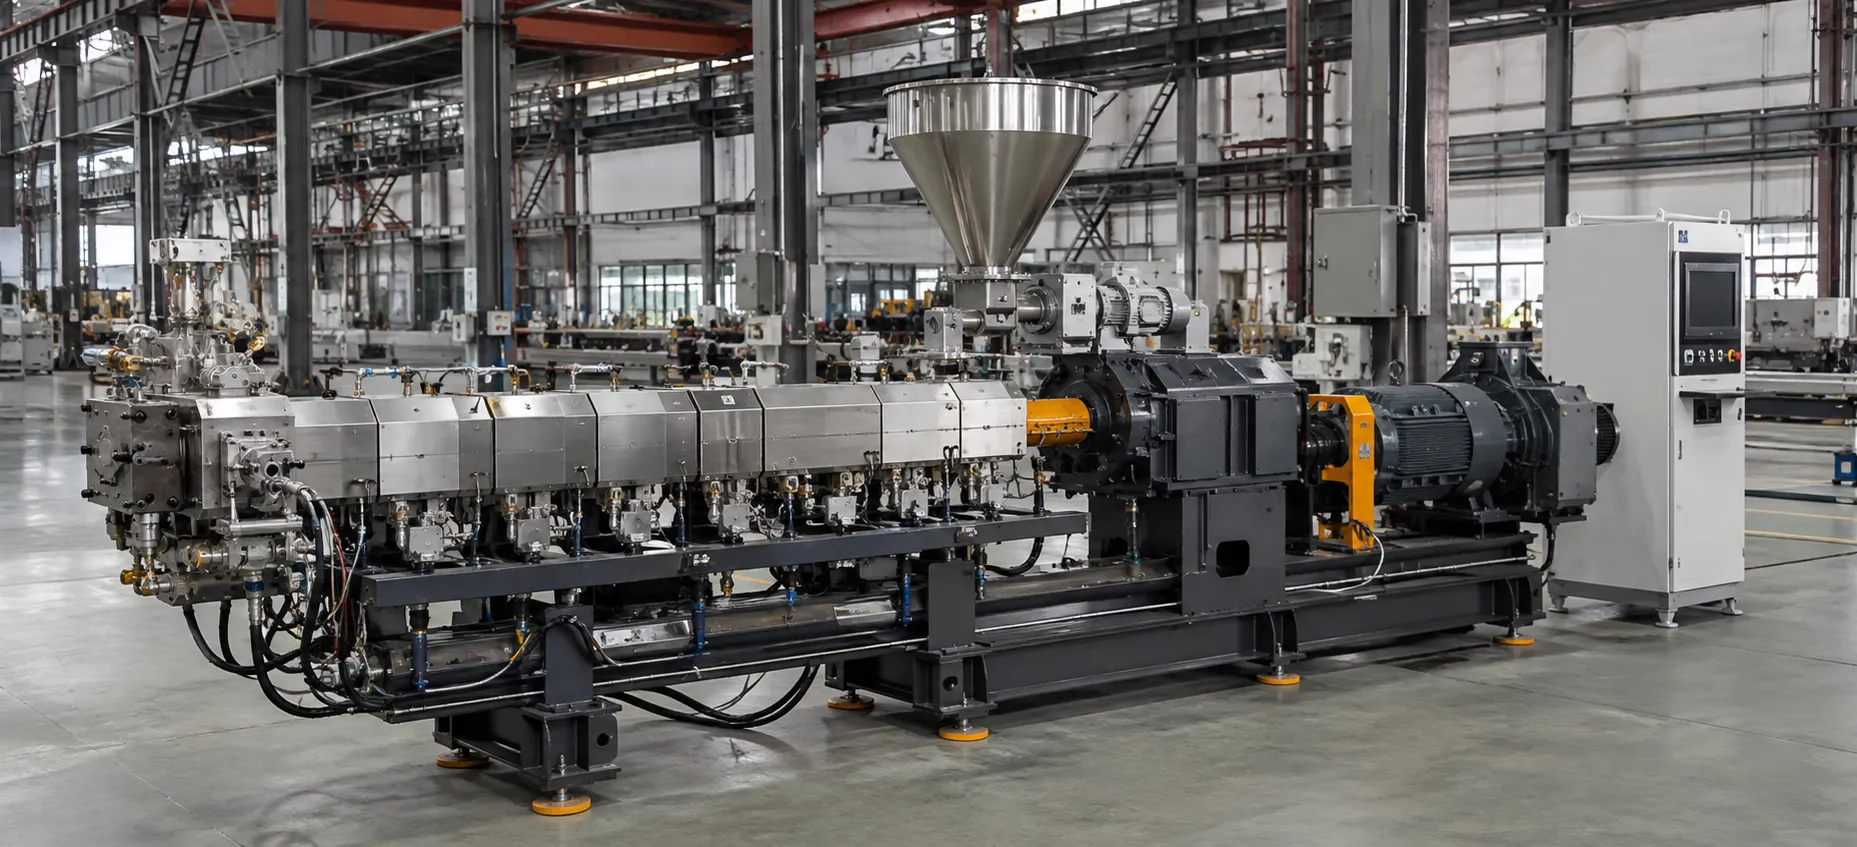
For composite materials, rubber-plastic blends and co-extruded films with frequent recipe changes.
- Twin screw forced feeding — no bridging
- Modular screw & barrel design
- Pressure fluctuation ≤5%
Lab Scale Series
R&D · pilot · universities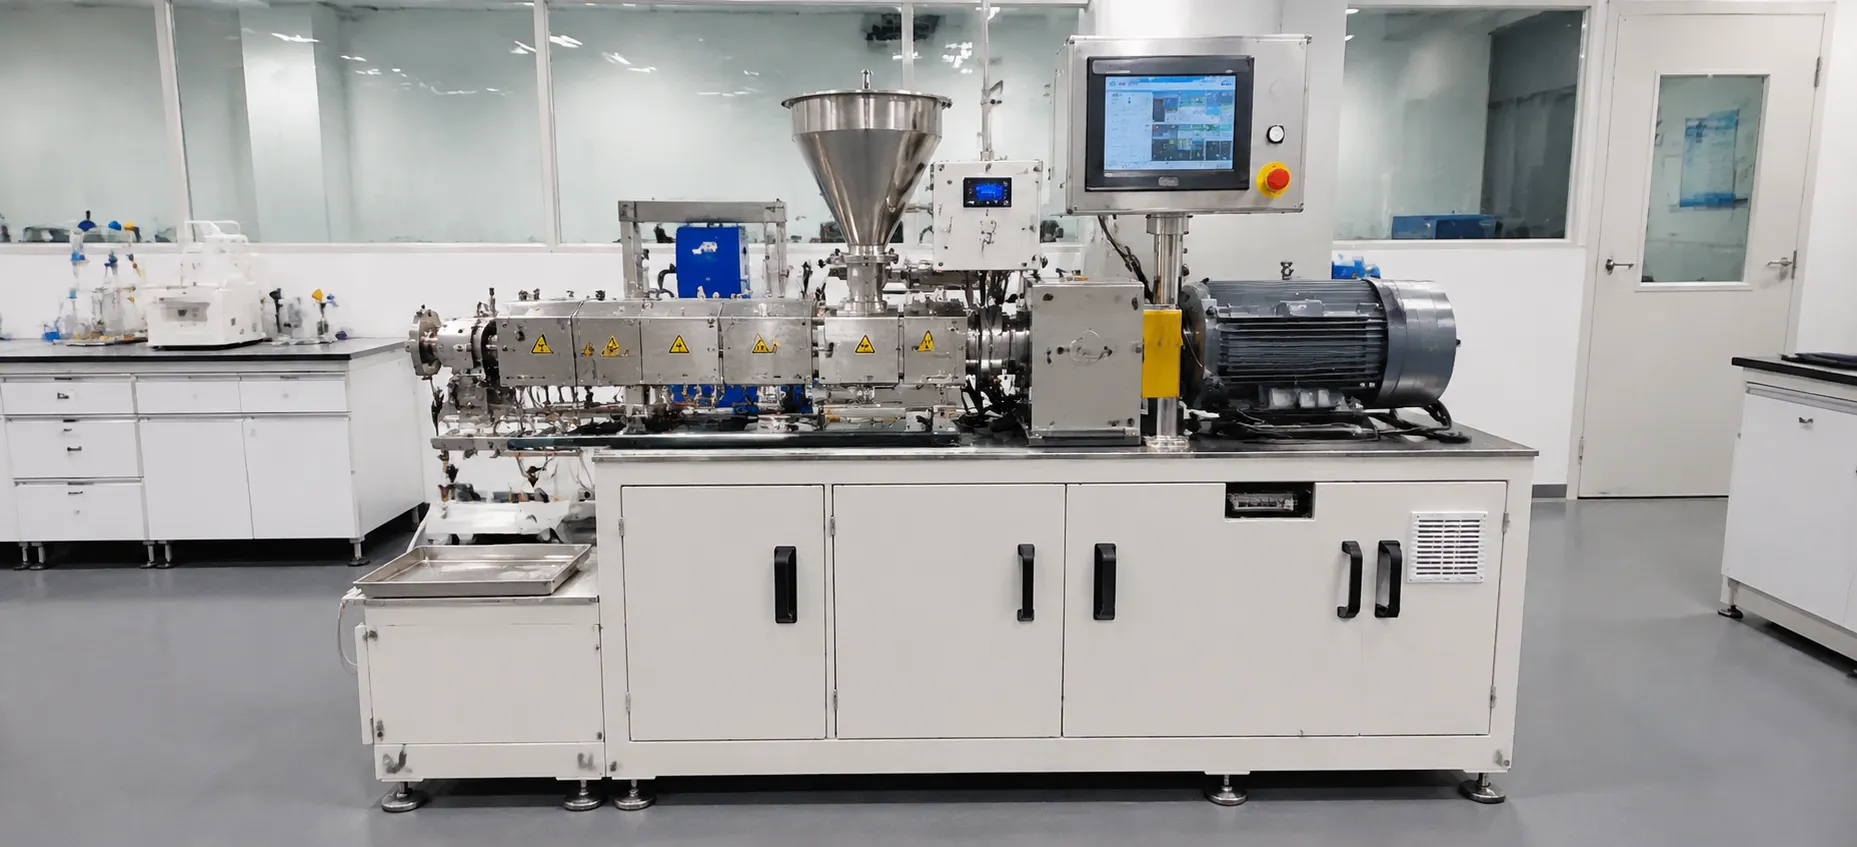
Compact 1.2 m² footprint with traceable parameters for formula iteration and scale-up studies.
- Multiple screw diameter options
- Intelligent temperature control
- Direct scale-up to production models
Technical Data
Triple Screw Extruder Specifications & Model Chart
All figures taken from current production drawings. Custom L/D, torque grade and downstream on request.
| Model | Screw Diameter (mm) | L/D Ratio | Screw Speed (rpm) | Motor Power (kW) | Output (kg/h) |
|---|---|---|---|---|---|
| UET-29 | 29.0 | 26–85 | 550–650 | 14 | 50–90 |
| UET-37 | 37.4 | 26–85 | 550–650 | 31 | 130–180 |
| UET-45 | 45.2 | 26–85 | 550–650 | 46 | 220–320 |
| UET-53 | 53.1 | 26–85 | 550–650 | 88 | 550–750 |
| UET-63 | 63.3 | 26–85 | 550–650 | 128–155 | 780–1,100 |
| UET-74 | 74.5 | 26–85 | 550–650 | 205–235 | 1,350–1,850 |
| UET-92 | 92.8 | 26–85 | 550–650 | 370–410 | 2,300–3,300 |
Available Configurations & Downstream Options
Feeding & Screw Combination
Gravimetric main feeder; twin-screw side feeder for powders; modular conveying, kneading and toothed-mixing elements; L/D 26–85 tailored to your recipe.
Barrel, Vents & Temperature
Atmospheric + vacuum vent ports; independent PID heating/cooling zones; bimetallic barrel option for abrasive high-fill recipes.
Pelletizing & Control
Strand, water-ring, hot-face or underwater pelletizing; PLC + touch HMI with recipe management; remote monitoring and data traceability.
Quick Model Selector — Match by Application
| Application | Target Output (kg/h) | Recommended Model |
|---|---|---|
| Lab R&D / sample pellets (PLA, PBAT trials) | 50–90 | UET-29 |
| Color / additive masterbatch, small batch | 130–320 | UET-37 / UET-45 |
| Filler masterbatch up to 75% CaCO₃ | 550–1,100 | UET-53 / UET-63 |
| Engineering plastics, glass-fiber reinforced | 780–1,100 | UET-63 |
| Cable compounds / PVC compounding | 1,350–1,850 | UET-74 |
| Large-scale biodegradable (PLA/PBAT) line | 2,300–3,300 | UET-92 |
Not sure which model fits your recipe? Send your material details for a free feasibility check →
30-Second Comparison
Single vs Twin vs Triple Screw Extruder
We build and sell all three types, so this table is the honest version of the argument we have with customers every week
| Feature | Single Screw | Twin Screw | Triple Screw |
|---|---|---|---|
| Best for | Melting & forming | Mixing & compounding | High-end nano dispersion |
| Mixing intensity | Low | High | Very high |
| Dispersion quality | Basic | Good | Excellent (98%+) |
| Typical materials | PE, PP, PVC | Masterbatch, engineering, recycled | Biodegradable, medical-grade, high-fill |
| Energy efficiency | Moderate | Good | Best (−20%) |
| Self-cleaning | Manual cleaning | Good | Excellent |
| Investment level | Entry | Mid-range | Premium — pays back via high-value materials |
Why UET
Why Choose UET as Your Triple Screw Extruder Supplier
The checks a serious buyer runs on a supplier — and our straight answers
20+ Years Manufacturing Experience
Established 2005 · 5,600+ machines delivered to 80+ countries with proven reliability in demanding 24/7 applications.
In-House Material Test Lab
Screw configuration and process parameters validated with your actual material before the equipment is built.
CE Certified Builds
Every line meets international safety and quality standards with full documentation for smooth market access.
Custom Engineering
Screw geometry, barrel zones, die and downstream tailored to your exact recipe, output target and product spec.
24/7 Lifetime Support
Round-the-clock engineer response via WhatsApp or video, 24-month core-component warranty, lifetime spare parts at cost.
Factory-Direct Pricing
No trading company in between — transparent, itemized quotations delivered within 2 hours, no hidden fees.
Applications
Applications of UET Triple Screw Extruders
Eight segments where UET triple screw lines run shifts every day
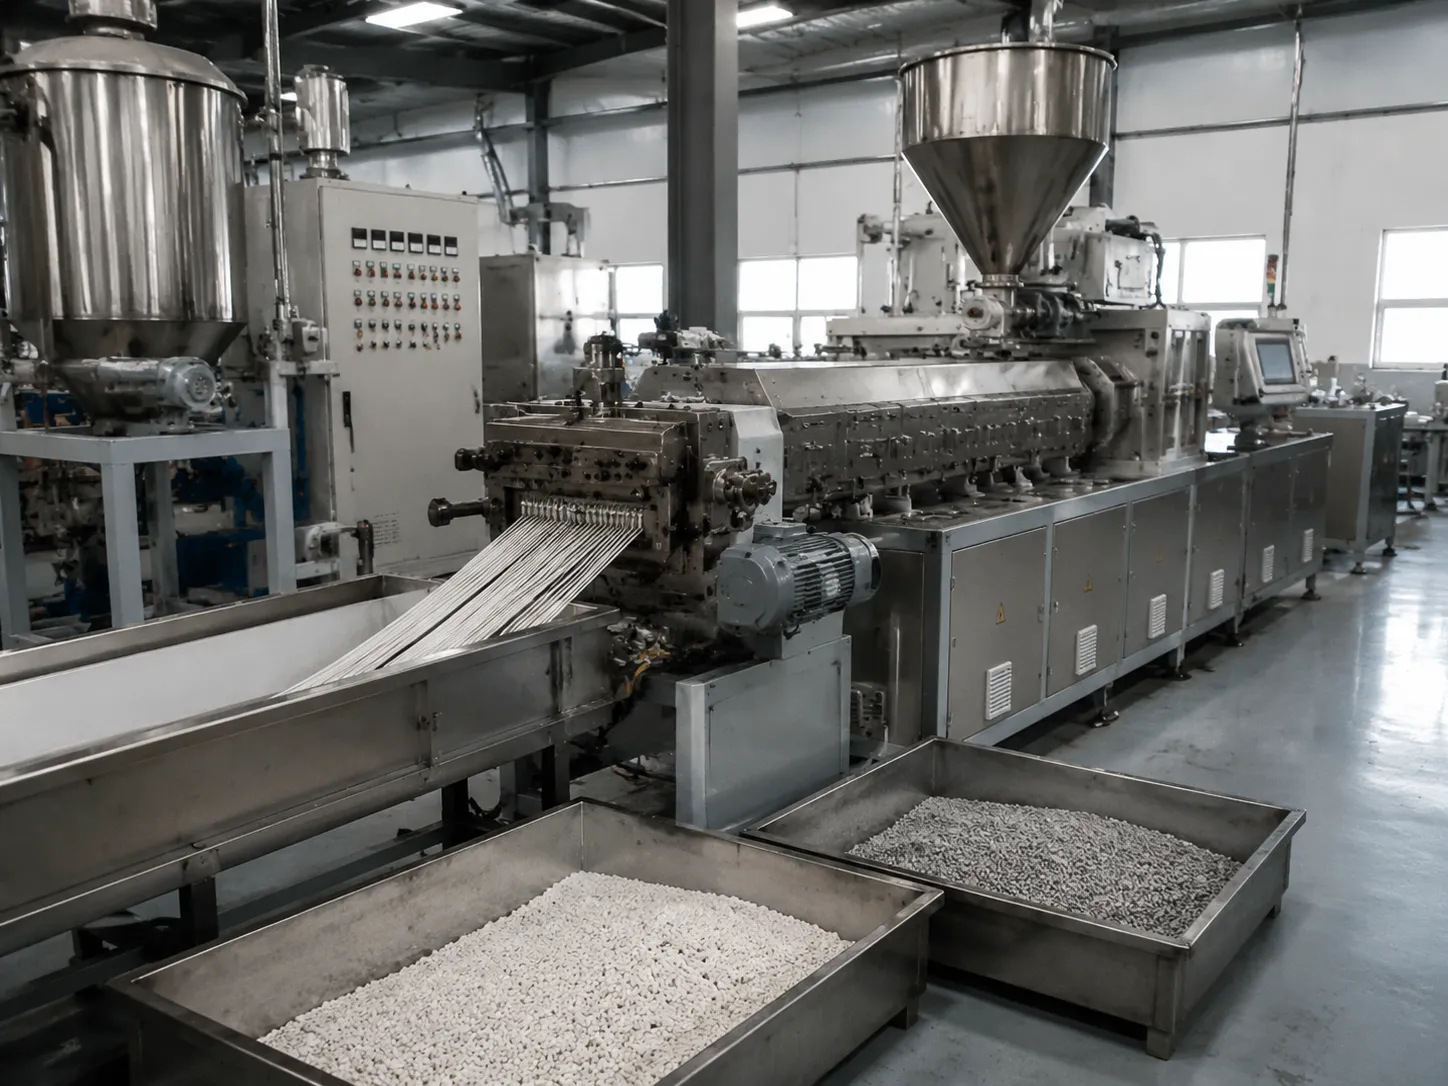
Filler Masterbatch
Coordinated triple-screw shear fuses 60–80% filler loads deeply into the base resin — higher rigidity without losing flowability.
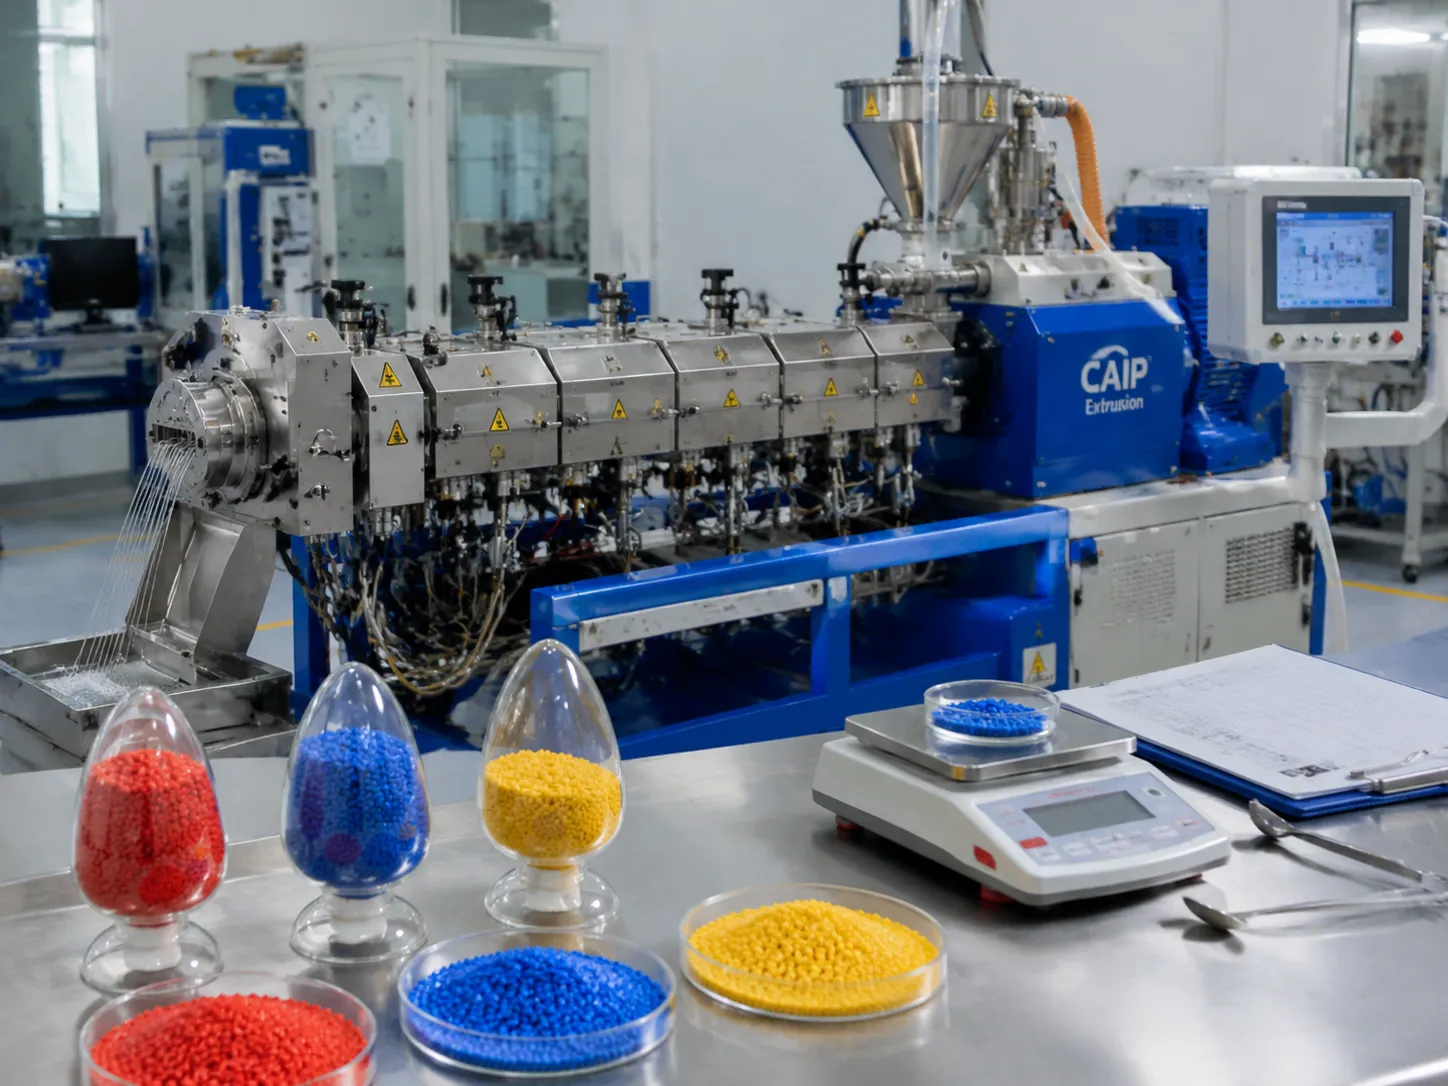
Color Masterbatch
Multi-zone temperature control and intermeshing structure coat high-concentration pigments uniformly — zero color variation in mass production.
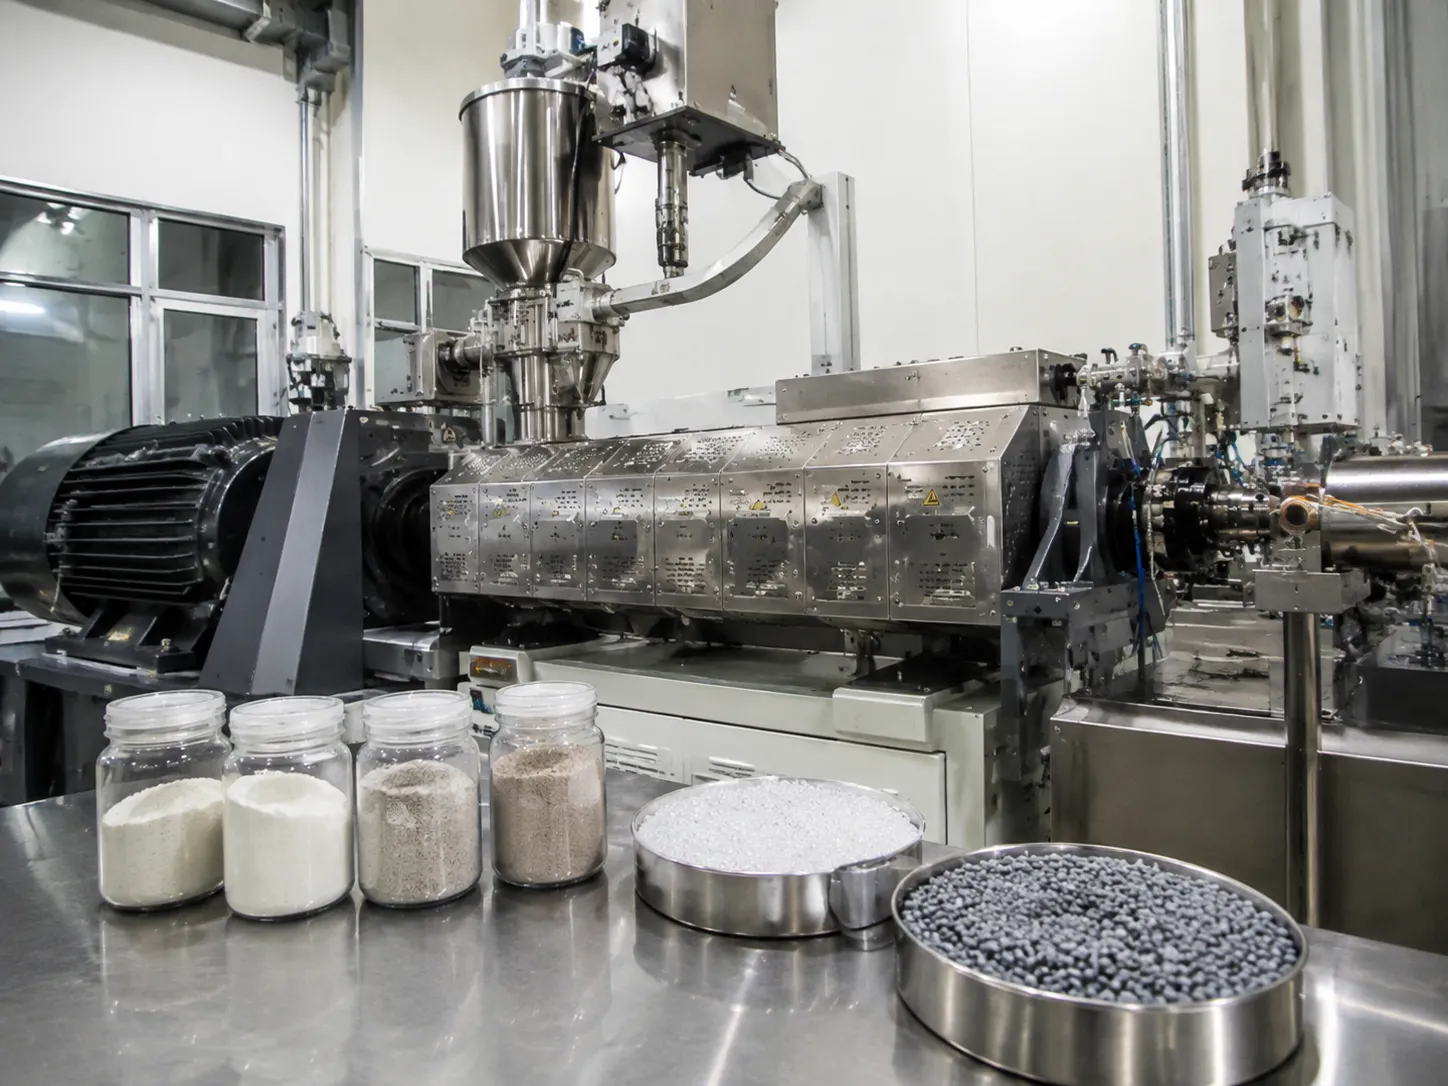
Additive Masterbatch
Three-stage compounding modules fully disperse antioxidants and UV stabilizers for accurate, long-lasting dosage stability.
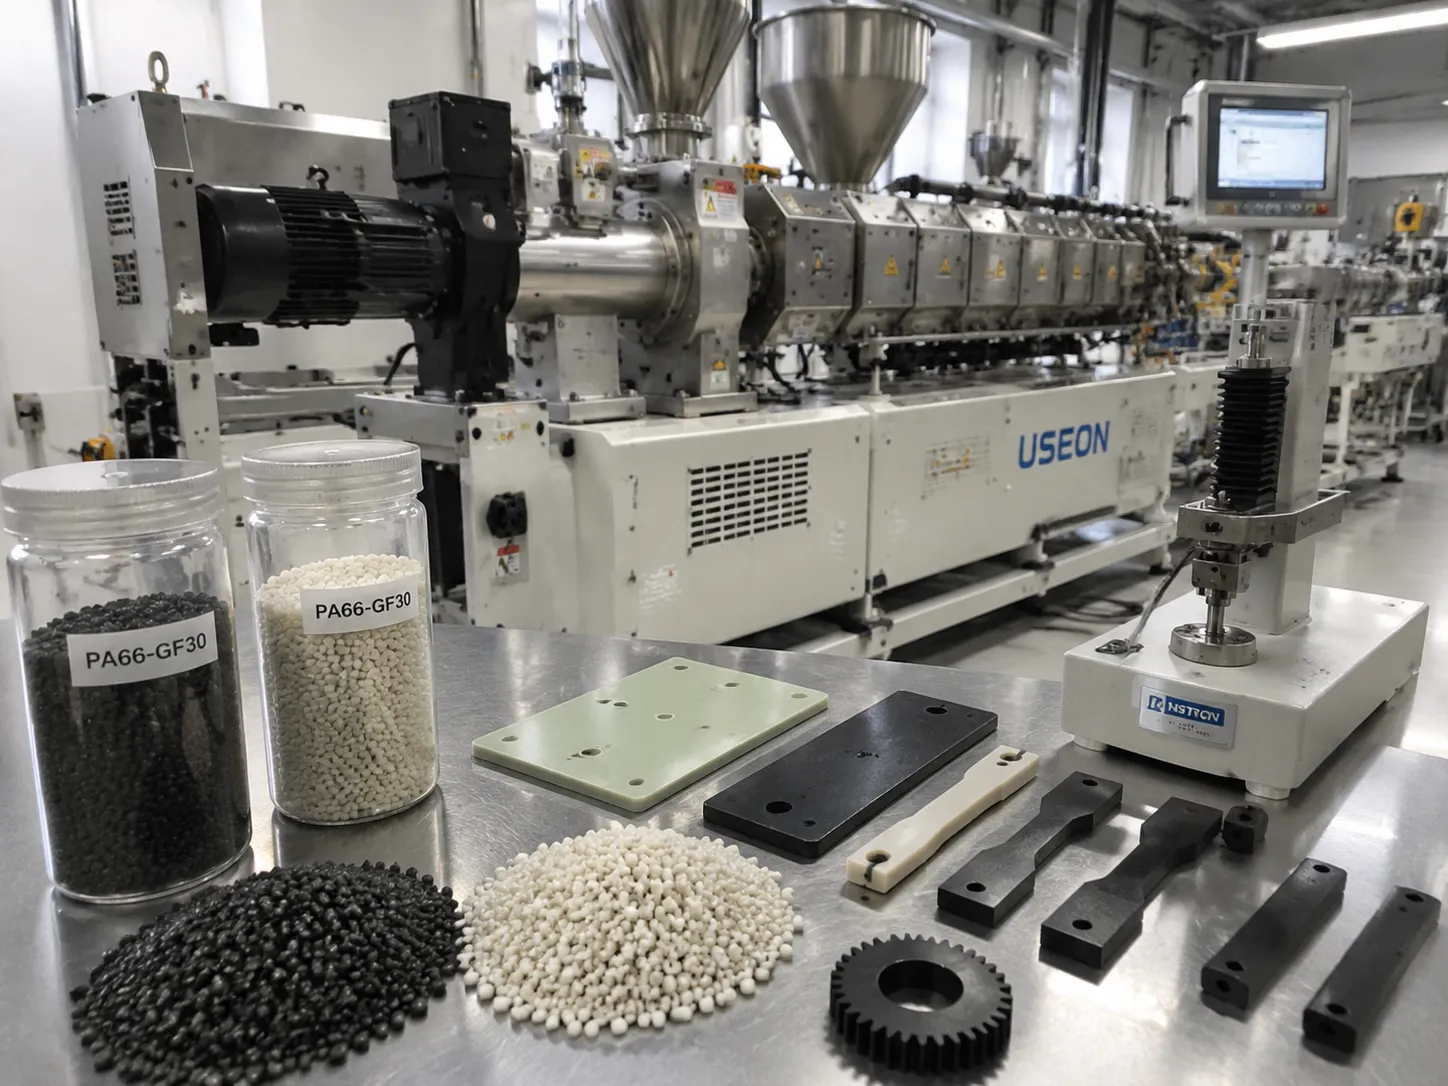
Engineering Plastics
Ultra-stable high-temperature plasticization integrates glass fiber and fillers fully — enhanced strength for precision electronic components.
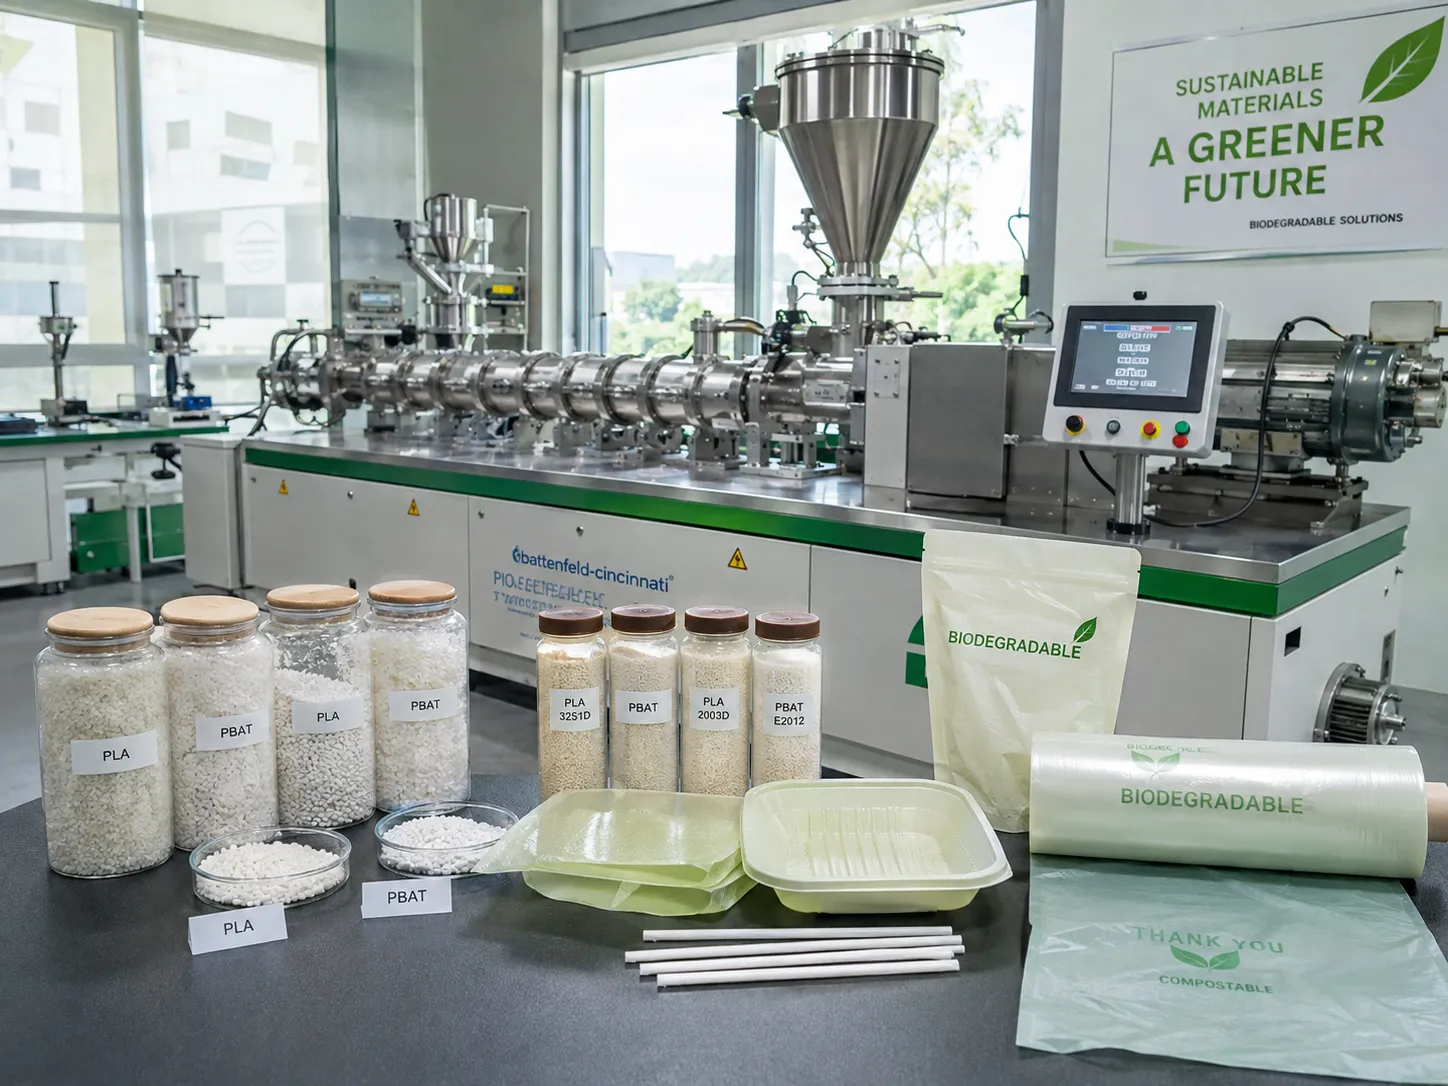
Biodegradable Plastics
Gentle yet efficient plasticization preserves PLA/PBAT resin activity while compounding fully with modifiers — stable degradation performance.
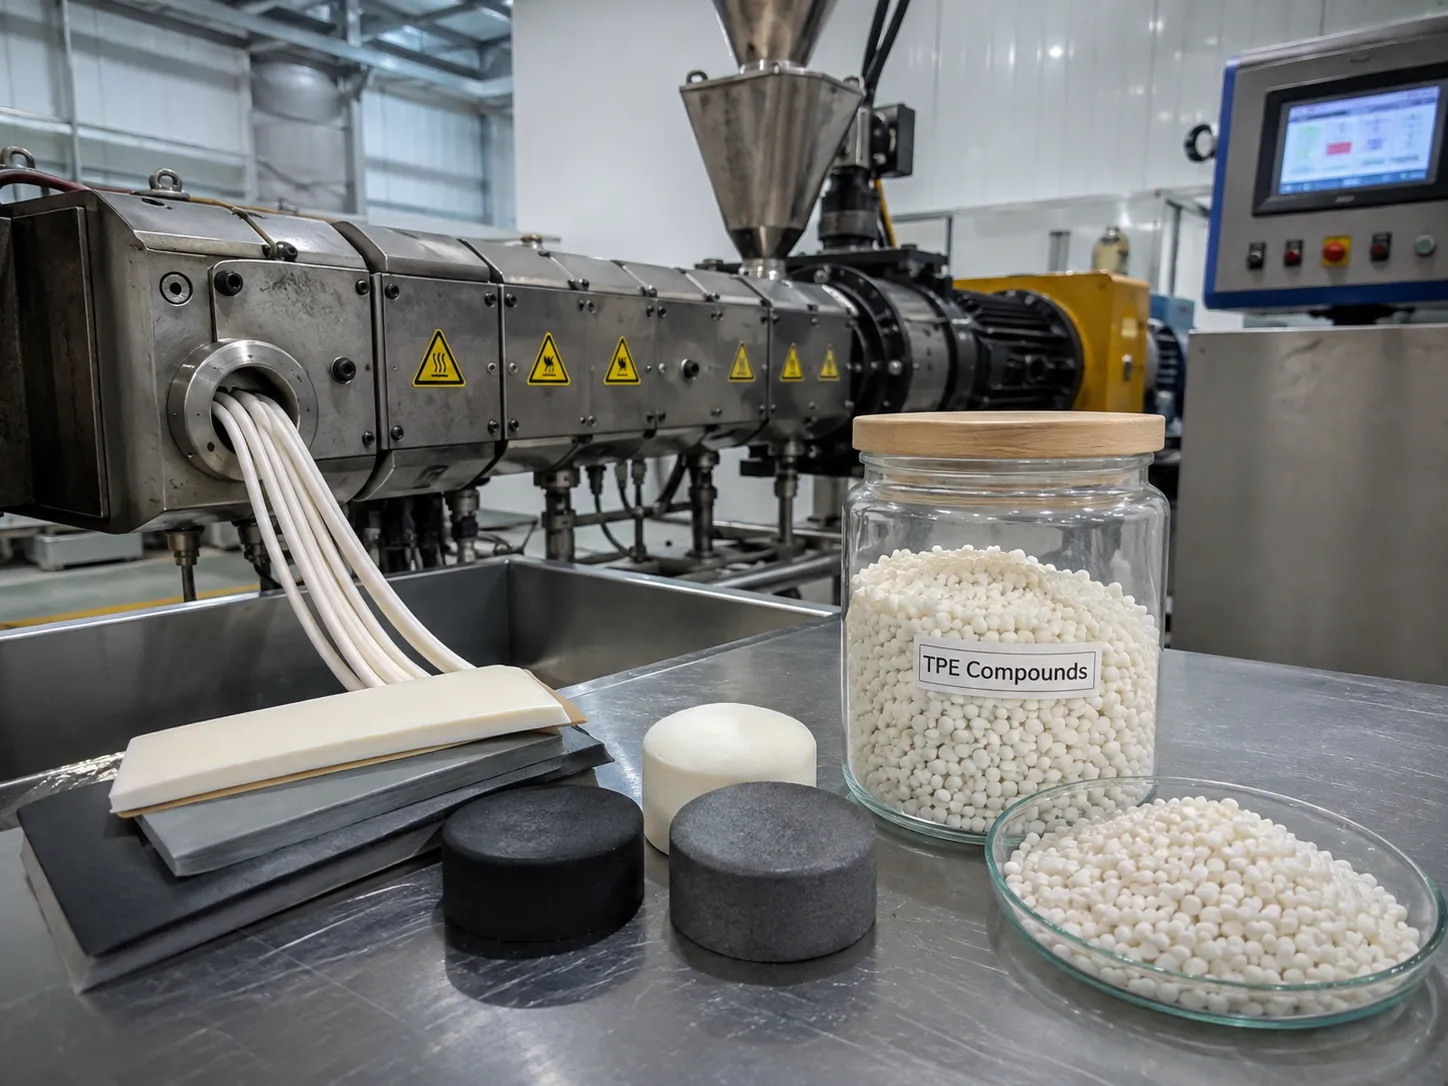
Thermoplastic Elastomers
Gradient shear blends elastic components uniformly — wider controllable hardness range, smooth texture, superior aging resistance.
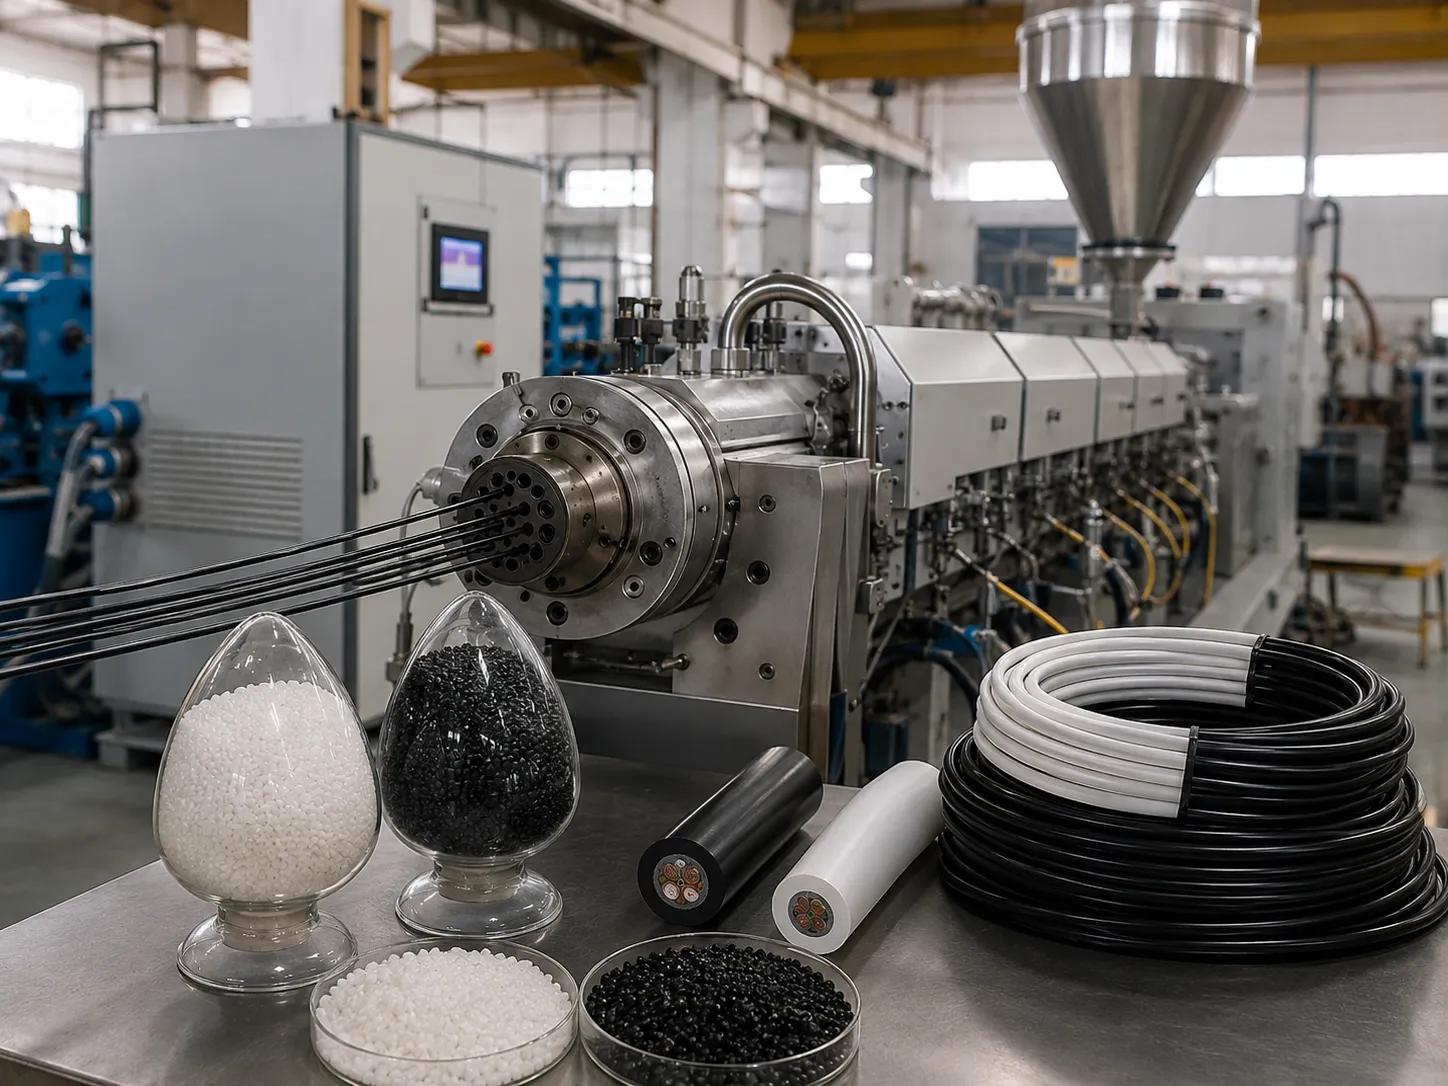
Cable Compounding
Dead-zone-free full-area compounding ensures tight fusion of insulation compounds — meeting high-end new energy and communication cable standards.
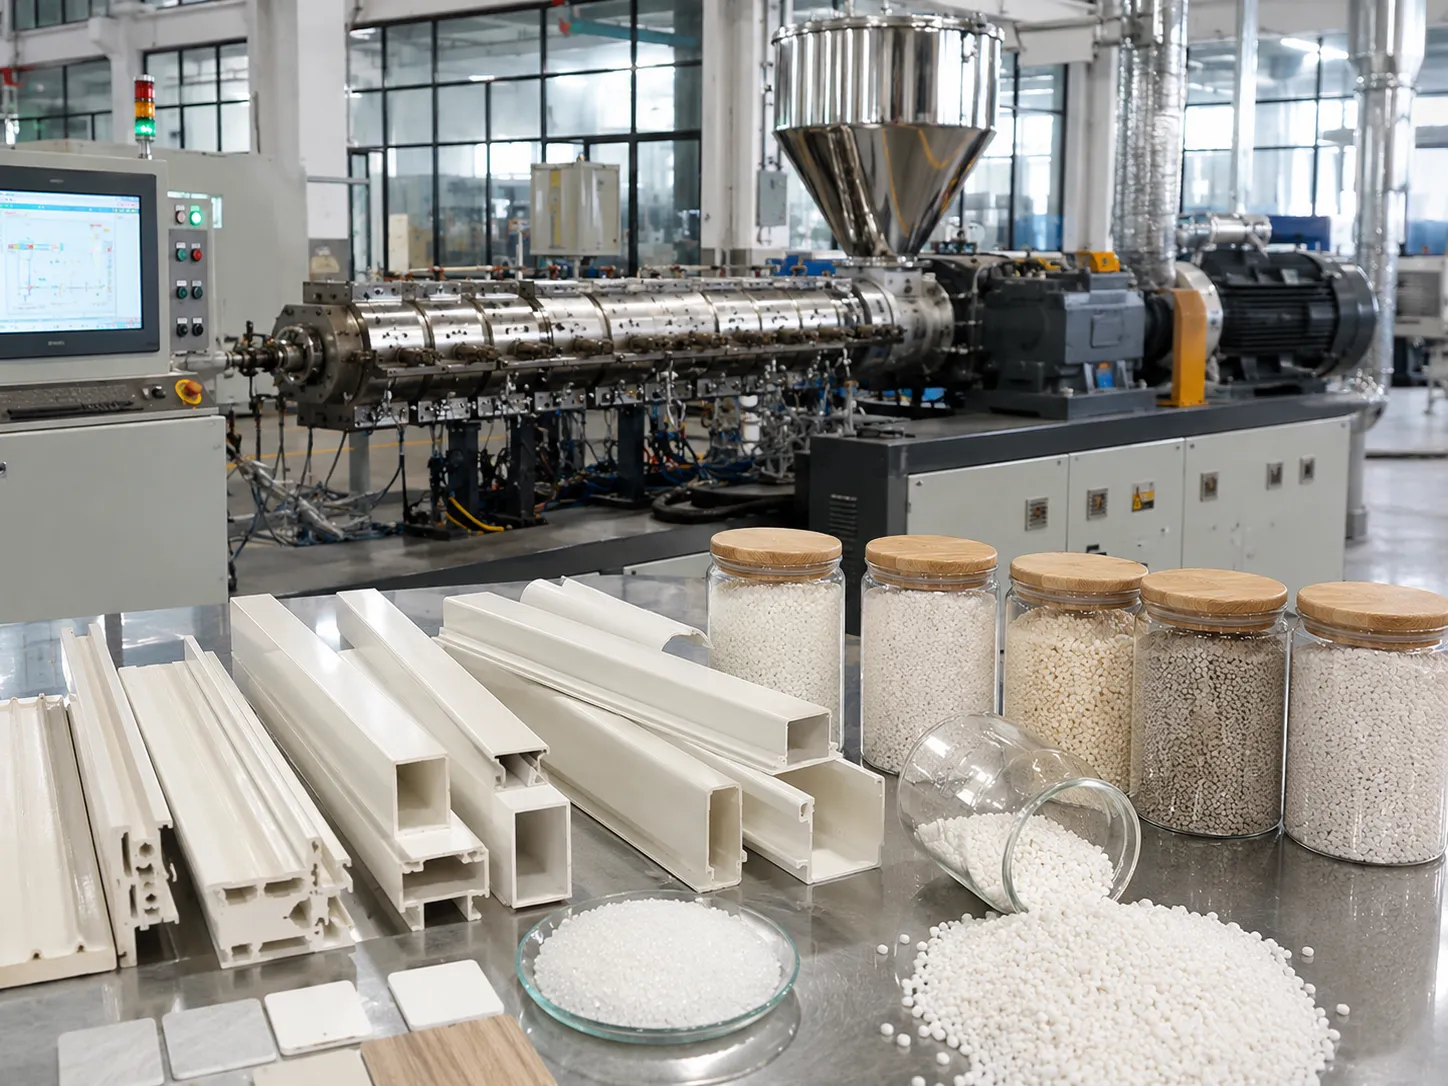
PVC Compounding
Low-shear, high-torque configuration plasticizes PVC uniformly without thermal decomposition — ideal for pipes, profiles and fittings.
Material Coverage
Materials a Triple Screw Extruder Can Process
If a polymer needs melting, mixing or dispersing, our test lab has probably already run it
Materials In — Supported Resins & Additives
Base polymers, elastomers and high-load additives that run stably on UET triple screw lines.
- PE / PP
- PA6 / PA66
- PC
- ABS / SAN
- PET / PBT
- PMMA
- POM
- EVA / POE
- PLA / PBAT / PBS
- TPE / TPU
- PVC
- Recycled regrind
- CaCO₃ / talc fillers
- Glass fiber
- Carbon black
- Antioxidants / UV additives
- Flame retardants
- Medical & food-grade resins
Products Out — What You Can Make
Finished compounds and semi-finished feedstock produced after pelletizing.
- Filler masterbatch pellets
- Color masterbatch pellets
- Additive / functional masterbatch
- Glass-fiber reinforced compounds
- Biodegradable compound pellets
- Cable insulation & sheathing compounds
- PVC dry-blend compounds
- TPE granules
- Sheet / film extrusion feedstock
- Pipe & profile compounds
- 3D printing filament feedstock
- Medical & food-contact compounds
Machine Anatomy
How a UET Triple Screw Extruder Works
Follow one pellet’s path through the machine — eight components do all the work
1
Feeding & Conveying
Material enters the enlarged free volume and is positively conveyed by three synchronized screws.
2
Triple-Shear Melting & Mixing
Dual meshing zones apply repeated shear — nano-level dispersion in short, uniform residence time.
3
Devolatilization & Homogenizing
Vent zones strip moisture and volatiles while zoned temperature control stabilizes the melt.
4
Die Extrusion & Pelletizing
Homogeneous melt exits through the optimized die for downstream pelletizing into premium pellets.
- 1Motor & High-Torque GearboxHigh torque density drives three screws steadily under high-fill load, without speed surging.
- 2Feed HopperEnlarged free volume (+40%) with optional forced feeder for powders like CaCO₃ and carbon black.
- 3Triple-Screw BarrelThree co-rotating intermeshing screws; modular barrel sections, L/D 26–85 tailored to your recipe.
- 4Zoned Heating / CoolingIndependent PID zones hold melt temperature within ±1.5°C to protect heat-sensitive resins.
- 5Vent PortFast surface renewal removes volatiles and moisture efficiently for cleaner pellets.
- 6Die HeadOptimized flow channel reduces pressure loss for uniform dimensions and lower energy use.
- 7HMI Control SystemRecipe-based touch operation with traceable parameters — new operators learn in days.
- 8Triple-Meshing Cross-SectionTwo intermeshing zones = double the shear and mixing range of a twin screw design.
ROI Estimator
Triple Screw Extruder ROI: Estimate Your Annual Energy Savings
Punch in your line parameters — the math uses the same 0.35 kWh/kg baseline our quotations quote against
Your Line Parameters
Adjust the three values — results update instantly.
—kWh saved per year
—USD saved per year
—tons CO₂ avoided per year
Estimate basis: 0.35 kWh/kg average specific energy for twin-screw compounding, 300 working days/year and a conservative 20% saving with UET triple-screw design.
Our Facility
Triple Screw Extruder Manufacturer in China
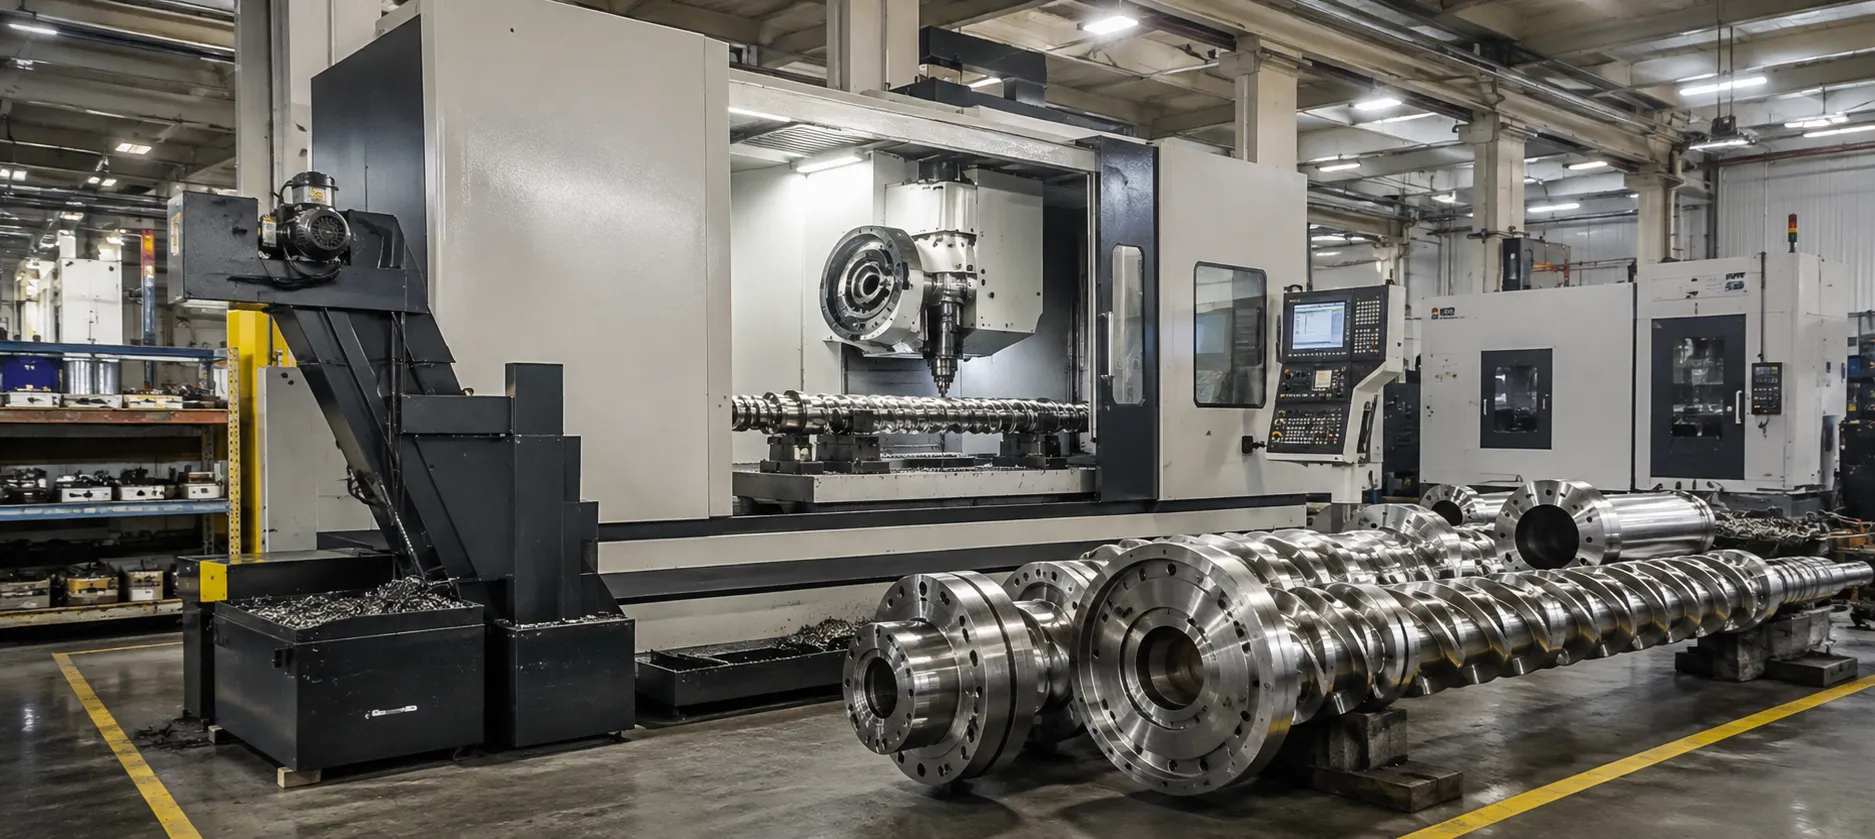
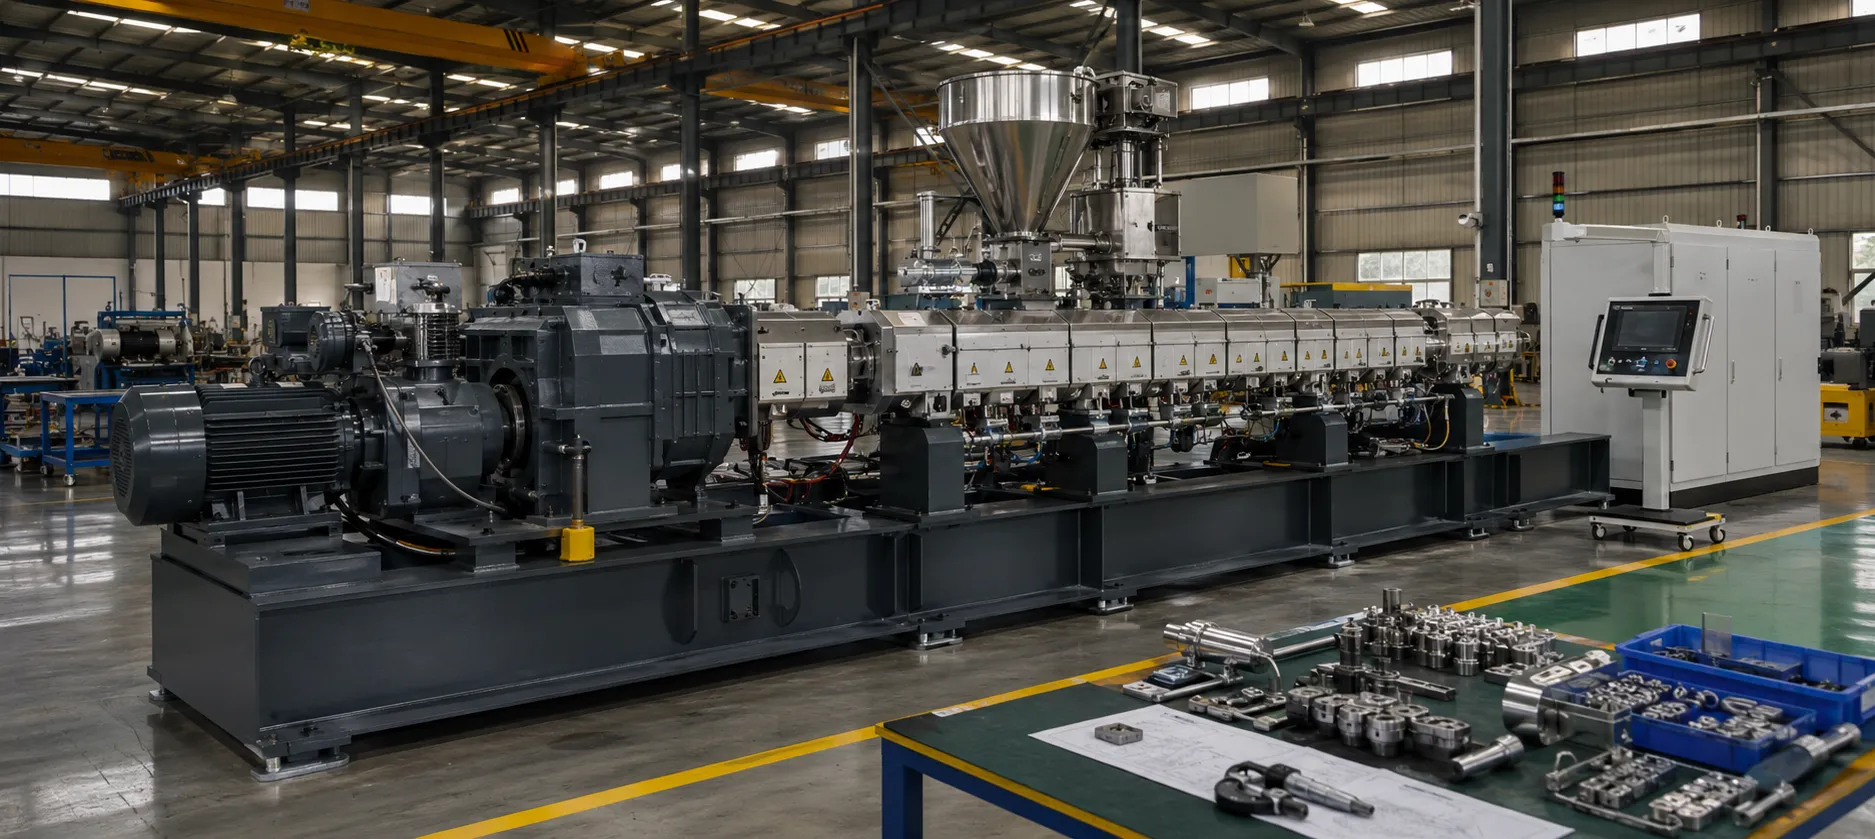
11,400 m² in Nanjing: machining, assembly and the test stands where every machine earns its shipping crate
11,400㎡Manufacturing Base
350+Engineers & Staff
100%Test-Run Before Shipping
5,600+Machines Delivered
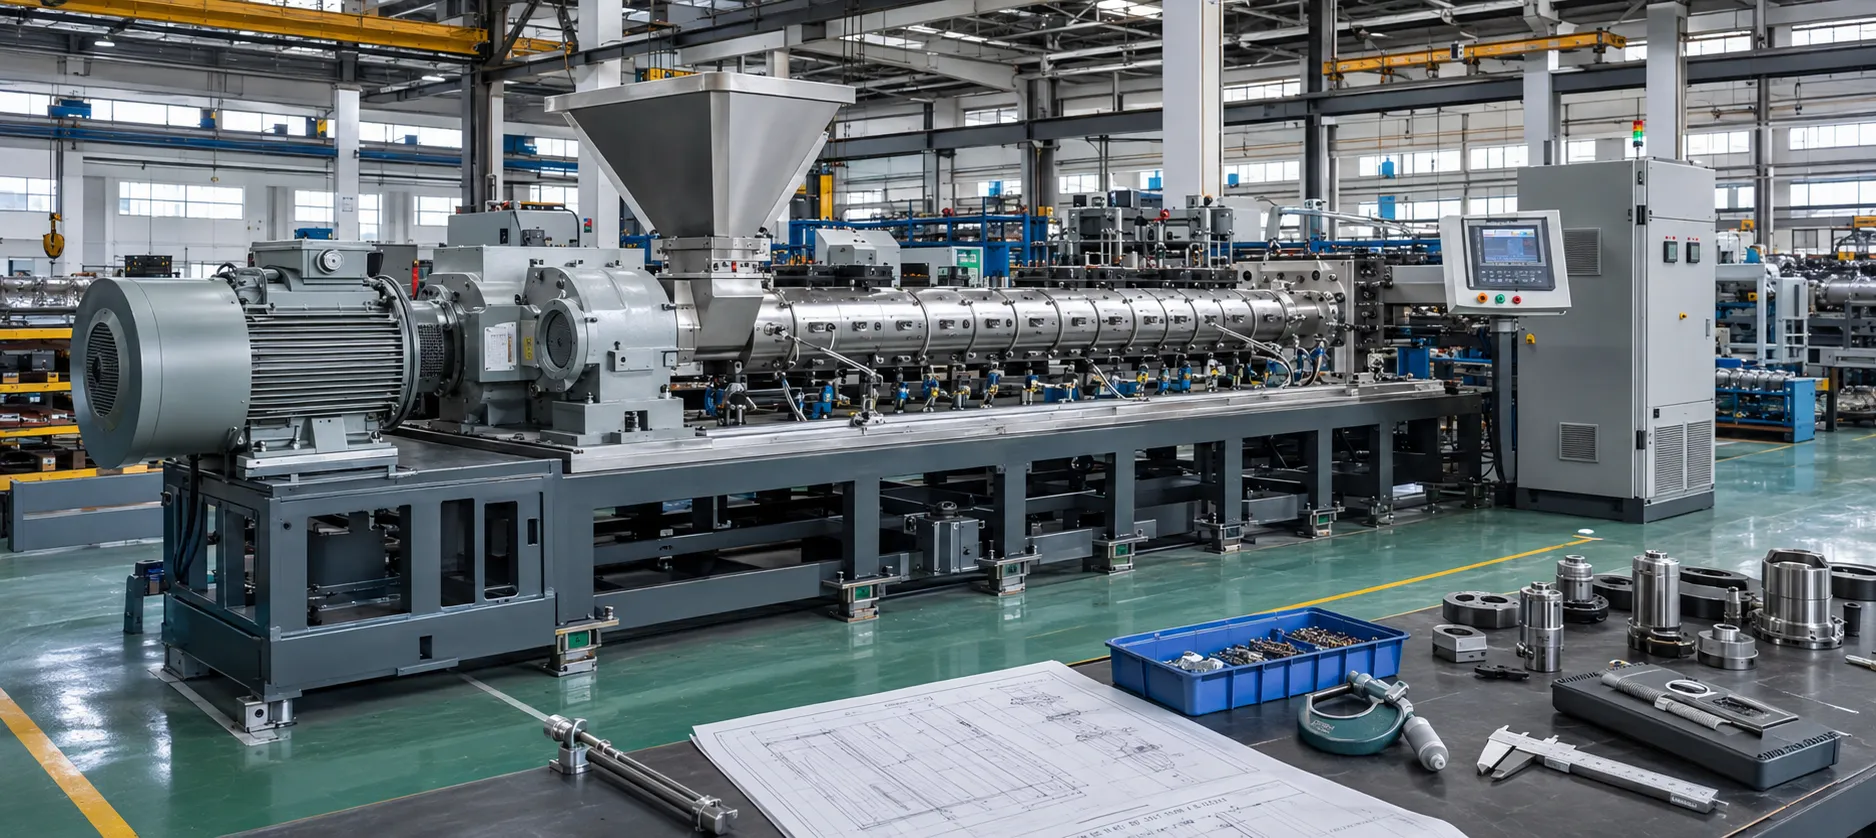
Quality Control Process
- Raw material inspection: steel and components tested for hardness, composition and dimensional accuracy.
- CNC precision machining: screws and barrels machined to 0.02 mm tolerance on 5-axis centers.
- Assembly verification: every component checked against engineering drawings before assembly.
- Full-load testing: 8-hour continuous operation test under maximum load.
- Material trial run: validation with your actual material — inspect in person or by live video.
- Final inspection: complete checklist covering safety, performance and export documentation.
Customer Success Stories
Triple Screw Extruder Customer Reviews
Unedited feedback from plants running UET triple screw lines right now
★★★★★
“We chose UET triple screw extruders for high-filler engineering plastics. Compounding uniformity and efficiency exceeded expectations — three months of continuous operation without failure, material waste down 18%.”
Ethan CarterProduction Manager · Engineering Plastics, USA
★★★★★
“Medical materials demand extreme cleanliness and stability. Precise temperature control and gentle compounding raised our qualified rate from 96% to 99.2% — daily operation is much easier now.”
David SmithQuality Director · Medical Materials, Germany
★★★★★
“On high-viscosity cable compounds the output is stable and insulation performance meets standard. Maintenance downtime down 25% — cost performance far superior to similar equipment.”
Sophia MillerOperations Director · Cable Compounding, Turkey
Service Commitment
Triple Screw Extruder Warranty & After-Sales Support
The part buyers forget to ask about — what happens after the crate arrives
Extended Warranty
18-month overall warranty, 24 months on screws, barrels and gearbox. Free parts and maintenance in warranty.
24/7 Engineer Response
Round-the-clock support via WhatsApp, video call or email — issues resolved in hours, not days.
Installation & Training
On-site or video-guided commissioning plus operator training on operation, maintenance and troubleshooting.
Lifetime Spare Parts
Screws, barrels, heaters and wear parts supplied at cost price for the entire equipment lifetime.
Complete Documentation
Operation manuals, electrical diagrams, maintenance guides and CE certification with every shipment.
Global Service Reach
Export packing, full shipping documents and remote or on-site commissioning support in 80+ countries.
Investment Guide
Triple Screw Extruder Price Guide
Ranges below come from quotations we actually issue. Your exact number depends on configuration.
Lab Scale Models
$10,000 – $35,000- Output 50–90 kg/h · 1.2 m² footprint
- Ideal for R&D and pilot production
- Traceable parameters, quick changeover
Mid-Range Models
$25,800 – $45,000- Output 130–750 kg/h
- High-filler masterbatch capable
- Modular screws · CE certified
High-End Models
$100,000 – $250,000- Output 780–3,300 kg/h
- High-torque gearbox, premium wear parts
- Advanced automation, custom engineering
What Determines Your Exact Price
Equipment Specifications
- Screw diameter & L/D ratio
- Motor power & torque grade
- Barrel zones & heating system
- Control system complexity
Customization Level
- Screw configuration design
- Food-grade / explosion-proof options
- Die head & downstream equipment
- Certification requirements (CE etc.)
Order & Service
- Order quantity discounts
- Installation & training services
- Extended warranty options
- Destination & shipping terms
Explore More
Related Extrusion Solutions from UET
Complete your production line or compare alternative platforms for your application
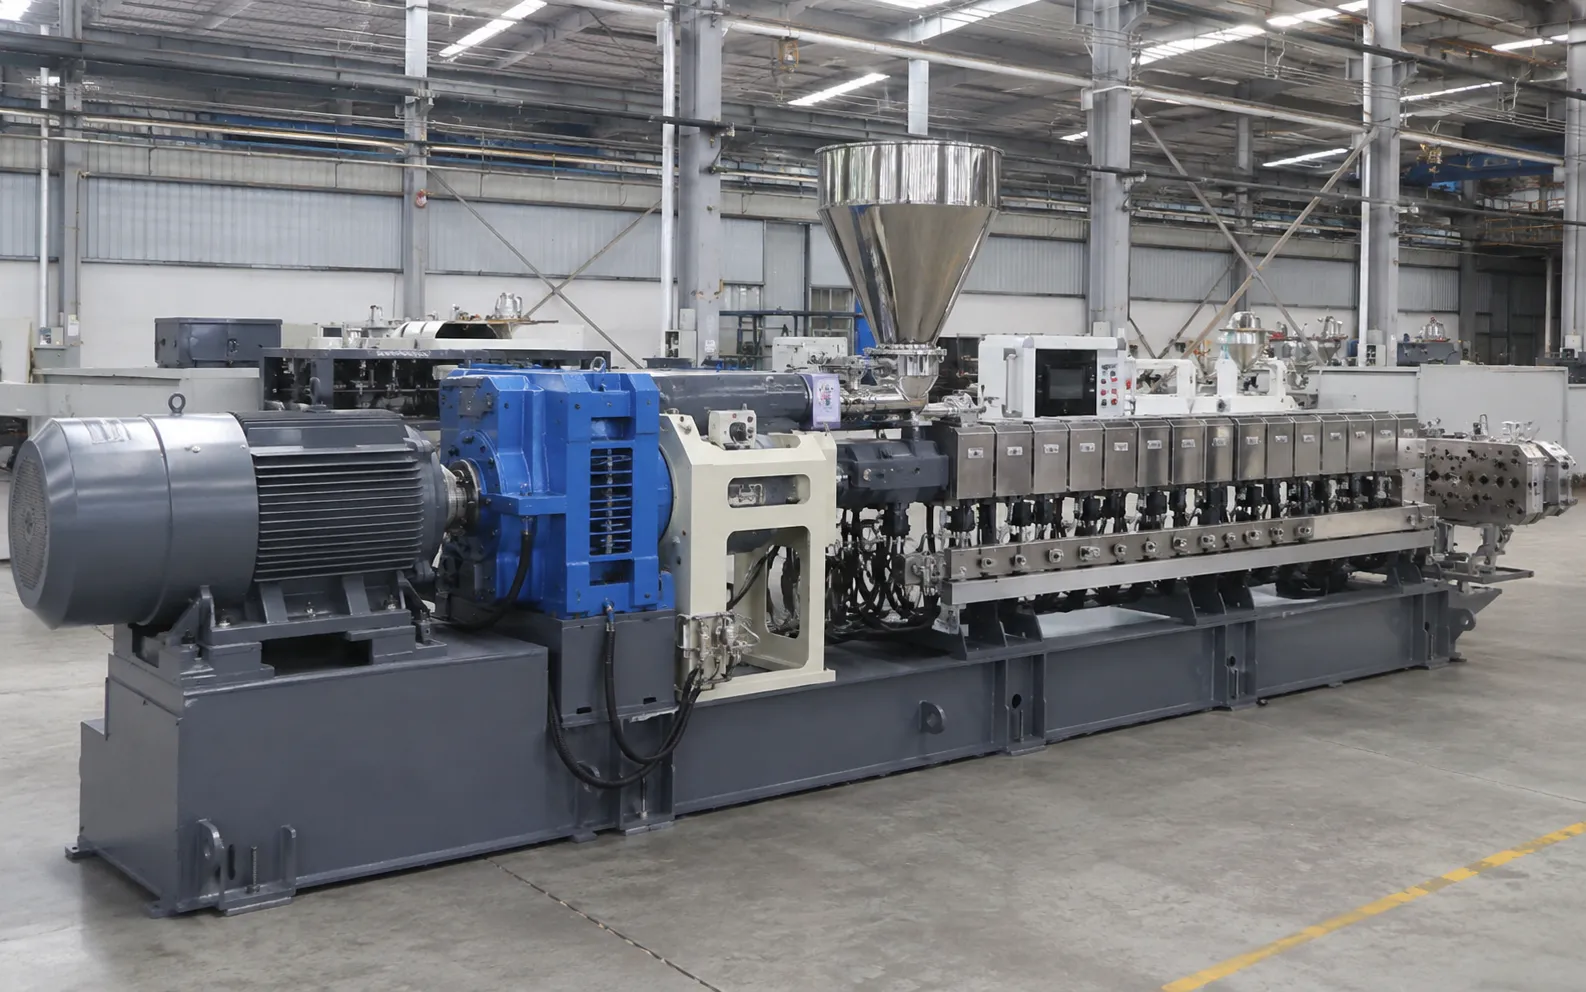
Most Chosen
Twin Screw Extruder
High-torque co-rotating compounding for masterbatch, modified and engineering plastics. 80–2,500 kg/h.
View Details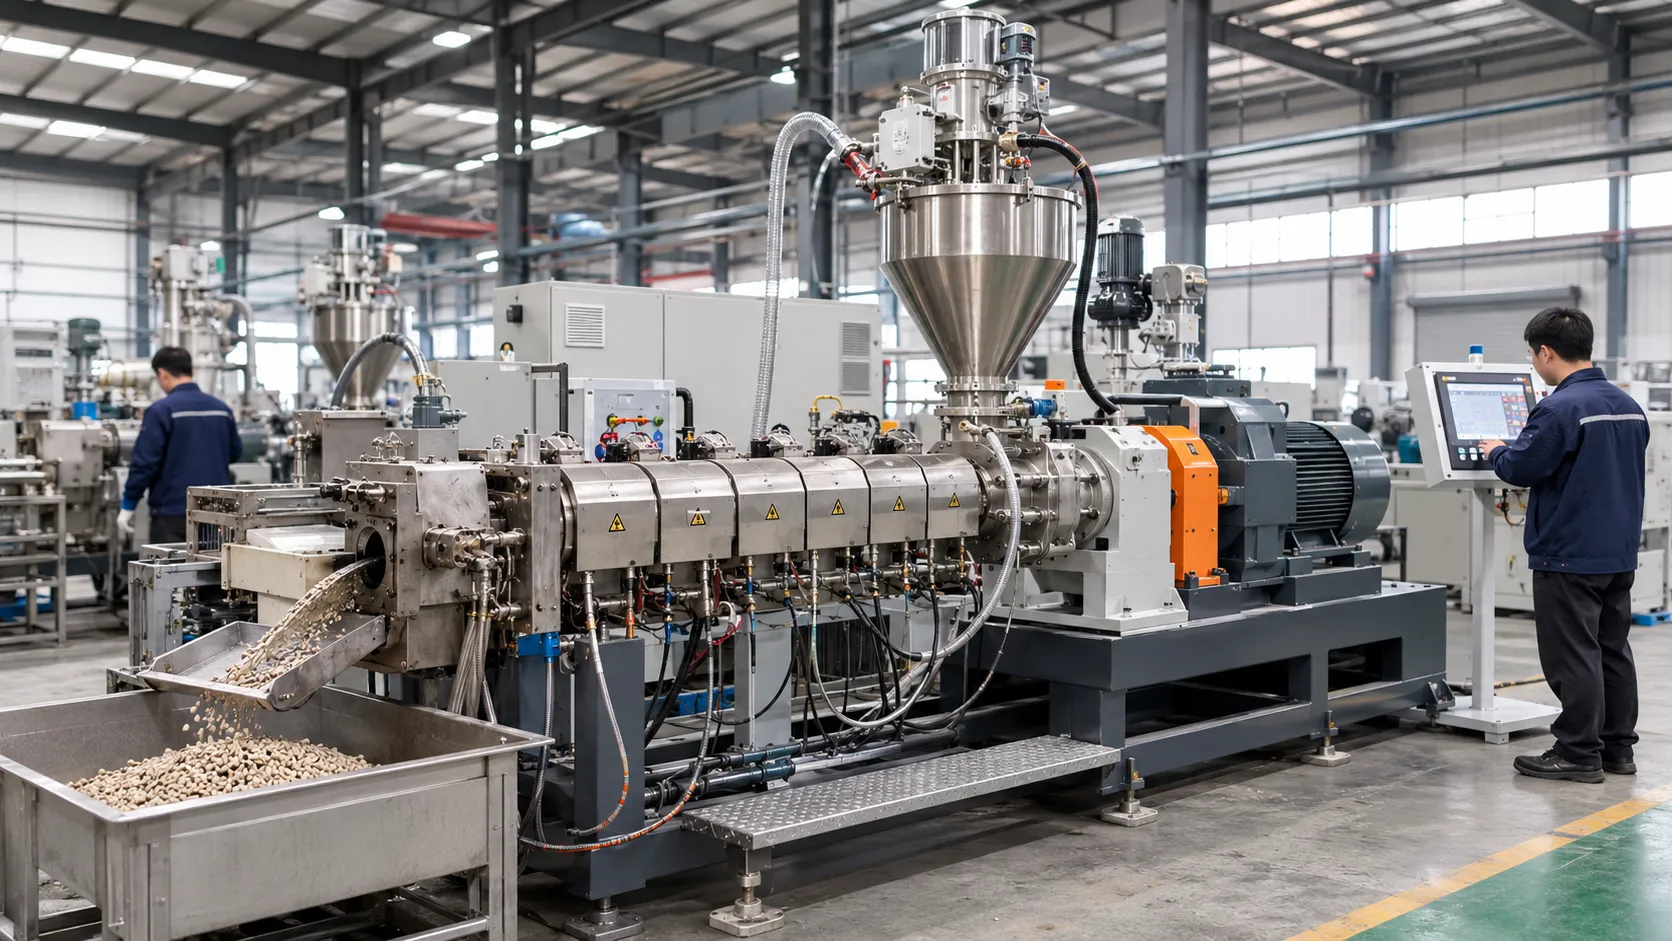
Biodegradable
Bio Extruder
PLA, PBAT, PBS and starch blends with gentle melt handling — 10–1,800 kg/h on four platforms.
View Details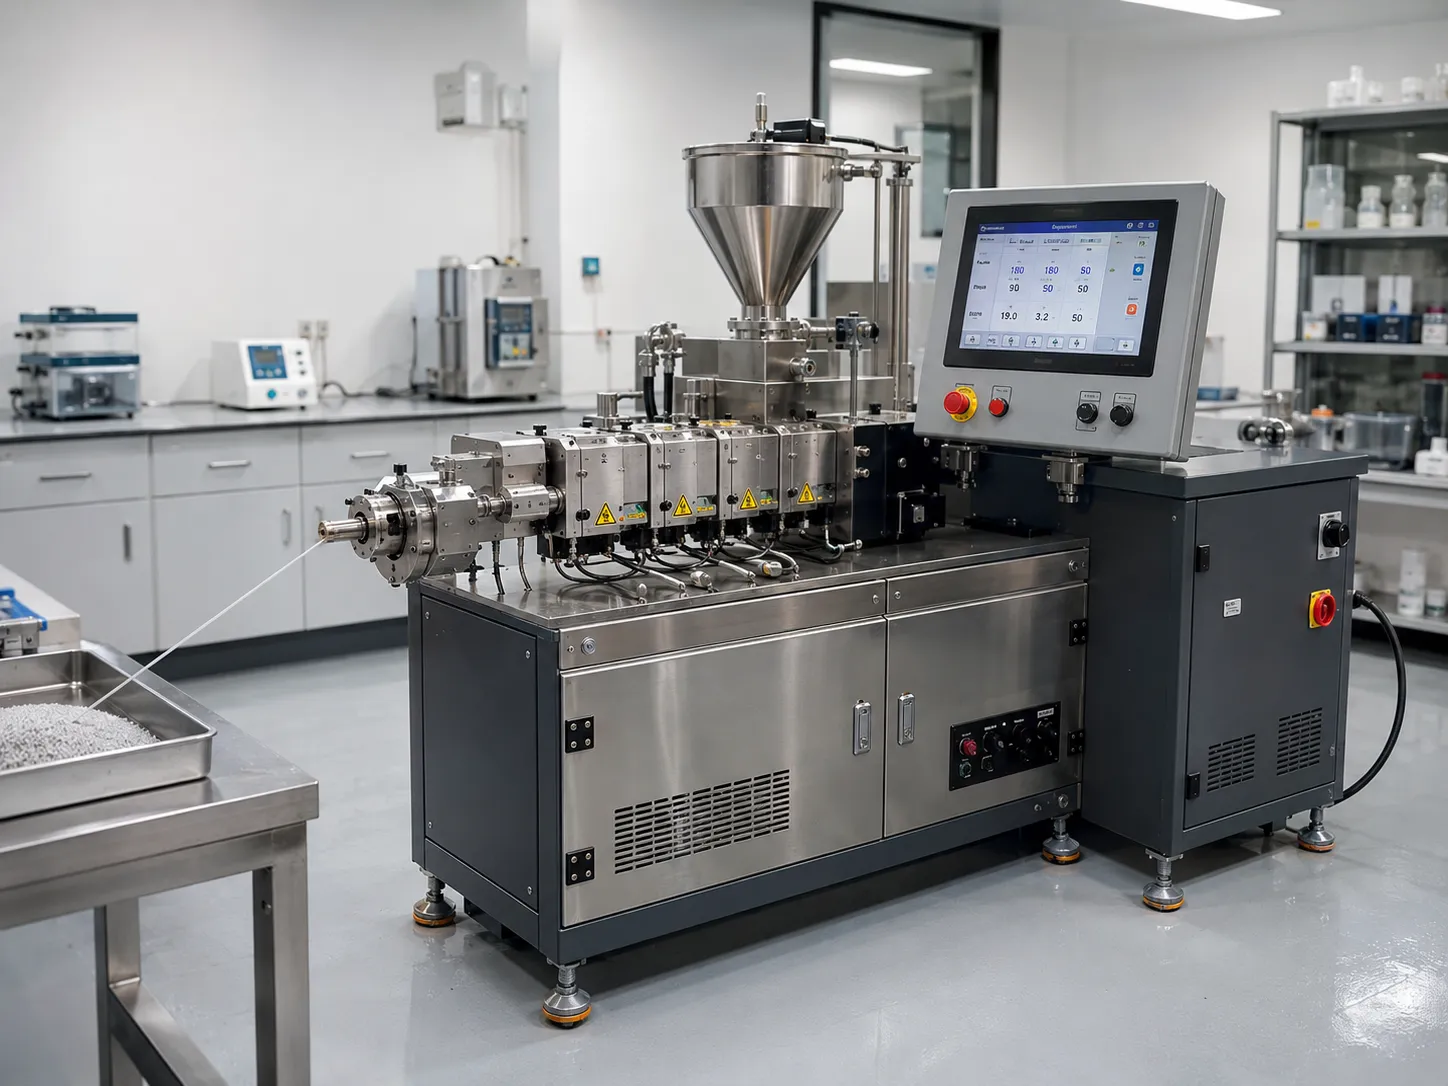
R&D Scale
Laboratory Extruder
Precision benchtop & pilot units, ±0.3°C control — formula testing with 100 g batches, direct scale-up.
View Details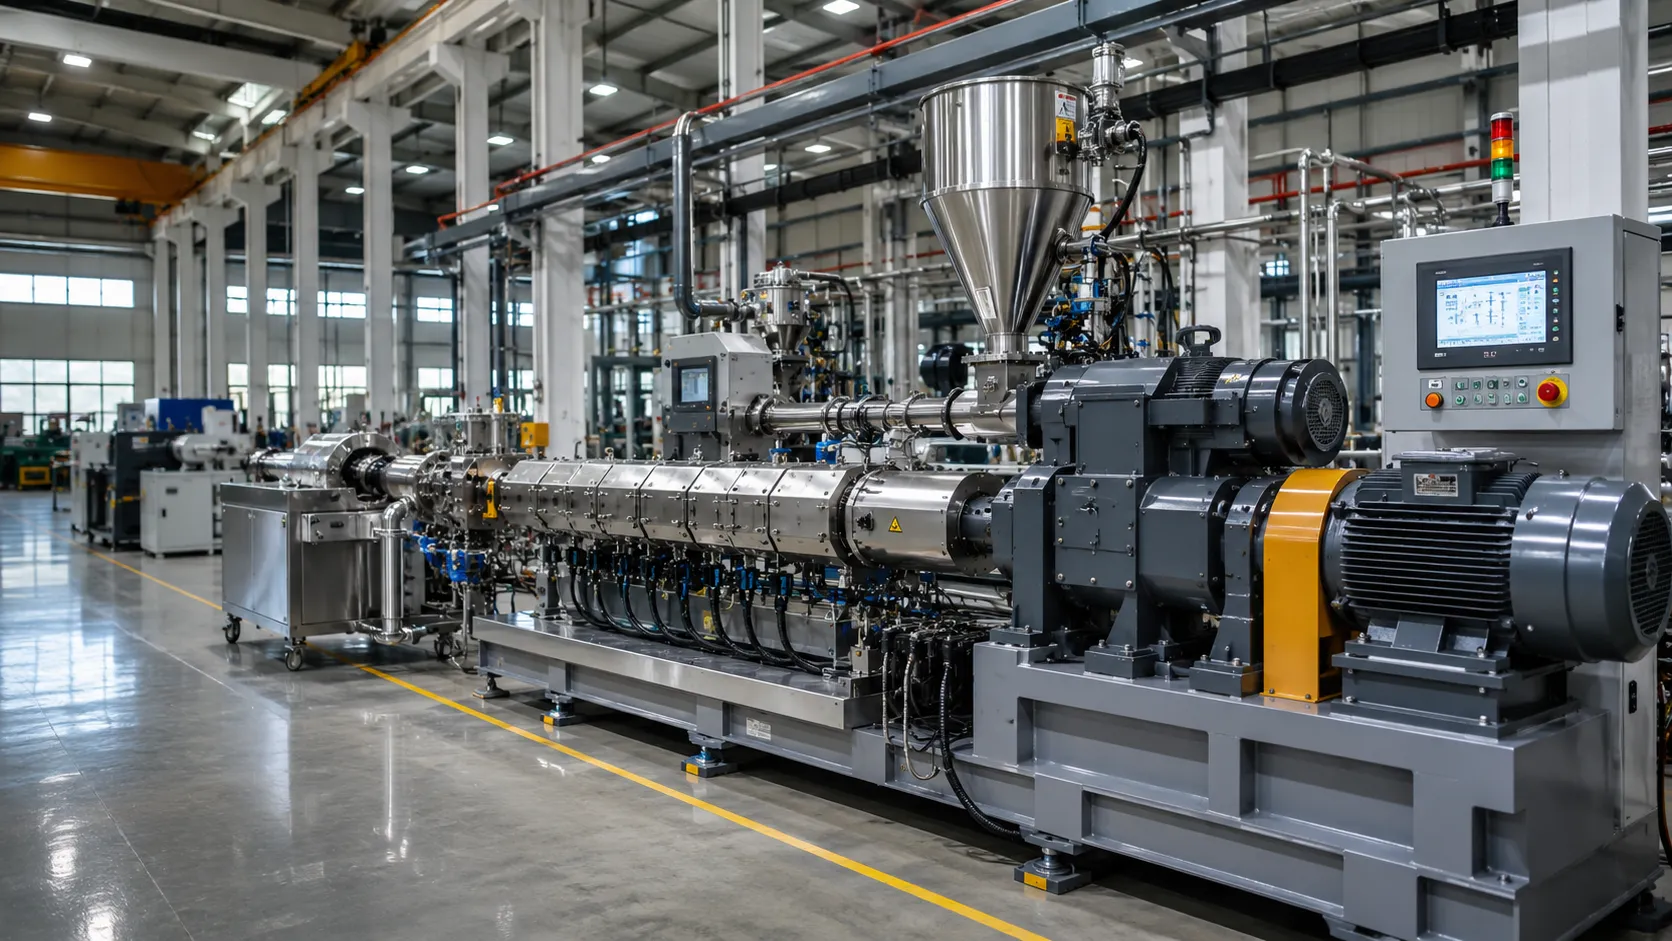
Advanced Process
Reactive Extruder
Continuous polymerization, grafting and devolatilization — replaces batch reactors at 30–40% lower energy.
View Details
Technical FAQ
Triple Screw Extruder Questions, Answered
Written by UET application engineers with 20+ years of compounding experience
A triple screw extruder is a compounding machine with three co-rotating, intermeshing screws arranged in line. The three-screw geometry creates two meshing zones instead of one, roughly doubling the mixing and dispersion performance of a same-size twin screw extruder.
Material enters the enlarged free-volume hopper and is positively conveyed by three synchronized screws. In the barrel, dual meshing zones apply repeated shear to melt, mix and homogenize the polymer; vent ports strip volatiles; zoned PID heating holds ±1.5°C; finally the melt is pushed through the die head for pelletizing.
The triple screw extruder adds a third intermeshing screw: +30% mixing uniformity, 20–40% higher output at the same screw diameter, ~20% lower specific energy and better self-cleaning. Twin screw remains the economical choice for standard compounding.
The UET triple screw extruder processes PE, PP, PA, PET, ABS and PC, plus modified plastics, biodegradable resins (PLA, PBAT), thermoplastic elastomers, cable compounds, PVC and high-viscosity formulations.
Yes. Fill levels of 60–80% — CaCO₃, talc, glass fiber, carbon black — run stably on the UET triple screw extruder. The intermeshing design and enlarged feed volume prevent bridging and agglomeration.
The extra meshing zone transfers mechanical shear into the melt more efficiently, and the larger heat-transfer surface reduces heater demand. Measured specific energy drops about 20% versus twin screw.
Each barrel zone runs an independent PID heating/cooling loop holding melt temperature within ±1.5°C. This protects heat-sensitive resins such as PLA, PBAT and medical-grade polymers from thermal degradation.
Match by output and material: UET-29 for lab R&D; UET-37/45 for small color & additive masterbatch; UET-53/63 for filler masterbatch and engineering plastics; UET-74 for cable compounds; UET-92 for large biodegradable lines.
18 months on the whole machine and 24 months on core components (screws, barrels, gearbox). Standard models ship in 1–2 weeks; customized lines take 4–6 weeks; international shipping adds 7–15 days.
Four items: ① material & recipe, ② target output (kg/h), ③ final product & dimensions, ④ plant power standard (e.g. 380V/50Hz/3-phase). Submit the form to receive a transparent, itemized quotation within 2 hours.